


The number nobody measures
Ask what decides whether a soft seated ball valve seals and the answer given is usually the seat material, the surface finish, or the pressure that energises the seat. All three matter. None of them is the quantity that actually varies between two valves built to the same drawing on the same day, and that quantity has no line on the drawing at all: it is the amount by which the seat insert is compressed when the valve is closed up.
That compression is not designed, and it is not the figure implied by a seat material data sheet. It is a residual, left over after a chain of dimensions has been subtracted from another chain of dimensions, and the chain is long enough that the ball valve seat squeeze differs from valve to valve even when every part is inside its tolerance. Two valves that are dimensionally identical on paper can therefore leave the factory with one seat squeezed enough to hold a gas test and the other barely touching, and neither is out of specification, because no specification states the value.
This is what ball valve tolerance stack-up means in practice, and it explains three things that are otherwise attributed to workmanship: why a batch of valves has a spread of operating torque, why a spare ball can make a good valve leak, and why a valve that passed a seat test in the workshop can fail its first seat test on site.
The chain, part by part
Start at the pocket and work outward. The seat pocket is machined into the body, and its depth is one dimension with its own tolerance. The seat ring sits in the pocket and has a height, which is a second dimension. The soft insert sits in the ring and protrudes by a third dimension, which is created by the ring's internal depth. The ball has a diameter, and the diameter is a tolerance band rather than a number. On the other side of the valve the same three dimensions repeat, and in a split body construction the position of the end cap relative to the body enters the chain as well, along with whatever sits between the two body faces.
When the valve is closed up, those dimensions compete. The ball's diameter plus two insert protrusions has to fit inside the space left by two pocket depths plus two ring heights plus the body joint. Whatever is left over is taken up by compressing the inserts, and if the sum of the parts is larger than the space, the surplus becomes seat load that the bolts or the body threads have to absorb. What looks like ball valve assembly clearance on the drawing is in fact the space the inserts are expected to fill, and the valve does not choose how much of it they fill; the arithmetic does.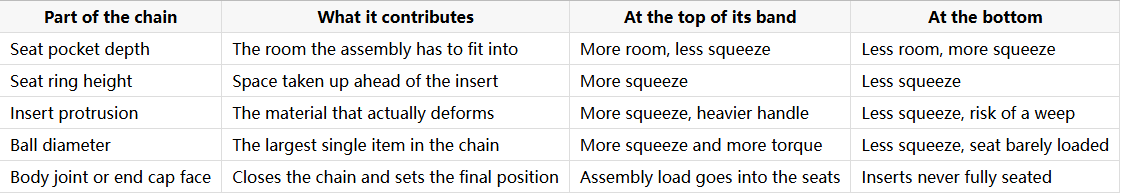
Two details make the chain worse than it looks. The first is that the tolerances do not all point the same way. A ball at the top of its band and inserts at the bottom of theirs give a large compression, and the same valve with the bands reversed gives almost none, which means the extremes are additive rather than self-cancelling. The second is that some of the chain is not a machined dimension at all: the body joint closes on a gasket or on metal-to-metal contact, and the amount it closes depends on how hard it was pulled up, which is why the stack in a split body valve includes the assembly operation.
Worst case, and the arithmetic nobody builds to
If every part in the chain sat at the limit that reduces compression, the valve would not seal. If every part sat at the limit that increases it, the valve would be stiff, and the seats would be compressed past the point where they can recover. A design that added up the extremes and demanded that both cases work would need tolerances so tight that the valve could not be built at a sensible cost, so the arithmetic is never done that way in production.
What happens instead is that the parts are made to comfortable individual tolerances, and the assembly is arranged so that the two bad extremes do not usually meet. In practice that means the distribution of squeeze across a batch is a bell rather than a range, with most valves in the middle and a few at each end. The ones at the ends are the ones that generate the complaints: the occasional valve that weeps on a gas test and the occasional valve that needs a bar on the handle, from the same order, with the same part numbers.
This is also why a drawing review that checks each dimension separately will pass a design that cannot be built consistently. Every dimension can be defensible and the chain still too long. The number of parts in series matters more than the width of any single tolerance, and that is a design decision rather than a manufacturing one.
Select fit: what the workshop does instead
The standard answer in a factory that builds ball valves well is not a tighter tolerance on the ball. It is to stop treating the seat insert as a single part number and to start treating it as a set: inserts made in a small number of thicknesses, with the fitter measuring the ball and the pocket and choosing the insert that lands the ball valve seat compression where it belongs.
That practice is sometimes described by buyers as a sign of loose manufacturing, which is the wrong reading. Select fit is what makes a wide tolerance affordable: the machining is allowed to be ordinary because the last step in assembly measures what actually arrived and compensates for it. A factory that instead insists on one nominal insert and holds every other dimension tight is buying the same result with more scrap.
What select fit requires is a record. The ball diameter and the insert thickness have to be written down against the serial number, because the moment they are not, the valve becomes unrepeatable: a repair years later has no idea what it is replacing, and a ball valve repair becomes a guess. This is the one place where paperwork genuinely changes the outcome rather than documenting it.
What changes the stack after delivery
The chain is fixed at assembly and then quietly altered by everything that happens afterwards, which is why a valve that worked for years can stop sealing after a maintenance intervention that replaced one part.
A new ball is the most common disturbance. Balls are supplied to a diameter band, and the new one is unlikely to sit at the same point in that band as the one it replaces. A ball at the top of the band with the original inserts gives more compression and a heavier handle; a ball at the bottom gives less and can turn a marginal seat into a leaking one. Neither is a defective ball, and neither is a defective seat.
A re-polished ball disturbs the stack in the same direction but further, because polishing removes material from the sphere and returns a ball that is smaller than the one that came out. Putting it back with the original inserts removes compression, and putting it back with a new insert of nominal thickness may still leave the assembly short, because the insert cannot know the ball changed.
Swapping end caps or body halves between valves is the third disturbance, and it is more common in workshops than anyone admits. The pocket depth belongs to the body half it was machined in, and the pair that was measured and recorded at the factory is not the pair being assembled. A ball valve rebuild that mixes parts from two valves has a stack that nobody has ever computed, and the resulting torque or leak is not traceable to any single component.
The fourth is the insert itself. A replacement ball valve spare parts kit normally supplies the insert at nominal thickness, which is correct for a new valve and only approximately correct for a used one, because the ring it sits in has also worn and the pocket has been cleaned of whatever had accumulated in it. The dimension that was recorded at build is the only way to know whether nominal still lands in the right place.
Temperature moves the same stack
Every part in the chain has its own response to heat, and the parts are not the same material. The body is frequently carbon steel, the ball is stainless, the insert is a polymer, and the ring may be stainless or a bronze. Each one grows differently, so the residual that was set at ambient is not the residual the valve has at its working temperature.
Two consequences follow, and they pull in opposite directions depending on the design. A polymer insert grows more than the steel around it, which increases compression as the valve heats, and that is one reason a valve can become difficult to operate at temperature without anything having worn. A metal seated valve has the opposite problem: the clearance that the seat needs in order to work at temperature is a designed gap rather than a squeeze, and if it is set at ambient the valve will either bind when hot or leak when cold. This is why the thermal clearance in a metal seated valve is specified at the working condition, and why a room temperature measurement of that gap proves very little.
For the buyer, the practical point is that a stack computed at ambient is only half a design. The temperature at which the valve must seal is part of the requirement, and it belongs in the enquiry next to the pressure class, because it changes which residual the factory is aiming for.
Why two identical valves feel different
Operating torque is the most visible symptom of the stack and the least reliable measurement of it. Two valves of the same size, class and construction will not feel the same, and the difference is not a quality signal: it is the band. Within a batch, the torque spread comes from the position of each part in its tolerance range, from the friction in the pocket, and from how much the insert was compressed when the body was closed.
What matters is not the spread but the position of the whole population. A batch that is uniformly heavy has a stack biased towards compression, which points at an insert thickness that is too generous or a pocket machined shallow, and it is a production question with a production answer. A single valve that is heavy among light ones is a stack question about that valve, and the answer is in the record, not in the handle.
The same applies to a valve that leaks. A leak on a valve with an undamaged seat face and a clean ball is a squeeze problem, not a wear problem: the ball valve seat interference between ball and insert is too small, and no amount of lapping will fix it. Lapping removes material from the band, which reduces the interference further; the repair makes the arithmetic worse while looking like it addresses the symptom.
What to measure, and what feel is worth
Four measurements describe the stack well enough to act on. The ball diameter, taken at more than one latitude because a ball can be round in one direction and not in another. The insert thickness, taken with a flat micrometer rather than a caliper, because a soft insert deforms under a pointed anvil and the reading will be wrong in the direction that matters. The ball valve pocket depth, taken from the pocket floor to the body face. And the contact pattern, taken with marking compound against the seat, which is the only one of the four that shows what the assembled valve actually did.
The contact pattern is the check that ties the arithmetic to the result. A band that prints across the whole seat face means the parts are concentric and the load is spread; a band that prints only at the outer edge or only at the inner edge means the geometry is wrong even if every dimension is inside tolerance. Ball seat lapping and blue checking are usually described as a way to achieve a leakage class, and they are equally a way to see whether the stack landed where it was supposed to.
Feel is worth nothing in this context. A handle that is easy to move can indicate a correct stack, an under-compressed stack, or a valve with no pressure on it, and an experienced fitter cannot separate those three by hand. The measurement takes a minute per valve and settles the question.
What can be specified, and what cannot
The squeeze itself cannot be specified on an enquiry, because it is not a feature of the delivered object that anyone can check without disassembling it. What can be specified is the chain: the pocket depth with its tolerance, the insert thickness with its tolerance, the ball diameter band, and the requirement that the assembly be measured and recorded. Those four items define the stack, and a supplier who works to them will deliver a consistent valve even if the individual numbers are unremarkable.
Three things are worth adding to a specification because they are where stacks go wrong in service. The first is that spare inserts are to be supplied against the recorded build dimension rather than at nominal thickness. The second is that a replacement ball is to be supplied within the band that the original was built to, not merely within the general tolerance. The third is that body halves and end caps are to be kept as matched sets, because a rebuild that mixes them produces a stack that was never designed.
None of this appears in a catalogue, and none of it shows up in a seat test on a new valve. It shows up two years later as a valve that will not isolate, or one that cannot be turned, on a line where nothing else has changed.
Frequently Asked Questions
What is tolerance stack-up in a ball valve? It is the sum of the dimensional tolerances between the seat pocket in the body, the seat ring, the soft insert, the ball and the body joint. No single one of those dimensions sets how far the seat is compressed; the residual left after the chain is closed up does. Because each part varies within its band, two valves built to the same drawing can end up with different seat squeeze.
Why do two identical ball valves have different torque? Because the parts inside them sit at different points in their tolerance bands, and because the friction between the seat ring and its pocket differs. The resulting seat squeeze and therefore the breakaway torque vary from valve to valve even when every part is in specification. A spread across a batch is normal; a batch that is uniformly heavy points at a stack bias in production.
Can a leaking seat with no visible damage be repaired by lapping? Usually not, and lapping can make it worse. If the seat face and the ball are undamaged, the leak is a compression problem: the interference between ball and insert is too small. Lapping removes material and reduces it further. The repair is to re-establish the interference, by measuring the parts and fitting an insert that restores it.
Does a new ball change the seat compression? Yes, and that is the most common cause of a valve that starts leaking after a ball replacement. A new ball sits somewhere in its diameter band, and the original insert was matched to the ball that came out. A ball at the lower end of the band reduces the interference, and the seat that was marginal before the repair becomes a leak after it.
How is the correct squeeze confirmed in the workshop? By measuring the parts and then checking the assembled result. The ball diameter, the insert thickness and the pocket depth are recorded, and the contact pattern is printed with marking compound to show whether the band is continuous and centred. Feel is not a check: an easy handle is equally consistent with a correct stack and with no load on the seat at all.
The number nobody measures
Ask what decides whether a soft seated ball valve seals and the answer given is usually the seat material, the surface finish, or the pressure that energises the seat. All three matter. None of them is the quantity that actually varies between two valves built to the same drawing on the same day, and that quantity has no line on the drawing at all: it is the amount by which the seat insert is compressed when the valve is closed up.
That compression is not designed, and it is not the figure implied by a seat material data sheet. It is a residual, left over after a chain of dimensions has been subtracted from another chain of dimensions, and the chain is long enough that the ball valve seat squeeze differs from valve to valve even when every part is inside its tolerance. Two valves that are dimensionally identical on paper can therefore leave the factory with one seat squeezed enough to hold a gas test and the other barely touching, and neither is out of specification, because no specification states the value.
This is what ball valve tolerance stack-up means in practice, and it explains three things that are otherwise attributed to workmanship: why a batch of valves has a spread of operating torque, why a spare ball can make a good valve leak, and why a valve that passed a seat test in the workshop can fail its first seat test on site.
The chain, part by part
Start at the pocket and work outward. The seat pocket is machined into the body, and its depth is one dimension with its own tolerance. The seat ring sits in the pocket and has a height, which is a second dimension. The soft insert sits in the ring and protrudes by a third dimension, which is created by the ring's internal depth. The ball has a diameter, and the diameter is a tolerance band rather than a number. On the other side of the valve the same three dimensions repeat, and in a split body construction the position of the end cap relative to the body enters the chain as well, along with whatever sits between the two body faces.
When the valve is closed up, those dimensions compete. The ball's diameter plus two insert protrusions has to fit inside the space left by two pocket depths plus two ring heights plus the body joint. Whatever is left over is taken up by compressing the inserts, and if the sum of the parts is larger than the space, the surplus becomes seat load that the bolts or the body threads have to absorb. What looks like ball valve assembly clearance on the drawing is in fact the space the inserts are expected to fill, and the valve does not choose how much of it they fill; the arithmetic does.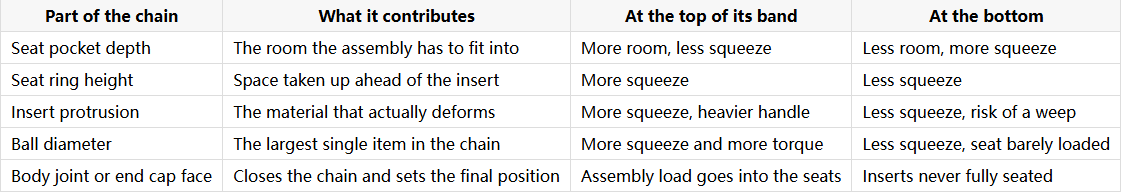
Two details make the chain worse than it looks. The first is that the tolerances do not all point the same way. A ball at the top of its band and inserts at the bottom of theirs give a large compression, and the same valve with the bands reversed gives almost none, which means the extremes are additive rather than self-cancelling. The second is that some of the chain is not a machined dimension at all: the body joint closes on a gasket or on metal-to-metal contact, and the amount it closes depends on how hard it was pulled up, which is why the stack in a split body valve includes the assembly operation.
Worst case, and the arithmetic nobody builds to
If every part in the chain sat at the limit that reduces compression, the valve would not seal. If every part sat at the limit that increases it, the valve would be stiff, and the seats would be compressed past the point where they can recover. A design that added up the extremes and demanded that both cases work would need tolerances so tight that the valve could not be built at a sensible cost, so the arithmetic is never done that way in production.
What happens instead is that the parts are made to comfortable individual tolerances, and the assembly is arranged so that the two bad extremes do not usually meet. In practice that means the distribution of squeeze across a batch is a bell rather than a range, with most valves in the middle and a few at each end. The ones at the ends are the ones that generate the complaints: the occasional valve that weeps on a gas test and the occasional valve that needs a bar on the handle, from the same order, with the same part numbers.
This is also why a drawing review that checks each dimension separately will pass a design that cannot be built consistently. Every dimension can be defensible and the chain still too long. The number of parts in series matters more than the width of any single tolerance, and that is a design decision rather than a manufacturing one.
Select fit: what the workshop does instead
The standard answer in a factory that builds ball valves well is not a tighter tolerance on the ball. It is to stop treating the seat insert as a single part number and to start treating it as a set: inserts made in a small number of thicknesses, with the fitter measuring the ball and the pocket and choosing the insert that lands the ball valve seat compression where it belongs.
That practice is sometimes described by buyers as a sign of loose manufacturing, which is the wrong reading. Select fit is what makes a wide tolerance affordable: the machining is allowed to be ordinary because the last step in assembly measures what actually arrived and compensates for it. A factory that instead insists on one nominal insert and holds every other dimension tight is buying the same result with more scrap.
What select fit requires is a record. The ball diameter and the insert thickness have to be written down against the serial number, because the moment they are not, the valve becomes unrepeatable: a repair years later has no idea what it is replacing, and a ball valve repair becomes a guess. This is the one place where paperwork genuinely changes the outcome rather than documenting it.
What changes the stack after delivery
The chain is fixed at assembly and then quietly altered by everything that happens afterwards, which is why a valve that worked for years can stop sealing after a maintenance intervention that replaced one part.
A new ball is the most common disturbance. Balls are supplied to a diameter band, and the new one is unlikely to sit at the same point in that band as the one it replaces. A ball at the top of the band with the original inserts gives more compression and a heavier handle; a ball at the bottom gives less and can turn a marginal seat into a leaking one. Neither is a defective ball, and neither is a defective seat.
A re-polished ball disturbs the stack in the same direction but further, because polishing removes material from the sphere and returns a ball that is smaller than the one that came out. Putting it back with the original inserts removes compression, and putting it back with a new insert of nominal thickness may still leave the assembly short, because the insert cannot know the ball changed.
Swapping end caps or body halves between valves is the third disturbance, and it is more common in workshops than anyone admits. The pocket depth belongs to the body half it was machined in, and the pair that was measured and recorded at the factory is not the pair being assembled. A ball valve rebuild that mixes parts from two valves has a stack that nobody has ever computed, and the resulting torque or leak is not traceable to any single component.
The fourth is the insert itself. A replacement ball valve spare parts kit normally supplies the insert at nominal thickness, which is correct for a new valve and only approximately correct for a used one, because the ring it sits in has also worn and the pocket has been cleaned of whatever had accumulated in it. The dimension that was recorded at build is the only way to know whether nominal still lands in the right place.
Temperature moves the same stack
Every part in the chain has its own response to heat, and the parts are not the same material. The body is frequently carbon steel, the ball is stainless, the insert is a polymer, and the ring may be stainless or a bronze. Each one grows differently, so the residual that was set at ambient is not the residual the valve has at its working temperature.
Two consequences follow, and they pull in opposite directions depending on the design. A polymer insert grows more than the steel around it, which increases compression as the valve heats, and that is one reason a valve can become difficult to operate at temperature without anything having worn. A metal seated valve has the opposite problem: the clearance that the seat needs in order to work at temperature is a designed gap rather than a squeeze, and if it is set at ambient the valve will either bind when hot or leak when cold. This is why the thermal clearance in a metal seated valve is specified at the working condition, and why a room temperature measurement of that gap proves very little.
For the buyer, the practical point is that a stack computed at ambient is only half a design. The temperature at which the valve must seal is part of the requirement, and it belongs in the enquiry next to the pressure class, because it changes which residual the factory is aiming for.
Why two identical valves feel different
Operating torque is the most visible symptom of the stack and the least reliable measurement of it. Two valves of the same size, class and construction will not feel the same, and the difference is not a quality signal: it is the band. Within a batch, the torque spread comes from the position of each part in its tolerance range, from the friction in the pocket, and from how much the insert was compressed when the body was closed.
What matters is not the spread but the position of the whole population. A batch that is uniformly heavy has a stack biased towards compression, which points at an insert thickness that is too generous or a pocket machined shallow, and it is a production question with a production answer. A single valve that is heavy among light ones is a stack question about that valve, and the answer is in the record, not in the handle.
The same applies to a valve that leaks. A leak on a valve with an undamaged seat face and a clean ball is a squeeze problem, not a wear problem: the ball valve seat interference between ball and insert is too small, and no amount of lapping will fix it. Lapping removes material from the band, which reduces the interference further; the repair makes the arithmetic worse while looking like it addresses the symptom.
What to measure, and what feel is worth
Four measurements describe the stack well enough to act on. The ball diameter, taken at more than one latitude because a ball can be round in one direction and not in another. The insert thickness, taken with a flat micrometer rather than a caliper, because a soft insert deforms under a pointed anvil and the reading will be wrong in the direction that matters. The ball valve pocket depth, taken from the pocket floor to the body face. And the contact pattern, taken with marking compound against the seat, which is the only one of the four that shows what the assembled valve actually did.
The contact pattern is the check that ties the arithmetic to the result. A band that prints across the whole seat face means the parts are concentric and the load is spread; a band that prints only at the outer edge or only at the inner edge means the geometry is wrong even if every dimension is inside tolerance. Ball seat lapping and blue checking are usually described as a way to achieve a leakage class, and they are equally a way to see whether the stack landed where it was supposed to.
Feel is worth nothing in this context. A handle that is easy to move can indicate a correct stack, an under-compressed stack, or a valve with no pressure on it, and an experienced fitter cannot separate those three by hand. The measurement takes a minute per valve and settles the question.
What can be specified, and what cannot
The squeeze itself cannot be specified on an enquiry, because it is not a feature of the delivered object that anyone can check without disassembling it. What can be specified is the chain: the pocket depth with its tolerance, the insert thickness with its tolerance, the ball diameter band, and the requirement that the assembly be measured and recorded. Those four items define the stack, and a supplier who works to them will deliver a consistent valve even if the individual numbers are unremarkable.
Three things are worth adding to a specification because they are where stacks go wrong in service. The first is that spare inserts are to be supplied against the recorded build dimension rather than at nominal thickness. The second is that a replacement ball is to be supplied within the band that the original was built to, not merely within the general tolerance. The third is that body halves and end caps are to be kept as matched sets, because a rebuild that mixes them produces a stack that was never designed.
None of this appears in a catalogue, and none of it shows up in a seat test on a new valve. It shows up two years later as a valve that will not isolate, or one that cannot be turned, on a line where nothing else has changed.
Frequently Asked Questions
What is tolerance stack-up in a ball valve? It is the sum of the dimensional tolerances between the seat pocket in the body, the seat ring, the soft insert, the ball and the body joint. No single one of those dimensions sets how far the seat is compressed; the residual left after the chain is closed up does. Because each part varies within its band, two valves built to the same drawing can end up with different seat squeeze.
Why do two identical ball valves have different torque? Because the parts inside them sit at different points in their tolerance bands, and because the friction between the seat ring and its pocket differs. The resulting seat squeeze and therefore the breakaway torque vary from valve to valve even when every part is in specification. A spread across a batch is normal; a batch that is uniformly heavy points at a stack bias in production.
Can a leaking seat with no visible damage be repaired by lapping? Usually not, and lapping can make it worse. If the seat face and the ball are undamaged, the leak is a compression problem: the interference between ball and insert is too small. Lapping removes material and reduces it further. The repair is to re-establish the interference, by measuring the parts and fitting an insert that restores it.
Does a new ball change the seat compression? Yes, and that is the most common cause of a valve that starts leaking after a ball replacement. A new ball sits somewhere in its diameter band, and the original insert was matched to the ball that came out. A ball at the lower end of the band reduces the interference, and the seat that was marginal before the repair becomes a leak after it.
How is the correct squeeze confirmed in the workshop? By measuring the parts and then checking the assembled result. The ball diameter, the insert thickness and the pocket depth are recorded, and the contact pattern is printed with marking compound to show whether the band is continuous and centred. Feel is not a check: an easy handle is equally consistent with a correct stack and with no load on the seat at all.


