


Two tests, one valve, two different questions
Every ball valve leaves the works having been tested. The shop test follows a valve standard, and the shape of it is always the same: a shell test at one and a half times the rated pressure to prove the body, and a seat test at a little above the rating to prove the closure. The valve is the object of that test. It sits on a bench, capped at both ends, filled with clean water, and a technician watches two seats and a gland for a defined interval. Nothing else is in the circuit.
A line hydrotest is a different event with a similar name. The pipe is the object. The valve is one of the components bolted into it, and the test pressure is set from the line's design pressure rather than from the valve's rating. The hydrotest pressure therefore follows the line and not the valve, and the governing rule in piping practice is that no component may be pushed above what it is rated for at the test temperature, which is a sensible rule and also the reason the valve ends up being the part that limits the test. Where the line's design pressure was chosen to match the flange class of the valve, the test pressure arrives close to the valve's own shell test figure, and at that point the valve is no longer being tested. It is holding the test.
The phrase ball valve hydrostatic test covers both events, and almost every disagreement about a damaged seat starts with the two being treated as one. A valve that passed its own test in Wenzhou can be damaged by a test in Rotterdam without anything being wrong with either the valve or the procedure, because the two tests ask different questions of the same part. This article is about the second one, the field test, and about the four places where it touches the valve: the direction of the pressure, the level of it, the water, and the way it is released.
What makes the subject worth a full treatment is that the damage is not visible. A seat that has been overloaded does not crack or tear in a way anyone sees at the flange. It creeps, takes a set, and comes back slightly thinner than it went in. The valve passes the handover, goes into service, and weeps four months later, at which point the seat is the only evidence and the test is a memory.
A seat only knows one direction
A floating ball valve seals because the line pressure does the work. The ball sits loose between two rings, the pressure on the upstream side pushes the ball downstream until it seats, and the downstream ring is held against the ball by that same pressure. The upstream ring is the other half of the arrangement: it is held by its own preload and by whatever pressure finds its way behind the ring. This asymmetry is the design, not a compromise. It is why a floating valve holds a high differential so well with a seat that would be too soft to do it by preload alone.
The floating pattern J-VALVES builds, from half an inch to eight inches in the screwed and flanged stainless bodies, works on that principle, and so does every other floating valve in the world. The trunnion pattern, from two inches to fifty-six inches in the API 6D range, changes the mechanism but not the logic: the ball is carried on trunnion bearings, each seat is a spring-loaded piston, and each seat is designed to be pressed on by pressure arriving from its own side. A trunnion seat is normally self-relieving as well, lifting when the cavity pressure exceeds the line pressure by a set amount, which is a feature that only exists because the seat is a piston with a defined direction.
Now put the pressure on from the other side. It happens more often than the procedure admits: a test flange fitted at the far end of a section, a section tested against a valve that has a live line behind it, a cavity that was filled before the test and not vented, a seat that is asked to hold while the other side is drained. In every one of those cases the seat that is supposed to be pushed onto the ball is being pushed off it, and the only thing keeping contact is a spring and the elasticity of the ring. That configuration is not what the shop seat test measured. The shop test measured the seat in the direction it was designed to work.
What the extra pressure does to a soft seat
Seat load is the differential multiplied by the area it acts on, and the differential a seat is allowed to see is bounded by the class the body was bought in rather than by the line's design pressure, which is the distinction behind the pressure class and its derating. Raise the differential by half and the load on the ring rises by half, and that is the mild version of the story. The stronger version is that the load is now being carried for hours rather than for the few minutes of a shop test, at whatever temperature the test water happens to be, with no opportunity for the ring to recover between holds.
PTFE and RPTFE do not fail under that load. They creep. The ring takes a permanent set, thins where it is loaded, and flows slightly into the clearance behind it. When the pressure comes off, the ring does not return to its original height, and the interference that made the seal is now smaller than the one the valve was assembled with. The valve still passes a seat test at a low differential, which is exactly why the shop record looks clean and the field complaint looks inexplicable. The leak arrives at working pressure, usually after a thermal cycle has taken the last of the resilience out of the ring.
This is the mechanism behind most ball valve seat damage that gets blamed on the manufacturer. The ring was asked to carry, for a whole afternoon, a load it was designed to see only inside the shell test, and it behaved exactly as a viscoelastic material behaves. Nothing in the valve was out of specification. The test was simply outside the envelope the seat was designed for, and no one wrote that envelope on the test pack.
The practical consequence for a buyer is that the ball valve seat test after the line test should be run at the valve's own rating, with clean water, in the direction the seat works, and recorded separately from the line test. Two tests, two records. A single line on a handover sheet that says the system held pressure tells you nothing about the part that has to seal again tomorrow.
The test water is part of the valve
Test water is usually whatever the site has. Project specifications often put a limit on chlorides in test water for stainless systems, and site water frequently exceeds it, particularly on a coastal plant or where the makeup comes from a brackish source. The result is not a general rusting of the body. It is pitting, and the place it starts is wherever water stands still against a stainless surface with a crevice around it. Which stainless is in the valve matters here only in how much chloride it takes before a pit starts, and the difference between the grades is set out in the comparison of the 304, 316 and 316L bodies.
A ball valve has an unusual number of such places. The seat pocket is an annular gap behind the ring. The cavity under the ball is a volume with only one or two small openings. The stem bore is a blind pocket above the ball. The threads of a plugged drain or vent are a spiral crevice. Every one of these holds water after the line is drained, because draining removes the water that can flow and leaves the water that cannot.
Chlorides in test water do their damage slowly, which is the problem. A pit that begins in a seat pocket during a test in March is a stain on the ring by June and a leak by the following winter, and by then the test water is long gone and the water in the line is clean. The complaint lands on the valve, and the valve is the only part of the system that kept a sample of the test water for six months.
Two habits reduce this to a nuisance. The first is to drain through the drain port rather than through the bore, with the valve in the orientation it will be installed in, so that the low point is the drain. The second is to dry the valve after the test rather than leave it wet: stroke it, blow it through with dry air if the site has it, and leave the bore open. A stainless ball valve after hydrotest should look and smell like a dry valve, not like a valve that has been drained.
Using the valve as the boundary
To hydrotest a closed ball valve is to make one seat into a test blind. It is done constantly, because the alternative is a spool piece, and on a large valve in a tight space the spool is a day of work. That is the arrangement people mean by a ball valve test boundary, and it is worth naming it precisely, because once the seat is the boundary the valve stops being the thing under test and becomes part of the test equipment. The question is not whether it is allowed. The question is what the seat is being asked to do while it happens.
On one side, the full test pressure. On the other, atmosphere. For the duration of the hold, the differential across a single soft ring is the entire test pressure, which is above the figure the seat test used. Then the test is dumped, and the dump is the part that never appears in the procedure. The seat is held against the ball by the differential. When the pressure on one side is released in a few seconds, the differential does not fall to zero; it crosses zero and comes back from the opposite direction. For a moment the seat is being pushed away from the ball, with nothing behind it, and the water that was compressed in the cavity expands through the seat line and carries with it whatever was sitting in the pocket.
A seat can survive the hold and be lifted by the release. It can also be lifted far enough to let a particle of grit or a flake of scale onto the sealing band, which is the same failure by a different route: the valve is closed, the pressure is gone, and the seat now has a mark on it that will not come off. On a three-piece or a top entry body that mark is a maintenance item rather than a replacement, and the point at which a marked seat is changed rather than cleaned is covered in the note on replacing a seat with the valve still in line.
The arrangements that avoid this are simple and none of them weakens the test. Bring the pressure up and down on the side the seat is designed for. Keep the cavity vented while the test runs, so that a leak past the seat shows up as a drip instead of a trapped volume. And if the valve has to serve as the boundary, write that down, because the seat is now part of the test boundary and its condition after the test is part of the test result.
The DBB case
A double block and bleed valve puts two seats and a cavity in one body, with a bleed port on the cavity. Its purpose in service is to let an operator prove that both barriers hold, by closing the valve and opening the bleed. In a test it is the one arrangement where pressure can be trapped between two closed seats with no path to either line.
DBB cavity pressure is the whole reason the design has a bleed, and the bleed is a test instrument as much as a service one. Vent the cavity before pressurising, and leave the vent open to atmosphere with any gauge on it isolated, so that a rise in cavity pressure appears as a drip at the vent rather than as a trapped volume looking for a way out. Never plug a weep at the bleed to get through a test. The weep is the result.
There is a second asymmetry worth knowing. In a DBB valve used as a test boundary, the upstream seat is holding the full test pressure while the downstream seat holds nothing, and both are being asked to do it in a direction that the shop test loaded one at a time. When the test is released, the cavity sees the reversal first, because it is the smallest volume and the only one with a vent that is already open.
The mechanical detail of how those seats relieve, and why the two common variants behave differently when the cavity is full, is set out in the note on the DBB and DIB-1 arrangements. For the purpose of a hydrotest, one rule is enough: the cavity is never a closed volume while pressure is on either side of it.
The drain port is not a convenience
A ball valve drain port is drilled at the lowest point of the cavity for one installed orientation. That is the whole of its design logic, and it is why the port position belongs on the enquiry along with the valve. Rotate the body, and the port is no longer at the low point; the water below it is unreachable, and the pocket that stays wet is the pocket that pits.
This shows up in three common situations. A valve ordered for a horizontal line and installed in a vertical riser, where the drain ends up on the side. A valve installed with the stem down because the actuator had to go underneath, where the drain is now on top and drains nothing. A trunnion valve with two cavity ports, one intended to be up and one down, installed rotated so that both are horizontal and neither does its job.
The first two are ordering errors, not installation errors, and they are cheap to avoid: state the line axis and the stem direction with the enquiry, and the port will be drilled where it belongs. The third is a drawing error and is worth catching at the GA stage, where the port positions, the stem direction and the face to face dimension are all on the same sheet, as set out in the note on reading a GA drawing.
After a test, the drain is also the only way to empty the cavity properly. Draining the bore empties the pipe. It does not empty the volume under the ball, because that volume is connected to the bore only through the clearances around the seats, and those clearances are exactly where the water is held by capillary action.
The sequence that avoids all of it
The sequence that keeps seats out of trouble is not a secret and it is not expensive. It is just rarely written down as a sequence.
Flush first, before the valve is asked to do anything. Construction debris in a new line is abrasive, and a valve stroked with grit in the bore will score the ball and mark the seat before the first day of service. Flush through an open valve, or flush with the valve isolated and a spool in its place, and only then close it.
Test with the valve fully open when the valve is inside the test section. With both sides at the same pressure there is no differential across either seat, the seat is not a boundary, and the test measures the body and the joints, which is what it is for. If the valve has to be closed to divide the section, fit a test flange on the far side and test each side separately, or accept the reduced pressure that the seat is rated for.
Then drain, dry, stroke the valve through a full quarter turn twice, and run the valve's own seat test at its own rating with clean water. That last step is the one that converts a line test into evidence about the valve. Without it, the handover proves the pipe and says nothing about the part that has to close.
What the record should contain
A test record that says the system held pressure answers none of the questions that come up when a seat weeps three months later. Six items make the record useful. The medium, including its chloride content if the system is stainless. The pressure held and the duration. The position of every valve in the circuit during the hold, open, closed, or isolated. Which side of each closed valve the pressure was on. How seat leakage was assessed, whether by bubbles at a vent, by a gauge on an isolated cavity, or by a drop on the pump. And the serial number of the valve, so that the record attaches to a part rather than to a line number.
Six lines on a sheet, written by the person who ran the test, will settle most seat arguments before they start. The alternative is a claim three months later that neither side can prove, which usually ends with the manufacturer replacing a seat that was damaged by a test no one recorded.
Symptoms that arrive later
The failure signatures are consistent enough to be worth knowing, because each one points at a different part of the test rather than at the valve. Brown water on the first stroke means the cavity held test water and the water carried corrosion products with it. Torque above the datasheet at the first operation means the seat took a set under load, or the ball picked up a film in the pocket. A leak that appears only from one direction means the seat that was loaded during the test is the one that has lost its interference. A seat that holds cold and weeps hot means the ring has lost the resilience that used to absorb the differential growth. Pitting found in the pocket at the next overhaul is the slow version of the same story, and it is the one that is easiest to attribute correctly, because the pit is where the water was.
None of these are visible at the moment the test is signed off, and all of them are cheap to prevent at the arrangement stage. The valve is the part of the system that cannot drain itself, cannot dry itself, and cannot tell anyone that it was asked to hold a pressure it was never meant to hold.
Who holds the pressure in each arrangement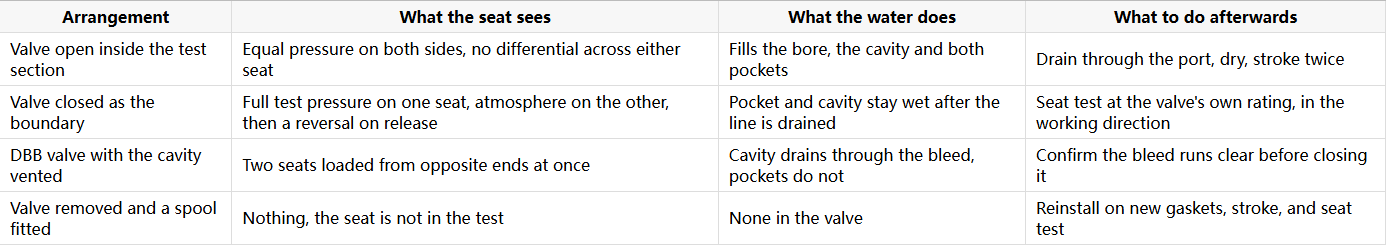
The table is not a ranking. It is a way of seeing that three of the four arrangements put water somewhere the valve cannot reach afterwards, and only one of them loads a seat in a direction it was not designed for. The fourth avoids both and costs a spool.
Frequently Asked Questions
Should a ball valve be open or closed during a hydrostatic test? Open, if the valve is inside the section being tested. With both sides at the same pressure there is no differential across the seats, the seats are not acting as barriers, and the test measures the body and the joints. Closed only if the valve is deliberately being used as the boundary, and in that case the seat is carrying the full test pressure and should be tested again afterwards at its own rating.
Can a hydrotest damage a ball valve seat? Yes, and usually without leaving a mark anyone can see. A soft seat creeps under a load it was not designed to carry for that long, so it comes back thinner and less resilient. The valve still passes a low pressure seat test and weeps later at working pressure. The damage is dimensional rather than visible, which is why the post-test seat test matters more than the visual inspection.
Why did a stainless ball valve show rust after the hydrotest? Almost never because of the steel. Test water carrying chlorides, or carrying free iron from the pipe, stays in the seat pocket, the stem bore and the plugged ports after the line is drained, and that is where the staining starts. The fix is a chloride limit in the test water, draining through the port in the installed orientation, and drying the valve rather than leaving it wet.
Can I use the ball valve as the test boundary? Only if the seat is rated for the pressure being applied and the release is controlled. A better arrangement is a spool piece or a test flange at the far end, so the pressure is equal on both sides of every seat. When the valve must be the boundary, record which side the pressure was on and seat test the valve afterwards.
Does a line hydrotest replace the valve's own test? No. The line test proves the pipe and the joints, and it may never load a seat in its working direction at all. The valve's own test follows the valve standard, with a shell test and a seat test in the direction the seat is designed to work. Two tests, two records, and the second one is the only evidence about the part that has to close in an emergency.


