A valve is never at one temperature
Open the drawing of a ball valve and every part sits at one temperature: the design temperature, written once in the title block, applied to everything inside the outline. In service the same valve carries at least four. There is the medium in the bore. There is the slug of the same medium that stayed in the body cavity after the last closure, which has been sitting there since, exchanging heat with nothing. There is the outer surface of the body, whose temperature is decided by insulation, tracing, sun, wind and the puddle it stands in. And there is the top of the stem, where the packing lives and where the temperature is whatever the neck and the bonnet allow it to be.
Most of the time this does not matter, because most of the time all four have already agreed. A valve that has been in service for a month is at one temperature in the sense that matters: every part has finished expanding, the geometry has settled into whatever it is going to be, and the seat load is the load the pressure and the springs give it. That is the condition every rating, every clearance and every test refers to. It is called steady state, and it is the only condition the paperwork describes.
The trouble lives in the interval before the four agree. That interval is short, it happens at the worst possible moment, and it is the one condition nobody specifies.
What a thermal shock is, and what it is not
The ball valve thermal shock case is a rate problem rather than a level problem, and it starts with a definition. A thermal shock is not a large temperature. A valve that has run for years at the top of its range is not being shocked; it is being cooked slowly and uniformly, and if the materials were chosen for that temperature it will be fine. A thermal shock is a large temperature difference across a wall, arriving faster than the wall can equalize it.
The mechanism is simple once it is stated as a sequence. The medium touches the wetted surface first, because that is where the medium is. The wetted surface therefore changes temperature first, and it changes volume with it. The outer surface is still at the old temperature, and it is still the old size. Between them is a wall of metal that is now trying to be two sizes at once, and metal is not allowed to be two sizes at once, so the two surfaces fight and the fight is measured as stress.
Which surface is in tension depends on the direction of the change, and the rule is worth memorizing because it decides where to look afterwards. When the inside is chilled, the inside wants to shrink and the outside will not let it: the inside is pulled apart, so the inside is in tension. When the inside is heated, the inside wants to grow and the outside will not let it: the inside is compressed and the outside is pulled, so the tension moves to the outside. Both directions are dangerous, and they are dangerous on different surfaces, which is why the same valve can crack on the bore in one plant and on the outer wall in another.
What is not a thermal shock is worth listing too, because three other things get blamed for it. Water freezing inside a closed cavity is not a thermal shock: that is a volume change of the medium against a fixed volume of metal, and the pressure it generates is the whole story. A blocked-in valve left in the sun is not a thermal shock either: the body heats evenly and the cavity pressure rises. And a seat that leaks because the line is hot is usually not a transient at all: that is the steady-state clearance question, which is a separate design calculation and a separate article.
The wall bends before anything cracks
A temperature gradient through a wall does two things, and engineers usually only talk about the first. It creates stress, which is what everybody worries about. It also creates curvature, which is what actually causes the leak.
Take a straight length of wall with one face hotter than the other. The hot face wants to be longer than the cold face. They are joined, so the wall cannot become longer on one side only; instead the whole section rotates, and the wall takes up a curve with the hot face on the outside of it. This is the same effect that makes a pipe with a hot top and a cold bottom bow upward, and it happens in a ball valve body for exactly the same reason.
The body of a ball valve is a short, thick, hollow shape with two seats bored into it and a neck on top. When the bore is chilled and the outside is not, the body bows. The bow does not need to be large. The features that matter in this body are two pockets on one axis with a ball between them, and they have very little tolerance for movement of any kind. A body that has bowed by a barely measurable amount has moved its two seat pockets out of the relationship they were bored in.
That is the sentence to keep: seat pocket alignment is what a gradient spends first, because the two pockets were bored on one axis and a bowed body does not keep them there. Boring both pockets in one setting, from one end or from both ends on the same line, is what makes a ball valve's seats face each other; it is the first operation in the machining sequence and the one the whole assembly depends on. A thermal gradient undoes it elastically, for as long as the gradient lasts.
The two seat pockets are the first thing to notice
A pair of pockets that is no longer quite coaxial does not open a gap, and this is why the failure is so hard to read. The ball is a sphere. A seat ring pressed against a sphere will still touch it all the way round, because a sphere forgives alignment. What changes is where it touches and how hard.
Two things follow. First, the contact band shifts and changes width: it is wider on one side of the seat face and narrower on the opposite side, which changes the unit load there without changing the total load very much. Second, the seat has to travel further in its pocket on one side than the other, so the seat's own secondary seal is asked to accommodate a tilt it was designed to accommodate as a translation. Both effects are reversible. Neither shows up on a bench test, because a bench test is at one temperature.
There is a third effect, and it is the one that gets written up as a mystery. The interference that makes the valve seal is a residual: it is what is left of the seat's designed compression after the pocket depth, the seat height, the insert protrusion, the ball diameter and the joint face have all contributed their tolerances and their expansions. That residual is a small quantity, and the reason a valve that was fine on the bench can be marginal in service is that the residual was already small. A thermal transient spends part of it. The squeeze is a residual, and a residual is the first thing a transient takes away.
The ball follows the medium faster than the body does
The ball is a thin shell or a solid forging sitting in the middle of the flow, wetted on most of its surface, with very little mass compared with the body that surrounds it. The body is a thick casting or forging with a large wall, an insulation jacket on the outside and, often, a pocket of stagnant medium in the cavity that is not being replaced.
Give the two the same medium and the same moment, and they do not arrive together. The ball is at the new temperature while the body is still on its way. On a heat-up that means the ball grows before the pocket does, and the interference at both seats rises at once. On a cool-down the ball shrinks first, and the seat load falls before the body has contributed any of its own contraction.
This is differential expansion, and it is the same physical fact that a metal seated ball valve is designed around, but it is being read at the wrong end. The design calculation asks what the clearance must be at the hot steady state so that the valve does not seize when everything has grown. The transient asks a different question: what is the clearance while the ball is hot and the body is not, and again when the reverse happens. A valve can be correct at both ends of its temperature range and still bind in the middle of the journey.
Why the leak stops on its own
Because most of this is elastic. The gradient is a temporary condition: as the wall equalizes, the curvature goes away, the pockets return to the axis they were bored on, and the seat load returns to the value the pressure and the springs give it. If the only thing that happened was a bend, the leak closes itself and leaves no evidence except a logbook entry and a maintenance team that does not believe the operator.
A ball valve leaking only during a start-up, and sealing itself afterwards, is therefore a timing rather than a mark. The valve leaks during the first part of a start-up, when the medium has arrived and the body has not caught up. It stops without anyone touching it. It passes every subsequent pressure test. It will do the same thing at the next start-up, which is the part that makes it diagnosable: a seat that is damaged fails progressively, and a seat that is distorted by a transient fails identically every time.
There is a second, less happy version. If the transient is severe enough, part of the distortion is not recovered: a seat face takes a set against the tilted ball, a gasket is crushed on one side, or the seat's secondary seal is deformed and stays deformed. The leak then does not stop, and the strip-down shows a seat with an uneven contact band and no scoring. That is the fingerprint of a transient that went past the elastic limit, and it is regularly misdiagnosed as a bad seat lot.
Insulation and tracing make the gradient worse
Everything done to a valve to protect it from the weather also protects it from the medium's attempt to warm it evenly. Insulation slows the outer surface down. Heat tracing holds the outer surface at a temperature of its own choosing. A cold box does the same in the other direction. Each of these is correct on its own terms, and each makes the through-wall gradient larger and longer-lived when the medium changes.
The worst arrangement is the one that looks most carefully engineered: a traced and insulated valve on a line that is emptied and refilled. The tracing keeps the outside warm while the inside is exposed to a cold slug of cleaning fluid, condensate or product from an upstream vessel. The outside cannot follow, because it is being deliberately held where it was. The gradient is not a fault of the tracing; it is the tracing doing its job while the inside does something else.
The extended designs have their own version of this. A cryogenic extended bonnet exists to hold the packing at a temperature it can survive, which means the neck carries a deliberate gradient along its length all the time. That is a designed gradient in a thin column, and it is a different problem from a gradient through a thick wall; but it explains why the same valve can be perfectly stable in continuous cryogenic service and troublesome on the day it is first cooled.
Where it actually breaks
When a thermal transient does produce a crack, it produces it in one of four places, and all four are places where a stress concentration sits on top of a thermal stress.
The neck, at the fillet where the cylindrical stem housing meets the body. This is the thinnest part of the pressure boundary and the part with the least metal around it to carry a gradient, and the fillet that is generous enough for casting is rarely generous enough for a transient.
The body-to-end weld on a welded body, where residual stress from the weld is already present and where the two sides of the joint are different thicknesses, so they heat at different rates as well as expanding differently.
The seat pocket shoulder, where the wall steps from thick to thin in one move and where the seat ring is preloaded against the step.
And the flange, not usually as a crack but as a face that is no longer flat, which is the next section.
Whether any of these becomes a crack rather than a distortion depends on the material's ability to yield, which is the one part of this subject that is written down properly and is not repeated here. A steel that would dent at ambient temperature can fail without warning at a lower one, because the mechanism of failure changes from yielding to cleavage; the low temperature range and its testing are set out on the low temperature ball valve page, and the design temperature on the data sheet is the number that decides which side of that line the valve sits on.
Cracks are the rare outcome; geometry is the common one
A cracked body is memorable, expensive and rare. The ordinary result of a thermal transient is a valve that is out of shape for a while and never announces it.
The flange face is the first casualty, because it is a flat surface on the end of a shape that has just bowed. Two flange faces that were parallel are no longer parallel, the gasket is asked to seal a gap that is now wedge-shaped, and the joint weeps. It weeps on cool-down, when the gradient reverses, and it stops when the line is at temperature. Nobody finds a leak on a cold depressurized valve, which is exactly when the leak is not there.
The bore is the second. A bowed body is an oval bore at the point where the bow is greatest, and an oval bore around a round ball changes the clearance on two opposite sides. On a metal seated valve that clearance is small by design, the valve gets harder to turn at exactly the moment the operator is trying to move it.
The seat pocket squareness is the third. A pocket that is no longer square to the bore tilts the seat ring, which moves the contact band and loads the seat's secondary seal on one side. This is the failure that gets attributed to a bad batch of seats, because the seat comes out of the valve looking worn on one edge and perfect on the other.
All three have the same tell: they are worse during a temperature change and better afterwards, and they are worst on the valves with the thickest walls and the most insulation. Thermal distortion is the ordinary outcome of a start-up, and a body that cracked is the case where the distortion had nowhere to go.
Four things that look like this and are not
The table exists to keep a transient from being blamed for damage it did not do, and to keep real damage from being excused as a transient.
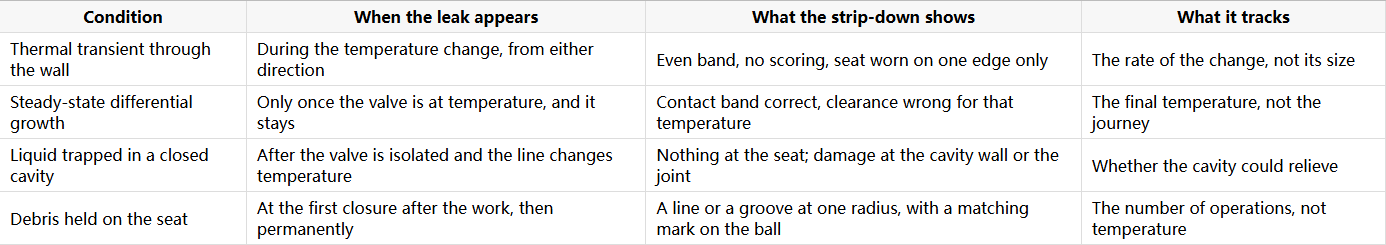
Two of these are regularly confused with each other, so the distinction is worth stating plainly. A transient is a leak that exists while the temperature is moving and disappears when it stops. A steady-state clearance problem is a leak that exists because the temperature has arrived. The first is diagnosed from a trend against a temperature log, the second from a single reading at operating temperature. If the plant has no temperature record, the two cannot be separated afterwards, which is the strongest argument for recording the body temperature during the first start-up.
Why a hydrotest never finds it
Because a hydrotest is the opposite of a thermal transient in every respect that matters. The water is at ambient, the body is at ambient, the test is short, and the pressure is applied slowly and held. The wall is at one temperature throughout, the pockets are on the axis they were bored on, and the seat sees a clean, uniform load. A valve that will leak for the first part of a start-up passes that test without a murmur.
This is worth saying carefully, because it is not an argument against the test. The hydrotest is asking a different question: whether the pressure boundary and the seat can hold at a defined pressure with a defined medium. It answers that question well. A hydrotest is not a simulation of service, and a thermal transient is precisely the part of service that a hydrotest cannot reproduce. Where a transient is a known feature of the duty, the evidence has to come from a temperature-recorded start-up, not from the test bay.
What to do on the line
Four measures, in order of how much they are worth, and none of them costs anything to install.
Change the rate, not the temperature. The gradient is a function of how fast the surface is asked to move, so a start-up that brings the body up over a longer time produces a smaller bow even when the end temperature is identical. A line that is warmed through a small opening, or through a warming connection, does this without any hardware beyond what the piping already has.
Bring the body up before the pressure. Warming an unpressurized valve creates the gradient without the seat load, and the two together are what produce the damage. Pressurizing a cold body and then heating it puts the largest seat load on the least expanded seat.
Drain before the hot medium arrives. A valve holding a slug of cold liquid in its cavity meets the hot medium across a boundary that is inside the body, which is the worst possible geometry for a gradient: the cold is trapped against one wall while the hot flows past the other side of it.
And record it. A start-up log with body temperature against time is the only artefact that can separate a transient from a damaged seat a month later, and it costs one thermocouple and one column in a spreadsheet.
What to specify
A specification that only names a design temperature has not described a thermal transient, because the design temperature is a steady-state number. Four additions make it a real requirement.
State the cycle, not just the range. A valve that is taken from ambient to operating temperature once a year and a valve that is cycled weekly are the same valve on the data sheet and different valves in the wall. Say which one it is, and say whether the line is emptied between cycles.
State the minimum metal temperature, and say that it is a metal temperature rather than a fluid temperature. The two differ during exactly the events this article is about, and the difference is what decides whether a carbon steel body is inside or outside the range where its toughness has to be proven. Where the answer is that the metal can go below the range, the material choice and the impact testing follow from the low temperature range rather than from the fluid temperature on the process sheet.
Ask for the warm-up procedure in the operation and maintenance manual, and read it before the valve is installed rather than after the first leak. A manual that says the valve must be brought to temperature slowly has told you that the design has a transient limit; a manual that says nothing has not told you the valve has no limit.
Where the duty is a genuine thermal cycle going up and down, the geometry choices that survive it are the ones with fewer thick-to-thin transitions: a forged body rather than a cast one where the shape allows, generous fillets at the neck, a seat pocket that does not step in one move, and, where the joint is welded, one whose stress relief is stated on the drawing rather than assumed. None of these removes the gradient. They decide whether the gradient is spent on a bend or on a crack.
Why J-VALVES builds for the cycle, not only for the temperature
J-VALVES builds floating ball valves from 1/2 inch to 8 inch and trunnion mounted ball valves from 2 inch to 56 inch, DN15 to DN1400, in ASME Class 150 to 2500, in carbon steel, stainless steel, duplex and low temperature grades, with soft seats up to the limit of the seat material and metal seats where the duty asks for them. Bodies are forged or cast according to size and shape, seat pockets are bored on a single axis in one setting, and where a body is welded the drawing states whether the joint is stress relieved and in which order the pockets are machined against it.
Shell tests are run at one and a half times the rated pressure to API 598, seat tests to the same standard, with ISO 5208 leakage classes stated on the data sheet, and material certificates to EN 10204 3.1 for body, ball and stem. Where a project has a thermal cycle, the drawing states the minimum metal temperature and the material's toughness requirement follows it, and the warm-up requirement goes into the manual with the valve rather than arriving as a note after commissioning.
A valve cannot be designed to be immune to a gradient. It can be designed so that the gradient produces a bend rather than a crack, and so that the bend is spent somewhere that is not the seat. That is a decision made on the drawing, and it is worth asking for before the first start-up rather than after the first mystery leak.
Frequently Asked Questions
Can a thermal transient crack a ball valve body without any warning? It can, and the reason is the material rather than the valve. A thermal gradient puts one surface into tension, and a steel that would yield at ambient temperature can fail by cleavage at a lower one, with no visible deformation first. That is why the minimum metal temperature, and not the fluid temperature, is the number that decides which material the body is made from.
Why does the valve leak at start-up and then seal itself? Because most of the distortion is elastic. The bore is chilled or heated before the outer wall, the body bows, the seat pockets lose the alignment they were bored with, and the contact band moves. When the wall equalizes, the geometry returns and the leak closes. If the transient was severe enough to take a set in the seat or the gasket, the leak does not close, and the strip-down shows an uneven band with no scoring.
Would a thicker body wall make it safer? No, it makes the gradient worse. A thicker wall holds more restraint, so a given rate of change produces a larger stress, and it takes longer to equalize, so the condition lasts longer. Thickness is there to carry pressure; using it as protection against thermal shock works in the wrong direction.
Is a metal seated valve more or less exposed than a soft seated one? More exposed, for two reasons that have nothing to do with the seat material. The clearance is smaller, so the same distortion uses up a larger share of it, and there is no polymer to absorb an uneven band. A soft seat conforms to a small misalignment and keeps sealing; a metal seat has to hold the alignment it was given.
What is the one record that proves a start-up leak was thermal? Body temperature against time for that start-up, read next to the leak. A leak that begins as the gradient builds and ends as the wall equalizes is thermal. A leak that appears when the valve reaches temperature and stays is a steady-state clearance problem, and the two need completely different answers.