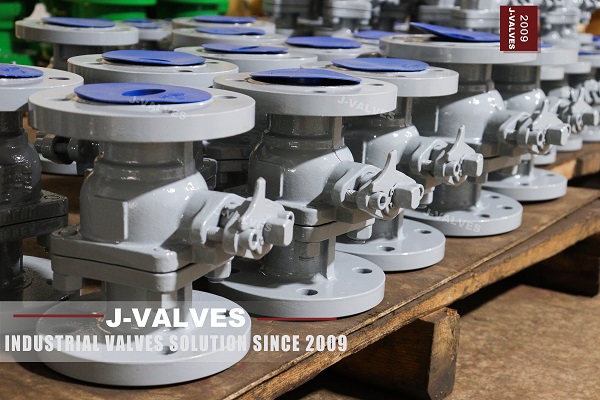
Oil & gas long‑distance pipelines operate under high‑pressure hazardous service. As critical isolation components, improperly selected pipeline valves may cause hazardous media leakage, costly shutdown and safety incidents. Complying with global industry standards API 6D for pipeline valves and ASME B16.34 pressure‑temperature rating, the 3‑piece (3PC) butt‑weld trunnion‑mounted ball valve has become a preferred solution for buried high‑pressure oil/gas transmission pipelines and compressor station piping.
I. Core Challenges for High‑Pressure Oil & Gas Pipeline Valve Selection
Whether for above‑ground process piping or buried trunk lines, valve selection for oil‑gas projects needs to resolve four key engineering pain‑points:
1. Risk of external leakage: Flanged connections rely on gaskets. Ground settlement, pipeline vibration and thermal cycling accelerate gasket aging and cause dangerous hydrocarbon leakage.
2. Sealing performance under high differential pressure: Floating ball valves may suffer ball offset driven by high medium pressure, leading to sealing degradation.
3. High maintenance downtime: Removing large‑size high‑pressure valves from piping for overhaul brings expensive production loss.
4. Pipeline pigging compatibility: Full‑bore flow path is required to permit pipeline pig inspection and cleaning without obstruction.
Conventional flanged floating ball valves cannot satisfy all requirements simultaneously. The 3PC butt‑weld trunnion ball valve is purpose‑optimized for harsh oil‑gas operating conditions.
II. What Is A 3PC Butt‑Weld Trunnion‑Mounted Ball Valve?
3PC refers to three‑piece split valve‑body construction, consisting of left, central and right body segments. The trunnion‑mounted ball is restrained by upper and lower trunnion shafts so process pressure cannot displace the ball. Butt‑weld (BW) ends are designed for direct fusion welding with pipeline instead of bolted flanges. Manufactured and tested per API 6D, it adopts forged/cast material grades including A105, WCB, LF2, supporting large bore and high‑pressure classes for crude oil, natural gas and sour‑gas projects.
Insert your factory photograph here
Image ALT: Large bore 3PC butt‑weld trunnion ball valve, API 6D pipeline ball valve for high pressure oil & gas service, 3‑piece body butt weld ends, factory real shot
III. Key Advantages of 3PC Butt‑Weld Trunnion Ball Valve for Oil‑Gas Service
3.1 Butt‑weld ends eliminate gasket leakage paths for buried pipelines
Butt‑weld joints remove flanged gaskets — one major leakage source. For buried piping and heavy‑vibration compressor station lines, welded construction resists ground movement and thermal stress, delivering robust long‑term maintenance‑free integrity.
3.2 Trunnion ball design delivers reliable bi‑directional sealing at high pressure
Unlike floating ball design, trunnion shafts absorb fluid thrust instead of transferring full pressure onto seats. Double‑piston‑effect seats provide bi‑directional bubble‑tight shut‑off per API 6D requirements. Under high differential pressure, operating torque remains low and actuator sizing cost can be reduced.
3.3 3‑piece split body enables in‑line maintenance & minimizes downtime
With three‑piece body structure, technicians can access seats and seals by disassembling central body section, without cutting and removing the whole valve from pipeline. For oil‑gas assets, this feature greatly cuts overhaul duration and avoids heavy economic loss caused by pipeline shutdown, bringing obvious advantage compared with monolithic fully‑welded ball valves.
3.4 Full‑bore flow path supports pipeline pigging operation
Full‑bore inner profile matches pipeline inner diameter, lowers flow resistance and allows smooth passage of cleaning pigs and inspection gauges for routine pipeline maintenance work.
3.5 Compliant safety features for oil‑gas industry standards
Optional fire‑safe & anti‑static construction, body cavity over‑pressure relief, anti‑blow‑out stem are available to meet API 607 fire‑test specification. Material can be customized to NACE MR0175 for sour‑gas containing H₂S, covering wide temperature ranges.
IV. Recommended Application Scenarios
✅ Buried high‑pressure natural gas trunk pipelines, compressor stations & metering stations
✅ Crude oil & refined‑product transmission pipelines
✅ Off‑shore platform & oil‑gas gathering lines with heavy vibration
✅ Projects requiring long service life, in‑situ repair and pig‑gable full bore
❌ Not ideal for locations where frequent valve removal is needed and on‑site welding capability is unavailable.
V. Critical Selection Tips To Avoid Project Risks
Standard compliance: Specify API 6D, ASME B16.34 and match pressure class with pipeline system.
Material compatibility: Metallurgy matching between valve and piping; apply NACE MR0175 for sour service.
Weld preparation: Butt‑weld end bevel shall follow ASME B16.25 for site welding quality control.
Confirm optional functions: cavity relief, fire‑safe design, full‑bore / reduced‑bore requirement.
VI. Conclusion
For high‑pressure oil‑gas pipeline projects, 3PC butt‑weld trunnion ball valve integrates four major strengths: leak‑free welded connection, high‑pressure trunnion sealing, in‑line maintainability and pig‑capable full bore. Built against authoritative international pipeline standards, it solves real‑world pain‑points including external leakage, high‑pressure sealing failure and costly shutdown repair. When flanged valves and monolithic fully‑welded ball valves show respective limitations, 3PC butt‑weld trunnion ball valve provides a cost‑effective well‑balanced option for high‑pressure oil‑gas pipeline systems.
Get Your Solution
Looking for qualified API‑6D certified 3PC butt‑weld trunnion ball valves for your oil‑gas project? Send us your technical parameters: size, pressure class, process medium and operating temperature, we will deliver customized proposal and quotation.