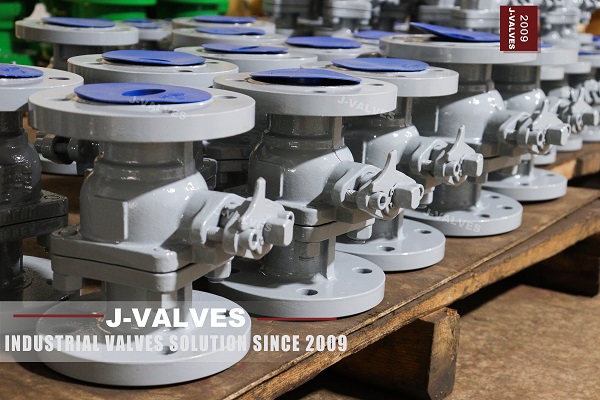
With the national integrated natural gas pipeline network expansion, long-distance high-pressure pipeline projects with DN1000+ oversized bore sizes grow year by year. As core isolation equipment for main transmission lines, DN1200 PN100 fully welded forged steel ball valves face strict standards on cryogenic material performance, integral welding strength and long-term underground anti-corrosion durability. Leveraging self-forged LF2M cryogenic steel and mature integral full-welding technology, J-VALVES won a bulk order of oversized bore valves for a northwest cross-provincial natural gas trunk line. Combined with our factory DN1200 finished valve photos, this article fully records the project requirements, customized solutions and full delivery process.
I. Core Working Condition Requirements
This 320km cross-provincial gas trunk line passes through frigid mountainous zones with minimum winter temperature of -38℃ and design transmission pressure of 10MPa (PN100). All valves adopt vault-free buried installation with three key requirements:
Cryogenic material resistance: LF2M forged steel body required, minimum temperature resistance -46℃ to prevent medium-induced brittle fracture in winter.
Long-term zero-leakage sealing: 30-year maintenance-free underground service, split flange structure forbidden to eliminate gasket leakage risks.
Stable pressure bearing for oversized bore: Integrally forged DN1200 body free of defects, no stress deformation post welding to sustain long-term 10MPa pressure.
Three valve manufacturers participated in the tender in the early stage. Competitors could not self-forge oversized DN1200 LF2M bodies and relied on outsourced forgings with less than 85% flaw detection pass rate. J-VALVES operates thousand-ton in-house forging lines with 100% forging inspection pass rate, winning the full isolation valve tender.
II. J-VALVES Custom Product Solution (Matching DN1200 Valve in Photos)
Body Raw Material: Integrally forged LF2M cryogenic carbon steel, piece-by-piece cryogenic impact test & UT ultrasonic flaw detection to eliminate internal microcracks. Standard BW butt-weld bevel ends seamlessly connect with trunk steel pipes and reduce gas transmission flow resistance.
Full Welding Process: Automatic submerged arc circumferential welding for two forged body halves, followed by integral stress relief heat treatment in large furnaces to remove residual welding stress and avoid body deformation under high pressure. External heavy-duty blue epoxy anti-corrosion coating resists soil acid-alkali and groundwater erosion.
Sealing System: Dual metal hard & flexible soft sealing, passed API 6D fire safety test to maintain zero leakage under unexpected pipeline high-temperature conditions.
Actuator Configuration: High-torque worm gear drive for manual operation at sites without power supply, upgradeable to electric smart actuators for remote pipeline monitoring later.
The factory photo shows bulk finished DN1200 PN100 LF2M fully welded ball valves after coating and assembly. Each unit weighs over 12 tons and passes 15MPa hydrostatic strength test + 10MPa pneumatic sealing test before warehousing.
III. Delivery & Field Operation Performance
Lead Time: Competitors take 90 days for DN1200 valves, while J-VALVES cuts the cycle to 65 days via fully self-owned production lines, guaranteeing on-schedule pipeline commissioning.
Construction Advantage: Integral flange-free welded body features compact outer diameter, reducing underground excavation volume and civil engineering costs by 28%.L
ong-term Operation Feedback: All line valves have run through 5 heating seasons without stuck operation, internal or external leakage under extreme winter cold. Annual third-party pipeline pressure retests show no degradation of valve pressure bearing performance compared to factory test data.
Follow-up Cooperation: Phase II distribution branch lines placed additional orders of DN800/DN1000 LF2M fully welded ball valves, with identical large bore LF2M valves exported to similar frigid gas trunk lines in Central Asia.
IV. Replicable Service Capacity for Similar Projects
Beyond this DN1200 PN100 gas trunk line case, J-VALVES holds mature experience of fully welded forged ball valves across multiple scenarios:
Bulk supply of DN300-DN700 medium bore buried welded valves for city gas gate stations
Custom LF2 cryogenic fully welded ball valves for LNG receiving terminals
Export PN63/PN100 LF2M valves to frigid regions of Central Asia & Russia
High-temperature resistant forged welded ball valves for coal chemical & high-pressure steam buried pipelines
For new or renovated domestic long-distance pipeline networks and overseas energy project tenders, J-VALVES provides full-process support including working condition calculation, material selection, drawing design, production witness inspection and after-sales warranty, with 5-year warranty & lifelong technical maintenance support.
Send your project parameters (medium, temperature, bore size, pressure) to receive free 3D drawings, inspection reports and reference cases of similar projects for DN600-DN1400 large bore PN63/PN100/PN160 cryogenic fully welded forged steel ball valve inquiries.