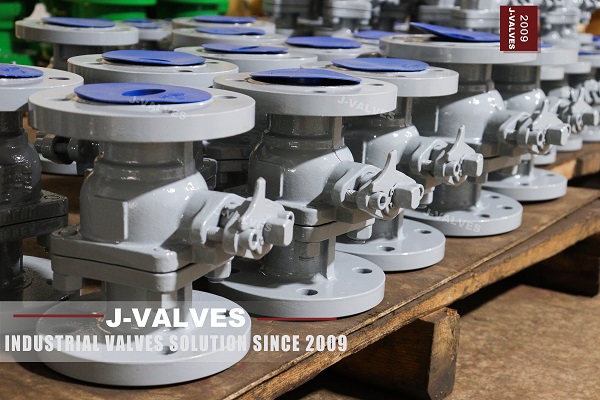
Major pain points for oil & gas and coal chemical large-scale valve procurement include delayed bulk delivery, inconsistent product quality, incomplete inspection documents for sour high-pressure valves and poor welding compatibility on site. Established in 2009, J-VALVES owns integrated forging, machining, assembly and testing workshops with 17 years industrial valve manufacturing experience. We realize full independent production of 3PC welded trunnion ball valves, as shown in mass finished valve photos in factory workshop, capable of undertaking bulk orders of thousands of high-pressure valves worldwide.
I. Full Self-Support Production Line for 3PC Welded Trunnion Ball Valve
Independent Forging Workshop for Valve Bodies
LF2, LF2M, A105, F304 and other forged blanks are produced in-house, avoiding counterfeit material from external suppliers. Spectroscopic test samples reserved for each batch to strictly follow NACE sour service standards.
CNC Precision Machining Production Line
Five-axis CNC machines process 3-piece body weld bevel, ball sealing surface and stem sealing area with tolerance ±0.02mm. Standardized extended butt weld ends eliminate on-site welding mismatch issues.
Separated Assembly Zones (Standard & H2S Sour Service)
Independent clean assembly workshop for sour resistant valves to prevent carbon steel impurity contamination on sealing surfaces. Special tooling for PN320 high-pressure models to ensure perfect ball alignment and zero leakage under high pressure.
Full-Scale High Pressure Test Laboratory
Equipped with PN420 ultra-high pressure hydro tester, low-temperature impact tester and H2S corrosion simulation bench. Every single 3PC trunnion ball valve receives 100% pressure test with complete API 6D & NACE inspection documents.
II. Three Key Delivery Advantages Over Competitors
Advantage 1: Large Mass Production & Short Lead Time
As shown in neat rows of finished 3PC welded trunnion ball valves in workshop, monthly output reaches 2000 sets of 3-piece fixed ball valves. European & American brands take 90~150 days for bulk orders, while J-VALVES finishes standard bulk orders within 60 days, rush orders down to 30 days to meet tight schedules of overseas energy projects.
Advantage 2: Custom Extended Butt Weld Ends for Buried Pipelines
Most suppliers supply short weld ends with limited underground welding space. All J-VALVES 3PC trunnion ball valves adopt standard extended weld tubes with anti-rust pre-treatment on bevels, less weld stress and long-term zero leakage, becoming preferred model for buried natural gas pipelines in Middle East & Central Asia.
Advantage 3: Split 3-Piece Design Cuts Aftermarket Maintenance Cost
One-piece ball valves require pipeline cutting for replacement when broken. J-VALVES bolted split 3-piece design allows technicians to replace seats & ball by removing center body only, no hot cutting needed, greatly lowering labor cost for remote overseas oilfields.
III. Overseas Bulk Delivery Success Case: Middle East Oilfield High Pressure Gathering Project
In 2025, a major Middle East oil group built 10 new sour high-pressure gas gathering stations, purchasing 1600 sets DN80~DN250 PN160/PN320 LF2M 3PC welded trunnion ball valves. Tender core requirements: full delivery within 65 days, complete NACE sour certificates, maintenance without pipeline cutting.
J-VALVES Project Achievements:
Finished mass production, pressure test, epoxy coating and wooden case packing of 1600 valves in two batches within 58 days;Supplied bilingual material reports, API inspection certificates and NACE heat treatment documents, passed client third-party audit at one time;
Field maintenance time per valve reduced by 75% thanks to split 3-piece structure, overall project maintenance budget cut by 58%;
Signed annual framework procurement contract after project completion, stable annual order of 800~1200 high-pressure sour resistant ball valves.
IV. Customization Scope
Pressure Class: PN16 / PN40 / PN100 / PN160 / PN250 / PN320
Material: LF2M, LF2, WCB, CF8M, F51 Duplex Steel
Actuator: Manual, Pneumatic, Electric, Hydraulic
Applicable Medium: H2S sour oil & gas, hydrogen, LNG, coal chemical syngas