


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q41F
-
J-VALVES
Overview of the J-VALVES 3 inch PN20 CF3M two piece floating ball valve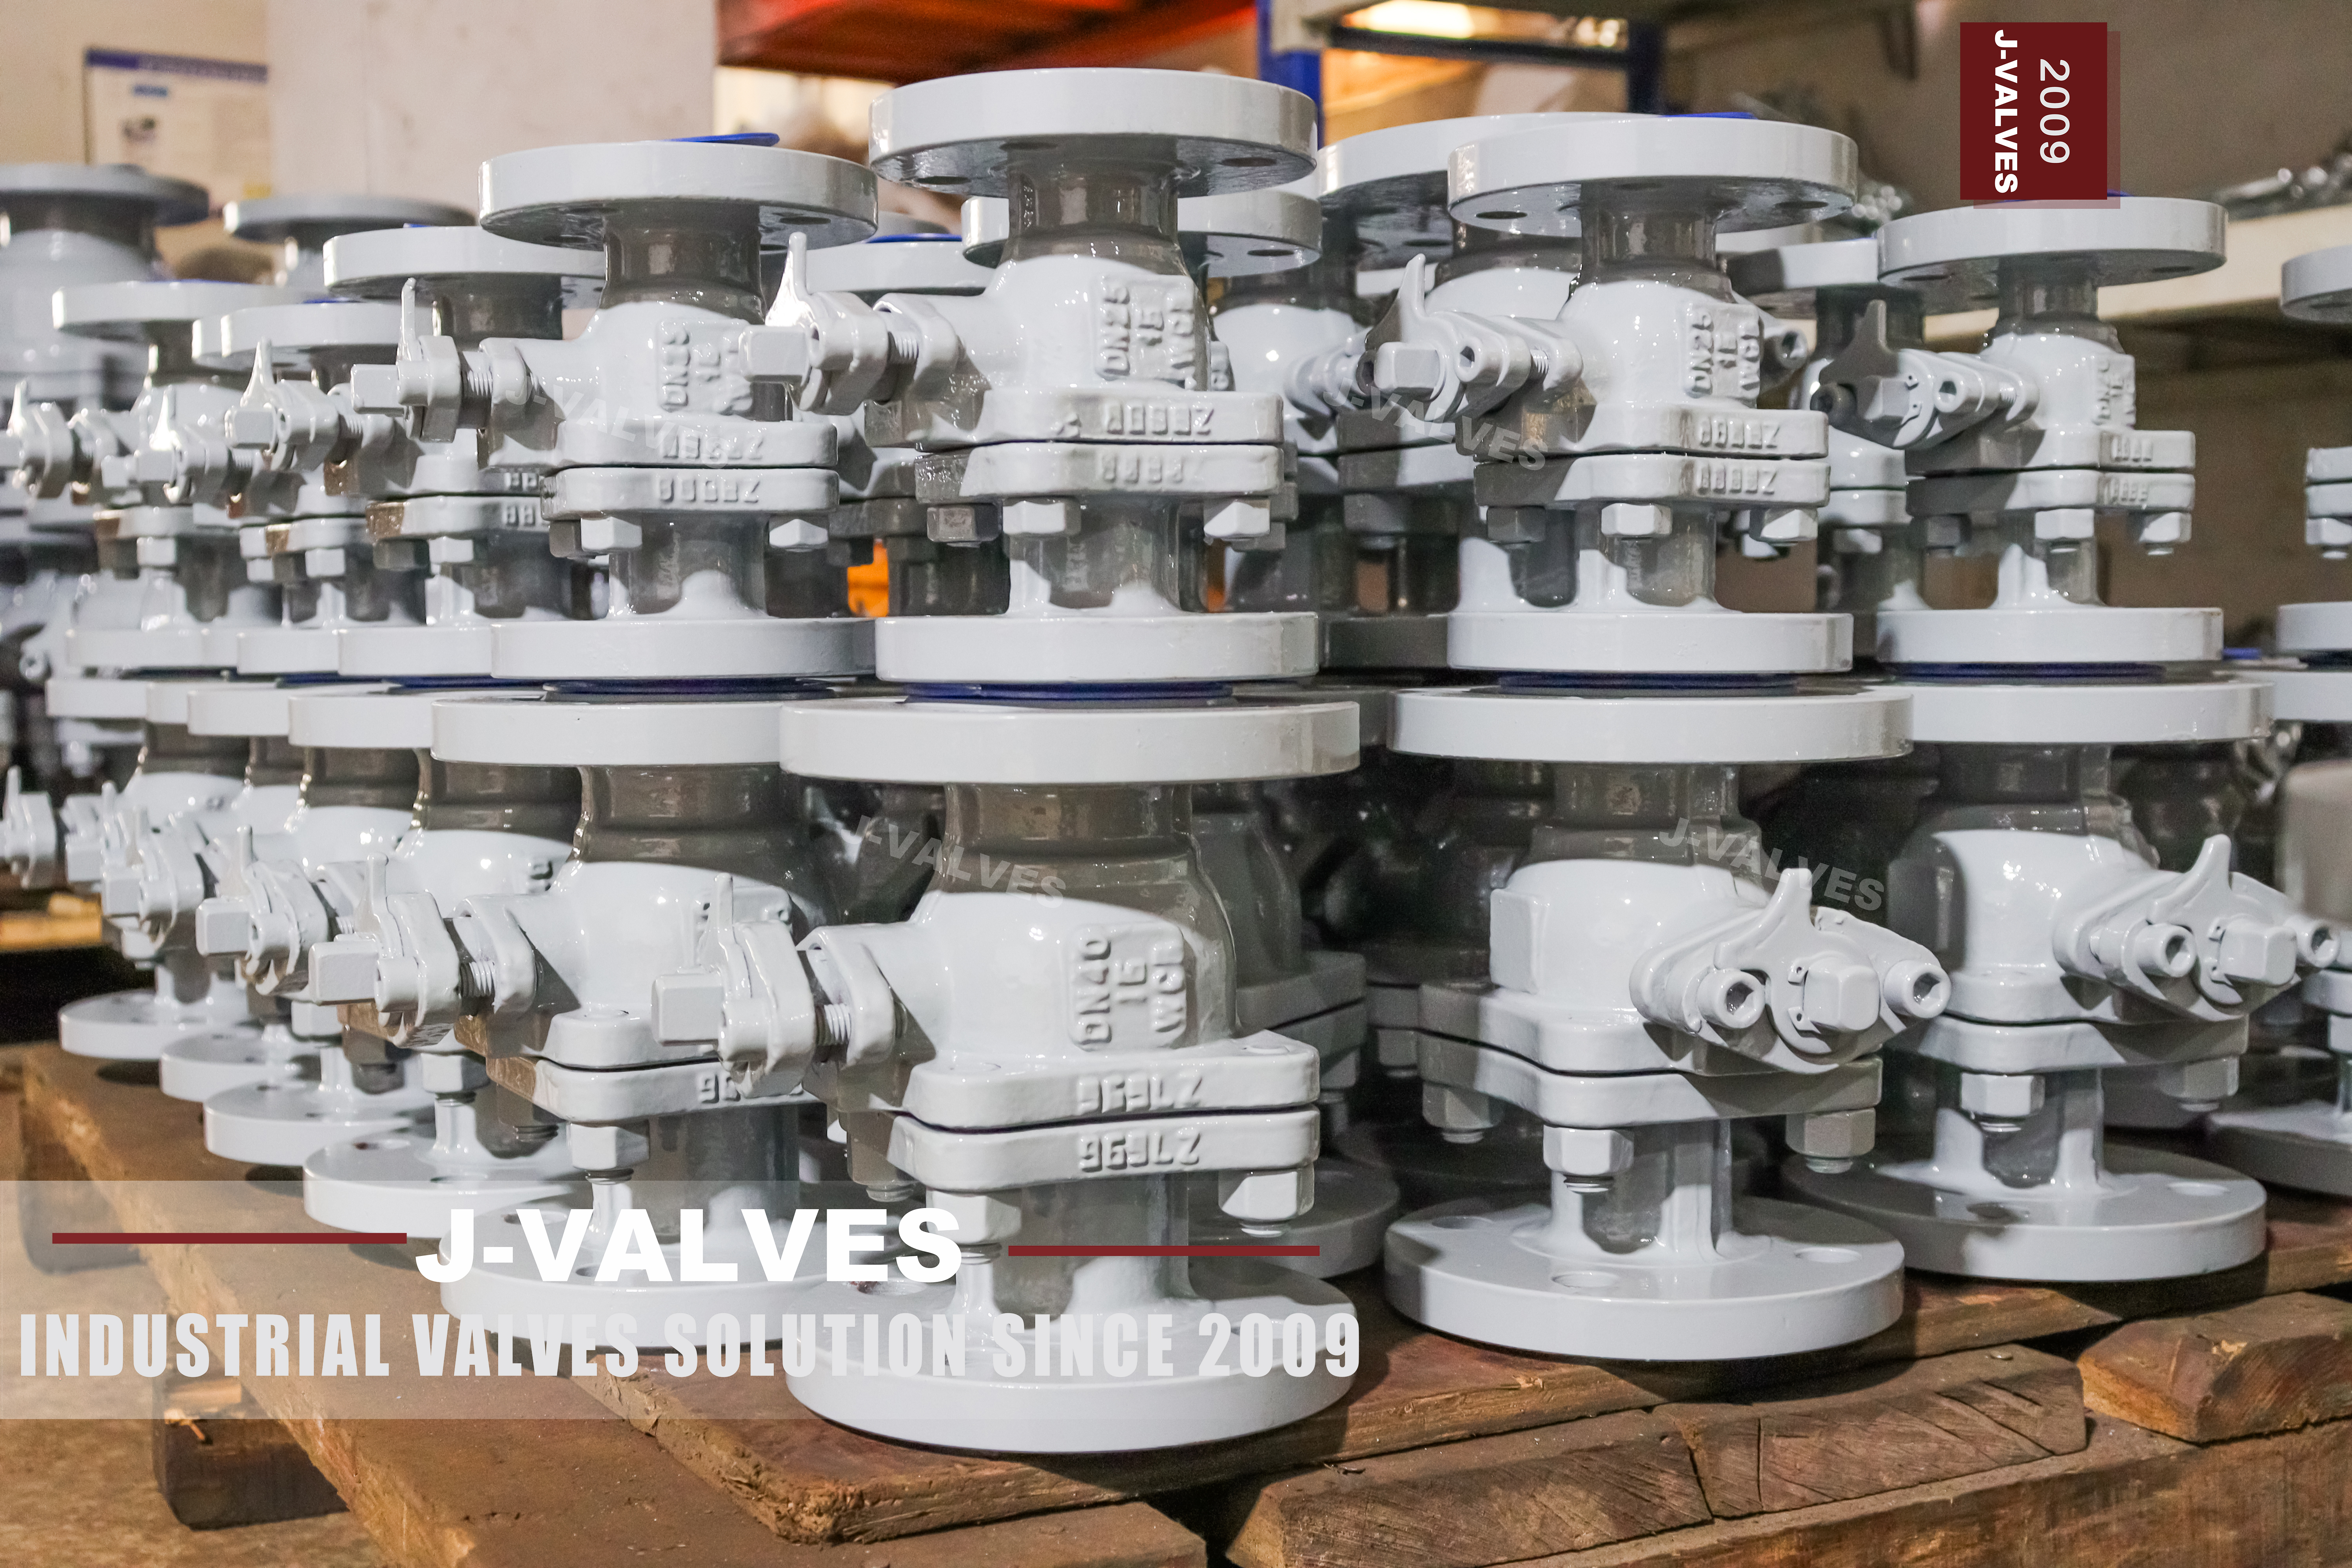
This page sells one valve and prints the specification of another. The top half is a three inch, Class 150, two piece floating ball valve in cast CF3M with raised face flanges and a lever. The bottom half carries a seat table headed single piston effect, double piston effect DIB 1 and combined DIB 2, with rows for cavity self relieving and double barrier, and a feature list that begins with a trunnion mounted ball.
A floating ball valve has no trunnion, no piston seat, no independent second barrier and no sealant injection port. Those parts belong to the trunnion family, and the table they appear in is a template that was left attached to the page rather than a description of the valve in the photographs.
That matters because the table is the part a buyer reads last and remembers. It promises a double block and bleed function that a single ball between two simple seats cannot deliver, and it promises piston effect seats on a design whose seats are rings held by preload. The valve is a good one at what it does. The footer sells a different one.
Design and Construction
The body is two pieces: a main body and an end piece, closed on one gasketed face by a ring of studs. The joint exists because the ball has to enter the body, and the opening that passes the ball also carries one seat pocket. The end piece carries the other seat pocket and one of the two flanges, so the joint is a pressure boundary and a machining reference at the same time.
The ball rests between the two seats and is not carried on bearings. Line pressure on the upstream side pushes the whole ball downstream, so the downstream seat is loaded by the medium while the upstream seat is held against the ball by its own preload alone. The force available to seal grows with the area of the bore, and the parts that have to resist it grow only with the diameter, which is the reason this pattern has a size ceiling.
What the footer lists and this valve does not have is worth naming one by one. A trunnion is a pair of shafts that carry the ball and take the thrust, and there is no such shaft here. A piston seat is a seat ring that sees pressure on both faces so that cavity pressure pushes it onto the ball, and these seats are rings with one sealing face. Double block and bleed needs two independent barriers with a vented space between them, and one ball with two seats gives one barrier.
The stem turns the ball and carries no radial load beyond seat friction. It has a shoulder below the packing that is wider than the hole it passes through, so pressure cannot eject it if the gland is dismantled with the line live. Packing is reachable from the top without opening the body, which is the one maintenance advantage this pattern really has over a welded design.

Material Options
CF3M is a cast austenitic stainless steel to ASTM A351 with the composition of 316L: chromium, nickel and molybdenum, with carbon held to 0.03 percent or less. CF8M is the same alloy with carbon allowed up to 0.08 percent. The two are not interchangeable on a certificate, they are interchangeable in a drawing, and the difference shows up in one place only, which is what happens to the metal beside a weld.
Carbon is what combines with chromium at welding temperature to form chromium carbides at the grain boundaries. Those boundaries then lose the chromium that was protecting them, and the loss is intergranular corrosion. A low carbon grade leaves too little carbon for that reaction to matter, so a CF3M body can be welded and put into service without a solution anneal. A CF8M body either gets the anneal or accepts a thinner skin of resistance beside every weld.
| Part | Material on This Build | What It Decides |
|---|---|---|
| Body and end piece | ASTM A351 CF3M cast stainless | Corrosion resistance of the shell, and weldability on site |
| Body options | CF8M or CF8 on request | Carbon level in the casting, and the certificate line |
| Ball | CF3M or CF8M bar, or ENP and hard chrome plated | The sealing band and the bore finish |
| Stem | CF3M or CF8M bar, or 17-4PH | Torque, packing wear, and stem strength |
| Seats | PTFE, reinforced PTFE, or PPL | The temperature and pressure ceiling of the valve |
| Packing | PTFE V-rings or flexible graphite | The stem seal and its temperature limit |
| Body gasket | Spiral wound with graphite, or PTFE envelope | The single joint |
| Studs and nuts | 316L, or A193 B8M with A194 8M | Joint preload and corrosion at the joint |
| Ends | Raised face flange to ASME B16.5 | The drilling that has to match the pipe |
The ball and stem rows need a note, because the page describes the ball as integral CF3M or CF8M. Those are casting designations, and a ball is not cast: it is turned from bar or from a forging, ground and lapped, because a sealing band cannot contain casting porosity. The correct name for the ball is 316L or F316L, and a casting grade in that row usually means the row was copied from the body row and left alone.
The seat row is where the service is decided. PTFE is the standard, reinforced PTFE carries a filler against creep, and PPL is the highest of the three at roughly 280 Celsius. All three are polymers, and all three fail the same way: at temperature the seat stops recovering, and a seat that does not spring back does not follow the ball. The 425 Celsius line at the top of the page is a body figure, and it is above every seat on the list.
Technical Specifications
The build on this page is one combination of size, class, grade and seat. The class is a rating, not a family: 150 and 2500 in the same column would be different castings with different walls, different stems and different bolting, and the table below only claims the first.
| Item | Value |
|---|---|
| Size | Three inch, DN 80 |
| Class | Class 150, PN 20 |
| Body | ASTM A351 CF3M, two pieces |
| Ball | 316L bar, floating, not trunnion supported |
| Seats | PTFE, reinforced PTFE or PPL |
| Temperature, seat limited | Minus 29 to plus 150 for PTFE, 180 for reinforced PTFE, 280 for PPL |
| Temperature on the page | Minus 29 to plus 425, which is a body figure |
| Ends | Raised face flange, ASME B16.5 Class 150 |
| Face to face | ASME B16.10 |
| Design | ASME B16.34 and API 608 |
| Test | API 598 |
| Fire | API 607 |
The minus 196 figure in the seat row needs separating from this build. A cryogenic valve is not a standard valve with a cold seat dropped into it: it needs an extended bonnet so that the packing sits far enough from the cold end to stay above the frost line, and a stem long enough that heat does not run down it into the seat. The photographs show a short bonnet with a lever on top, which is the ambient build. A seat material alone does not make a cryogenic valve.
Standards and Compliance
Three documents are named on the page and they do different work. ASME B16.34 gives the wall thickness and the pressure temperature ratings for the material group, and for a Class 150 stainless body it is generous. API 608 covers steel ball valves from DN 15 to DN 600 and Class 150 to Class 600, and a three inch Class 150 valve sits comfortably inside that window.
| Document | What it fixes | What it does not fix |
|---|---|---|
| ASME B16.34 | Wall, material groups, class ratings | Seat material, leakage, or the body joint |
| API 608 | Steel ball valves, DN 15 to DN 600, Class 150 to Class 600 | Anything above Class 600 |
| ASME B16.5 | Flange dimensions and drilling | The internals, the seats, the torque |
| ASME B16.10 | Face to face for flanged valves | Weld end or threaded lengths |
| API 598 | Shell and seat test procedure and acceptance | Which seat the valve should have |
| API 607 | Fire test for quarter turn valves | A leakage rate in normal service |
The fire certificate is a type test on a design and a size. It says that a valve of this construction, with these seats, passed a defined test after the soft parts were destroyed, and that the metal parts still restricted flow to the permitted rate. It is a statement about a design, not a statement that the unit in the crate went through the test, and it does not make the valve fire proof. What survives a fire is the metal contact between ball and seat once the polymer is gone.
The anti-static spring is a small part with a real job. A ball turning in polymer seats can hold a charge, and a spring bearing between the stem and the body gives that charge a path to earth. On a valve in a flammable service the spring is a safety device, and its absence is the kind of thing that only shows up in an incident report.
The licence list in the footer needs reading for what it is. API 6D, 6DSS and 6A PSL4 describe what the works is qualified to build, not what this valve is. A Class 150 two piece floating valve is not an API 6D valve and is not tested to 6D, and quoting that list beside a DN 80 floating body invites a specification that the valve cannot meet.
Manufacturing Process
The body starts as a casting. After fettling, the first setting establishes the bore axis and one flange face, and every other feature is cut from that reference: the opposite flange face, the seat pocket, the stem bore and the joint face. A casting set up on a rough surface produces a valve whose seat is not square to its flanges, and that error shows up later as a seat that leaks from one side only.
The seat pocket is bored from the joint face, in the same setting as the joint face where the machine allows, because pocket depth, squareness and finish all decide how the seat sits. Finish matters more with a polymer seat than with a metal one: the polymer conforms to a rough surface but cannot correct a pocket that is out of square. Assembly then fits the seats and the ball through the joint and closes the end piece on its gasket.
The studs are torqued in a crossing sequence rather than around the circle, so the gasket is compressed evenly and the end piece does not cock. The stem and packing go in from the top afterwards, and the lever is fitted on a square that is cut after the gland face is machined, so the handle sits square to the gland rather than to the raw casting. A lever that is out of square looks like a cosmetic defect and feels like a bent stem.

Quality Control and Testing
The shell test is applied with the ball open, at the multiple of the class that the test standard names, and the body joint is watched throughout because it is the boundary a one piece body does not have. A joint that weeps under the shell test is a gasket, a face or a torque sequence problem, and all three are cheaper to find at the works than on a line that is already full.
The seat test is run twice, once from each side. With pressure on one side, only the downstream seat is loaded by the medium and the upstream seat is held by preload, so a single sided test describes one seat and says nothing about the other. The procedure exists in that form because the mechanism requires it, not because the standard is being cautious.
The plate is struck after the tests and carries the size, the class, the grade and the heat number. On this page the grade line is the one that settles the argument between CF3M in the heading and CF8M in the photographs, because the plate and the 3.1 certificate follow the heat that was poured, and neither follows the page. A buyer who needs CF3M should ask for the certificate before the crate is opened.

Applications and Industry Service
Chemical and petrochemical transfer is the largest use, and it is the reason a low carbon grade appears on a three inch valve at all. The molybdenum in the alloy resists chlorides that a 304 grade does not, and much of the damage a stainless ball valve takes in a chemical plant involves chlorides at some concentration. Where the line will be welded on site and cannot be annealed afterwards, CF3M is the grade that survives the weld.
Water and utility headers are the second family. There the stainless body is often chosen for the wetted path rather than for the pressure, because a stainless line with a carbon steel valve in it makes a corrosion cell at every flange. Food, beverage and pharmaceutical service uses the same pattern with a smoother bore and a seat chosen for the cleaning regime rather than for the pressure.
Where the valve should not be used is a short list. Not on a line that needs throttling, because a part open ball puts the flow across the seat edge and erodes the polymer. Not above the seat temperature, whatever the body can take. Not on a line that genuinely needs double block and bleed, because that requirement describes a different valve with two barriers.

Installation, Operation and Maintenance
Installation is a flange joint at each end, with the valve supported so the pipe does not hang from the body, and with the faces parallel before the bolts are tightened. A valve pulled into line by its bolts puts a bending load through the body joint, and the joint is the part that will weep first. Gaskets are chosen for the flange facing, and the studs are tightened in a crossing pattern to the torque the joint design names.
Servicing this pattern means going in from two places: the gland at the top for the stem seal, and the joint at the side for the seats. The joint gasket is renewed whenever the body is opened, and the seats are replaced as a pair rather than one at a time, because a new seat against a worn one loads unevenly and the new one takes the wear. The ball is inspected at the same time, since a scratched band will destroy a new seat within a few cycles.
Storage matters more than it looks. A valve left closed with the ball pressed into one seat for months can take a set in the polymer, and the first movement after installation then leaks until the seat warms and recovers. Storing with the ball open, in a dry place with the flange faces protected, avoids the set and keeps the bore from rusting in a carbon steel neighbour.
How to Specify and Order
The lines below are the ones the page does not settle, and the first is the one that decides what actually ships.
| Line on the order | What to write | Why it matters |
|---|---|---|
| Grade and certificate | CF3M, with a 3.1 certificate naming the heat | The heading and the photographs disagree, and only the certificate decides |
| Seat material | PTFE, reinforced PTFE or PPL | It sets the temperature ceiling, not the body |
| Temperature | Minimum and maximum in service | A seat limit is not a body limit |
| Size and class | Three inch, Class 150 | The pattern has a size ceiling that the footer ignores |
| End standard | ASME B16.5, with the facing | The drilling has to match the pipe |
| Function | Blocking only, or double block and bleed | If bleed is required, this is the wrong valve |
The single most useful thing a buyer can take from this page is that the valve and the seat table at the bottom are not the same product. Order the top half, with the grade written on the certificate and the seat written on the order, and ignore the footer. If the footer is what the process actually needs, the requirement is a trunnion valve with two barriers, and it should be quoted as one.
FAQ
Q: Does this valve have double block and bleed?
A: No. Double block and bleed needs two independent barriers with a vented space between them, and one ball between two seats is one barrier. The feature list at the bottom of the page describes a trunnion valve, where each seat can hold on its own and the cavity between them can be drained and checked.
Q: What is a piston seat and why is it not on this valve?
A: A piston seat is a ring that sees pressure on both faces, so cavity pressure pushes it onto the ball. On a floating valve the seats are simple rings with one sealing face, and the ball is pushed into the downstream one by the medium. There is no piston area to act on.
Q: Is the body CF3M or CF8M?
A: The heading says CF3M and the body row offers CF8M and CF8 as options. Both are A351 austenitic castings of the 316 family, and they differ in carbon: 0.03 percent maximum for CF3M and 0.08 for CF8M. The plate and the 3.1 certificate follow the heat that was poured, so the certificate decides, not the page.
Q: Can this valve run at minus 196 Celsius, as the seat row suggests?
A: Not in this build. A cryogenic valve needs an extended bonnet so the packing stays above the frost line and a stem long enough that heat does not run down into the seat. The photographs show a short bonnet with a lever, which is the ambient build, and a seat material on its own does not change that.
Q: Which temperature do I quote, 425 or 280?
A: The seat. 425 Celsius is a figure the CF3M body can take, but the seats on this page stop at 150 for PTFE, 180 for reinforced PTFE and about 280 for PPL. A valve is limited by the part that touches the ball, so the seat figure is the one that belongs on the order.


Hot Products


News
Direct Air Capture Ball Valves The Vacuum Side Runs The Seal Backwards, And Three Hundred Thousand Strokes Decide The Design
A solid sorbent DAC plant moves 1.3 million cubic metres of air per tonne of CO2, then asks a DN50 ball valve to hold 0.9 bar from the wrong side.
Read More
Your Ball Valve Is Not A Test Blind: What A Hydrotest Does To The Seats
A line test puts pressure on the wrong side of the seat logic, above the valve's own seat test, with water that stays in the pocket. What to arrange instead.
Read More
Remanufactured Ball Valves: Five Checks That Decide Whether A Rebuild Deserves A Certificate
A rebuild at 45 percent of price with half the life is no saving. Five checks that separate a real remanufacture from a repaint with a certificate.
Read More
The Squeeze Is A Residual: How Tolerance Stack-Up Decides Whether A Ball Valve Seals
No dimension sets the seat squeeze. Five tolerances do, in series. Why identical valves feel different, and why a new ball changes the arithmetic.
Read More