


A slug is mass, not a spike
Two different events get called the same thing in an operating report, and separating them is the first step in deciding whether the valve has a problem. A surge, or water hammer, is a pressure transient: a moving column of liquid is stopped or accelerated, the energy has nowhere to go, and for a fraction of a second the pressure at the valve is far above anything on the datasheet. A slug is not that. A slug is a volume of liquid travelling along a line that is mostly gas, arriving at the valve as a body with a front, a length and a mass. The pressure gauge often barely moves. What changes is what is inside the bore.
That distinction matters because the remedies are different and the damage is different. A surge problem is solved by slowing a closure or by removing an accumulation of liquid before it moves. A slug is solved upstream, by not letting the liquid accumulate in the first place, or by giving it somewhere to go before it reaches a valve that was bought to be either open or closed. A ball valve in a slugging line is usually not the cause of anything. It is the place where the consequences become visible, because it is the one component in the line with a soft seat, a moving part and a sealing surface that has to be flat.
Where slugs come from, and why the valve gets the blame
In a two phase line, liquid collects wherever the gas cannot carry it. Low points, the bottom of a riser, a section where the line dips under a road, the upstream side of a control valve that has been throttling. Once enough has collected, the gas flow pushes it out as a body rather than as a mist, and that body travels at a speed closer to the gas than to a liquid film. Nothing in that description involves a ball valve, and yet the ball valve is where the complaint lands, because it is the component that is expected to hold.
Four sources account for most of it. A shutdown is the first: liquid drains to the low point while the line is static, and the first hours of restart push the whole accumulation through as a bank. A pig run is the second: the pig sweeps the line clean and delivers everything ahead of it in one arrival, which is why a valve downstream of a pig trap sees the worst of the line's liquid in a single pass. Upstream level control is the third: a separator or a knock-out drum that dumps liquid into a gas outlet does it in batches, and each batch is a slug. The fourth is the line itself, where a change in elevation or a change in gas rate moves the flow from a regime where liquid travels as a film to one where it travels as plugs.
In all four cases the valve is asked to do something it was not specified for. A block valve is bought to isolate a section, not to condition a flow. It will still be the part that fails, and it will still be the part blamed.
What changes at the seat when liquid arrives
A soft seated ball valve sealing against dry gas is doing one of the easier jobs in valve engineering: the seat conforms to the ball, the contact band is narrow, and there is nothing in the fluid to interfere with it. When the fluid at the seat becomes liquid, four things change at once.
The first is the film. Liquid wets the ball and the seat, and a film of liquid between two surfaces that were designed to touch metal to polymer is a change in the sealing mechanism, not a change in degree. A valve can seal better when wet, because the liquid fills the microscopic leak path that gas was finding, and it can seal worse, because the same film now carries whatever is suspended in it into the contact band. Both outcomes are observed, which is why a leak that appears and disappears with the flow regime is so often misdiagnosed as a seat that is "on its way out".
The second is the direction of the assist. A seat is pressure energised, and it is energised in the direction the differential pushes it. A slug arriving from downstream, which happens on a line with a downstream liquid leg, a backflow event or a closed section that is being equalised, puts the assist on the other side of the same seat, and a seat that was tight in the design direction is now being lifted rather than pressed. This is not a defect and it is not a spring problem; it is a valve being used outside the direction it was bought for, and the only fix is a seat arrangement that seals both ways.
The third is what the liquid can carry. Gas at line velocity will not move sand, scale or corrosion product any meaningful distance. Liquid will. Every slug is therefore a delivery mechanism for the particles that damage seats, and it delivers them to the one place in the valve where two surfaces are in sliding contact: the seat band. The wear mechanism itself is the same one described for slurry and erosive service, but the delivery is different, and it arrives in batches that a dry gas line would never produce.
The fourth is the noise, and it is the only one the operator gets for free. A slug passing a partly open valve makes a sound that gas does not, and a change in that sound over months is a better early warning than any trend on a pressure gauge.
The valve can create the surge it is blamed for
Here is the part of the subject that is genuinely counter-intuitive. A slug does not arrive at the valve as a pressure event, but the valve's own closure can convert it into one. When a valve closes on a line that is carrying a body of liquid, the liquid column behind the closure has to stop, and the energy of that stop is a pressure wave that travels back up the line. The faster the closure, the higher the wave. The valve did not receive a surge; it made one.
That is why the closing time of an actuated ball valve on a two phase line is a process decision rather than a mechanical one, and why it belongs with the surge study rather than with the actuator supplier's catalogue. It is also why a valve that has been converted from manual to actuated is a different valve from a hydraulic point of view, even though nothing in the pressure boundary changed. The torque calculation that sizes the actuator is a separate exercise and is covered in the torque chain from stem to actuator; the closing time is the part that the torque calculation does not answer.
For a spring return actuator the two are linked, because the spring that closes the valve is also the spring that sets how fast it closes. A spring chosen to guarantee closure against a fouled stem will close quickly, and on a line that slugs that speed has a cost. The honest resolution is to state the required closing time to the actuator supplier as a process requirement, and to accept that a failsafe closure and a gentle closure may need different hardware rather than one compromise.
The part-open trap
A ball valve is a block valve. Its seat is designed to hold with the ball against it and its bore is a straight passage; nothing in its geometry is intended to be a control element. At part open the flow is squeezed between the edge of the ball port and the lip of the seat, and the highest velocity anywhere in the line is created at the one place where the material is softest and the clearance is smallest. That is true in clean gas. In a slug it is true with liquid carrying solids.
The instinct when a slug starts arriving is to throttle back and smooth it out. It is the wrong instinct for this valve, and it converts a transport problem into a wear problem in a way that is invisible until the seat is inspected. If throttling is genuinely required, the answer is a trim designed for it, such as a V-port or segmented ball valve, where the control edge is a shaped feature and the seat is protected from the jet. A standard ball valve held at part open in a slugging line is a valve being consumed.
The other side of the same argument is the reason full port matters here. A reduced port valve presents a step in the bore, and a step is where a slug's liquid front changes velocity and where solids settle. On a line that slugs, the bore through the valve should match the line and the valve should be either fully open or fully closed, with the throttling done somewhere built for it.
The cavity fills, and stays full
On a trunnion valve there is a volume between the two seats and around the ball, and in normal gas service it is a gas volume that follows the line. When a slug passes, that volume fills with liquid. When the gas comes back, the liquid does not leave. It sits in the least scoured part of the valve, against the seat carriers, the springs and the body wall, and it stays there for as long as the valve is closed.
Two consequences follow, and both are slow. The first is corrosion in a place that nobody inspects, because the cavity is only opened during a strip-down and the liquid is only visible then. The second is that the cavity stops being a reliable indicator: on a valve with bleed connections, a cavity full of liquid tells you what the liquid is but not whether the seats are holding, because the pressure that arrives at the bleed point came through the seats or was already there. Bleeding a liquid filled cavity and finding liquid proves nothing about isolation, and the mistake is common enough to be worth stating plainly.
The practical answer is geometry and procedure rather than a different valve. A drain at the low point of the installed orientation, a bleed that is used with the valve in the position it actually sits in, and a routine of draining after a slug event. A valve installed with its drain on the high side has a drain that will never remove the liquid it was fitted for.
Damage that accumulates by the season
The individual slug does almost nothing. What accumulates is the repetition. Each passage loads the seat band, wipes it with whatever the liquid carried, and unloads it again, and the result after a few seasons is a contact band that is polished, slightly widened and lightly scored rather than gouged. A gouge is a single event, usually a hard particle trapped at closure, and it announces itself. The polished, widened band is the signature of many small events, and it produces a leak that starts as a weep and grows with each season.
This is also why a valve that is tested once a year on a clean test bench keeps passing. A seat leak test with clean water at rated pressure is not a severe test for a seat that has been polished by a slurry of line solids. The damage is in the surface, and a test that measures leakage through a closed seat at pressure is not sensitive to a surface that still conforms well enough to hold water. The evidence is in the contact band, and the contact band is only visible when the valve is open.
What arrives, what it touches, what is found later
The table maps the event to the part. Read it from the left when a line is being designed, and from the right when a valve is being inspected.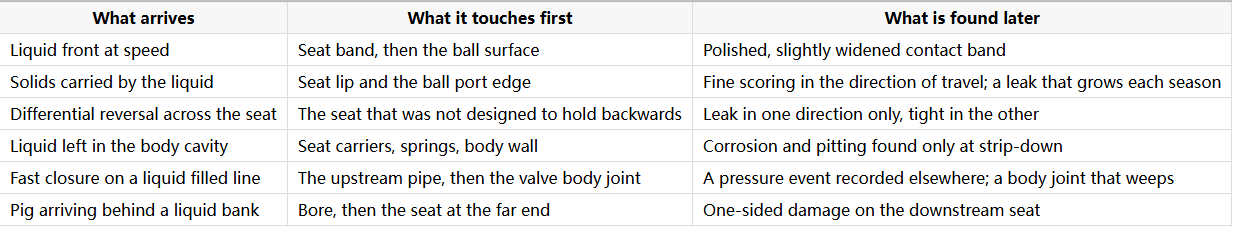
Specifying a valve for a line that slugs
Most of the protection is bought at the enquiry stage, and it costs nothing but a sentence. State that the line slugs. A valve supplier who is told that will ask about the flow regime, the solids and the orientation; one who is not told will supply a valve that is correct on paper and wrong in the line. State the duty: block, fully open or fully closed, no throttling. A valve ordered as a block valve and used as a control valve is a warranty argument waiting to happen, and the argument will be about the seat.
State the seat arrangement for the direction the differential actually takes, and if the line can reverse, say so, because a single direction seat is a legitimate design choice that becomes a defect the first time the flow turns around. Name the seat material for the solids the liquid can carry rather than for the gas, since the gas is not what reaches the seat. Agree the closing time with whoever owns the surge study, and pass it to the actuator supplier as a requirement rather than accepting whatever the spring produces. Require a drain or vent arrangement that matches the installed orientation, not the one that is convenient on the drawing.
Then require the two documents that make the rest enforceable: a seat test to API 598 in both the high pressure and the low pressure sequence, and a material certificate to EN 10204 3.1 for the wetted parts. Neither will stop a slug. Both are what allow a valve to be compared with another valve, and on a line that is going to damage its valves, the ability to compare is the difference between buying on price and buying on life.
J-VALVES supplies pipeline ball valves from 1/2 to 56 inch (DN15 to DN1400), ASME Class 150 to 2500, in floating and trunnion designs, with full port and reduced port bores, welded or flanged bodies for buried transmission service, seat and body materials certified to EN 10204 3.1, fire safe qualification to API 607 where the line carries hydrocarbon, and shell and seat tests to API 598 at 1.5 and 1.1 times rated pressure. On lines with a known two phase regime the seat arrangement, the bore and the drain position are agreed on the approval drawing against the flow data supplied with the enquiry, because those three decisions are the ones a slug will test first.
Frequently Asked Questions
Is a ball valve suitable for slug flow? As a block valve, yes, provided it is either fully open or fully closed and its seat arrangement matches the direction the differential takes. It is not suitable as a throttling device in a slugging line, and it is not suitable if the slugs carry abrasive solids and the valve is cycled often, because the seat band is the part that takes the damage.
Can I throttle a ball valve to control slugs? You can, and it will work for a while, at the cost of the seat and the ball port edge. A part open ball valve creates the highest velocity in the line at the point where the material is softest, and in a slug that jet is carrying solids. Slug control belongs upstream, at the separator, the level control or the pig schedule, or in a trim designed for throttling.
Why does my ball valve leak only after liquid carries over? Because the liquid is what delivers solids to the seat band, and because a liquid film changes the sealing mechanism at the contact. A leak that tracks the flow regime rather than the pressure is a seat surface problem, not a pressure problem, and it usually shows as a polished band with fine scoring once the valve is opened.
Does a slug cause water hammer? Not by arriving. A slug becomes a pressure event when something stops it, and the most common something is the valve closing on it. If the surge appears at the moment of closure rather than at the moment of arrival, the closure is the cause and the closing time is the variable to change.
Which seat material should be used on a line that slugs? The one matched to the solids and the temperature rather than to the gas, because the gas never reaches the seat in a way that matters. On a line that slugs often with abrasive particles, a harder seat and a harder ball surface last longer than a soft seat that conforms better, and the trade is sealing class against life. The comparison of PTFE, RPTFE, PEEK and metal seats covers the temperature and pressure side of that choice; the solids side is a conversation with the valve supplier about what the liquid actually carries.


