


A cycle count is a result, not a property
"One million cycles" reads like a specification and behaves like a slogan. It is not a property of the valve the way a pressure class or a bore diameter is a property. It is a result produced by a test stand, and that test stand has a medium, a pressure differential, a temperature, a cycle rate, a dwell time, a leakage criterion and a definition of what counts as one cycle. Change any one of them and the same valve produces a different number. Change two and the number is not comparable at all.
This is not a complaint about honesty in catalogues. It is a statement about where the wear happens: at the interface between the seat and the ball, under a load that comes partly from line pressure and partly from seat preload, at a temperature that decides whether the polymer can recover after each stroke. Not one of those three quantities appears in the phrase "one million cycles".
What a manufacturer can publish honestly is the condition set plus the raw data behind the count. What a buyer can require honestly is a test at the conditions of their own service. Everything in between is a comparison between two valves tested the same way, which is useful, but only inside that comparison.
What one cycle is, and where the definitions part company
One cycle is normally open, close, open — the valve ends where it started, so the next cycle begins from the same state. That much is agreed. The divergence starts with the first question anyone asks about the test stand: is the valve cycled with pressure on it?
Unpressurised cycling moves the ball with nothing but the seat springs and the stem friction resisting. It measures the mechanism: whether the trunnion bearings bind, whether the seat pocket was machined concentric, whether the stem turns freely after assembly. As a production check it is worth running on every valve, because it catches an assembly fault in ten seconds. As a life figure it is close to worthless for a soft-seated valve, because the load that destroys a polymer seat — line pressure pressing the seat into the ball while the ball turns — is simply absent.
Cycling with the differential held across the closed valve is the configuration that means something. The upstream seat is loaded by line pressure, the ball is pushed into the downstream seat, and the quarter turn scrubs two faces together under the pressure the valve will see in service. This is the test that produces a number worth arguing about.
Then come the secondary conditions, and each one moves the result. Is the valve cycled hot or at ambient? A PTFE seat at ambient and the same seat at the top of its range are two different materials in mechanical terms. At what rate? A fast cycle does not leave the polymer time to recover and heats the interface; a slow one does both. Does the valve dwell closed, and for how long? A valve that sits closed for a shift is not the same as one that is cycled continuously, because creep under load is a function of time as well as of cycles.
Three different tests that all get called life testing
The confusion in the market comes from three legitimate activities sharing one name.
The type test runs on prototypes or on a sample from the first production batch. Its purpose is to find the failure mode, not to certify a number. A well-run type test ends with a torn-down seat, a photograph of the wear track, a torque curve and a statement of what failed first. The cycle count is the by-product; the failure analysis is the deliverable.
The routine functional check runs on every valve or on a sample of every order. A handful of cycles, torque recorded, then the seat test. It proves the valve was assembled correctly. It says nothing about life, and it is where most "cycle tested" claims in a datasheet actually come from.
Condition monitoring on site is the only life data that belongs to the real service, because it is the only data taken with the real medium, the real differential and the real temperature. Very few sites keep it, and the ones that do can tell you more about a valve's life in one spreadsheet than any brochure.
Mixing the three is how a short bench check becomes "tested to one million cycles" in a sales conversation. The question that separates them is not "how many cycles" but "what was on the stand, and what did you measure besides pass or fail".
The five wear mechanisms, and the signature each one leaves
A cycling test is only interpretable if it can tell these apart. They progress at different rates, they respond to different variables, and they point at different fixes — which is why a single leakage number at the end of a test tells you almost nothing about what to change.
Adhesive wear and burnishing of the seat. The polymer smears and polishes against the ball. Torque falls slowly and steadily as the surface becomes smoother, leakage creeps up as the seat thins, and the seat face at teardown is glossy with a faint dished track. This is the normal, benign wear mode, and the fix for a short life here is more seat thickness or a harder grade, not a different body style.
Abrasive embedding. Particles pressed into the seat become the abrasive that cuts the ball. Torque rises because the seat is now a loaded lap, and the leak appears as a scratch track on the sphere rather than as a uniform seep. The variable that controls it is medium cleanliness, not cycle count, which is why a valve that lasts forever on filtered water fails in a year on an unfiltered line.
Extrusion and cold flow. The seat material is squeezed into the clearance between seat carrier and body, or between seat and ball, and the volume that provided preload is now somewhere else. The signature is leakage that appears first at low pressure, before it appears at high pressure, because the seat has lost the elastic reserve that seals when the differential is small. Near the top of the material's temperature range this accelerates sharply.
Ball surface damage. A dent, a scratch, a weld bead that went through the bore. The signature is leakage at high differential only, with the low-pressure test still passing, because the seat can still bridge a local defect until the pressure pushes it into the defect.
Stem seal wear. Unrelated to the seat and independent of the differential, but it accumulates with every stroke. It shows up as an external leak at the gland, and it is the one mechanism a cycle test on a bare valve will not catch if the test rig does not hold pressure on the stem.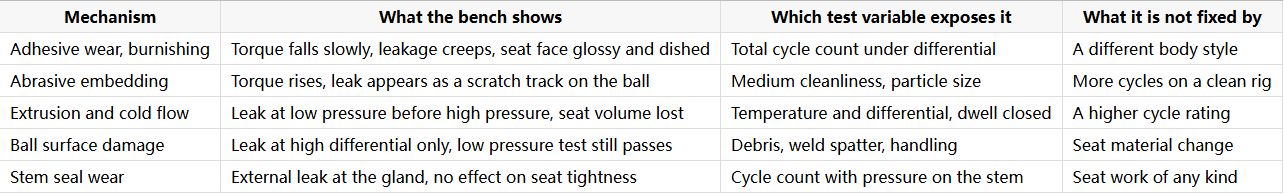
Torque is the measurement; leakage is only the gate
A test that reports pass or fail at the end has thrown away the data that predicts. The three torque values a cycling test should record are the ones that mean different things. Breakaway torque is what it takes to lift the seat off the ball, and its trend is the single most informative curve in the whole test. Running torque is the bearing and bore friction with the seat unloaded. Seating torque is the ball being pressed home at the end of the stroke.
A rising breakaway trend means something is being added: seat swelling from chemical attack, particles embedding, a stem packing that has been re-tightened, or a seat that is extruding into a narrowing clearance. A falling breakaway trend means something is being lost: seat preload relaxing, spring load decaying, the polymer creeping away from the ball. The two trends call for opposite responses, and a leakage-only report cannot tell them apart, because both end in the same place.
This is also where the actuator enters the argument. A valve that is cycled by an actuator set to deliver far more seating torque than the seat needs is being extruded a little on every closure, and its life will be shorter than the same valve cycled by hand. The chain from breakaway torque through running torque to seating torque, and the margin the actuator has over each, is set out in the actuator torque article; for endurance purposes the point is narrower — the endurance test should be run at the torque the site will actually apply, not at whatever the bench cylinder happens to deliver.
Where the standards stop, and why the number is left to the buyer
The standards a ball valve is bought against fix how tight it must be and how that tightness is proved. API 598 sets the shell test at 1.5 times rated pressure and the seat test at 1.1 times, with a duration that depends on size; ISO 5208 defines what "tight" means in rates, from no visible leakage at one end of the scale to a quantified allowance at the other. Those two documents are the backbone of acceptance, and they are discussed in detail in the ISO 5208 leakage rate article.
What none of them does is put a number of cycles into the purchase. A valve can be fully compliant with every product standard and have no declared life at all, because the standards describe a condition at the moment of test, not a duration. The one family of standards that does write cycling into its protocol is the fugitive-emission family, where a stem seal's endurance has to be demonstrated by repeated thermal and mechanical cycles — and that is a statement about the stem seal, not about the seat, which is why it is a separate subject from this one.
So the cycle count is a commercial negotiation rather than a compliance item. That is not a gap in the system; it is a correct allocation, because the buyer knows the medium, the differential and the temperature, and the standard does not. The consequence is that the buyer has to write the requirement, and a buyer who writes "one million cycles" without the conditions has written a sentence that cannot be checked.
Temperature is the variable that ruins extrapolation
The seat materials that carry most ball valve service have known ceilings: PTFE around 180 °C, PPL around 280 °C, PEEK around 260 °C, with metal seating beyond what a polymer can hold. Those are limits, not operating points, and the difference matters for life far more than for pressure rating. A PTFE seat tested at ambient and the same seat tested near its ceiling are not the same test, because creep accelerates with temperature and the seat's elastic recovery — the thing that keeps it tight between cycles — falls as the temperature rises.
Thermal cycling adds a second effect that a steady-state hot test misses entirely. The seat carrier, the body and the ball expand by different amounts, so the interference between seat and ball changes with every temperature swing, and the seat is worked in a way that no isothermal test reproduces. A valve that runs at a constant temperature and a valve that is bathed and cooled on a batch schedule can have the same medium, the same pressure class and the same size, and completely different lives. The seat material comparison covers how the grades behave; the endurance question is what the grade does after thousands of those swings, which is why a metal-seated valve's clearance has to be set for the hot condition rather than the shop condition.
Reading a competitor's cycle claim without being unfair
None of this means a published number is dishonest. It means the number needs a condition sheet before it can be used. Six questions turn a claim into information. Was the valve a prototype or a production unit? Was it cycled pressurised, and with the differential across the closed valve or across the open one? What medium — water, air, oil, slurry — and at what temperature? What cycle rate and what dwell? What leakage criterion, measured how often? And what failed first, if anything did?
The last question is the one that separates a test from marketing. A valve that completed the count and was then torn down with a measured wear track is a data point. A valve that "passed one million cycles" with no statement of what was measured is a phrase. A supplier who cannot answer the six is not necessarily misleading anyone; more often they are repeating a number that originated somewhere upstream and lost its test report on the way.
The site conditions that decide life more than the valve does
In the field, the ranking of causes is not the ranking that a bench test suggests. Debris is first. A valve on a line without a strainer, or with a strainer that was bypassed during commissioning, embeds particles in the seat in the first weeks and then spends the rest of its life cutting the ball. The fix is upstream of the valve and costs a fraction of the valve.
Throttling is second. A standard ball valve left part open puts the seat in the highest-velocity, most erosive position it will ever see, and it does so continuously rather than for a quarter turn. A valve recorded as "open" in a log while the lever sits at forty-five degrees is a valve being destroyed quietly, and no cycle rating covers it because it is not cycling.
Third is the pressure event rather than the pressure level. Water hammer, a fast closure against a moving column, a pump trip — the seat sees a load far above the rating for a moment, and a polymer seat that is extruded once does not come back. Fourth is the actuator setting already discussed. Fifth is chemical attack on the seat, which shows up as swelling and a rising breakaway torque long before it shows up as leakage.
What to write into the purchase order
Six lines turn endurance from an adjective into a requirement. Define one cycle explicitly and state the pressure condition during cycling, because unpressurised cycling is a different test with a different result. Name the medium, its cleanliness and the temperature, and say whether the test is isothermal or thermally cycled. State the cycle rate and the dwell at each end. Name the leakage criterion by ISO 5208 rate and the interval at which it is measured — a valve that holds Rate A for the first thousand cycles and Rate D at the end has a different value from one that never leaves Rate A. Require breakaway and running torque to be recorded at stated intervals and reported as a curve, not a single number. And require the report to state what failed first, with photographs of the seat and ball at teardown.
If a cycle count is quoted by the supplier, require the condition sheet behind it as a deliverable, not as a courtesy. A number without its conditions cannot be compared, and a comparison is the only thing a buyer is actually trying to make.
J-VALVES builds ball valves from 1/2 to 56 inch (DN15 to DN1400) in ASME Class 150 to 2500, with shell tests at 1.5 times and seat tests at 1.1 times rated pressure and EN 10204 3.1 certificates available for ball and stem. Endurance is quoted against the conditions named in the enquiry — medium, differential, temperature and leakage criterion — rather than against a catalogue cycle count, and production valves are functionally cycled with torque recorded before the seat test. Where the duty is abrasive rather than simply repetitive, the wear question is a materials question, and the trunnion wear and erosion article covers which design features change the rate. Where the seat has already failed, the choice between re-seating and replacing is set out in the in-line seat replacement article.
Frequently Asked Questions
How many cycles should a ball valve last? There is no universal number, and any figure quoted without conditions should be treated as a comparison rather than a specification. Life depends on the differential across the closed valve, the medium and its cleanliness, the temperature relative to the seat material's ceiling, the cycle rate, and whether the valve is cycled by an actuator that over-seats it. A soft-seated valve on clean water at moderate temperature and a metal-seated valve on slurry at high temperature are not on the same scale at all.
Is dry cycling a valid life test? It is a valid assembly check and an invalid life test for a soft-seated valve. With no pressure on the seat, the load that causes extrusion and scrubbing is missing, so the test measures bearing friction and stem freedom rather than seat wear. It becomes useful only when the same valve is then cycled under differential and the two results are compared.
Why does leakage appear before torque changes, or the other way round? Because the two measure different things. Torque responds to preload and friction, so it moves as soon as the seat swells, embeds particles or loses its elastic reserve. Leakage responds to the contact band, so it stays inside the criterion until the band is actually broken. Which one moves first tells you which mechanism is running, which is exactly why a cycling test should record both.
Does a higher cycle rating mean a better valve? Not by itself. A valve tested unpressurised on clean water will always out-count a valve tested under differential on the medium it was sold for, and the second number is the smaller and more useful one. Compare counts only when the condition sheets match, and prefer the supplier who publishes the conditions over the one who publishes the biggest number.


