


Three devices on a gantry, and only one of them is a valve
Walk to the end of a bottom loading arm and there are three pieces of hardware in series, and they are routinely discussed as if they were interchangeable. The first is the isolation valve, almost always a quarter-turn ball valve, whose job is to hold the header contents on the rack side. The second is the dry break coupling, whose job is to close both halves of the connection when the hose comes off. The third is the breakaway, whose job is to separate at a defined pull force before the structure behind it fails.
None of the three does another's work, and the confusion between them is the root of most of the arguments about leakage on a loading rack. A valve that passes does not make the coupling leak, and a coupling that drips on disconnection does not mean the valve is worn. The breakaway has nothing to do with either, until the day it operates, at which point it decides which side of the release stays closed.
The valve is the piece that gets specified with the most confidence and inspected the least, because it is the only one of the three whose failure is invisible during normal operation. A coupling that is going to drip announces itself the moment it is opened. A breakaway either works or the arm is on the ground. The valve, when it starts to pass, produces no external sign at all, and the product goes into the tank instead of onto the concrete where somebody would notice.
The duty cycle is the part nobody writes down
A ball valve on a process line may be operated a handful of times a year and is bought on that basis. The same valve on a loading gantry is operated on every truck, twice, for as long as the rack is in service. The annual count is a number the terminal knows from its weighbridge records and the specification almost never contains, which means the valve is designed, tested and warranted against a cycle count that has no relationship to its life.
That mismatch does not show up as a strength problem. A ball valve is not failing structurally on a loading rack; the pressure is modest and the body has margin. It shows up at the seat, because the seat is the one part whose condition depends on how many times it has been loaded and unloaded rather than on how much pressure it has held. Each closure presses the seat against the ball, each opening releases it, and the material at the contact band is worked in a way that a static test never reproduces. A seat that holds 1.1 times rated pressure for the full API 598 duration on the test bench has demonstrated that it can seal once, under ideal conditions, with clean test water and a stationary ball.
The second thing the count does is change what maintenance means. On a process valve, a seat is a part that is replaced when a leak is found. On a loading rack, by the time a leak is found the valve has been passing product into trucks for an unknown number of loads, which means the maintenance decision is not just about the valve. This is the argument for treating the rack valve as a consumable with a planned replacement interval, and for choosing the interval from the counted cycles rather than from the calendar.
Creep, and the three ways a seat starts passing
Internal leakage on a loading valve is usually described as passing, and passing has three distinct mechanisms that are told apart by how the leak behaves rather than by how big it is.
The first is creep in the seat material. A soft seat is a polymer ring pressed against a polished ball, and polymers deform under sustained load. The deformation is slow and it is not elastic, so the ring thins at the contact band and the contact stress falls. The signature is a leak that grows gradually over months, is worse when the line is hot, and is absent or nearly absent when the valve is first closed and the seat has just been loaded. This is the mechanism that a low pressure bubble test at the bench does not catch, because the test loads the seat once and reads it immediately.
The second is indentation from solids. Product arriving at a loading rack is not clean: it carries rust from the header, catalyst fines from upstream, sand from a road tanker that was not properly closed, and polymer from a previous service. When the valve closes on a particle sitting on the seat band, the particle is pressed into the polymer and leaves a pit with a raised lip. The signature is a leak that is roughly constant and does not change with temperature or with how long the valve has been shut, and that appears suddenly after a period of no leakage at all.
The third is scoring on the ball. A particle that is dragged across the ball while the valve is being operated cuts a scratch that runs across the sealing band rather than along it, and a scratch that crosses the band is a channel from the upstream side to the downstream side regardless of how well the seat conforms. The signature is a leak that changes with the valve position and that may disappear entirely when the ball is moved a few degrees, which is exactly why a valve that passes on one closing and fails on the next is usually a scored ball rather than a worn seat.
Telling the three apart matters because only one of them is fixed by a new seat. A creeping seat is replaced. An indented seat may be replaced, but if the product is still carrying solids the new seat will be indented too, and the answer is a strainer or a different seat material rather than a maintenance campaign. A scored ball is not fixed by a seat at all, and a rack that keeps replacing seats on a valve with a scored ball will keep finding leaks.
Why shut-off cannot be proved on a gantry
A seat test needs a closed volume downstream of the closed valve, instrumented so that a rise can be seen. On a loading rack that volume does not exist. Downstream of the valve sit the coupling, the hose or arm, and a tank truck that is either connected or not, and the only closed volume available is the truck itself, which is not a test vessel and is not instrumented to the sensitivity the test requires.
So the operator is left with three weaker proofs. The first is the factory seat test, which as already noted is a single closure under ideal conditions and says nothing about the state of the seat today. The second is the visual check at disconnection, which only shows what escapes from the coupling, not what went past the valve. The third is the batch controller, which will show a discrepancy if the delivered volume does not match the metered volume, but only after the truck has left and only if somebody reconciles the two.
This is the reason a passing valve can run for a long time on a busy rack. The failure has no external signature, the available proof is indirect, and the person best placed to notice it is the driver, who has no reason to look and no instrument to look with. A terminal that wants to find these valves early has to build the detection into the routine, for instance by isolating the arm, venting the short spool between valve and coupling, and watching whether pressure returns. It takes a minute and it is the only direct test available on the rack. The same logic that applies to condition monitoring on process valves applies here in a cruder form: pick a signal that changes before the consequence does.
The product switch nobody models
Most loading racks are not dedicated to one product. The same arm may load gasoline, diesel, an ethanol blend and a biodiesel blend in the course of a shift, and the valve sees the whole list. The seat and the stem seals see it too, and they do not respond to all of it in the same way.
Elastomer components swell in hydrocarbon service and shrink or harden when the aromatic content drops. An ethanol blend is the harder case, because ethanol is a solvent as well as a fuel: it extracts material from elastomers, and the extraction is progressive. The observable result is not a leak but a change in feel. The valve becomes heavier to operate as the seals take up volume, or the stem seal loses resilience and begins to weep after the valve has been sitting closed. A rising operating torque on a rack valve is very often read as contamination or as a dry stem, when it is the seals responding to a product they were not selected for.
Ethanol brings a second issue that has nothing to do with polymer compatibility. It has low electrical conductivity, so static charge generated by flow does not dissipate through the liquid the way it does in a hydrocarbon with additives. The path that has to carry it is the one through the ball, the stem and the body, and a valve whose anti-static provision has been lost, usually because the spring or the contact has been left out during a repair, is a valve that will not carry it. That failure is not visible and it is not a leakage failure, which is why it survives inspections that are looking for leaks.
The practical answer is to specify the seal package from the product list rather than from the design temperature, to state the full list of products including the blends, and to accept that a rack which switches products needs either a wider compatibility envelope or a shorter seal replacement interval. A single-material specification copied from a gasoline-only rack and applied to a rack that now loads ethanol is the most common way this goes wrong.
Vapour recovery is a second line, with its own valve
Bottom loading is closed loading: vapour displaced from the tank has to go somewhere, and on a modern rack it goes back through a vapour recovery line that runs alongside the product line and connects to the truck at the same time. That line has its own valve, usually smaller, usually lower in pressure, and almost always treated as an accessory rather than as part of the containment boundary.
It is still a containment boundary. A vapour valve that passes does not put liquid on the ground, which is why it is ignored, but it does two things. It allows product vapour to escape to atmosphere when the rack is idle, which is an emission and an odour and in some jurisdictions a permit issue. And it allows the vapour space of the truck to be connected to the header when it should be isolated, which matters on a rack where different products share a recovery header and cross-contamination between loads is a quality problem rather than a safety one.
The valve on this line has the same seat mechanism as the product valve and a fraction of the attention. It should be on the same replacement interval and it should be tested with the same vent-and-watch method, because it is the cheapest place on the rack to prevent an emission complaint.
Overfill protection does not live in the valve
A loading rack needs overfill protection, and it is worth being explicit that this is not a valve function. The protection is a separate system: a sensor on the truck, a signal to the batch controller, and a command that closes the flow path. The valve executes the command. It does not decide when to execute it, and a valve that is closed by an operator who judged the fill by sound or by experience is not overfill protection, it is a habit.
Where this becomes a valve question is at the interface. The closure has to be fast enough to matter, which means an actuated valve with a defined closing behaviour rather than a manual one, and the position feedback has to report the ball rather than the handle. A limit switch that senses the actuator stem at the end of travel is reporting that the actuator finished its stroke; it is not reporting that the ball is against the seat. On a rack where the interlock is the last barrier, that distinction is the whole point of the interlock.
Where the breakaway sits decides what survives
The breakaway is a mechanical fuse, and its position decides what is protected. Sitting between the valve and the hose, it parts and leaves the valve on the rack, closed, with the hose going with the truck; that is the only arrangement that puts a valve between the header and the break. Sitting upstream of the valve, between header and valve, it parts and takes the valve away with the arm, leaving the header side of the joint to whatever closure the breakaway itself provides. Sitting downstream of the coupling, it parts and leaves the coupling with the truck and the rack side open.
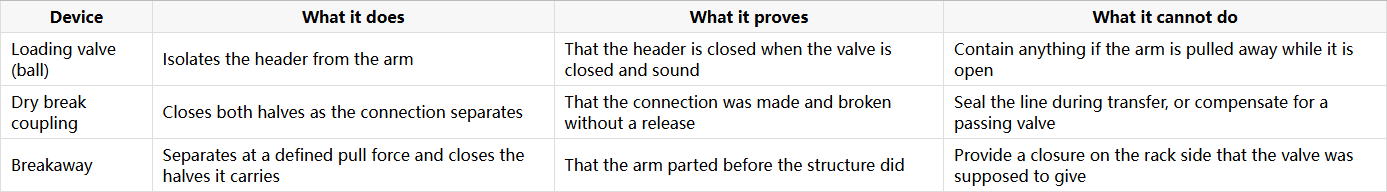
Two details deserve a line in the specification. The first is whether the breakaway is resettable or single-use, because that decides whether the terminal carries a spare on the shelf or waits for a delivery after every incident. The second is which side of the breakaway the valve sits on, because that decides whether a drive-away leaves the rack with a closed valve and a damaged arm, or with an open pipe and no valve at all. Both are cheap decisions at the order stage and expensive ones afterwards.
What belongs on the enquiry
The specification for a rack valve is short and almost always incomplete. Six items close most of the gap.
Give the annual cycle count, taken from the terminal's own records, and state whether the valve is expected to last a fixed interval or a fixed number of operations. Give the full product list including blends and any product that is loaded seasonally, and let the seal package be selected from that list rather than from the design temperature. State the seat and stem seal materials and the reason for each, so that a substitution during manufacture is visible. State whether the valve is manual or actuated, and if actuated, require position feedback that reports the ball rather than the actuator stem. State the anti-static requirement explicitly, because it is the one feature that is removed during a repair without anyone noticing. And state the pressure test basis, API 598 shell at 1.5 times and seat at 1.1 times rated pressure, with a certificate package that identifies the heat numbers of the pressure-retaining parts.
J-VALVES supplies API 6D trunnion mounted ball valves and floating ball valves from 1/2 to 56 inch (DN15 to DN1400), ASME Class 150 to 2500, with soft or metal seats, manual or actuated operation, and cavity vent and drain plugs as standard options. Bore selection for terminal duty follows the pressure loss and the risk of solids rather than the pigging requirement, which is set out in the comparison of full port and reduced port designs. Where a rack needs a positive isolation point for maintenance, double block and bleed arrangements give a vented barrier between the header and the arm. Shell tests run at 1.5 times and seat tests at 1.1 times rated pressure to API 598, and EN 10204 3.1 certificates are available on request.
Frequently Asked Questions
How often should a loading rack ball valve be replaced? From the cycle count rather than from the calendar. Take the number of loads per year from the terminal records, multiply by the operations per load, and set the interval against the number of operations the seat is expected to survive, which the manufacturer should state as a test condition rather than as a marketing figure. A valve on a rack that loads continuously is a consumable, and treating it as a permanent fitting is why passing valves are found late.
How can I tell if a loading valve is passing? Isolate the arm, vent the short spool between the valve and the coupling, and watch whether pressure returns. That is the only direct test available on a rack, because there is no closed downstream volume to pressurise. In service, a delivered volume that does not reconcile with the meter, or a persistent odour at the coupling, are the indirect signs. A drip at disconnection is the coupling, not the valve, until proven otherwise.
Why does a ball valve on a loading gantry get stiff? Usually because the stem seals have taken up volume in response to the product, and ethanol blends are the common cause because they extract material from elastomers as well as swelling them. Contamination on the stem and a dry stem produce a similar feel. The distinction matters because a stiff valve is often the first sign that the seal package was selected for a different product list.
Does a dry break coupling replace the need for a tight valve? No. The coupling closes the connection when it is separated; it does not hold the header while the connection is made. A passing valve on a rack with a good coupling produces no visible leak at all, which is precisely why it goes unnoticed, and the product ends up in the truck rather than on the ground.
Should a loading valve be full port or reduced port? For terminal duty the choice is driven by pressure loss and by the risk of solids settling, not by pigging, since a loading arm is not pigged. Full port gives the lowest loss and the least chance of a pocket holding product between loads. Reduced port is acceptable where the pump has margin and the product is clean, and it costs less at the same pressure class. Either way the bore should be stated on the order, because it is not implied by the size.


