


What an ESD valve is asked to do
An emergency shutdown valve is not a control valve that happens to close. Its job is to close, or to open, once, on demand, after an event that nobody planned, and to still be able to do it after years of sitting still. That one sentence rules out most of the attractive options. A valve that closes cleanly on day one and has a sticking stem on the day of demand has failed, and that failure never shows up in the torque figure printed on the datasheet.
Three properties decide whether a ball valve can carry the duty. The failure mode has to be the safe one without any external help. The closing path has to be short enough to matter. And the whole final element, valve plus actuator plus accessories, has to be testable without taking the process down. Most of the engineering argument is about which actuator type satisfies all three.
Spring return against double acting
A double acting actuator needs air to move in both directions. It is smaller, cheaper and holds torque symmetrically in both strokes, which makes it the right choice for isolation valves operated from a control room where the failure mode is not safety critical. On loss of instrument air it simply stays where it is. For an ESD valve that is usually the wrong answer, because the most likely cause of a demand is exactly the event that also takes out the air supply.
A spring return actuator stores energy in a spring pack and uses air only to move against it. Loss of air, loss of signal or a solenoid de-energising all release the spring and drive the valve to its fail position. The cost is paid twice: a larger actuator is needed to overcome the spring on the opening stroke, and the torque available on the closing stroke is not constant.
The spring torque curve, and why the sizing point matters
Spring torque rises as the spring is compressed and falls as it extends. At the valve's open position the spring is at maximum compression and stores its highest torque; as the valve strokes towards closed the spring relaxes and the available torque drops, often to between 35 and 40 percent of the starting value depending on the spring set. The valve torque does the opposite in the critical region: seating torque at the very end of the closing stroke is usually the highest torque the valve demands. The two curves therefore converge at the closing seat, and that intersection, not the break torque at the open position, is the point that decides whether the valve will actually shut.
A sizing that quotes only break torque will pass on the bench and fail on a cold morning. The correct method is to plot spring torque against valve torque over the full 90 degree stroke at the minimum air supply and the minimum ambient temperature in the specification, and require a margin at every point, not just at the start.
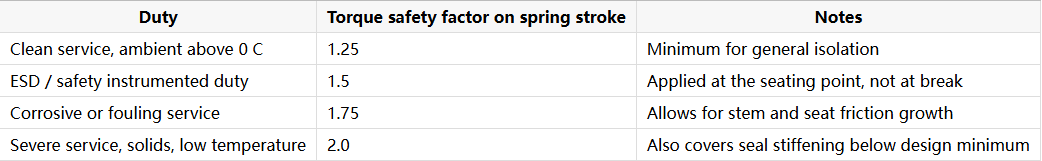
Failure mode has to be defined before the actuator is chosen
Fail closed is the default assumption and not always correct. A valve on a pressure relief path, a vent line or a fuel gas inlet may have to fail open. A diverting valve may have to fail to one particular leg. Writing failure close, failure open or failure last on the datasheet is the first line of the safety narrative, and it decides whether the spring pack is configured to close or to open, and whether the solenoid is energised to open or energised to close. Getting this wrong is a systematic error that no amount of torque margin corrects.
Failure last, meaning stay put, is not achievable with a spring return actuator without additional hardware such as a lock-up valve or a volume bottle. Where the process demands it, the block-and-bleed arrangement and the air volume needed to complete one stroke both have to be calculated, not estimated.
What IEC 61511 asks of the final element
IEC 61511 treats the valve, actuator and solenoid as one final element with a single probability of failure on demand, and it is usually the weakest part of the loop. The standard does not prescribe a valve type, but it does require that the final element has a defined and verifiable safe state, that its failure modes are analysed, and that proof testing demonstrates it reaches that state. A double acting actuator can be given a safe state by adding an accumulator, but the accumulator is then a component with its own failure mode and its own proof test, and it has to be maintained. A spring return actuator carries the safe state in a mechanical component that does not need an energy source to work.
Partial stroke testing follows from the same logic. Stroking the valve 10 to 20 percent and back proves that the stem is free, the solenoid shifts and the actuator moves, without interrupting the process. It does not prove seating, so full stroke proof tests at the interval defined in the safety requirement specification remain necessary. A spring return actuator with a partial stroke test facility and a position feedback switch gives both diagnostics without adding a second energy source.
Mounting, accessories and the details that fail
The interface is standardised and worth checking on the drawing. ISO 5211 defines the flange size, bolt circle and drive square or star, with F05 and F07 covering roughly 1/2 to 2 inch valves, F10 and F12 covering 2 to 6 inch, F14 and F16 covering 6 to 12 inch, and F25 and F30 covering 12 to 24 inch. A mismatch here is discovered at assembly, not at design review.
The accessories are where most installed failures originate. A solenoid mounted in a position where condensate collects, a filter regulator sized for steady flow and not for the surge when the actuator strokes, tubing that was not pressure tested after assembly, and a limit switch box whose cam drifts after a hundred cycles. Each is cheap to prevent and expensive to diagnose inside a safety loop. J-VALVES supplies trunnion mounted ball valves from 2 to 56 inch (DN50 to DN1400) in Class 150 to 2500 with pneumatic, electric and manual actuation, ISO 5211 mounting pads machined to the actuator drawing, API 607 fire tested designs and ISO 15848 fugitive emission tested stem sealing, with shell tests at 1.5 times and seat tests at 1.1 times cold working pressure.
Frequently Asked Questions
Should an ESD ball valve always be spring return? In most cases yes, because loss of instrument air is often the same event that creates the demand. Double acting is acceptable where the safe state can be proven another way, for example with a dedicated accumulator, but the accumulator then becomes part of the safety loop and needs its own proof test.
What torque safety factor applies to an ESD valve? 1.5 is the common specification for safety instrumented duty, applied at the seating point where spring torque is lowest and valve torque is highest. Severe and corrosive services often call for 1.75 or 2.0.
Can a double acting actuator be used with a spring? Only if it is built as a spring return unit, which means an added spring cartridge and a larger cylinder. A standard double acting actuator has no spring and will hold position on air failure.
Does partial stroke testing replace a full proof test? No. Partial stroke testing proves the valve is free and the pilot circuit works, but it does not verify that the valve seats or that it reaches the safe state under full differential pressure. Full stroke testing at the specified interval is still required.


