


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q47F
-
J-VALVES
Overview of the J-VALVES forged reduced bore trunnion valve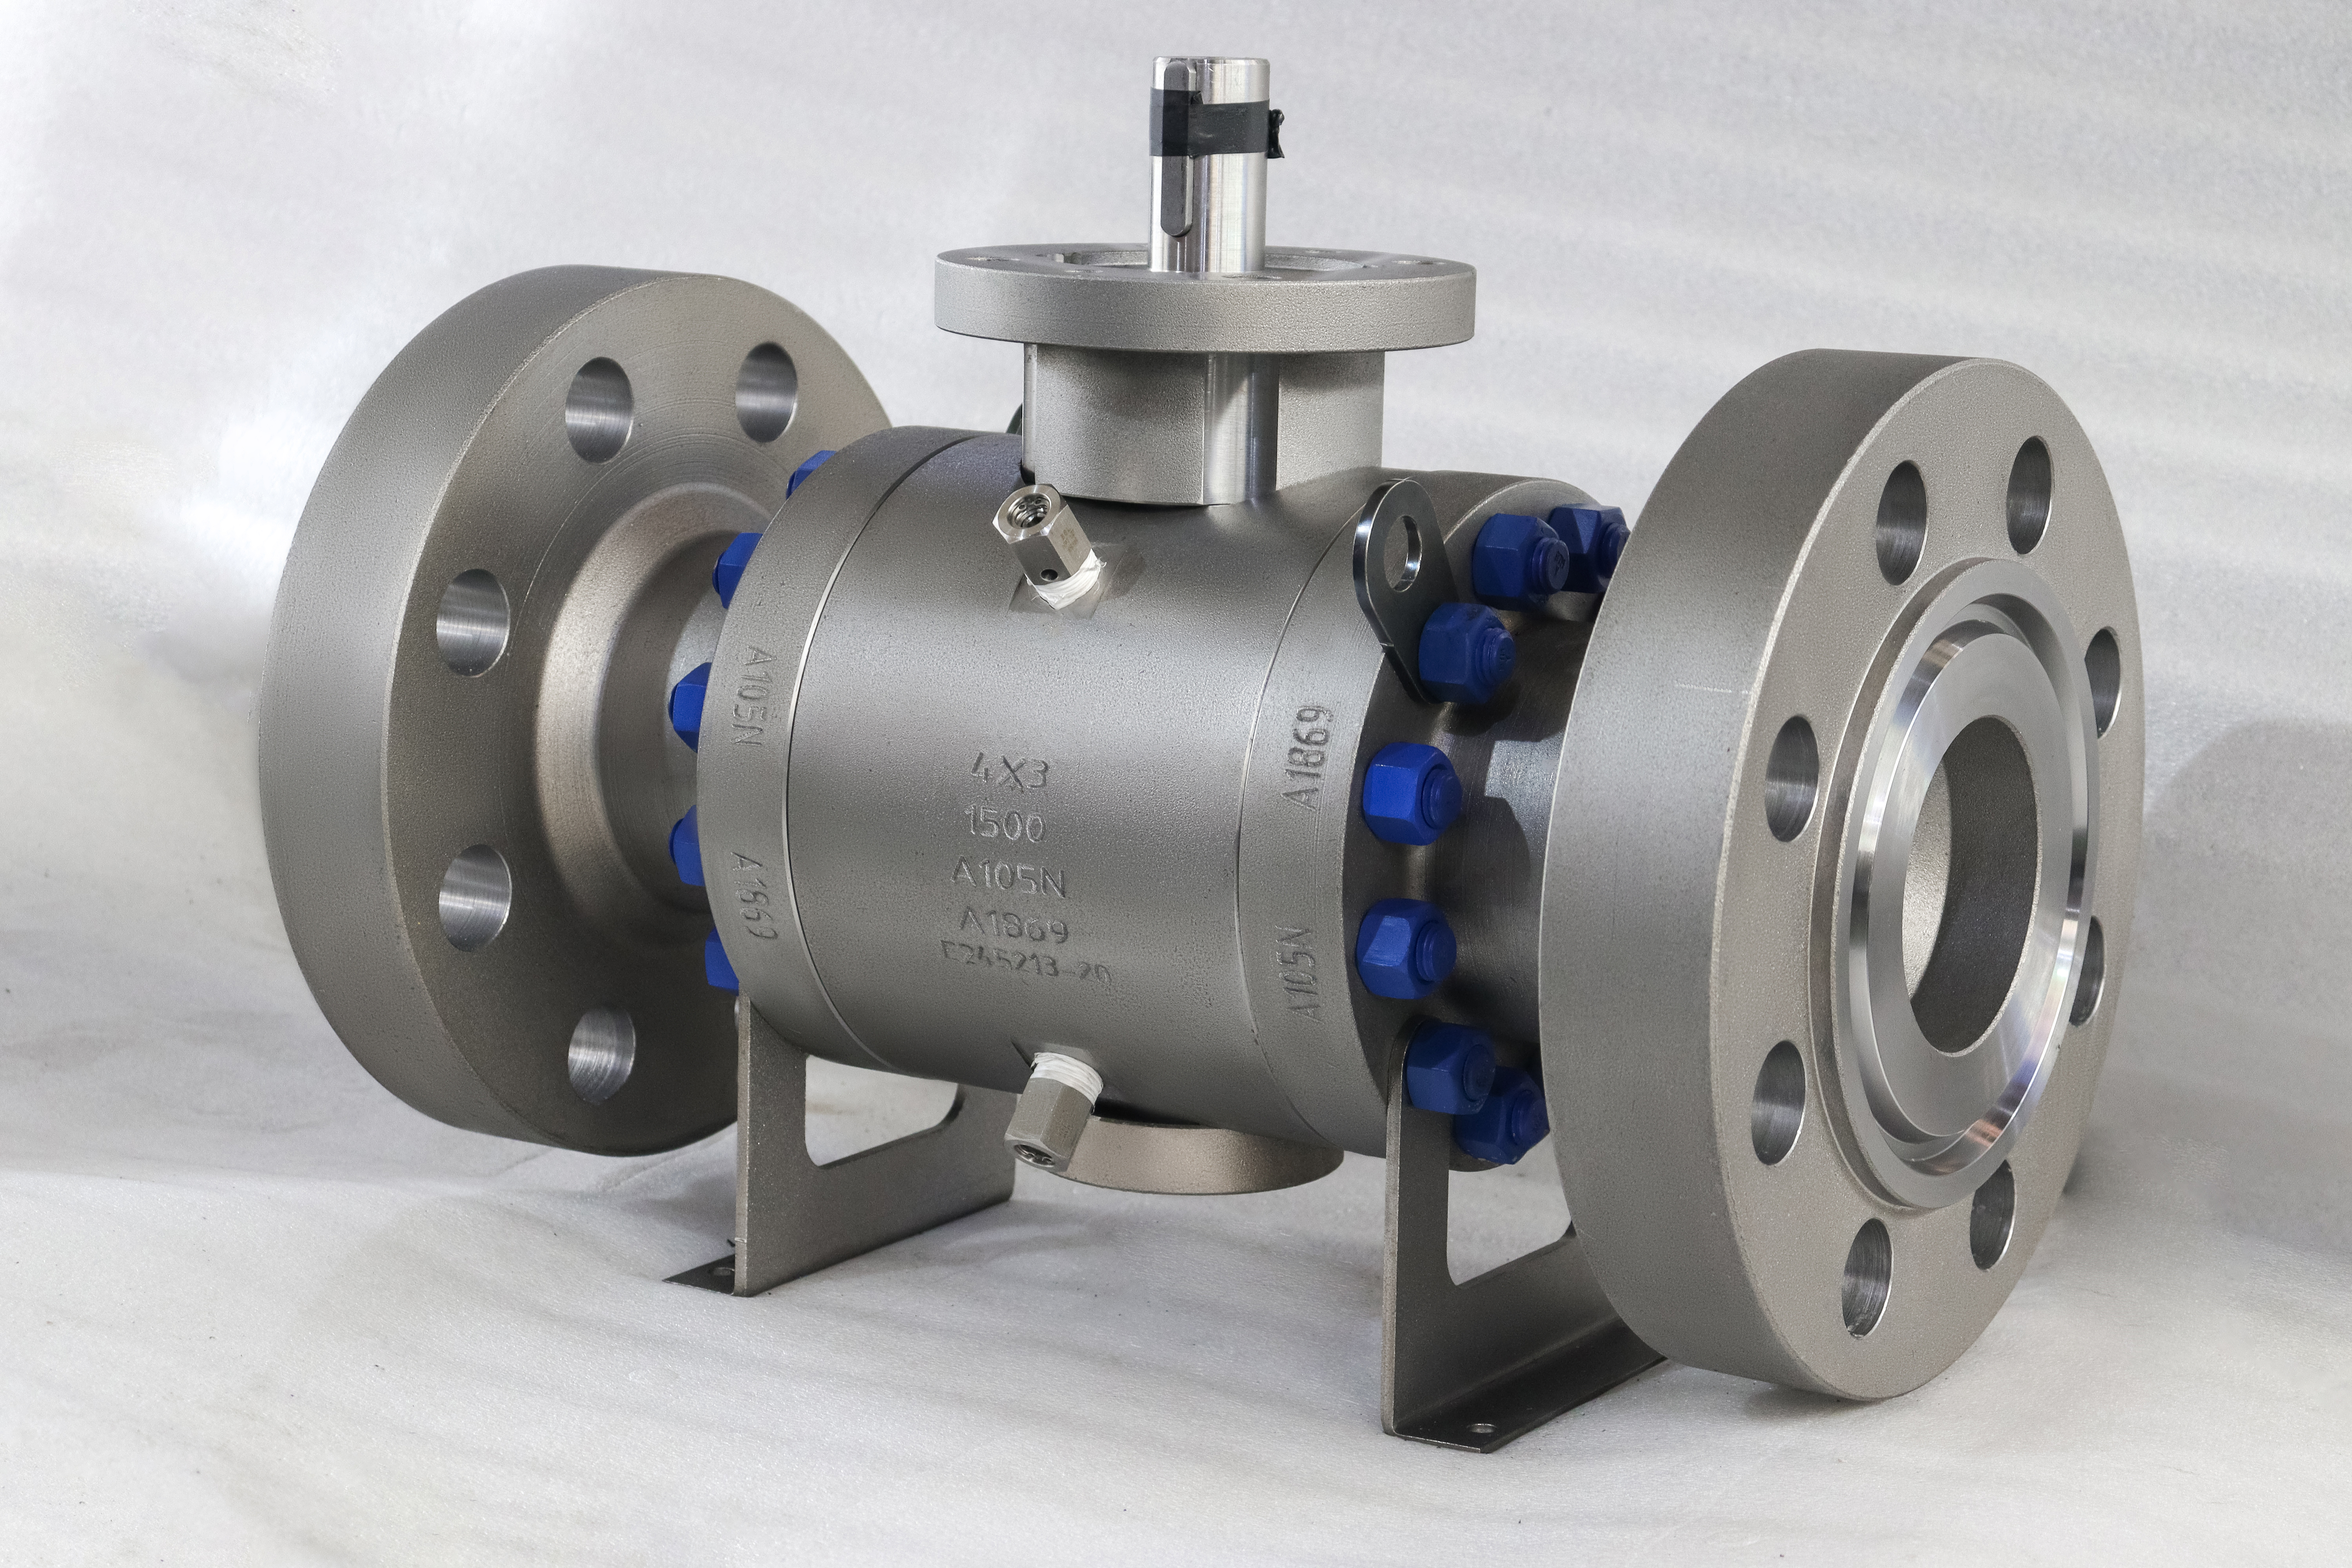
A reduced bore ball valve has a ball smaller than the pipe it sits in. That single fact is the whole of the design, and it produces two consequences that catalogues habitually get backwards: the valve costs less, and it obstructs the flow more. There is no version of this design in which the smaller bore improves the hydraulics, because the bore is the restriction.
The family runs from two inch to fifty six inch, Class 150 to Class 2500, in forged carbon steel, stainless or alloy steel, with a temperature range of minus 46 to plus 200 Celsius that belongs to the seat rather than to the body. The photograph on this page is a four by three inch Class 1500 A105N build, and the four by three notation is the part of the design that deserves the most explanation.
The argument here is narrow and it is worth stating plainly. Reduced bore is bought for the ball, the torque, the envelope and the price, not for the flow. A page that sells it as a way to reduce fluid resistance is selling the opposite of what the geometry does, and a buyer who reads that and then orders reduced bore for a low pressure drop duty will spend the rest of the project explaining the pressure drop.
Design and Construction
The body is forged, in three pieces on most builds, with the ball carried on trunnions and the seats spring loaded on either side. Forging is the normal route at these sizes because the body is compact and because a forged block can be machined all over without the porosity risk that a casting of the same section carries.
The four by three notation means a four inch end connection and a three inch bore through the ball. The valve is ordered, dimensioned and pressure rated as a four inch valve: the flanges are four inch, the face to face dimension is the four inch dimension, and the shell test is the four inch test. Only the bore is three inch, and that is why the notation exists rather than a single number.
That distinction matters at the interface between departments. A piping engineer who reads four by three as a four inch valve will allocate the space correctly and may still be surprised by the pressure drop. A process engineer who reads it as a three inch valve will size the pump correctly and may then find that the flange does not match the line. Both readings are half right, which is why the notation is written out in full on a good order.
The ball is smaller than a full bore ball of the same end size, and everything follows from that. A smaller ball means a smaller seat ring, a shorter body, less material in the forging, a lower operating torque and a smaller gearbox or actuator. On a Class 2500 valve in a large size, that chain of consequences is worth more than the pressure drop costs, which is why reduced bore is common at the top of the pressure range.
The comparison between the two is worth putting in one place, because the trade is a straight one and it should be made deliberately.
| Property | Full Bore | Reduced Bore |
|---|---|---|
| Bore through the ball | Matches the pipe bore | Smaller than the pipe bore |
| Pressure drop | Lowest of the ball valve family | Higher, and it is permanent |
| Pigging | The bore passes a pig | The shoulder stops a pig |
| Ball and seat size | Larger, higher torque | Smaller, lower torque |
| Body envelope | Longer, heavier | Shorter, lighter |
| Operator size | Larger gearbox or actuator | One size down, often |
| Cost | Higher | Lower at the same class |
| Best use | Pigged lines, low drop duties | On off service, cost driven |
The row that is most often misread is the pressure drop. A reduced bore valve has a contraction, a short throat and an expansion, and the loss across that combination is a permanent loss that the pump pays for continuously. It is not a large loss in a line that is mostly pipe, and it is a significant one in a line that is short, has several valves and runs at a high velocity.
The pigging row is the hard limit. A pig cannot pass a shoulder, so a reduced bore valve makes a line unpiggable at that point unless the pig is a special design that can be bypassed around the valve. That is a decision made at the line design stage, and it cannot be undone by choosing a different seat or a different operator later.

Material Options
The forged body covers carbon steel, stainless and alloy steel, and the choice follows the medium and the temperature rather than the pressure. A105 covers general service and A105N is the same grade in the normalised condition, where the N is a heat treatment state and not part of the grade name. The low temperature grades cover cold duty, and the alloy grades are there for temperature rather than for strength.
The ball and the seat are where the shut off is decided. A hardened stainless ball with a reinforced PTFE seat gives tight shut off at moderate temperature, and a metal seated build gives temperature capability at the cost of a leakage rate that is a rate rather than zero. On a reduced bore valve the seat is smaller, so the same seat material sees a lower total load than on a full bore valve of the same end size, which is one of the reasons reduced bore builds tolerate higher classes.
The stem and the packing follow the temperature. Below about two hundred Celsius a PTFE based packing is normal, and above it the packing becomes graphite and the gland hardware changes with it. That change is often missed when a valve is uprated, because the body and the seat get all the attention and the packing is treated as a consumable.
Technical Specifications
| Item | Value |
|---|---|
| Size range | Two inch to fifty six inch, DN 50 to DN 1400 |
| Pressure class | Class 150 to Class 2500, PN 20 to PN 420 |
| Notation | End size by bore size, for example four by three |
| Body | Forged carbon steel, stainless, or alloy steel |
| Ball | Hardened stainless or alloy steel |
| Seat | PTFE, reinforced PTFE, or metal |
| Ends | Raised face flange or butt weld |
| Face to face | The dimension for the end size, per ASME B16.10 |
| Temperature | Minus 46 to plus 200 Celsius, seat dependent |
| Test | API 598 shell and seat |
The face to face row is the one that catches buyers out on a replacement. A four by three valve is dimensioned as a four inch valve, so a replacement ordered as a three inch valve will be short in every dimension. The safest way to order a replacement is to send the gap and the flange drillings rather than the model number, because the model number has already lost the information that matters.
Standards and Compliance
| Requirement | Document | What It Means Here |
|---|---|---|
| Product requirements | API 6D | Design, materials, marking, testing |
| Wall and rating | ASME B16.34 | Rating by group, falls with temperature |
| Pressure test | API 598 | Shell at 1.5 times, seat at 1.1 times |
| Fire test | API 607 or ISO 10497 | Type test with a stated scope |
| Material certificate | EN 10204 3.1 | Heat number per pressure part |
| Heat treatment | A105N normalised, recorded | The N is a condition, not a grade |
| Flanges | ASME B16.5 | Class and size decide the drilling |
The A105N line is worth a sentence because it appears on orders as if it were a material. A105 is the grade and the N says the forging was normalised after forging, which changes the grain structure and the toughness. A certificate for A105 without a normalising record is a certificate for a valve that may not be what was ordered, and the difference cannot be seen on the valve.
Manufacturing Process
The forging starts as a billet that is upset and punched, then machined. Because the body is short in the reduced bore design, the forging is smaller than the equivalent full bore body, and that is where a large part of the saving comes from before any machining starts.
The bore is machined through the ball and the body in line with the seat pockets, and on a reduced bore valve the transition from the end bore to the ball bore is a machined step. That step has to be radiused rather than sharp, because a sharp step in a high velocity line is where erosion starts and where debris collects.
A forging is not automatically a cleaner body, but it is a body that can be examined in a way a casting cannot. Ultrasonic examination looks through the section for internal discontinuities, and magnetic particle examination finds surface indications after machining. On a high pressure body those two examinations are the reason a forging is chosen, and they belong on the order as a scope rather than an assumption: a forging that has been hydrostatically proof tested and painted has been pressure checked and has not been examined.
The ball is ground and lapped, and on a metal seated build it is lapped against its own seat ring so that the two surfaces match. That pairing is why a metal seated spare is a pair rather than a part, and why a ball from one valve should not be fitted into a seat from another.

Quality Control and Testing
| Step | Check | Acceptance |
|---|---|---|
| 1 Incoming | Heat number and normalising record for A105N | Chemistry, mechanicals, condition |
| 2 Identity | Positive material identification on body and trim | Grade match |
| 3 Bore | Bore diameter against the order notation | Drawing figure |
| 4 Step | Transition radius at the bore step | Drawing tolerance |
| 5 Shell test | Body and joints at 1.5 times | API 598, no leakage |
| 6 Seat test | Each seat at 1.1 times | API 598 rate |
| 7 Torque | Operating torque recorded | Works limit for the operator fitted |
| 8 Final | Drained, ends masked, marked, crated | Works standard |
The bore check is specific to this design. A valve whose bore has been machined to the wrong figure is still a valve that holds pressure, still passes a seat test and still opens and closes. It is simply a valve with a different pressure drop from the one the line was designed around, and there is no test on the bench that will reveal it.

Applications and Industry Service
Reduced bore belongs on on off service in lines that do not need to be swept: isolation at a pump discharge, block valves at a vessel nozzle, sectionalising valves in a utility header, and the many places where a valve is either open or closed and the flow is decided elsewhere. In those duties the pressure drop is irrelevant because there is a control valve doing the regulating.
It also belongs where the envelope is tight. A shorter body and a smaller operator can be the difference between a valve that fits inside a skid and one that requires the skid to be redesigned, and on a packaged unit that is a real constraint rather than a preference.
It is the wrong valve where the line is pigged, where the pressure drop budget is tight, and where the medium is abrasive. In an abrasive service the higher velocity through the reduced throat accelerates erosion, so the saving on the valve is paid back in seat life. That is the trade that a page describing reduced bore as a flow improvement never mentions.

Installation, Operation and Maintenance
Install the valve with the arrow or the marking in the direction the line was designed for where a preferred direction is stated, and confirm the flange drillings before the valve is lifted into place. A four by three valve ordered against a three inch line will not bolt up, and that mistake is made more often than the notation suggests.
Operate the valve fully open or fully closed. A reduced bore valve part open is a throttling orifice with a ball and two seats in the high velocity jet, and the seat will be cut before the line is due for its next shutdown. If the duty needs regulation, the answer is a control valve, not a partly open ball valve.
For maintenance the line is isolated, vented and drained, and the body is opened at the end that carries the seat. The bore step is inspected for erosion, which is the failure mode specific to this design and which shows as a polished or washed area downstream of the step. Both seat inserts are replaced as a pair, the gasket is renewed, and the body is closed with the studs brought up in a cross pattern.
How to Specify and Order
Six lines fix the valve: size and bore notation, class, body grade, seat type, end connection and operator. On a reduced bore valve the first line has to carry both numbers, and on a replacement it also has to carry the face to face dimension, because the notation alone will not tell a supplier which build the line was designed around.
Three questions belong to the line rather than to the valve: will it be pigged, what pressure drop can the line afford, and is the medium abrasive. The first rules reduced bore out where a pig has to pass, the second decides whether the saving is real, and the third decides whether the throat will survive.
Documents to name in the order: the EN 10204 3.1 certificate for each pressure part with its heat number, the normalising record where A105N is specified, the shell and seat test record with a result per seat, the torque record for the operator fitted, and the general arrangement drawing carrying both the end size and the bore.
FAQ
Q: Does a reduced bore reduce flow resistance?
A: No, it increases it. The bore through the ball is the restriction, so a reduced bore valve has a smaller flow area, a lower capacity and a higher permanent pressure loss than the full bore valve of the same end size. What reduced bore reduces is the ball size, the torque, the envelope and the price.
Q: Can this valve be used for flow control?
A: No. A ball valve part open puts the whole pressure drop across a narrow opening between a ball and a seat, and the seat is cut by the resulting jet. Throttling is a control valve duty, and a reduced bore ball valve offered as a flow control device is a valve being sold outside its function.
Q: What does four by three mean?
A: A four inch end connection and a three inch bore through the ball. The valve is flanged, dimensioned, pressure rated and shell tested as a four inch valve; only the passage is three inch. Ordering it as a three inch valve produces a valve that is short in every dimension and will not bolt to the line.
Q: Why is reduced bore common at Class 2500?
A: Because the ball is the expensive part at that class. A smaller ball means a smaller seat ring, a shorter body, less forging, a lower torque and one size down on the operator, and on a high class valve that chain is worth more than the pressure drop costs in a line that is not swept.
Q: What is the difference between A105 and A105N?
A: A105 is the grade and the N records that the forging was normalised after forging, which refines the grain and improves toughness. An order that says A105N without a heat treatment record has asked for a condition and left the evidence for it to chance, and the difference cannot be seen on the finished valve.


Hot Products


News
Why A Ball Valve Gets Harder To Turn: Five Causes, And The Test That Tells Them Apart
A ball valve that stiffens over months points at one of five parts. Measure torque with the line pressurised and again vented, and the split becomes visible.
Read More
The Ball Valve at Four Thousand Bar: Seat Load, Erosion And Fatigue in Waterjet Circuits
At 4,000 bar a 10 mm bore puts 31 kN on the seat and a 0.1 mm leak cuts steel. What a ball valve must survive in a waterjet or intensifier circuit.
Read More
Large Diameter Ball Valves: Four Limits That Change The Design
Above a certain size a ball valve stops being a scaled one. Ball weight, operator torque, body split and the test bench each set a limit at a different size.
Read More
Cast Or Forged Ball Valve Body, And What A Radiography Acceptance Level Actually Buys You
Casting or forging is only half the decision. What RT, UT, MT and a proof test each find in a ball valve body, and where the geometry defeats all of them.
Read More