

Double block and bleed is an arrangement, not a valve
Double block and bleed is quoted in almost every isolation specification and examined in almost none. It is not a feature a valve either has or lacks. It describes what an arrangement of sealing surfaces and a vent can do: hold pressure on two sides at once, and offer a point between them where that pressure can be released and watched. The word block refers to a seating surface rather than to a valve body, which is why one ball valve with two seats can honestly be sold as DBB, and why two valves in series with a bleed between them are also DBB and are a different thing entirely.
The difference costs money in both directions. A single-valve DBB is compact: one body, one ball, one set of end connections, and on a metering skid or a filter header where the space is already fixed that is usually the only thing that fits. A two-valve arrangement doubles the length, the weight and the price and gives two independent balls. Both descriptions are defensible on a datasheet. Only one of them is what an operator means when he says he wants to work on the equipment behind it.
Two seats around one ball
In a trunnion-mounted ball valve the ball is held on its axis and each seat is a ring that moves axially in its own pocket. With the valve closed, line pressure pushes the upstream seat onto the ball, and the downstream seat is pushed onto the ball from the other side by its spring or by whatever pressure is trapped in the cavity. The space enclosed between the two seats, outside the ball, is the body cavity, and it has a port to the outside world. That port is what makes the arrangement a bleed.
What makes it a double block is not that both seats touch the ball. It is that each seat seals against the direction it is loaded from, so that with the valve closed and the cavity empty, nothing crosses either seat. Two conditions have to hold at the same time, and they are demonstrated separately: each seat holds against the pressure it faces, and the cavity is genuinely at zero.
The bleed is a test, and it is the part that gets skipped
The procedure is short. Close the valve, open the bleed, let the cavity come to zero, close the bleed, and watch. A bleed that keeps running tells you the upstream seat is passing, which means you have one barrier and not two. A bleed that stops but a gauge that creeps back tells you the same thing more slowly. A bleed that stops and stays at zero, on a line that is actually pressurised, is the only evidence that both seats are holding at that moment.
Most DBB claims are lost here rather than in the seat design. If the cavity port is a plug with a cap and no valve, the operator has nothing to bleed and the DBB claim is a drawing note. If the port is a needle valve with no cap, it is a leak path left open by whoever used it last. If the port faces a wall, into a pipe rack, or sits under insulation, it will not be used at all. A bleed point has to be operable by a person standing in front of the valve and it has to discharge somewhere that person is permitted to discharge to. That is a piping decision made at the valve, and it is much cheaper to make it before the valve is ordered than after it is welded in.
Where the claim quietly fails
Four failure modes are worth knowing, because none of them shows on a datasheet.
The first is the shared ball. The two seats are independent; the ball is not. A score, a pit or a piece of weld spatter across the ball surface crosses both seats at once, and a valve that was DBB when it was new becomes a single barrier with two leaking seats. This is the strongest argument for two valves in series wherever the isolation is the point of the installation rather than a convenience.
The second is the self-relieving seat. A seat designed to let excess cavity pressure escape back into the line is doing the right thing for thermal expansion and the wrong thing for isolation, because the escape route it uses is the very seat being counted on as a barrier. If the pressure source is on the side that seat relieves towards, it will pass that pressure into the cavity, and the bleed will show pressure that arrived by a route nobody modelled.
The third is the cavity relief device. Where the body carries a relief valve or a rupture disc on the cavity, that device is a path out of the cavity and it sits between the seats and the gauge. It has to be understood before the bleed is read, and it must not be the only route by which the cavity can be vented.
The fourth is a seat that holds on preload alone. On a line with no differential pressure the upstream seat has nothing pushing it onto the ball except its spring, so a stiff or coil-bound spring produces a seat that holds on a test bench at pressure and passes on a line sitting at zero. The bleed is the only place this shows, which is one more reason to make it operable.
DBB, DIB-1 and DIB-2, and why the third label exists
Once the requirement shifts from a maintenance convenience to isolation that a permit depends on, the question stops being whether the cavity can be bled and becomes whether the seats can be relied on to block from either side. That is what the double isolation and bleed labels describe, and the difference between them is entirely about which seat relieves.
In DIB-1 both seats are double piston. Each seals against pressure from either direction, so neither seat relieves into the line, and the cavity therefore needs a relief device of its own, because trapped liquid will expand and either lift a seat or find the weakest wall. In DIB-2 one seat is double piston and the other is self-relieving, so the valve blocks in both directions and still has a defined path for cavity pressure to escape to one nominated side. Which side is nominated is a decision made against the process, not against the catalogue: the relief side is the side that receives whatever the cavity contains.
The practical consequence is about paperwork. A DBB valve with self-relieving seats is a good maintenance tool and a poor positive isolation device, because a self-relieving seat is a one-way door out of the cavity and the door faces upstream. A specification that writes double block and bleed while meaning positive isolation has asked for the wrong thing, and it will be supplied the wrong thing, correctly and with a certificate.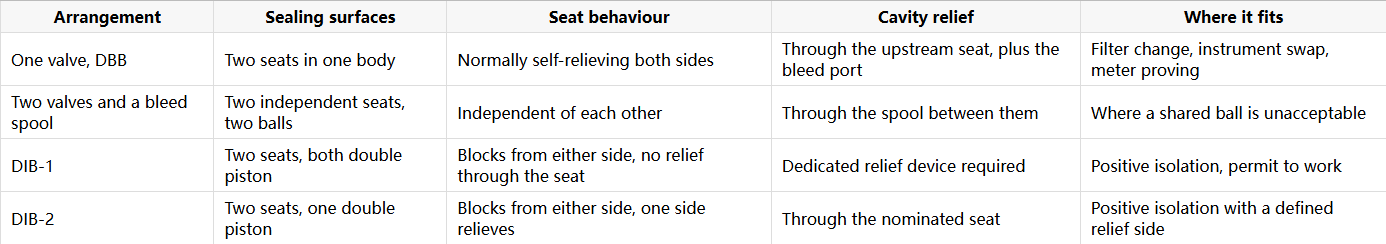
Where each one belongs
A single-valve DBB belongs where the isolation is short, the medium is clean and the operator is standing there: a filter change, an instrument swap, a proving run, a sample point. Two valves with a bleed belong where the ball itself is the risk, in dirty service or on a line that has been pigged, and where the space and the budget allow it. DIB belongs where a permit depends on the barrier, where the line cannot be drained down, and where the consequence of a seat passing is not a spill but an event.
The common error runs the other way. A project specifies DBB for every isolation point because it is a familiar phrase, pays for a cavity port and a bleed valve on every unit, and never uses either, while the two or three places that genuinely need DIB are supplied with the same valve as everything else.
Sealant injection is not a bleed port
Both are small threaded ports in the body and in the field they are confused constantly. A seat sealant port exists to push viscous sealant into the seat-to-ball interface and restore a leaking seat well enough to keep a line running until the next shutdown. It is a repair path, not a pressure path. Using it as the cavity bleed is worse than useless for two reasons: a plugged sealant port holds pressure with no way to see it, and injecting sealant into a leaking seat hides precisely the evidence that the bleed exists to produce. A valve supplied with sealant fittings should have those fittings identified on the drawing, and the DBB bleed should be a separate port with its own valve.
The test that proves the seats but not the arrangement
The standard hydrostatic test is a seat test. Shell at 1.5 times and seat at 1.1 times rated pressure, with the seat test run in both directions, proves that each seat holds against the pressure it is asked to hold. It says nothing about whether the cavity can be brought to zero, whether the bleed valve is operable, or which way the seats relieve. The DBB function needs its own demonstration and it is a functional one: close the valve, pressurise one side, bleed the cavity to zero, confirm it stays at zero, then repeat from the other side. That sequence takes minutes in the shop and is worth asking for in writing, because it is the only evidence that the arrangement works as an arrangement.
What to write into the purchase order
Five lines carry it: whether the requirement is DBB, DIB-1 or DIB-2, stated by name rather than by description; the seat behaviour, self-relieving or double piston, and on which side relief is nominated; the cavity port, meaning its size, its valve type, whether it is capped and where it discharges; whether sealant injection fittings are fitted and, if they are, that they are separate from the bleed; and the functional test sequence at the factory, witnessed or documented.
J-VALVES builds DBB ball valves from 1/2 to 56 inch (DN15 to DN1400) in ASME Class 150 to 2500, in floating and trunnion-mounted patterns, with the body cavity ported and fitted with a bleed valve, self-relieving or double piston seats to the isolation duty specified, and shell testing at 1.5 times and seat testing at 1.1 times rated pressure in both directions. Fire-safe construction to API 607, NACE MR0175 materials and EN 10204 3.1 certificates are available on the same order.
Frequently Asked Questions
Is a single ball valve with two seats really double block and bleed? Yes, provided each seat seals against the pressure it faces and the cavity between them can be brought to zero and stay there. The two blocks are the two seats and the bleed is the cavity port. What a single valve cannot offer is two independent balls, so a defect across the ball defeats both seats at once.
What is the difference between DBB and DIB? DBB is about venting the cavity; DIB is about blocking from both directions. A DBB valve normally has self-relieving seats, which let cavity pressure escape upstream, which is useful for thermal expansion and is the reason a DBB valve is not a positive isolation device. DIB-1 uses two double-piston seats and needs a dedicated cavity relief; DIB-2 keeps one self-relieving seat so the cavity still has a defined relief side.
Can the seat sealant port be used to bleed the cavity? No. The sealant port is a repair path into the seat interface, not a vent from the cavity. Using it as a bleed hides the evidence a bleed is meant to give, and a plugged sealant port holds pressure where nobody can see it. The cavity bleed should be its own port with its own valve.


