


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q41F
-
J-VALVES
Overview of the J-VALVES DIN DN100 PN16 Two-Piece Floating Ball Valve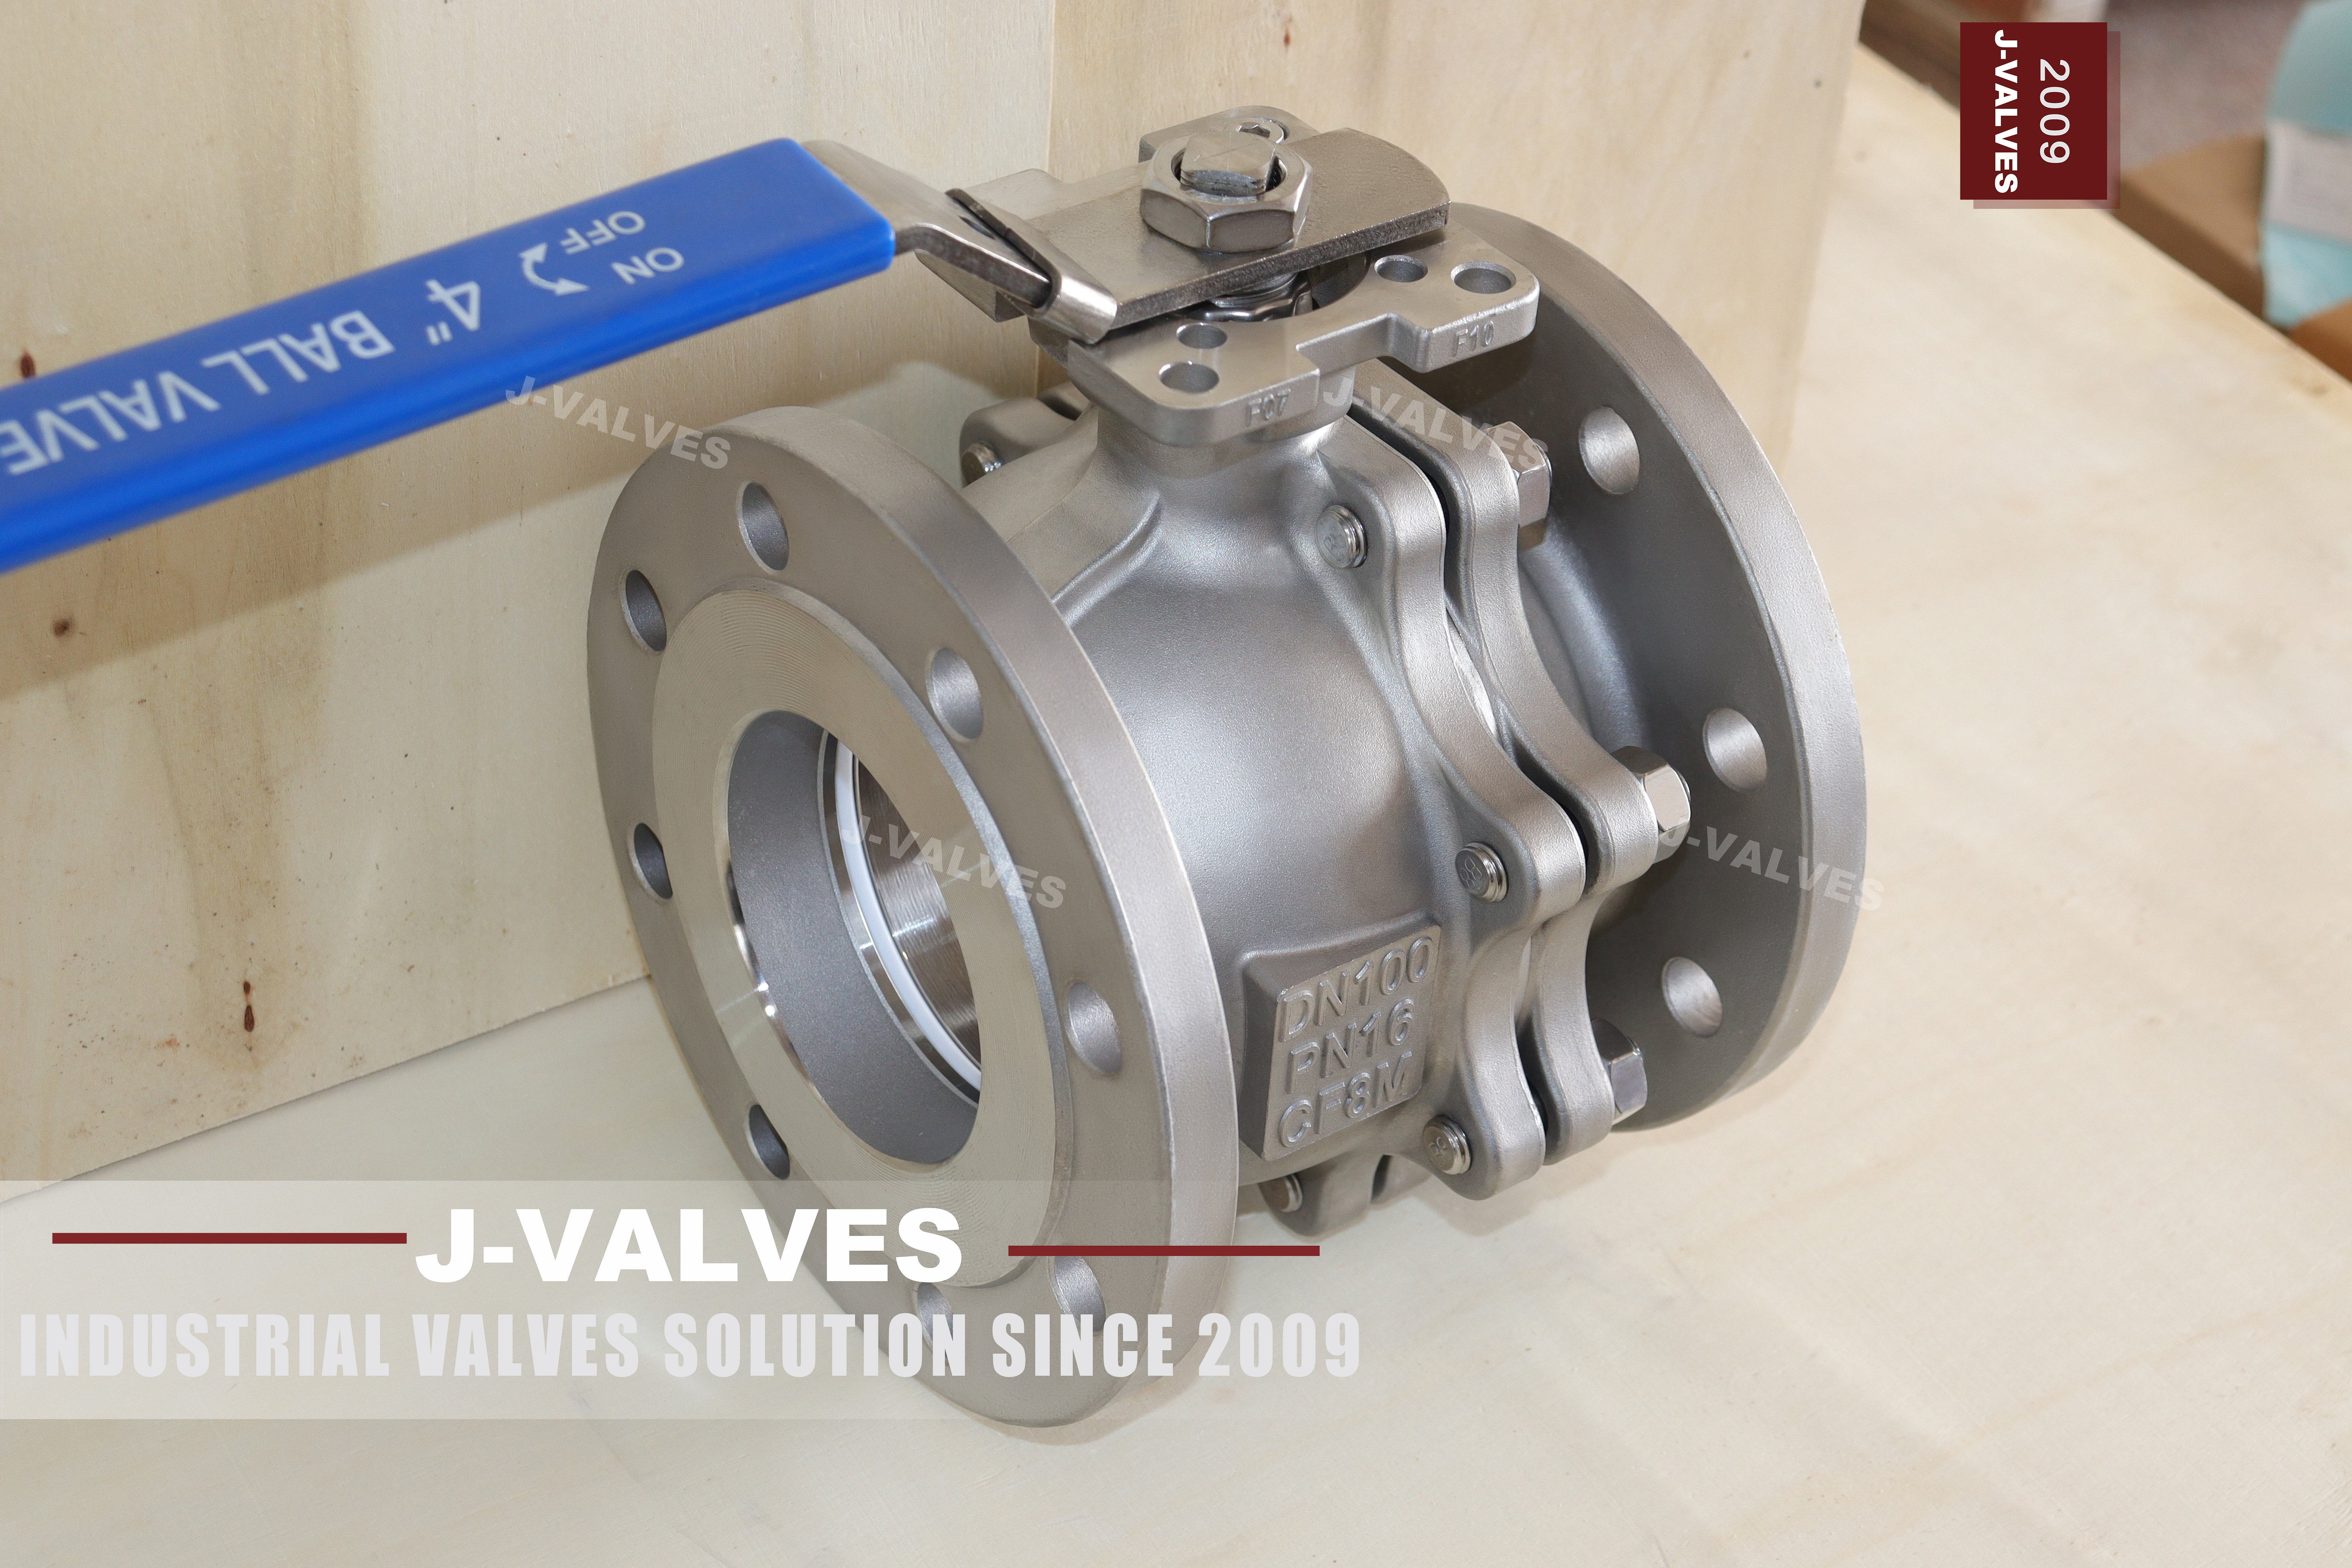
The J-VALVES DIN DN100 two-piece floating ball valve is a PN16 isolation valve built for EN pipework: a DN100 bore, EN 1092-1 Type 11 Form B1 raised-face flanges at both ends, and a body made from two castings, a main body and one bolted end cap. The ball is not carried on trunnions. It sits loose between two seat rings, and line pressure pushes it onto the downstream seat, which is where the seal is made. Full port means the waterway equals the nominal size, not the pipe: Schedule 40 pipe at NPS 4 runs about 102 mm internally.
Two pieces is the compromise this size normally wants. A one-piece body has no joint to leak but cannot be opened at all, and a three-piece adds a second joint, a second gasket and a second bolt circle in exchange for lifting the centre section out. At DN100 the two-piece keeps one body joint and one gasket and still lets the ball, both seats and the stem be renewed. What it does not give is a valve that opens without moving pipe, and section 9 says why.
Most of these valves go into plant utilities rather than process licensable duty: chilled and condenser water, compressed air, dosing and CIP skids, filter stations. The buyer there is matching a DN100 gap in metric pipework and wants PN16 with a flange that bolts to the one already welded on.
Design and Construction
The split is at one end only. The main body carries the stem bore and the upstream seat pocket in one casting; the end cap carries the downstream seat and closes the joint. Both are machined from the same heat of castings, so the joint faces and the bore are turned from one datum and the ball does not have to find its centre across two unrelated parts. Between them sits a gasket, the only soft element in the pressure boundary apart from the packing.
The ball is free. Pressure on the upstream side acts on the whole projected area and slides the ball until it seats on the downstream ring, so sealing improves as pressure rises. That load path is why the design needs no trunnion, no bearing blocks and no springs strong enough to hold the ball in place. It is also why the cavity is self-relieving: if trapped liquid expands, the ball is pushed off the upstream seat and the overpressure escapes back into the line. No relief device is fitted.
Two things follow that catalogue pages get wrong. There are no piston-effect seat rings here, single or double, and no seat injection ports, because neither has a function when the seat is unloaded by the ball moving away. What the valve does carry is an anti-blowout stem inserted from inside the cavity, a spring path from stem to ball to body for static, and a fire-safe arrangement so joint and seat still close on metal if the soft parts burn.

Material Options
CF8 and CF8M are the two standard bodies, and the choice is about the water, not the pressure. CF8, the 304 grade, is enough for potable water, closed chilled water, compressed air and most neutral duty. CF8M adds molybdenum, which is what buys resistance to pitting and crevice attack in chloride-bearing water, brackish cooling water and chemical dilution lines. Neither grade raises the pressure rating, and paying for 316 does not buy a higher class.
The seat is where the specification work sits, because the body is rated far above what any soft seat will take. PTFE and RPTFE cover the ordinary range to 200 C, PPL reaches 280 C and PEEK 260 C, and above that the valve needs a Stellite-faced metal seat, which changes both leakage class and price. Packing matters as much: PTFE V-rings for clean cold duty, flexible graphite where the line runs hot or the site has an emission limit.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Body | ASTM A351 CF8 | ASTM A351 CF8M, CF3M | CF8M for chlorides and brackish cooling water |
| End cap | CF8 or CF8M, same heat as body | CF3M | Paired and machined with the body it closes against |
| Ball | ASTM A351 CF8 or CF8M, mirror lapped | Hard chrome, Stellite overlay | Lapped against its own seat, not against a master |
| Stem | ASTM A182 F316 | 17-4PH, UNS S17400 | F316 standard; 17-4PH where more strength is wanted |
| Seat | PTFE | RPTFE, PPL, PEEK, Stellite-faced metal | The seat sets the temperature, not the body |
| Body gasket | PTFE flat gasket | Spiral wound, graphite filled | Graphite is what holds the joint in a fire |
| Packing | PTFE V-ring set | Flexible graphite, live loaded | Graphite for hot lines or tight emission limits |
| Anti-static | Spring from stem to ball to body | Not optional | Continuous path, checked on every valve |
| Operator | Worm gear at DN100 | Lever, pneumatic, electric, hydraulic | Mounting pad to ISO 5211 |
Technical Specifications
The table below is the specification as quoted; everything in it comes from the data sheet or a named standard, and nothing is interpolated. Face-to-face is given as a standard reference rather than a number, because the number belongs to the signed drawing for this size and bore, and a figure lifted from another maker's catalogue is how wrong spool pieces get made.
| Item | Value |
|---|---|
| Nominal size | DN100, NPS 4 |
| Pressure rating | PN16 |
| End connection | EN 1092-1 Type 11, Form B1 raised face, both ends |
| Bore | Full bore, nominal size waterway |
| Body style | Two-piece, one bolted end cap |
| Body material | ASTM A351 CF8 or CF8M |
| Seat | PTFE, RPTFE, PPL, PEEK or Stellite-faced metal |
| Temperature, body | -29 to +425 C, per the J-VALVES ball valve table |
| Temperature, valve | Set by the seat, the lower of body and seat |
| Design | DIN 3357, EN 12516-1 |
| Face to face | EN 558, confirmed on the signed GA drawing |
| Pressure test | EN 12266-1, shell 1.5 times PN, seat 1.1 times PN |
| Seat leakage | EN 12266-1 rate A |
| Fire safe | API 607, ISO 10497 |
| Marking | EN 19 |
| Series range | 1/2 to 56 inch, Class 150 to 2500, -29 to +425 C |
The temperature line is the one buyers misread. Minus 29 to plus 425 C is the body figure carried across the J-VALVES range, and it is a shell limit, not a promise about the seat. The valve as sold is limited by whichever is lower, and at DN100 with a PTFE seat that is the seat by a wide margin.
Standards and Compliance
Start with the flange, because PN16 at DN100 is where European and American pipework quietly fail to meet. EN 1092-1 does have a PN16 step, and at DN100 it is drawn as a 220 mm outside diameter, a 180 mm bolt circle and eight 18 mm holes for M16 bolts, with a 158 mm raised face. ASME B16.5 Class 150 at NPS 4 is 228.6 mm outside diameter, 190.5 mm bolt circle, eight 19 mm holes for 5/8 inch bolts and a 157.2 mm raised face. Both are eight-bolt DN100 flanges, and neither will pass a bolt through the other.
The trap is the label. API 6D clause 7.2 records Class 150 as PN20, not PN16, so a PN16 valve has no Class number on the ANSI side; the nearest is 150 and it does not fit. What PN16 does share is the PN10 drilling: at DN100 both are the same 220 mm, 180 mm, eight-hole pattern, so a PN16 valve bolts onto a PN10 flange with the same bolts. That is useful on a retrofit, and it is not the same statement as PN16 equals Class 150.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Flange drilling | EN 1092-1 | Type 11 Form B1, DN100 PN16, eight M16 on a 180 mm circle |
| Face to face | EN 558 | Series stated on the drawing; DIN 3202 no longer applies |
| Shell design | EN 12516-1 | Wall section checked by the tabulated method |
| Pressure test | EN 12266-1 | Shell and seat on every valve, record kept by serial number |
| Fire type test | API 607, ISO 10497 | Certificate issued per size and per rating |
| Marking | EN 19 | Size, rating, body material, heat number, flow arrow |
| Material certificates | EN 10204 3.1 | Casting and bar stock, issued with the delivery |
Face-to-face follows EN 558. Old drawings still say DIN 3202, and that number should be read as a historical label: DIN 3202-1 was withdrawn and replaced by EN 558, whose part 1 lists face-to-face dimensions for PN-designated valves and carries a table for plug and ball valves specifically. When replacing a valve, ask for the series as well as the size, because changing series moves the flange faces.
The pressure and temperature rating needs one more sentence. PN16 is an ambient rating. EN 1092-1 rates austenitic stainless on a material group of its own, and the allowable pressure falls as temperature rises, so the plate is not the working pressure at 200 C. On a soft-seated valve this rarely bites, because the seat reaches its limit first, but a metal-seated version should be checked at the design temperature.
Pressure testing is to EN 12266-1: shell at 1.5 times the rated pressure, seat at 1.1 times, every valve tested rather than sampled, and the certificate carries the serial number. Seat tightness is offered at rate A, no visible leakage, the class a soft-seated ball valve should be held to and one a metal-seated version cannot promise.
Manufacturing Process
Bodies start as investment castings in CF8 or CF8M, solution annealed and pickled, and each heat is checked for chemistry before it reaches a machine. Machining runs in two operations with the ball cavity, both flange faces and the stem bore referenced to each other; the cap's joint face is machined as a pair with the body face it closes against, which decides whether the gasket is squeezed evenly.
The ball is turned, ground and lapped against its own seat ring rather than a master, and the pair stays together through assembly and packing. Assembly is done in a clean bay: seats and gasket dry, stem inserted from inside the cavity so the shoulder sits behind the body, packing set to a measured gland load, then cap bolts brought up in a cross pattern in stages. Marking follows the pressure test.

Quality Control and Testing
Eight checks stand between the casting and the crate. The first three cover what cannot be corrected later: casting soundness and chemistry, joint face flatness, ball roundness and finish. The next three cover assembly: seat squeeze, gland load, dry operating torque. The last two are the pressure tests and the marks.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| 1 | Casting chemistry and soundness | Heat analysis to A351; penetrant check on the joint faces |
| 2 | Joint face flatness and finish | Checked on a surface plate before the cap is paired to the body |
| 3 | Ball roundness and lapped surface | Measured against the seat it will run in; finish by comparator |
| 4 | Seat squeeze and gland load | Set from the drawing, recorded per valve |
| 5 | Dry operating torque | Stem turned dry, logged against the drawing figure |
| 6 | Shell test | EN 12266-1, 1.5 times rated pressure, no leak or distortion |
| 7 | Seat test | EN 12266-1, 1.1 times rated pressure, rate A acceptance |
| 8 | Anti-static path and marking | Continuity checked stem to body, then EN 19 marks and serial |

Applications and Industry Service
The natural home is utility water: chilled water and condenser water in plant rooms, firewater only where the authority accepts a soft-seated isolation valve, and potable water in CF8. In these lines the valve cycles a few times a season, the medium is clean, and what matters is a flange that matches and a seat that does not weep after a year of standing pressure.
Chemical and process duty is the second group, and there the grade and seat do the work: CF8M for chloride-bearing solutions, PPL or PEEK where the line runs above the PTFE band, and graphite packing where the emission limit is tight. Food, beverage and CIP lines are the third, on the same CF8M body with a polished ball and a PTFE seat, provided the cleaning cycle stays inside the seat's temperature.
Where this valve should not be used is worth stating plainly. A floating ball cannot give the double block and bleed function trunnion valves are bought for, because the pressure that seals the downstream seat unloads the upstream one, so there are not two independent barriers to prove. If the line cannot be opened, use a three-piece or top-entry body. If the pipe is Class-rated, the flanges will not mate and the ANSI equivalent is the correct order.
Installation, Operation and Maintenance
Mount it with the end cap downstream. The valve seals both ways, which is not the same as being indifferent to orientation: the cap side carries the joint and the downstream seat, and putting that joint on the high-pressure side of a closed valve, where it sees full line pressure rather than cavity pressure, is a choice nobody needs to make. The flow arrow states the convention.
Bolting and gasket are where most of these joints are lost. Use the gasket made for the Form B1 raised face rather than a full-face sheet cut to the flange outside diameter, bring the bolts up in a cross pattern in at least three passes, and check the faces are parallel before the last pass. On a hot line, re-torque after the first cycle and again after the first week; a PTFE gasket that has taken a set will not recover.
Operation is quarter turn and nothing else. The valve is an isolation device: throttling on a soft seat erodes the seat edge and the ball's sealing band, and a part-open ball valve in a dirty line is a valve that will not seal when it is finally closed. On a line that stands idle for months, cycle it a few times a year so the seat does not take a permanent set against one spot on the ball.
How to Specify and Order
Six lines are enough to get a correct quotation. State DN100 and PN16, then state the flange standard and facing explicitly, because the size and rating alone will be read as EN 1092-1 Form B1 by one supplier and as something else by the next. Name the body grade, the seat compound with the design temperature, the operator with the ISO 5211 pad, and the documents wanted: certificates, test record and signed GA drawing.
Two of those lines carry most of the risk. The seat compound is a temperature decision, not a price decision, and asking for PTFE on a line above 200 C is how a valve gets ordered twice. The flange standard is a dimension decision: if the mating flange is Class 150 rather than PN16, the right answer is a different valve, not an adapter plate, because the bolt circles differ and the raised faces do not match either.
FAQ
Q: Is PN16 the same as Class 150?
A: At the valve, no, and at the flange also no. API 6D clause 7.2 records Class 150 as PN20, so a PN16 valve has no Class number on the ANSI side; the nearest class is 150. The drillings differ at DN100: EN 1092-1 PN16 is a 220 mm outside diameter, a 180 mm bolt circle and eight 18 mm holes for M16 bolts, against ASME B16.5 Class 150 at 228.6 mm, 190.5 mm and eight 19 mm holes for 5/8 inch bolts, with raised faces of 158 mm and 157.2 mm. Neither flange will pass a bolt through the other. What PN16 does share is the PN10 drilling at this size, so the valve bolts straight onto a PN10 flange with the same bolts.
Q: Can the body be opened without taking the valve off the line?
A: No, and the distinction matters. The ball and both seats come out through the end cap, but the cap only clears the pipe once the valve has room to move along the pipe axis, so the line has to be opened or the valve lifted out. A three-piece body avoids that by leaving both end caps bolted to the pipe and lifting only the centre section, which is the design to order when the line cannot be broken. Even then the body joint is pressure boundary, so the valve must be isolated, drained and the cavity vented before the bolts come out.
Q: How high can the temperature go?
A: The body is stated to 425 C across the J-VALVES ball valve range, but that is a shell figure and not the working limit of this valve. The seat governs: PTFE and RPTFE to 200 C, PPL to 280 C, PEEK to 260 C, and a Stellite-faced metal seat above that, with a lower leakage class. Order by the seat compound that suits the medium temperature, and read 425 C as the point where a different body material and a metal seat are both required.
Q: Does a full bore DN100 mean the bore matches the pipe?
A: No. Full bore means the waterway equals the nominal size, so a DN100 valve has a 100 mm bore; it does not mean the bore matches the pipe. Schedule 40 pipe at NPS 4 has an internal diameter of about 102 mm, so the valve is slightly smaller than the pipe, which is normal and does not make it a reduced bore design. If the line is pigged, size the pig against the 100 mm waterway rather than the pipe, because the valve is the tightest point in the run.


Hot Products


News
Ball Valves in A Kraft Pulp Mill: Black Liquor, Green Liquor And The Cost of Choosing The Alloy by Habit
White liquor at pH 14 cracks carbon steel welds, black liquor sets solid below 100 C, green liquor dregs grind seats: alloy choice and torque in a kraft mill.
Read More
Slug Flow And Ball Valves: What Actually Arrives At The Seat
A slug is liquid mass with momentum, not a pressure spike. What changes at the seat, in the cavity and at the actuator when liquid reaches a ball valve.
Read More
Ball Valves in Direct Lithium Extraction: PH 1 Eluate, Gypsum Scale And 438,000 Cycles in Twenty-Five Years
Direct lithium extraction swings valves from pH 1 eluate to pH 12 caustic, 48 column switches a day and gypsum scale. Materials, seats and torque.
Read More
Ball Valves in Geothermal Brine: Silica Scale, Chloride Cracking And The Cooling Trap
Why geothermal brine destroys ball valves: retrograde silica scale, calcite at the flash point, chloride cracking above 60 C and the 250 C seat limit.
Read More