


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us

-
J-VALVES-Q347F
-
J-VALVES
Overview of the J-VALVES 2500LB F316 F304 Three Piece Trunnion Ball Valve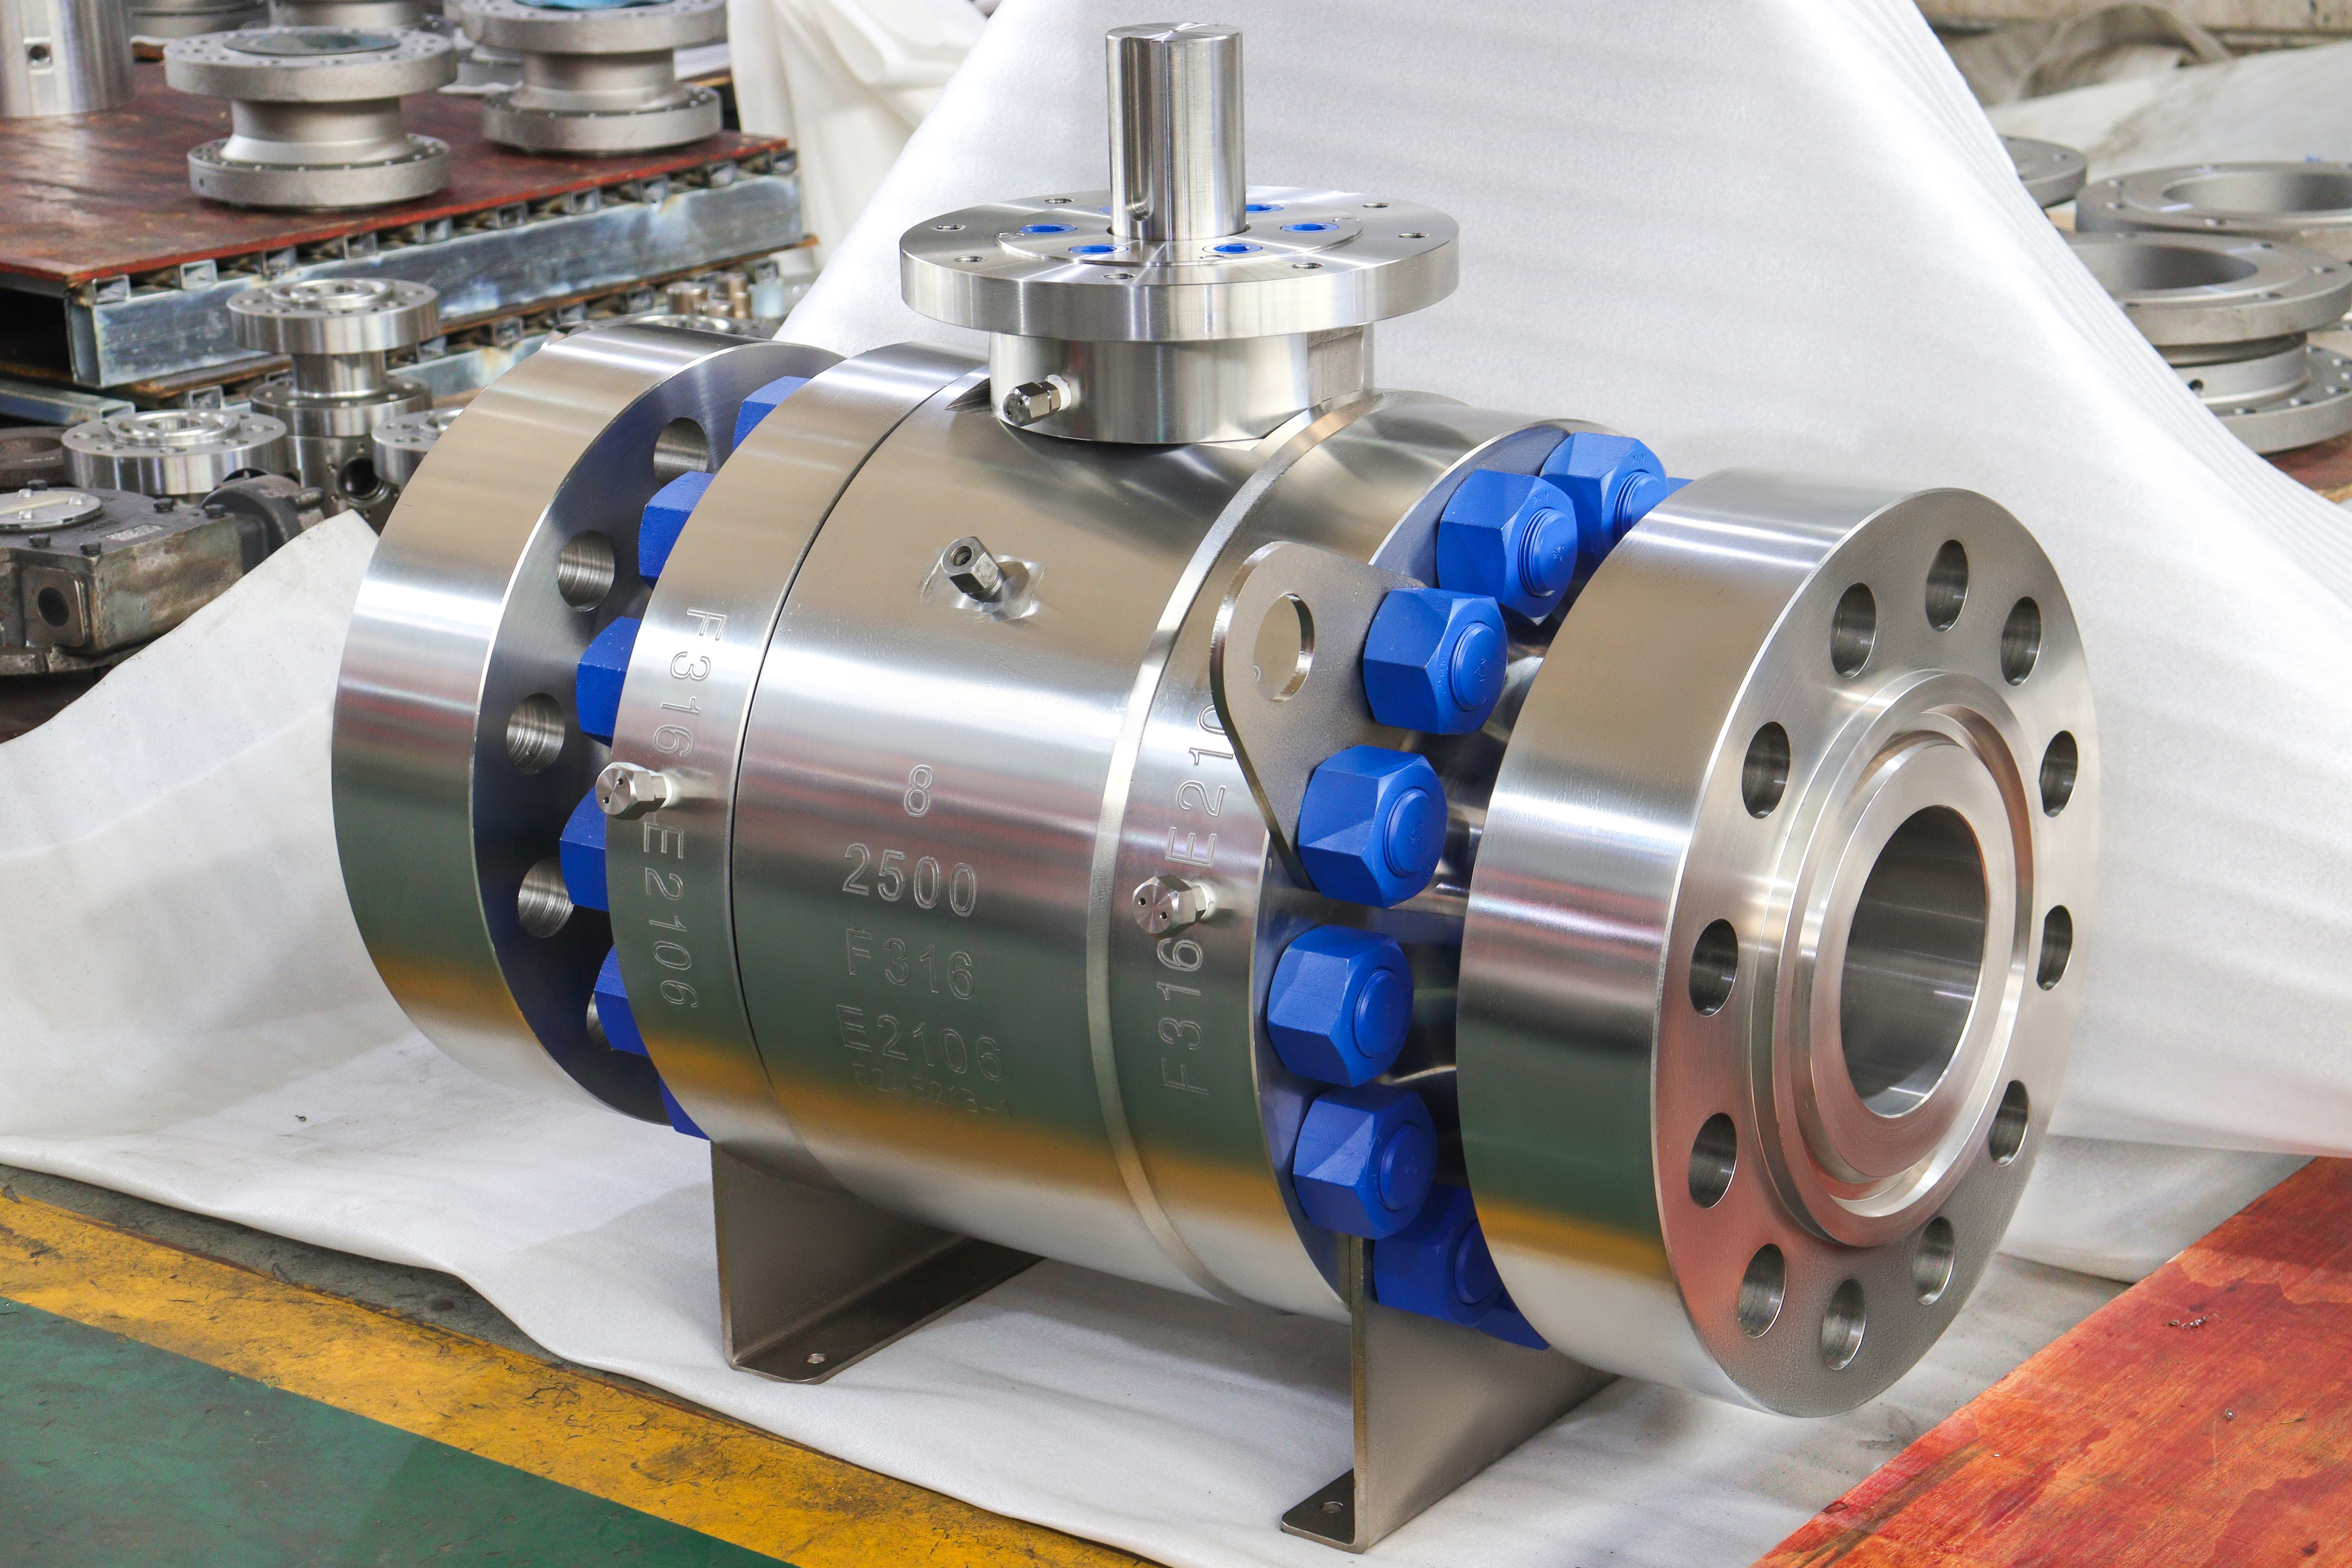
This page prints the ball surface and the seat facing as two separate lists, and a buyer who reads them as two menus will order a pair that does not work together. At class 2500 the seat is metal. There is no soft insert to absorb a mismatch, so the seal forms where two surfaces touch, and those two surfaces are one decision rather than two. A soft nickel deposit running against a hardfaced seat wears through; two surfaces of the same hard material can pick up on each other instead of sliding.
The valve around that contact is a three piece forged body in an austenitic stainless grade, with the ball carried on an upper and a lower trunnion, ring joint flanges, and a bolted joint at each side of the centre section. The published range runs from two inch to twenty four inch and the body is offered in several grades of the same family, from the general purpose 304 through 316 and the low carbon variants to the super austenitic grades. Two grades in the title, one body on the drawing.
So the page has one job. It takes the two lists that the specification block prints apart and treats them as one pair that has to be chosen together, against the medium, and confirmed on the same drawing that carries the seat pocket. Everything else here, the class, the flange, the body code and the test, is written the way the standards write it, and no figure on the page came out of a calculation.
Design and Construction
The body is three pieces: a centre section that carries the stem and both seats, and an end cap bolted to each side. It is a side entry layout, so the trim goes in from the side rather than down through the top, and the centre section is what comes out when the valve is opened for a repair. That makes two body joints rather than one, and each joint is a pressure boundary with its own gasket, its own stud set and its own place in the shell test, which is what the three piece layout buys and what it charges.
The ball is carried at top and bottom rather than resting on a seat. On the smaller sizes of this series the trunnions are housed in the primary body; from six inch upward they run in two bearing blocks, because a ball of that diameter has to be machined, carried and replaced as one part. The trunnions take the side load that line pressure puts on the ball, so the stem turns the ball instead of holding it against the flow, and the seats only have to seal.
Each seat ring is a separate assembly with its own spring set, and one can be changed without touching the other. The rings are set up as single piston effect or double piston effect, and that choice decides whether the cavity relieves to the line by itself or has to be vented through a fitting, which is a maintenance decision as much as a sealing one. The space between the two rings is the body cavity, and the drain, the vent and any injection fitting all connect to it rather than to the bore.

Material Options
The body is forged austenitic stainless, offered as F316 or F304 and at the top of the range in the stabilised and super austenitic grades. The plate carries one code, and that code is what the certificate is written against. Where the medium needs a family the plate does not name, the answer is an inspection certificate at the grade the order asks for, not a longer product name. The ball is the same family as the body, and the trunnion and stem are a precipitation hardening grade because they carry load rather than resist corrosion.
The ball surface is offered four ways: an electroless nickel plating, abbreviated ENP, hard chrome, tungsten carbide, and a cobalt alloy overlay. They are not four prices for the same thing. The nickel plating is the smoothest and the softest and is what a clean, non abrasive medium wants. Hard chrome sits above it. Tungsten carbide is the one that holds up where particles are present. The cobalt alloy overlay is a welded layer, thick enough to be re-machined, and it is the one to ask for when the ball may be refurbished rather than replaced.
The seat facing is offered as PEEK, as metal with a graphite seal, and as tungsten carbide on a nickel alloy. Here the two lists meet. A PEEK seat against a tungsten carbide ball is a soft face running on a hard one, which is a workable pair. A metal seat with a graphite seal is a different pair again, and it is the only one that reaches the top of the published temperature range. What cannot be done is to pick the hardest ball and the hardest seat independently, because two surfaces of the same hardness at this contact pressure do not slide, they fret.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Body | forged austenitic stainless, F316 or F304 | stabilised or super austenitic grades | code on the plate |
| Body joints | two bolted joints, one each side | ring joint or spiral wound gasket | new gasket at every break |
| Ball | F316 or F304 | same family as the body | carried on upper and lower trunnions |
| Ball surface | electroless nickel plating | hard chrome, tungsten carbide, cobalt alloy overlay | chosen with the seat facing |
| Trunnion | surface hardened F316 or 17-4PH | bearing blocks from six inch up | takes the side load |
| Stem | 17-4PH with an anti blowout shoulder | nickel alloy for the highest ratings | gland sits above the shoulder |
| Seat facing | PEEK | metal with graphite, or tungsten carbide on a nickel alloy | sets the temperature ceiling |
| Seat setting | single piston effect | double piston effect, DPE | decides how the cavity relieves |
| Packing | graphite with wire reinforcement | low emission arrangement | ISO 15848 on request |
| Bolting | B8M studs and 8M nuts | B7 studs and 2H nuts | pair the nut to the stud |
Technical Specifications
Class 2500 is written as PN 420 in the API 6D pressure code list, and the two designations describe the same rating. The published size range is two inch to twenty four inch, which is a statement about what the works can make rather than about the valve on this page. Twenty four inch is also the last size inside ASME B16.5, so the range stops where the flange standard stops, and above it the flange moves to ASME B16.47 and the series has to be chosen.
The flange is a ring joint, and the groove is cut in the flange face rather than added at site. That makes the facing a property of the valve, not an accessory: a raised face and a ring joint are two different valves with two different overall lengths, and the length is the one in ASME B16.10 for the size and class ordered. The ring itself is a consumable and is ordered with the valve, in the profile and the material the medium allows.
The temperature range is minus 29 to plus 425 Celsius, measured as metal temperature rather than as medium temperature. The top of that range is not reached by every seat facing on the list, and the bottom of it is not reached by every packing. This is the second reason the ball and the seat belong in one decision: the pair sets the ceiling, and a valve ordered at the body rating and fitted with the wrong facing is a valve with a narrower range than its nameplate suggests.
| Item | Value |
|---|---|
| Nominal size | two inch to twenty four inch (DN50 to DN600), the size named on the order |
| Pressure class | class 2500, written as PN 420 in the API 6D code list |
| Body style | three piece side entry, two bolted body joints |
| Ball support | trunnion mounted, upper and lower |
| Bore | full bore or reduced bore to API 6D table 1 |
| Body material | forged austenitic stainless, F316 or F304, code as stamped |
| Ball material | F316 or F304 |
| Ball surface | electroless nickel plating, hard chrome, tungsten carbide or a cobalt alloy overlay |
| Seat facing | PEEK, metal with graphite, or tungsten carbide on a nickel alloy |
| Seat pairing | ball surface and seat facing chosen as one pair, confirmed on the drawing |
| Seat setting | single or double piston effect, DPE, chosen on the order |
| Trunnion material | surface hardened F316 or 17-4PH |
| Stem material | 17-4PH with an anti blowout shoulder |
| Packing | graphite with wire reinforcement |
| Body gasket | ring joint, octagonal or oval |
| Bolting | B8M studs with 8M nuts, or B7 studs with 2H nuts |
| End connection | ring joint flange to ASME B16.5, weld ends to ASME B16.25 on request |
| Face to face | ASME B16.10 for the size and class ordered |
| Design standard | API 6D, with ASME B16.34 and API 608 underneath |
| Test standard | API 598 or API 6D |
| Shell test | one and a half times the rating |
| Seat test | one and a tenth times the rating, both directions |
| Temperature range | minus 29 to plus 425 Celsius, metal temperature |
| Temperature ceiling | set by the seat facing and the packing, not by the body |
| Operation | gear operator as standard at this class |
| Anti blowout | stem retained by the body cover |
| Fire safe | API 607, API 6FA or ISO 10497, named on the order |
| Fugitive emissions | ISO 15848 tested arrangement on request |
Standards and Compliance
The three documents in the block do different jobs, and it matters which one is allowed to speak. One sets what has to be on the plate and in the file; one sets the wall and the rating curve against temperature; the third covers the same ground from the position of a general steel valve rather than a pipeline one. Where two of them answer differently, the order has to name a winner, or the file will carry two true statements that cannot both be applied to the same valve.
Fire safe is proved by a type test on one valve, not by a test on every valve, and the three procedures in circulation answer different questions: a report to one is not a report to another, and a page listing all three should say which was run and on what size, because a report that covers a size range was still run on a single valve. Low emission is separate again and is measured on the stem. None of it describes seat tightness in normal service.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Pipeline valve | API 6D | design, marking and test |
| Pressure boundary | ASME B16.34 | rating and minimum wall |
| General ball valve | API 608 | overlapping requirements |
| Flange | ASME B16.5 | ring joint, up to twenty four inch |
| Face to face | ASME B16.10 | value stated in the size table |
| Weld ends on request | ASME B16.25 | butt weld preparation |
| Testing | API 598 or API 6D | 1.5 times shell, 1.1 times seat |
| Fire test | API 607, 6FA or ISO 10497 | named, and not interchangeable |
| Fugitive emissions | ISO 15848 | separate claim and separate test |
Manufacturing Process
The body is forged, cleaned and then machined from the flange faces inward, so that the bore, the seat pockets and the trunnion bores are all cut from the same reference. The seat pocket is finished after the face it sits against, because a pocket cut from a rough face is square to nothing, and a seat ring that is not square to its pocket loads on one edge. On the sizes with bearing blocks the two trunnion bores also have to be coaxial, since any offset shows up as a ball that is stiff to turn.
Assembly is where the pair becomes physical. The ball goes into the centre section, the two seat rings follow, and the trunnions are set before either joint is closed, so that the ball sits where the seats were cut to meet it. Each joint then goes down on a new gasket with the studs taken up in a cross pattern, and the valve is re-tested with both joints in place. Opening either joint later means another gasket and another test, which is the recurring price of a three piece body.

Quality Control and Testing
The certificate is written against the heat number stamped on the plate, and a material identification report is issued against the same heat when the order asks for one. It matters more here than on a carbon steel valve, because two austenitic grades can leave the works looking identical after passivation, and the plate code is the only thing at goods in that says which one arrived. The certificate follows the plate; it does not replace the check against it.
The shell test runs at one and a half times the rating with both body joints assembled, so it tests the wall and both joints in one pass. The seat test follows at one and one tenth times, in both directions, with the cavity monitored. On a metal seat the acceptance is a permitted rate rather than no visible leakage, and the rate is written on the record. A metal seat that is asked to hold zero is a seat that will be rejected at the bench for behaving exactly as a metal seat behaves.
Because the seat is a contact between two surfaces, the test record should name the pair that was run: the ball surface and the seat facing, as ordered. That line is what makes a later claim possible, because a seat that passes on delivery and fails after a year can only be argued about if the two surfaces in the valve are the two that were tested. An order should ask for the pair on the certificate rather than only the body grade and the class.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| Forging | heat number and certificate | read against the plate code |
| Material identity | report against the same heat | quoted when the order asks |
| Seat pocket | square to the joint face | cut after the face is finished |
| Trunnion bores | coaxial with the bore | set in the machining sequence |
| Shell test | wall and both joints at 1.5 times | run with the joints assembled |
| Seat test | both directions, cavity monitored | acceptance by rate, not zero |
| Pair record | ball surface and seat facing named | as ordered, on the record |
| Marking | plate, certificate and drawing | size, class, code, heat |

Applications and Industry Service
A metal seated valve at this class belongs where the medium is clean enough for two surfaces to keep their finish, the pressure is high enough that a soft seat would extrude, and the valve is cycled a few times a year rather than a few times an hour. High pressure injection lines, letdown stations, isolation on a corrosive duty and the outlet of a high pressure separator are the usual places. In those duties the ball surface is chosen for wear rather than for tightness, and the seat facing for temperature.
It is the wrong valve where the medium carries solids that would be trapped between the two faces, because a metal seat has no resilience to swallow a particle and the pair will be damaged rather than just marked. It is also the wrong choice where the duty needs a bubble tight seat at ambient temperature, since that is what a soft seat is for, and where the line has to be pigged, because a three piece body of this class is not built to pass a tool through its cavity.

Installation, Operation and Maintenance
The seat rings come out with the middle section, and that is what decides how a repair is planned: the line is isolated, the body drained and the cavity vented, both joints are released, and the centre section leaves with the ball and both seats in it. A seat change is therefore also the moment to look at the ball, because a new facing run against a worn ball surface is a pair that was never matched. Changing one without the other is how a valve ends up back in the workshop inside a year.
The injection fittings are the exception that buys time rather than life. They push sealant to a seat ring that is passing, which holds a line until the next planned stop, and they do not restore a damaged facing. The drain plug does the opposite job: it empties and samples the cavity, and what comes out tells you which seat is passing before the line is opened. Both are maintenance aids, and neither of them is a substitute for renewing the pair.
How to Specify and Order
The order needs the size, the class written once as class 2500 or PN 420, the flange as ASME B16.5 ring joint, the bore, the body code, the ball surface, the seat facing, the packing, the operator, the test standard and the certificate grade. Of those lines, the ball surface and the seat facing are the two that have to be written next to each other, because they are chosen as a pair and a quotation that answers them separately has not answered the question.
The sentence to put on the enquiry is short: ball finish and seat facing as a matched pair, to be confirmed on the approved drawing, with the leak rate stated. That one line does two things. It stops the two lists being quoted independently, and it puts the acceptance on the drawing where it can be checked, instead of in a catalogue where it can be assumed. Weight and torque belong on the drawing too, and not in a table that was filled in before the size was known.
FAQ
Q: Should the ball and the seat be ordered together?
A: Yes, and at class 2500 it is not a preference. The seat is metal, so the seal forms where the ball surface and the seat facing touch. A soft nickel deposit against a hardfaced seat wears; two surfaces of the same hardness fret rather than slide. Quoting the two lines independently is how a valve gets built from parts that were each the best in their own list.
Q: Which ball surface goes with a metal seat?
A: It depends on what is in the medium rather than on a ranking. A clean, non abrasive duty is served by a nickel plating or hard chrome. A duty carrying particles needs tungsten carbide. Where the ball may be refurbished rather than replaced, the cobalt alloy overlay is the one that can be re-machined. In every case the seat facing is chosen at the same time, and the pair is confirmed on the drawing.
Q: What leak rate should be written for a metal seat?
A: A permitted rate rather than zero. A metal seat has no resilient insert to take up a particle or a mark, so it is judged against a rate stated on the order, and the test record names the rate that was applied. A specification that asks a metal seat to hold bubble tight will be rejected at the bench for behaving the way a metal seat behaves.
Q: Is class 2500 the same as PN 420?
A: They are two designations for one rating. The API 6D pressure code list pairs class 2500 with PN 420, in the same way that it pairs class 1500 with PN 250 and class 600 with PN 100. The flange is a separate decision: up to twenty four inch it is an ASME B16.5 ring joint flange whichever designation the order uses.
Q: Why does the page give a size range instead of a size?
A: Because two inch to twenty four inch is what the works can make, not what is being quoted. Above twenty four inch the flange leaves ASME B16.5 for B16.47 and the series has to be chosen, and the body layout also changes at six inch, where the trunnions move into bearing blocks. A size on the order is what turns this page into a valve.
Q: Does a three piece body mean the seat can be changed in line?
A: The middle section has to come out, so no. The line is isolated, drained and vented, both body joints are released, and the centre section leaves with the ball and both seats inside it. What the three piece side entry layout does buy is that the middle section is a manageable part to handle and the pipe does not have to be cut.


Hot Products


News
Ball Valves On A Bottom Loading Gantry: Creep, Dry Break And The Test That Proves Neither
A loading gantry cycles a ball valve far more than it is designed for and still cannot prove shut-off. Where creep starts, and what to specify.
Read More
Lined Ball Valves in Acid Service: The Liner Does Not Fail, The Steel Behind It Does
The valve came out of the line looking better than most valves that come out of a hydrochloric acid line. Three inch, PFA lined, cast body, Class 150, fourteen months in service on a 32 percent acid transfer duty at 55 to 60 degrees C, about forty open and close cycles a week. The paint was intact.
Read More
Ball Valves in Amine CO2 Capture: Heat Stable Salts, Rich Amine, And The Three Places The Body Thins
Rich amine at 110 C with heat stable salts is where capture plant ball valves fail. Materials, velocity limits, cavity gas and seat choice, with numbers.
Read More
Fail-Safe Ball Valve Actuators: Spring Return, Stored Air, And The Torque Nobody Checks
Spring return or stored air? The answer is a torque curve, not a datasheet box. Sizing, receiver volume, closing time and four silent failures.
Read More