


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q41F
-
J-VALVES
Overview of the J-VALVES API 6D DN80 WCB floating ball valve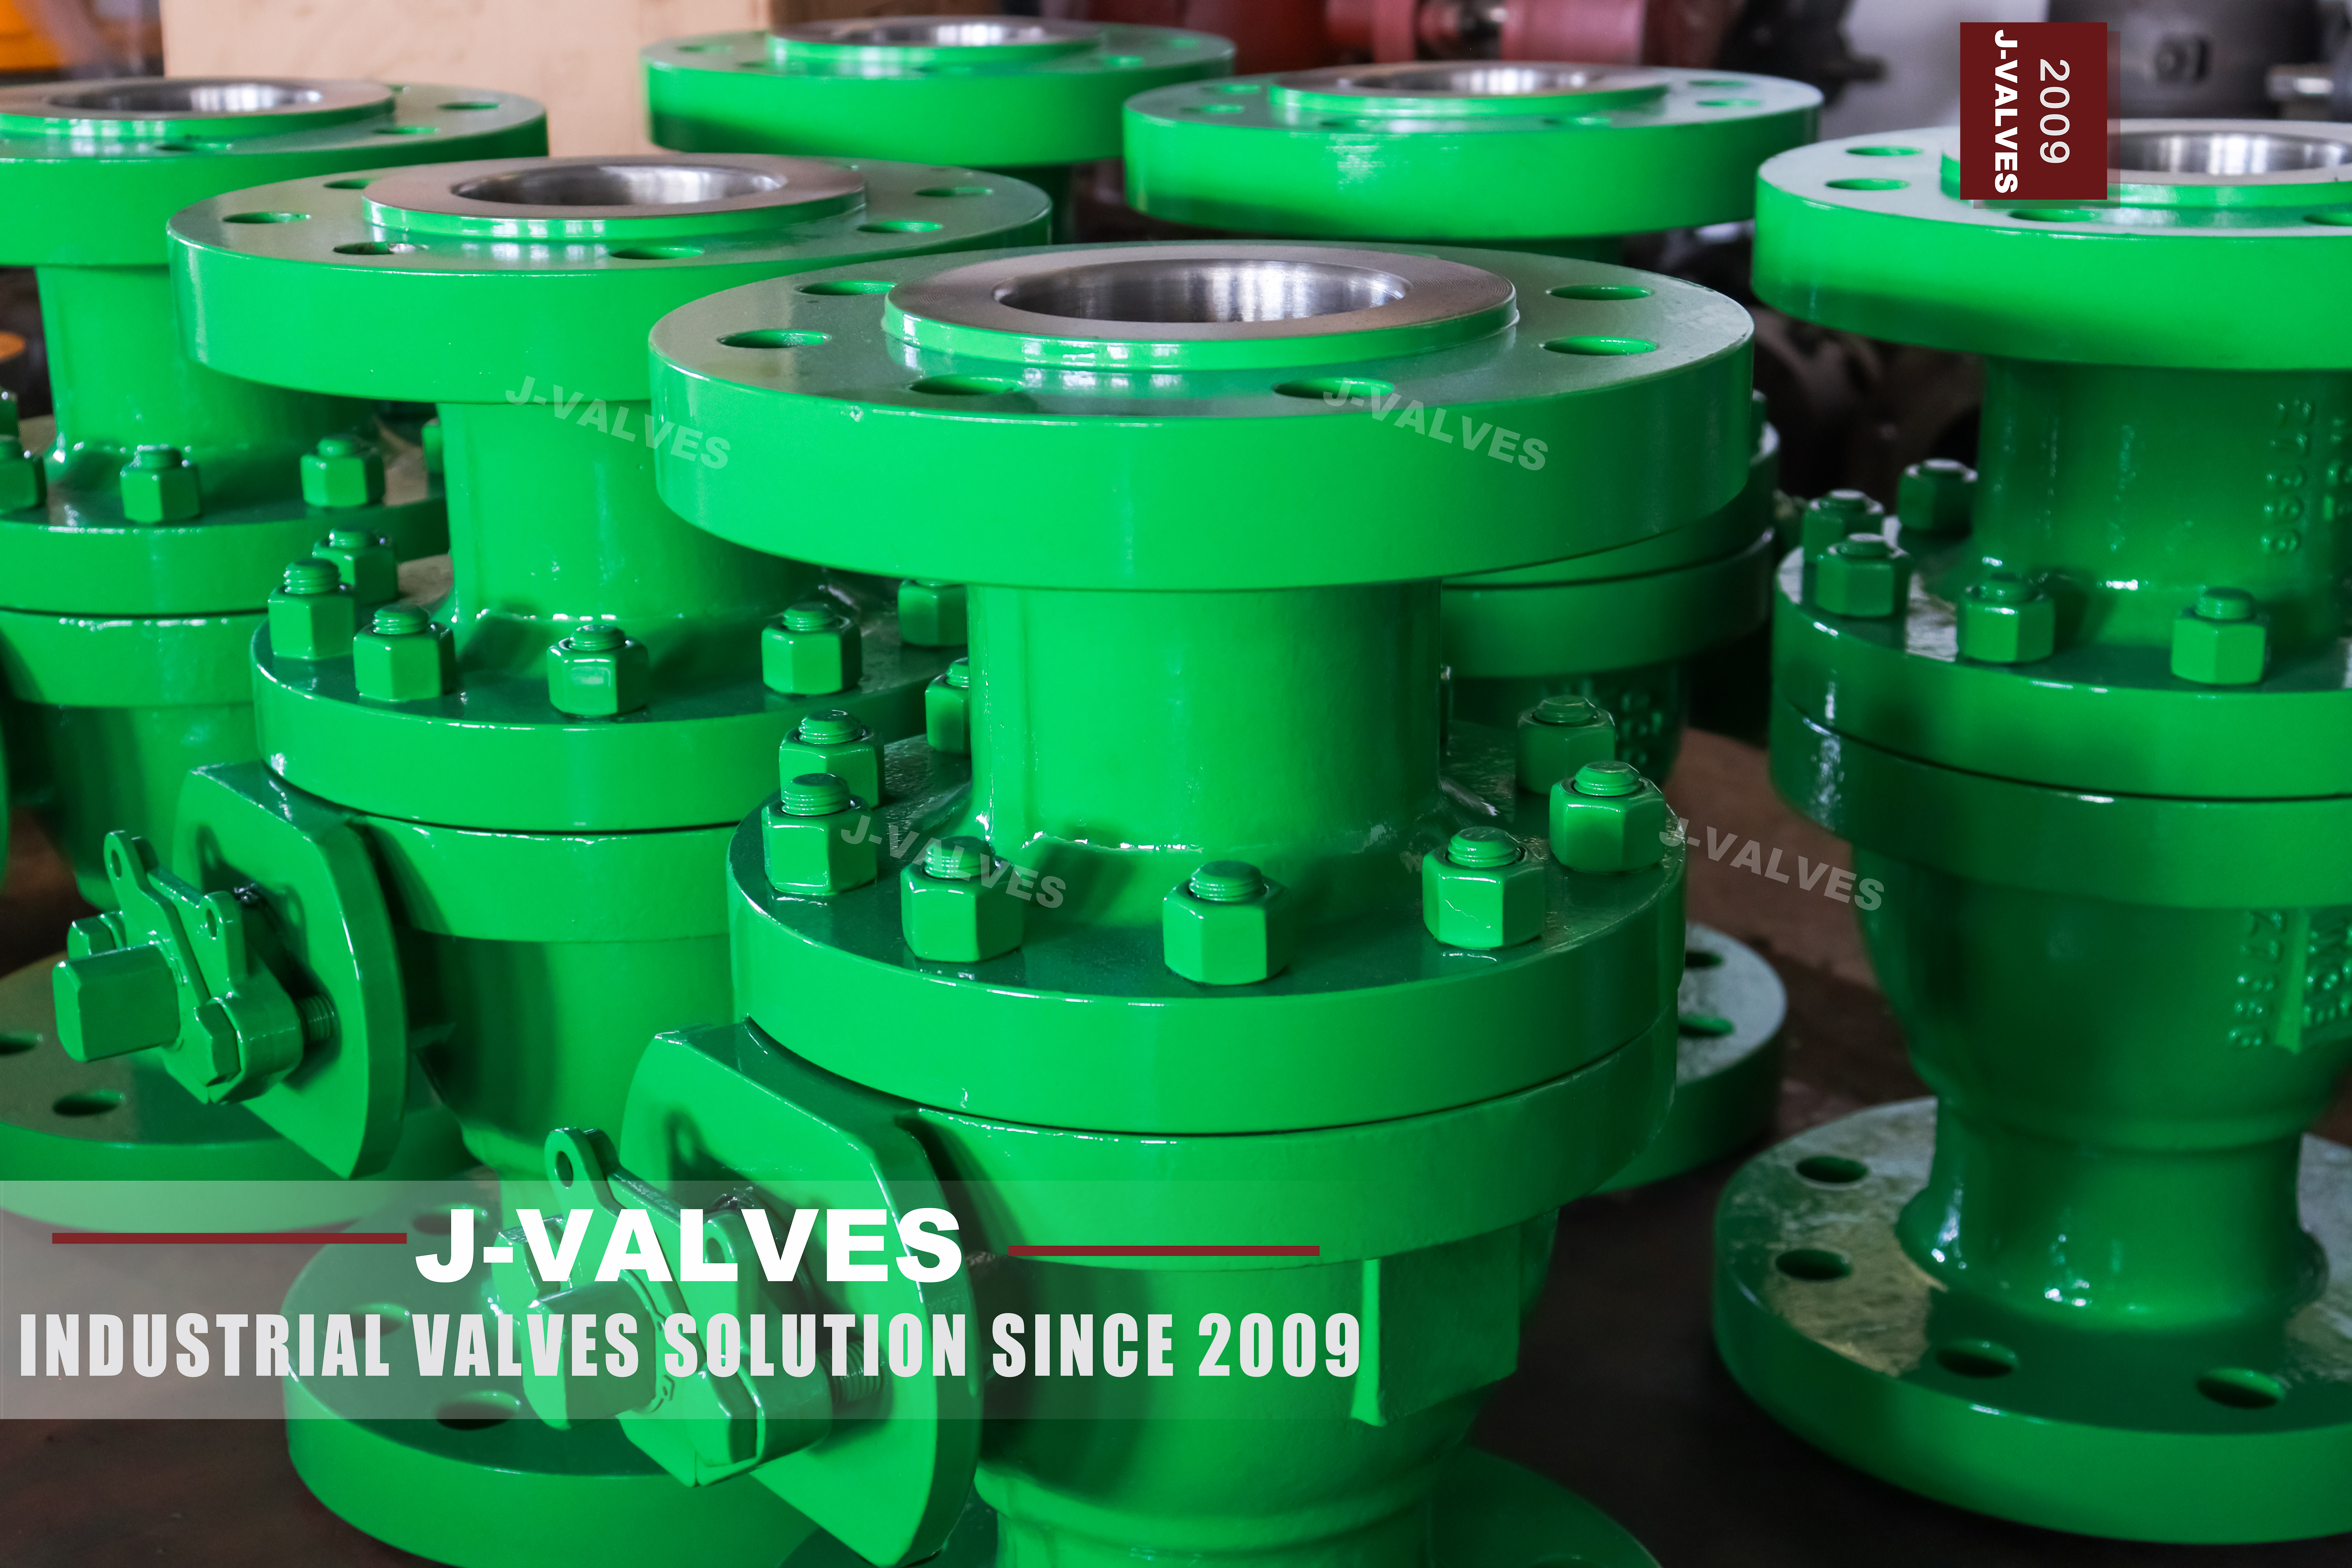
Three inch, cast carbon steel, floating ball, and a product standard that is normally associated with pipeline valves rather than with a plant valve. That combination is the point of this page: DN80 is the size where a floating ball still works well and where API 6D is often the standard a buyer's specification asks for, whatever the valve is actually doing in the plant.
The body is ASTM A216 WCB, which is the cast carbon steel grade that most of the world's general purpose valves are made from. The ball floats, the ends are raised face flanges to ASME B16.5 or butt weld preparations to ASME B16.25, and the published pressure range runs from Class 150 to Class 2500. What that range does not say is that every class in it behaves the same way, and the top of the range is where the seat is doing the most work.
Two claims need separating before anything else on the page is useful. The first is the seat: a floating ball has two seats but only the downstream one is a barrier, so the valve is not a double block and bleed device however the catalogue describes it. The second is the standard: API 6D is a pipeline valve standard, and a DN80 valve can be built to it and still be installed in a plant rather than a pipeline, which is exactly what most of these valves are.
Design and Construction
A floating ball is supported by its seats rather than by trunnions. Pressure on the upstream side pushes the ball downstream into the seat on the low pressure side, and that contact is what seals. The mechanism is simple and it scales down well: at DN80 the force on the ball is small enough that the seat can take it without deformation, and the result is a valve with very few parts and a very short stroke.
The consequence of that mechanism is that the two seats do not do the same job. The downstream seat is the seal; the upstream seat is a guide, a back-up and, when the valve is closed with pressure on both sides, another sealing surface. That is why a floating ball valve can be sold as bidirectional and cannot be sold as double block and bleed: a bleed requires two independently sealing seats and a cavity port, and on this design the two seats are not independent.
The stem is a plain shaft with a shoulder under the gland, so pressure cannot blow it out, and the anti-static path runs from the ball through the stem to the body. On a valve that may sit in a fuel gas line, that continuity is a safety item rather than a nicety, and it is one of the few things on the valve that cannot be checked by looking at it.
The ends decide how the valve is installed and how it can be removed. Raised face flanges to ASME B16.5 make it a plant valve that can be unbolted; butt weld ends to ASME B16.25 make it a permanent part of the line and are what API 6D expects for a pipeline application. The same body can be supplied either way, and the choice belongs on the order rather than in a conversation after the valve has been cast.

Material Options
WCB is a cast carbon steel with good strength, reasonable toughness and excellent weldability, and the last of those is why it is used so widely. A casting can be repaired by welding under a qualified procedure, which means a body with a minor surface defect does not have to be scrapped; a forging usually cannot be repaired that way, and a forging with a defect is scrap. That is the economic argument for cast bodies at this size and it is a real one.
The counter-argument is quality control. A casting is only as good as its pattern, its gating and its risers, and the internal soundness of the body depends on the foundry rather than on the mill certificate. That is why radiography or ultrasonic examination of a cast body is a legitimate thing to ask for, and why the answer to the question which foundry made it matters more on a WCB valve than on a forged one.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Body | ASTM A216 WCB casting | A105 forging for higher strength; A350 LF2 for low temperature | Cast body can be repaired by welding under procedure |
| Ball | WCB or A105 with electroless nickel plating | Hard chrome; stainless steel hard facing | The coating is the wear surface |
| Stem | A105 with ENP | 17-4PH; SUS420 for wear resistance | Blowout proof, anti-static |
| Seat | PTFE or reinforced PTFE | PPL; metal with flexible graphite | The seat sets the working temperature |
| Packing | PTFE V rings | Flexible graphite with wire reinforcement | Graphite for the high temperature end |
| Body joint gasket | Flexible graphite spiral wound | Metal ring joint gasket | One per joint |
| Bolting | A193 B7 with A194 2H nuts | B8M with 8M nuts | Carbon bolting is correct on a carbon body |
| Ends | Raised face to ASME B16.5 | Butt weld to ASME B16.25 | API 6D expects a weld end for pipeline duty |
Technical Specifications
The table fixes the size and the class range, and it deliberately does not fix a single class, because the page covers a range and the class is chosen by the line. What it does fix is the standard, the ends and the seat family, which are the three items that decide whether the valve can be used at all.
| Item | Value |
|---|---|
| Size | 3 inch, DN80 |
| Pressure class | Class 150 to 2500, recorded as PN 20 to PN 420 in API 6D clause 7.2 |
| Body style | Cast body, floating ball, side entry |
| Body material | ASTM A216 WCB casting, ASME B16.34 group 1.1 |
| Ball | WCB or A105 with electroless nickel plating |
| Stem | A105 with ENP, blowout proof, anti-static |
| Seat | PTFE or reinforced PTFE; PPL; metal with flexible graphite |
| End connections | Raised face to ASME B16.5; butt weld to ASME B16.25 |
| Bore | Full bore as standard, reduced bore on request |
| Face to face | ASME B16.10 for the size and class ordered, confirmed on the signed GA drawing |
| Temperature | Minus 29 to plus 425 C as published; the seat sets the working limit |
| Operator | Lever with a locking device; worm gear, pneumatic, electric or hydro-pneumatic on request |
| Design standard | ASME B16.34 and API 6D |
| Test standard | API 598, shell at 1.5 times and seat at 1.1 times the rating |
Standards and Compliance
API 6D is written for pipeline valves, and its requirements are about the things a pipeline needs: a defined bore table, a defined face to face, ends that can be welded, cavity and drain provisions, marking and a document package that travels with the valve. A DN80 valve built to it is a valve that can be specified by a pipeline engineer without a conversation, and that is why the standard appears on plant specifications even where there is no pipeline in sight.
ASME B16.34 supplies the pressure boundary. The class is a number, group 1.1 is the material group for a carbon steel body, and the wall that goes with them is calculated rather than copied from a table on a supplier website. What the standard cannot tell a buyer is whether the casting inside that wall is sound, because that is a question about the foundry and it is answered by an examination report rather than by a clause.
API 608 is listed on the source page alongside 6D, and the relationship between them is a scope question. API 608 covers DN 15 to DN 600 and Class 150 to 600; API 6D covers pipeline valves without that class ceiling. At the bottom of this valve's range both standards can apply, and at Class 900 and above only 6D does. A data sheet that lists both without saying which applies to which class is not telling the reader anything.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Wall thickness and rating | ASME B16.34 group 1.1 | Design calculation for the product form supplied |
| Pipeline valve requirements | API 6D | Bore table, marking, cavity and drain provisions, documentation |
| Soft seated ball valves | API 608, Class 150 to 600 only | Applies at the bottom of the range |
| Pressure testing | API 598 | Shell at 1.5 times, seat at 1.1 times the rating |
| Fire test | API 607, ISO 10497 as the equivalent | Type test certificate with a size and class scope |
| Flange dimensions | ASME B16.5 | Raised face cut to the facing ordered |
| Casting examination | Radiography or ultrasonic, supplementary | Report when the order asks for it |
| Material certificate | EN 10204 3.1 | Body, ball and stem, heat number matched to the marking |
Manufacturing Process
The body is cast, which means a pattern, a mould and a pour, and the quality of the body is decided before any machining starts. Sand inclusions, shrinkage and gas porosity are the three defects a casting can hide, and the way to control them is the foundry's process rather than the machine shop's skill. That is why the first question about a WCB valve is not about the machining tolerance.
Machining is where the casting becomes a valve. The flange faces, the bolt circles, the bore and the seat pockets are cut in sequence, and the seat pockets have to end up square to the bore and concentric with each other, because a floating ball has no trunnion to correct a misalignment. On this design the seats are what position the ball, so any error in the pockets becomes an error in the seal.
Assembly and test follow the usual order: seats in, ball between them, body closed, stem and gland fitted, lever fitted, shell test, seat test, drain, dry, mask and paint. The masking is the step that decides whether the flange leaks on site, because paint on a raised face is a leak waiting for a hydro test that will be blamed on the gasket.

Quality Control and Testing
Every valve is shell tested, seat tested and dimensionally checked. On a cast body there is one extra question that a forged body does not raise: whether the casting itself is sound, and whether that soundness was verified or assumed.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| 1 Material | Heat number, chemistry and tensile on the casting | ASTM A216 WCB, EN 10204 3.1 |
| 2 Casting | Radiography or ultrasonic examination when ordered | Report with the certificate |
| 3 Dimensional | Flange facing, bolt circle, face to face | ASME B16.5 and B16.10 |
| 4 Machining | Seat pocket concentricity, bore, joint face flatness | Drawing tolerance |
| 5 Shell test | Body and body joint at 1.5 times the rating | API 598, no leakage |
| 6 Seat test | Each seat at 1.1 times the rating, both directions | API 598, zero visible leakage |
| 7 Function | Quarter turn, lever stop, anti-static continuity | Works standard |
| 8 Final | Drained, dried, faces masked, painted, capped | Works standard |
The seat test is run in both directions and the result is not the same in each. With pressure on one side the ball is pushed into the far seat and that seat seals; with pressure on the other side the reverse happens. A valve that holds one way and weeps the other has a damaged seat or an out of round ball, and no amount of gland tightening will change it.

Applications and Industry Service
The ordinary homes for a DN80 WCB floating valve are plant piping rather than pipelines: water and utility headers, compressed air, fuel gas distribution inside a battery limit, steam condensate, and the isolation point in front of equipment. In all of those the valve is a block valve, it is operated occasionally, and it is expected to be cheap enough to have a spare on the shelf.
It is also used on small pipeline branches and on pig launcher and receiver piping, which is where the API 6D requirement usually comes from. On a branch that will never be pigged a floating valve is fine; on the mainline itself the choice is usually a trunnion valve, because the seat load and the operating torque at larger sizes make a floating ball impractical.
A cast WCB body also has one practical advantage that rarely appears in a data sheet: it can be machined into shapes that a forging cannot, which is why the body has the rounded section around the ball and the integral bosses for the stem and the drain. On a three inch valve that shape is not decoration. It is what allows the wall to follow the load instead of being a uniform section, and it is the difference a buyer sees as shape on a cast body and as a plain machined outline on a forged one.
Where it is the wrong valve is at the top of its own pressure range with a large seat, or on a duty where two independent barriers are required. On those duties the answer is a trunnion valve with a defined seat arrangement, and the difference is not a matter of quality but of what the design can promise.

Installation, Operation and Maintenance
The valve is bolted between flanges with a gasket on each side, or welded in at the butt ends. On a flanged joint the gasket is centred by the bolts and the studs are brought up in a cross pattern; on a weld end the preparation is cut to ASME B16.25 and the root is what decides whether the joint passes inspection. The valve should be open during welding so that heat does not trap anything against a seat.
The gasket is chosen with the flange rather than after it. A spiral wound gasket with a flexible graphite filler covers the temperature range of this valve and is the default; a sheet gasket is cheaper and is the wrong answer on anything above the low temperature end. On a raised face joint the gasket sits inside the bolt circle and is located by the studs, and the faces have to be clean and unpainted, because paint under a gasket is a leak path with a predictable future.
Operation is a quarter turn of the lever, and the locking device is there so that the position can be fixed. The stem packing can be adjusted with the valve under pressure because the stem is retained by the body, and the upper seal can be replaced after the cavity has been vented. A floating valve has no seat injection fitting as standard, so a leaking seat is a bench job rather than a site fix.
Maintenance is limited to the gland, the lever and, on a body that comes apart, the seats and the ball. Before any of that the line has to be isolated and the cavity vented through the drain plug, and on a valve that has been in fuel gas service the cavity has to be treated as a hazard until it has been proved empty.
How to Specify and Order
Five things decide the valve: the size, the class, the body grade, the end connection and the seat. The class is the one that a range page can hide, because 150 to 2500 is a range and a valve is one class; writing DN80 without a class leaves the supplier to ask, and the answer changes the price more than any other single item.
Three more questions are about the line: the medium, the temperature and whether the joint will be flanged or welded. The medium decides the body grade and the seat, the temperature decides whether PTFE is enough, and the joint type decides whether the valve can ever be removed without cutting the pipe.
Documents should be named: EN 10204 3.1 for body, ball and stem, the shell and seat test records, the dimensional report, the casting examination report if one was ordered, and the fire test certificate with its scope if fire safe is claimed. None of them are in the standard crate unless the order says so.
FAQ
Q: Why does a plant valve carry API 6D?
A: Because a specification asked for it. API 6D is written for pipeline valves and it fixes the bore table, the face to face, the end preparations, the cavity and drain provisions and the document package. A DN80 valve built to it can be dropped into a plant line and still satisfy a specification written by a pipeline engineer, which is why the standard turns up on plant enquiries far more often than pipelines do.
Q: Is this a double block and bleed valve?
A: No. On a floating ball the downstream seat is the barrier and the upstream seat is a guide and a back-up; the two are not independent. A cavity bleed will tell you whether the downstream seat is holding, and that is a useful check, but a double block and bleed claim needs two independently sealing seats and a cavity connection. That is a trunnion valve with the right seat arrangement.
Q: Cast WCB or forged A105 at the same class?
A: WCB is cheaper and can be cast into the shape the wall wants, and it can be repaired by welding under a qualified procedure. A105 is a forging, so it is denser and it cannot be repaired in the same way. Which one is right depends on how the valve is being bought: a general purpose plant valve is usually cast, and a valve where soundness has to be proved rather than assumed is usually forged.
Q: Should the ends be flanged or welded?
A: Flanged if the valve has to be removable with hand tools, butt weld if it is going into a line that will be tested and left alone. API 6D expects a weld end for pipeline duty, and on a small branch the butt weld is also the joint that can be radiographed. The same body can be supplied either way, so the choice is made on the order.
Q: What limits the temperature on this valve?
A: The seat. The published body range is minus 29 to plus 425 C, but PTFE sits far below the ceiling and only PPL, PEEK or a metal seat reaches the top of it. The temperature on the order should be the one the seat can take, and if it is not, the seat is what changes.


Hot Products


News
Stainless Steel Ball Valve Grades: 304, 316 And 316L, And What Actually Decides
Molybdenum is the difference that decides the duty, carbon is the difference that gets missed, and the chloride in the line matters more than the price.
Read More
Ball Valve Spare Parts for Overseas Projects: The Wear Part List, The Quantity Math, And Four Traps
Why isolation valves fail on calendar time, not cycles. Wear part lists, Poisson stock maths, seat kit traps and the clauses that decide year six.
Read More
Ball Valves On A Bottom Loading Gantry: Creep, Dry Break And The Test That Proves Neither
A loading gantry cycles a ball valve far more than it is designed for and still cannot prove shut-off. Where creep starts, and what to specify.
Read More
Lined Ball Valves in Acid Service: The Liner Does Not Fail, The Steel Behind It Does
The valve came out of the line looking better than most valves that come out of a hydrochloric acid line. Three inch, PFA lined, cast body, Class 150, fourteen months in service on a 32 percent acid transfer duty at 55 to 60 degrees C, about forty open and close cycles a week. The paint was intact.
Read More