


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q41F
-
J-VALVES
Overview of the J-VALVES 0.75x0.5 Inch 150LB Two Piece Stainless Steel Extended Stem Floating Ball Valve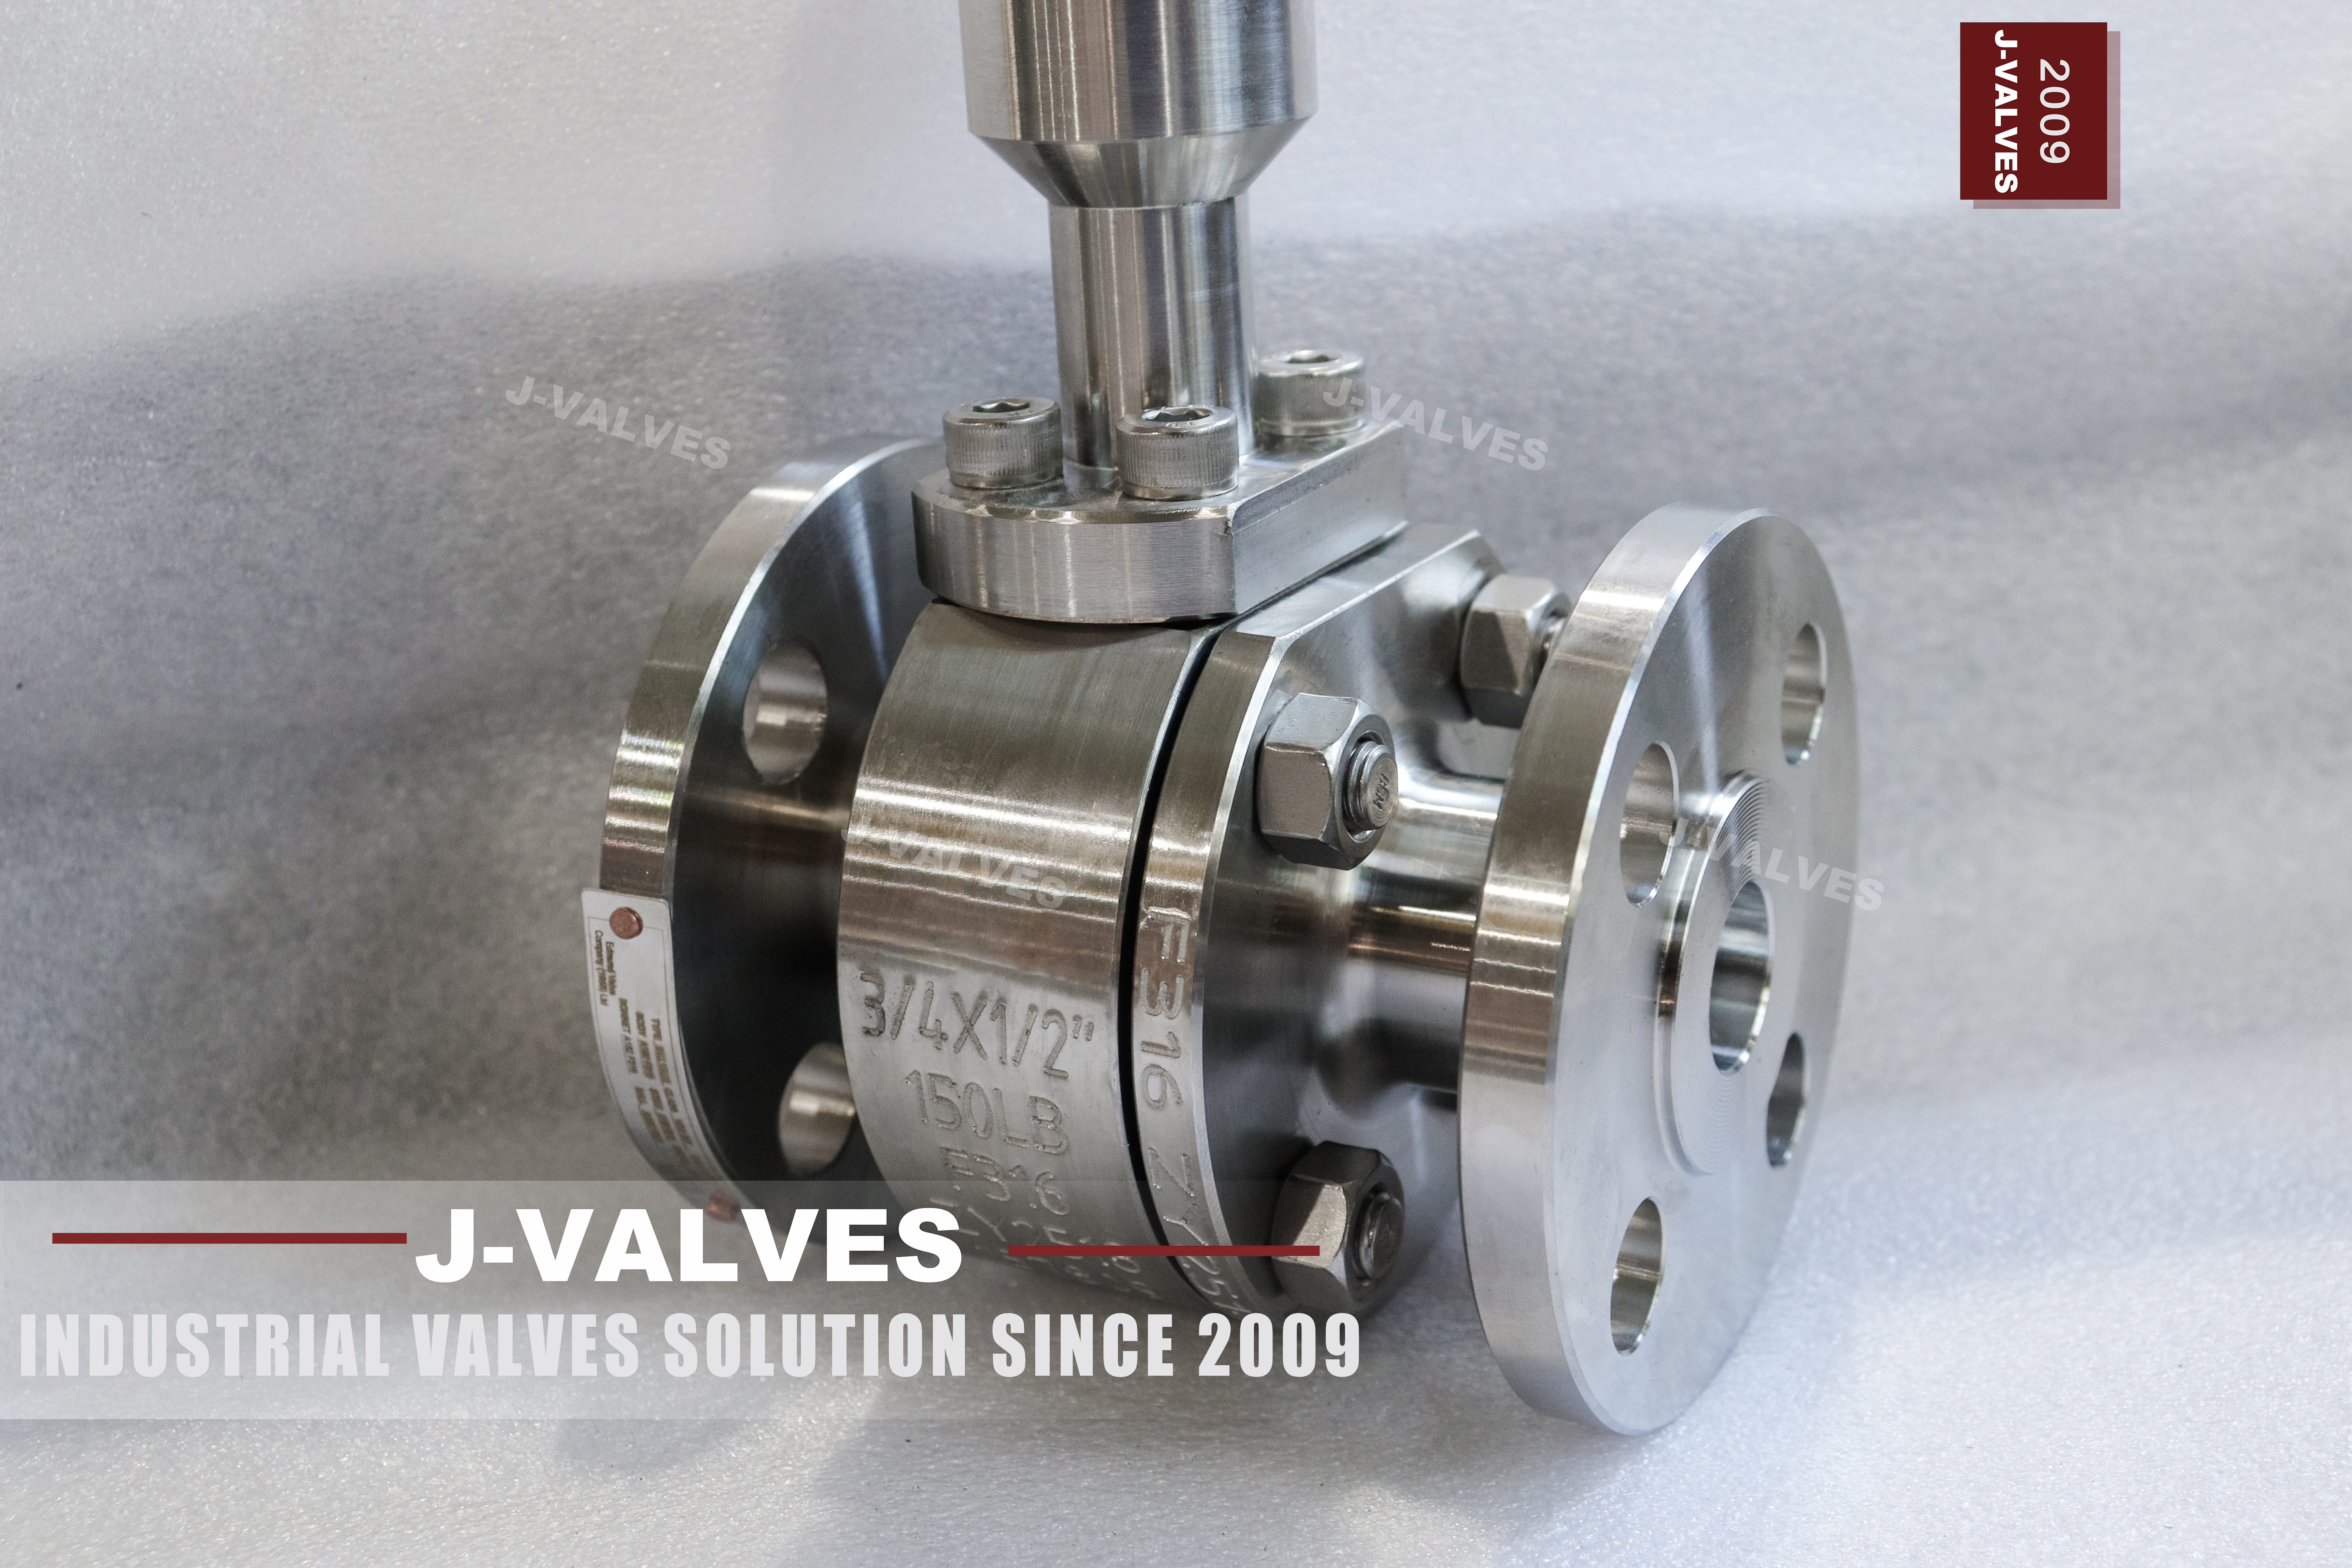
Three numbers sit in this valve designation and only one of them is a pipe size. The 0.75 inch end is a DN20 Class 150 raised face flange, so that is the pipe it bolts to. The 0.5 inch figure is the bore through the ball and the seats, a DN15 passage. The 150 is the pressure class, which sets the wall, the flange drilling and the test pressure, and says nothing about either of the other two numbers. Read left to right, the name tells you which line it fits and how much it passes.
One temperature range is printed for the whole valve, minus 29 to plus 425 Celsius, and three seat materials are listed underneath it. That range describes the metal. It is the band in which the body, the ball and the stem keep their strength, and it comes from the rating table for the class rather than from a bench measurement. The seat is a polymer, and no polymer seat follows the metal to the top of that band. When temperature decides the order, the seat material on the line above decides it.
Design and Construction
A two piece body splits at a single bolted joint. The ball, both seats and the stem packing go in through that side, which is the only reason the joint exists: at half an inch the body could be made in one piece, or welded shut, and it would be cheaper and easier to keep tight. The pattern is kept because the seats wear and somebody has to reach them. On a small valve in a dosing or sampling line, replacing a seat is the only maintenance the valve will ever need.
Nothing carries the ball. It sits loose between the two seats, and line pressure pushes it downstream until it bears on the outlet seat; that contact is the seal. Because the force scales with bore area and with pressure, a DN15 bore at Class 150 produces a small seat load, a light lever and a short quarter turn stroke. The same design at three inches is a different proposition, and that is where the industry changes over to a trunnion. Here there is no such need.
Material Options
The parameter block on the original page names a cast stainless body, CF8 or CF8M, to the castings specification. The product photograph filed for this same valve is named as a forged F316 body. Both patterns are made at three quarter inch and both are sold under the same description, so the page cannot settle it and this page does not try. The alloy family is stainless steel; the grade is whatever the nameplate and the mill certificate say, and the order should be written so that either answer is acceptable.
Trim follows the body. The ball is stainless with hard chrome plating, or a low carbon grade if the medium asks for it. The stem is stainless and extended, and the extension is the same alloy as the stem so the two do not grow at different rates when the line heats up. Seats are PTFE, reinforced PTFE or PPL; packing is flexible graphite or PTFE. Those four lines decide service life, and they are worth writing on the order rather than leaving to the standard build.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Body and side body | stainless steel, grade as stamped | cast CF8 / CF8M or forged F316 | two pieces, one bolted joint |
| Ball | stainless with hard chrome plating | low carbon stainless | ground, then plated |
| Stem | stainless, extended | same alloy as the extension | packing stays in the body |
| Seat | PTFE | reinforced PTFE or PPL | sets the service temperature |
| Packing | flexible graphite | PTFE | gland adjustable |
| Extension | stainless, 200 mm to 800 mm typical | length to the drawing | not a pressure boundary |
| Ends | raised face to ASME B16.5 | Class 150 only | DN20 pattern |
Technical Specifications
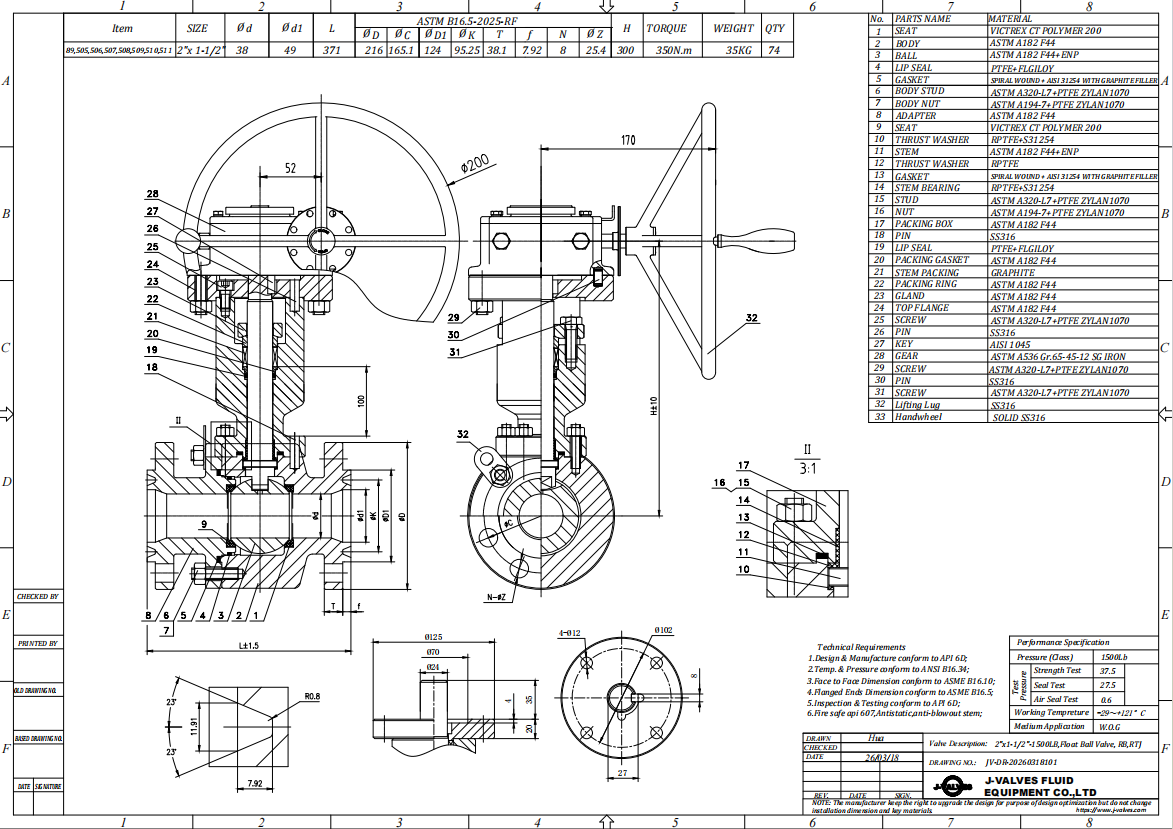
The size data sheet gives the bore, the face to face length and the flange dimensions for the DN20 pattern. The wall and the pressure temperature rating come from the class, not from this valve, so they are read off the standard table for the material and the class rather than quoted as if they had been measured here. Anything beyond that, such as overall height with a particular extension, is dimensioned on the signed general arrangement drawing for the size and trim ordered.
Reduced bore has a different cost at this size than it does at twelve inches. There is no meaningful pressure drop to argue about when the whole line is three quarters of an inch and the flow is a few cubic metres an hour. What the reduction does do is make the valve the narrowest passage in the run, and at DN15 that passage is small enough for scale, thread tape or a stray weld bead to bridge it. A strainer upstream is cheaper than the downtime.
| Item | Value |
|---|---|
| Nominal size | 0.75 x 0.5 inch (DN20 ends, DN15 bore) |
| Pressure class | Class 150 (PN 20) |
| Body style | two piece, one bolted joint |
| Ball support | floating, no trunnion |
| Bore | reduced bore, DN15 |
| Body material | stainless steel, grade as stamped on the nameplate |
| Ball material | stainless with hard chrome plating, low carbon grade optional |
| Stem | stainless, extended, same alloy as the extension |
| Seat | PTFE, reinforced PTFE or PPL |
| Packing | flexible graphite or PTFE |
| Extended stem length | 200 mm to 800 mm typical, set by the service |
| End connection | raised face flange, ASME B16.5, Class 150 |
| Face to face | dimension on the signed GA drawing |
| Design standard | ASME B16.34 and API 608 |
| Test standard | API 598 shell and seat test |
| Test pressure | shell 1.5 times and seat 1.1 times the class rating |
| Temperature range | minus 29 to plus 425 Celsius, metal temperature |
| Temperature limit | set by the seat material, not by the body |
| Operation | lever with locking hole; worm gear, pneumatic or electric optional |
| Fire test | not claimed on this page, API 607 to be specified if required |
| Anti static device | not claimed on this page |
| Marking | size, class, body code, heat number |
| Documentation | EN 10204 3.1 on request |
| Weight | quoted with the drawing for the size and trim ordered |
| Country of manufacture | China |
Standards and Compliance
Two standards are named on the page and they do different jobs. ASME B16.34 is the pressure boundary document: it fixes minimum wall thickness against bore and class and publishes the pressure temperature ratings the valve may work to. API 608 is the ball valve document, and it covers the things specific to a quarter turn valve rather than to a gate or a globe. Testing is a third document, API 598, and it is where the acceptance numbers come from.
What the page does not claim matters as much as what it does. No fire test is named for this valve, no anti static device is described, and no actuator mounting pattern is specified. A soft seated quarter turn valve is normally required to pass a fire test of the API 607 type before it goes into a hydrocarbon line, and that is a type test on the design, not something a single unit is checked against. If a project needs it, it has to be asked for by name.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Pressure boundary | ASME B16.34 | wall thickness and the rating table for the alloy at Class 150 |
| Ball valve design | API 608 | the quarter turn requirements specific to this product |
| Shell and seat test | API 598 | 1.5 times the rating for the shell, 1.1 times for the seat |
| Flange drilling | ASME B16.5 Class 150 | DN20 raised face pattern |
| Marking | API 608 and the order | size, class, body code, heat number |
| Fire test | not claimed on this page | API 607 named on the order if the line needs it |
| Documentation | EN 10204 3.1 | issued against the heat number on request |
Manufacturing Process
Body blanks arrive as castings or forgings and are machined in one setup where possible, so that the bore, both seat pockets and the flange faces stay concentric. The ball is ground and then plated; the plating is what gives the soft seat something harder to run against. Seats are turned or moulded, and the sealing face is lapped flat. Each part is measured before assembly, because a seat that is out of flat by a few microns will leak at low pressure however well the rest is made.
Assembly is done dry and clean. The ball goes in between the seats, the stem drops through the packing bore, and the body halves are drawn together to a controlled torque so the seat crush is the same on both sides. The extension is fitted afterwards and the coupling is set so the stem turns without side load on the gland. Every unit is cycled and pressure tested before marking, and the marking carries size, class, body code and the heat number that ties it to the certificate.

Quality Control and Testing
Shell and seat tests follow API 598. The shell test is one and a half times the rated pressure at the class and is held long enough to show a leak; the seat test is one and one tenth times the rating and is done in both directions. Both multipliers are written in the standard, which is why they can be quoted here. The acceptance criteria are in the standard too: no visible leakage through the body wall, and for a soft seated valve no visible leakage past the seat.
A pressure test proves the body does not leak. It does not prove what the body is made of, and on a stainless valve that is the question that goes wrong in service. That is answered by the mill certificate behind the 3.1 documentation and, where the buyer asks for it, by a positive material identification check on the finished body. The test and the certificate cover different failures, and an order that asks for one but not the other is only half protected.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| Incoming body | grade, heat number, wall thickness | certificate against the stamped code |
| Machining | bore, seat pocket depth, flange face squareness | in process gauging against the drawing |
| Ball | roundness and plating thickness | sampled before assembly |
| Assembly | seat crush on both sides, stem torque | controlled torque on the body joint |
| Shell test | no leakage through the body wall | API 598 at 1.5 times the rating |
| Seat test | no visible leakage, both directions | API 598 at 1.1 times the rating |
| Marking and packing | nameplate against certificate and drawing | checked before boxing |

Applications and Industry Service
This valve is bought for lines that somebody has to reach past something. The extension puts the lever outside insulation, outside a cold box wall or above a pit cover, while the body stays where the pipe is. That makes it a natural fit on chilled water and refrigeration headers, on small cryogenic branches where the line runs below ambient, and on dosing or sampling points where the pipe is lagged and the operator still needs a handle at a sensible height. The medium is normally clean and non abrasive.
It is the wrong valve in three situations. Slurries and media with solids will bridge the DN15 bore. Service above the seat material own ceiling will deform the seat long before the body is in trouble. And a line cycled thousands of times a year will wear seat and packing on a schedule that has nothing to do with pressure, which is a maintenance planning problem rather than a valve selection problem, but it should be priced in at the start rather than discovered later.

Installation, Operation and Maintenance
Mount it with the stem vertical or horizontal, never upside down, because the cavity above the ball has to drain and the packing has to stay in contact with whatever is in the line. Leave room to swing the lever through ninety degrees and to get a wrench on the body joint. Where the line is insulated, the insulation stops at the body and the extension passes through it; the extension joint is not a pressure boundary, so it does not need insulating, but it does need to stay reachable.
Maintenance is seat replacement, and it is done by taking the body joint apart with the valve out of the line. The ball comes out with the seats, and both seats are replaced as a pair, because a worn seat on one side will damage a new one on the other. Packing is adjusted at the gland and replaced when the gland runs out of travel. The lever should turn without a cheater bar; if it needs one, the seat has swelled or the cavity has scaled, and forcing it damages the stem.
How to Specify and Order
The order line needs six things: the size written as flange by bore, the class, the body alloy code as it will be stamped, the seat material, the end facing, and the extension length with its datum. Anything not on that list will be supplied to the standard build, and the standard build is what the catalogue page shows rather than what the line needs. If the grade of the body is not settled, say so on the order and let the certificate settle it, instead of writing a grade the foundry may not pour.
Before shipment three documents should agree with each other: the nameplate, the mill certificate and the general arrangement drawing. The nameplate carries size, class, body code and heat number. The certificate carries chemical and mechanical results for that heat. The drawing carries face to face, flange drilling and extension length. When those three disagree, either the valve is right and the paperwork is wrong or the reverse, and neither can be discovered at site without taking the line apart.
FAQ
Q: What does 0.75x0.5 mean on a ball valve?
A: It is the flange size by the bore size. The 0.75 inch figure is the DN20 flanged end that bolts to the pipe, and the 0.5 inch figure is the DN15 passage through the ball and the seats. The valve therefore fits a three quarter inch line and passes what a half inch line would pass. That is what reduced bore means at this size, and it is the reason the valve is light and the lever is easy to turn.
Q: Can this valve be used at the top of its printed temperature range?
A: Not with a polymer seat. The range printed for the valve, minus 29 to plus 425 Celsius, is the band in which the metal parts keep their properties. The seats listed on the same page are PTFE, reinforced PTFE and PPL, and each of those has its own much lower ceiling. If the service temperature is near the top of the printed range, the valve has to be ordered with a metal seated design, not this one.
Q: Is the body cast or forged?
A: The page does not settle it and neither does this one. The parameter block names a cast stainless body to the castings specification, while the product photograph for the same valve is filed as a forged body in a low carbon grade. Both patterns are made at three quarter inch. The nameplate and the mill certificate behind the 3.1 documentation are what actually state the grade, and the order should be written to accept either.
Q: How is the extended stem length decided?
A: By the insulation or the pit, plus the clearance the operator needs, measured from a stated datum on the valve. The catalogue figure of 200 to 800 mm is a range, not an order line, so the length and the datum both have to appear on the purchase order and on the general arrangement drawing. A valve built to a length with no stated datum is the most common cause of a unit arriving at site too short or too long.
Q: Does this valve come with a fire safe certificate?
A: No fire test is claimed for this valve on this page, and no anti static device is described either. A soft seated quarter turn valve is commonly required to hold a fire test of the API 607 type before it is accepted into a hydrocarbon service, but that is a type test on the design and it has to be asked for by name on the order. It is not something a single unit is checked against during the routine shell and seat test.
Q: What is the difference between this valve and the other 0.75x0.5 listing?
A: They describe the same size, class and body pattern, and the other listing is named as a forged body. Only one of the two should be kept as the indexed page, because two URLs for the same valve split their own link equity and give a search engine two answers to the same question. The recommendation in the overview is to keep this page and redirect the other to it.


Hot Products


News
Ball Valves in A Kraft Pulp Mill: Black Liquor, Green Liquor And The Cost of Choosing The Alloy by Habit
White liquor at pH 14 cracks carbon steel welds, black liquor sets solid below 100 C, green liquor dregs grind seats: alloy choice and torque in a kraft mill.
Read More
Slug Flow And Ball Valves: What Actually Arrives At The Seat
A slug is liquid mass with momentum, not a pressure spike. What changes at the seat, in the cavity and at the actuator when liquid reaches a ball valve.
Read More
Ball Valves in Direct Lithium Extraction: PH 1 Eluate, Gypsum Scale And 438,000 Cycles in Twenty-Five Years
Direct lithium extraction swings valves from pH 1 eluate to pH 12 caustic, 48 column switches a day and gypsum scale. Materials, seats and torque.
Read More
Ball Valves in Geothermal Brine: Silica Scale, Chloride Cracking And The Cooling Trap
Why geothermal brine destroys ball valves: retrograde silica scale, calcite at the flash point, chloride cracking above 60 C and the 250 C seat limit.
Read More