


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q41F
-
J-VALVES
Overview of the J-VALVES 1 Inch 600LB F316 Stainless Steel High Pressure Floating Ball Valve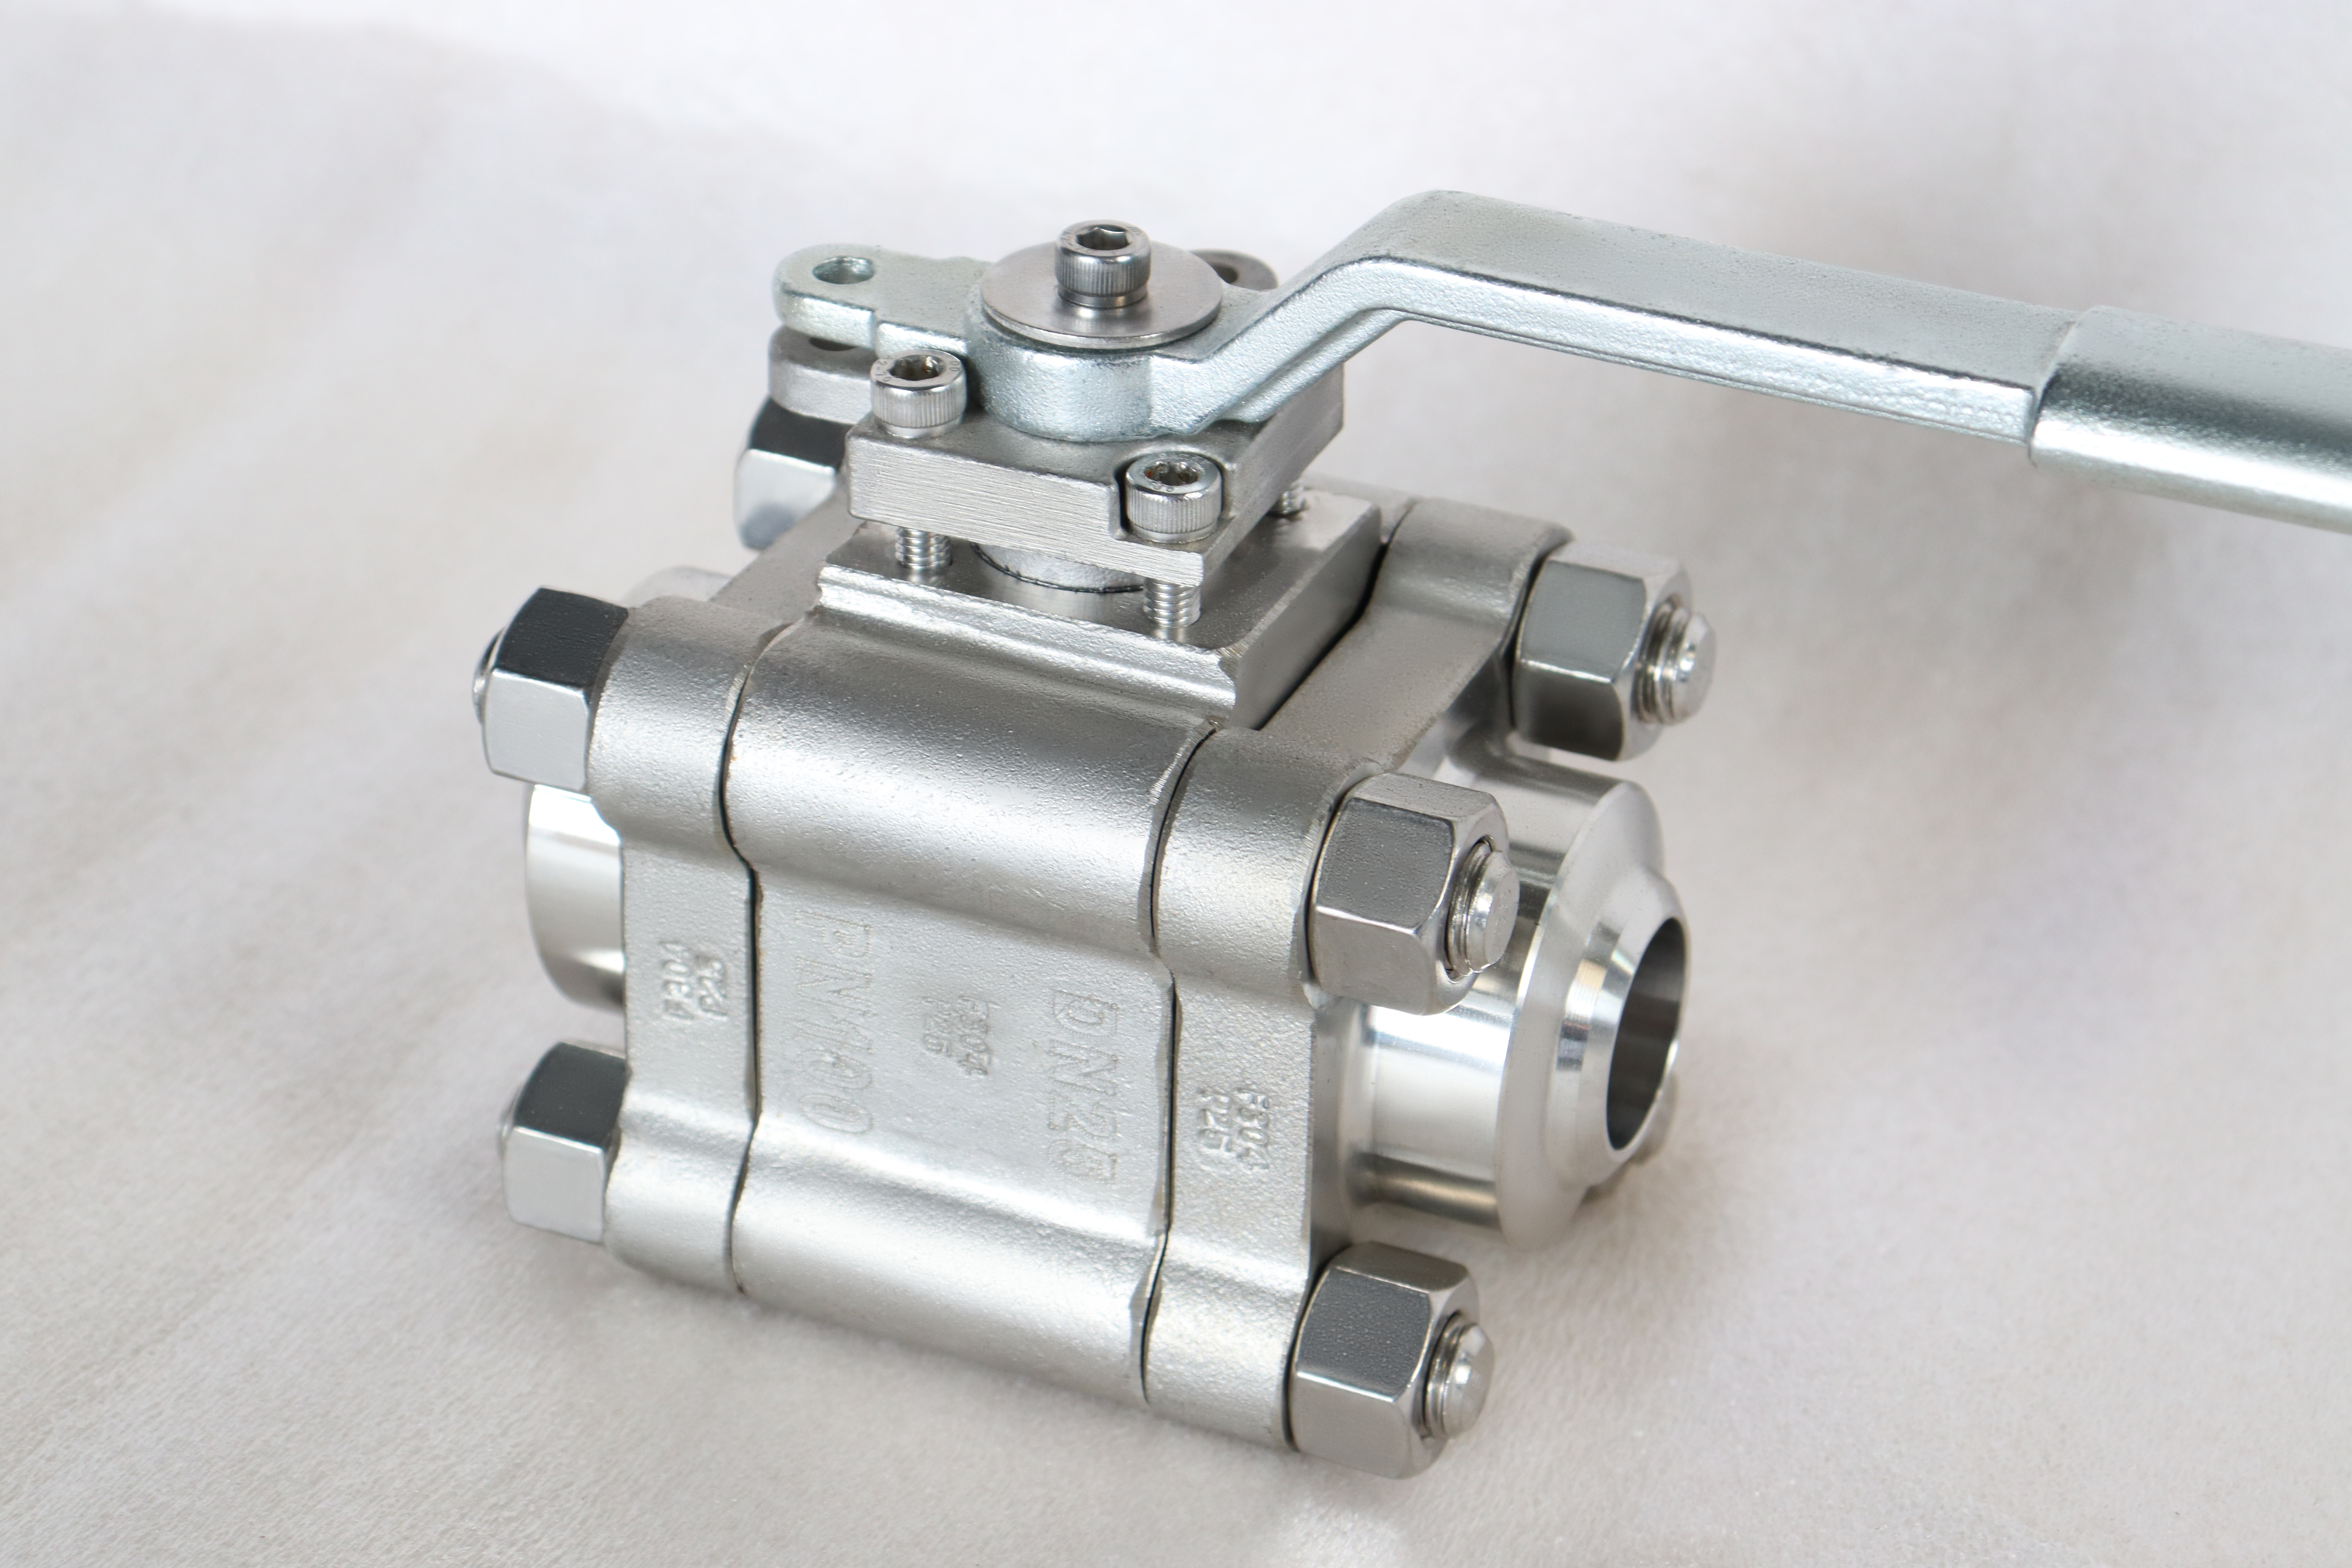
This is a one inch forged stainless valve at Class 600: DN25 bore, three piece body in A182 F316, a ball floating between two seat rings, and flanged ends. At this bore the wall required by the rating is far more than the pressure needs, so the valve is not a thin walled compromise; it is a small, stiff body that will hold the rating at temperature without argument.
The decision that actually shapes the product is the flange facing. The same valve is built with a raised face or with a ring joint groove, and those are two different valves rather than two finishes: the groove, the gasket, the stud length and the flange thickness all change. On a small high pressure line the ring joint is often the correct choice, and it is the one that gets ordered by mistake.
Design and Construction
Three pieces: a centre body carrying the ball, both seat rings and the stem, and two side bodies carrying the flanges. The joints are bolted and gasketed, and undoing one side body exposes a seat and the ball without disturbing the other seat. The ball floats, so the line pressure pushes it onto the downstream ring and the sealing force rises with the pressure. That short list of parts is the whole valve, and at this size all of them are accessible from the outside without cutting the line.
The stem comes up through the bonnet with a shoulder that stops it being blown out, and the packing sits above the stem seal in an adjustable gland. On a high pressure small bore valve the gland is a real maintenance point rather than a formality, because the stem is thin and the packing volume is small: a gland that is a quarter turn too tight will wear the stem, and one that is loose will weep at the first thermal cycle.

Material Options
The body is forged A182 F316, solution annealed and machined. F316 is the molybdenum bearing austenitic grade, and at this size it is chosen for the medium rather than for the pressure: chloride bearing water, chemical injection, sampling lines and process fluids that would pit a 304 body. The ball is F316 with hard chrome, or F316L where a softer ball is acceptable. Neither of those two grades is chosen for strength here, and that is the point on a valve this small.
The seat is the part that decides how far the valve can be pushed. PTFE and RPTFE cover the ordinary range, PPL takes it further, and PEEK or a metal seat is used where the temperature or the cycling demands it. Because the body has far more strength than the rating needs, the seat is almost always the limiting item on this valve, not the shell.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Body and side bodies | ASTM A182 F316 forged stainless, solution annealed | F316L, F304 | three pieces, two bolted joints |
| Ball | F316 with hard chrome plating | F316L, unplated | floats onto the downstream seat |
| Stem | 316 stainless | 17-4PH precipitation hardening | blowout proof shoulder, anti static |
| Seat | PTFE | RPTFE, PPL, PEEK, metal seat | the limiting item on this valve |
| Packing | PTFE | flexible graphite, braided | adjustable gland, replaceable in line |
| Body gasket | PTFE | spiral wound stainless | renewed at every opening |
| End connection | RF flanged to ASME B16.5 Class 600 | RTJ flanged with an R, RX or BX groove | the choice that defines the valve |
| Ring gasket where RTJ | ASME B16.20 metal ring | soft iron, low carbon steel, F316 | new ring at every opening |
| Operator | Lever with a locking hole | worm gear, pneumatic, electric | quarter turn, stops set |
Technical Specifications
The envelope is DN25, Class 600, three piece forged F316 body, full bore, flanged to ASME B16.5 at Class 600 with either a raised face or a ring joint groove, face to face to ASME B16.10, PTFE or PPL seat, lever with a locking hole, and testing to API 598. Class 600 corresponds to PN100 in the API 6D designation table. The table below is the declared envelope, and the drawing for the build ordered carries the actual dimensions.
The facing is the field that has to be stated and not assumed. A raised face takes a flat or spiral wound gasket and relies on the gasket being compressed by the studs; a ring joint takes a metal ring that sits in matching grooves in both flanges and seals on metal to metal contact. One facing cannot be converted into the other on site, because the groove is machined into the flange.
| Item | Value |
|---|---|
| Nominal bore | 1 inch (DN25) |
| Pressure class | Class 600 (PN100) |
| Body construction | three piece, two bolted joints |
| Body | ASTM A182 F316 forged stainless |
| Body options | F316L, F304 |
| Ball | F316 with hard chrome plating |
| Ball option | F316L |
| Stem | 316 stainless, blowout proof |
| Stem option | 17-4PH |
| Seat | PTFE |
| Seat options | RPTFE, PPL, PEEK, metal seat |
| Packing | PTFE, adjustable gland |
| Packing option | flexible graphite, braided |
| End connection | RF flanged to ASME B16.5 Class 600 |
| End option | RTJ flanged with an R, RX or BX groove |
| Ring gasket | ASME B16.20 metal ring, new at every opening |
| Facing conversion | not possible on site, the groove is machined in the flange |
| Face to face | ASME B16.10 for Class 600 at DN25 |
| Bore | full bore, DN25 |
| Operator | lever with a locking hole |
| Operator options | worm gear, pneumatic, electric |
| Design standard | ASME B16.34 and API 608 |
| Pressure test | API 598, shell 1.5 times, seat 1.1 times |
| Fire test | API 607 where ordered |
| Seat test direction | both, because the two seats are independent |
| Material certificate | EN 10204 3.1 per heat |
| Marking | size, class, body grade, heat number, facing |
| Temperature band | set by the seat compound first, then by the body grade |
| Pig passage | not applicable at DN25 |
| Joint reuse | ring joint needs a new ring each time the joint is opened |
Standards and Compliance
ASME B16.5 sets the flange dimensions and the facing, including the ring groove profile, and ASME B16.20 sets the ring joint gasket that goes into it. ASME B16.34 gives the wall and the rating, API 608 the ball valve requirements, ASME B16.10 the face to face, and API 598 the pressure test. Where a fire test is required it is API 607 on a soft seated valve of this kind.
The ring joint is the part of this standard set that is most often half understood. The ring is not a gasket in the usual sense: it is a metal ring that is deformed into the groove by the stud load, and it is used once. The groove has a tapered profile that has to be undamaged, and the ring has to match the groove type, because an R ring, an RX ring and a BX ring do not interchange even where the flange size is the same.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Pressure boundary | ASME B16.34 | wall thickness and rating, austenitic group |
| Ball valve requirements | API 608 | stem retention, marking, testing |
| Flanges and facing | ASME B16.5 | raised face or ring joint groove, Class 600 |
| Ring joint gaskets | ASME B16.20 | R, RX and BX rings, matched to the groove |
| Face to face | ASME B16.10 | for the size and class |
| Pressure testing | API 598 | shell at 1.5 times, seat at 1.1 times |
| Fire test where required | API 607 | on the soft seated build |
| Material certificate | EN 10204 3.1 | per heat, with the grade on the certificate |
Manufacturing Process
The forging is solution annealed and machined, with the bore, the seat pockets and the flange facing taken from common datums so that the seat sits square to the bore. Where a ring joint is ordered, the groove is machined after the facing and checked with a profile gauge rather than by eye, because the seal depends on the angle and the depth of that groove rather than on its surface finish.
The three parts are assembled on new gaskets, tested, and only then fitted with the lever. For a ring joint build the ring is not fitted at the works: the valve ships with the grooves protected and the rings supplied separately, because the ring belongs to the joint that will be made on site, and a ring that has been compressed once cannot be used again.

Quality Control and Testing
Every valve is shell tested at one and a half times its rating and seat tested at one point one times in both directions. On a floating valve the two seats are independent, so the test has to be run both ways: a valve tested from one side has proved one ring and nothing about the other, which is exactly the failure that shows up after installation when the line is back pressured from the other end.
The checks specific to this product are dimensional and material. The ring groove is checked for profile, depth and surface condition against the B16.5 table for the size and class; the flange facing is checked for flatness and finish; and the body and ball are confirmed as F316, since the two austenitic grades look identical and a certificate is only as good as the piece it is attached to.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| Forging | composition, mechanical properties, solution annealing record | 3.1 certificate against F316 |
| Machining | bore, seat pocket square to the bore, joint face flatness | drawing tolerance |
| Ring groove | profile, depth and surface condition | B16.5 table for the size and class |
| Raised face | flatness, finish, outside diameter | B16.5 for Class 600 |
| Ball and seat | sphericity, plating thickness, seat interference | checked with the ball in the pocket |
| Shell test | body and both joints at 1.5 times | API 598, no leak |
| Seat test | each seat in both directions at 1.1 times | API 598, no visible leak |
| Material identification | positive identification on body and ball | confirms F316 against the certificate |
| Packing and gland | ring count, gland setting, stem friction | adjusted after cycling |

Applications and Industry Service
The duty is isolation on small bore high pressure lines: chemical injection and dosing, sampling systems, instrument and impulse lines, high pressure water for cleaning and descaling, hydraulic supply lines, and the block valve on a small pressure reducing station. In most of those the valve is opened rarely and has to seal completely when it is closed. In almost all of those duties the valve is closed for long periods and opened for a few minutes, which is the opposite of the duty a control valve sees.
It is the wrong valve for a line that has to be pigged, for a medium that will attack F316, and for a service where the seat temperature is above what PTFE or PPL will hold. It is also the wrong valve where the joint will be broken often: a ring joint is a good seal and a poor convenience, because every opening needs a new ring and a careful look at the groove.

Installation, Operation and Maintenance
On a raised face joint, check that the gasket is the right size for the facing, align the flanges and draw the studs up in a cross pattern. On a ring joint, clean the grooves, check them for damage, fit a new ring, bring the flanges together without forcing them and tighten in a cross pattern in stages, because the ring has to be deformed evenly to seal. A ring that has been cocked in its groove will leak and cannot be re-used.
Never mix the two systems: a ring joint flange will not seal against a raised face flange with a flat gasket, and an adaptor that tries to bridge them adds joints that nobody has rated. Operate the valve a quarter turn, fully open or fully closed, and leave the lever locked where the valve must not be moved. A lever that has been used to force a stuck ball is the most common way a seat ring on a valve this size is destroyed.
How to Specify and Order
An order needs the size, the class, the body grade, the bore, the facing with the ring type where RTJ is chosen, the seat compound, the packing, the operator and the standard. A typical line reads: one inch, Class 600, body A182 F316, full bore, RTJ flanged to ASME B16.5 with R rings to B16.20, PPL seat, graphite packing, lever with a locking hole. Getting the facing wrong is the only mistake on this valve that cannot be corrected after delivery.
Two lines are worth adding. State the medium and the design temperature, because they decide between F316 and a higher alloy and between PTFE, PPL and PEEK. And state whether the joint will be opened during maintenance, because that decides between a ring joint that seals hardest and a raised face that comes apart easily, and it is the one choice on this valve that cannot be revisited later.
FAQ
Q: Should this valve be ordered with RF or RTJ flanges?
A: RTJ where the line is hydrocarbon, hydrogen, high pressure steam or anything where a leak is a hazard, and where the mating flanges are already ring joint. RF where the line is utility water, air or a general process line and the flanges are raised face. The choice belongs to the line, not to the valve, and it cannot be changed after the flange is machined.
Q: Can a ring joint valve be fitted to raised face flanges?
A: No. The ring sits in a groove and seals on metal to metal contact, so both flanges in the joint need the groove. An adaptor that tries to bridge the two adds joints that nobody has rated, and on a Class 600 line that is where the leak will be. Either change the valve or change the mating flange.
Q: Why is a ring joint used more often on small high pressure lines?
A: Because the joint is the weak point, not the pipe. At one inch the body is stiff and the wall is generous, while the flange is small and the stud load is concentrated. A metal ring that is deformed into a groove holds that joint better than a flat gasket, especially through thermal cycles, which is why instrument and injection lines at this class are usually ring joint.
Q: Is the ring gasket reusable?
A: No. The ring is deformed into the groove by the stud load and takes a set; a second make up will not seal the same way and may damage the groove. Every opening of the joint needs a new ring, and the groove is inspected before the new one goes in. That is the cost of the tighter joint and it should be in the maintenance plan.
Q: What is the difference between an R, an RX and a BX ring?
A: They are different ring geometries for different groove profiles and pressure ranges, set out in ASME B16.20. They do not interchange even when the flange size is the same, so the ring type has to be stated on the order along with the facing, and it has to match the groove that is actually machined in the mating flange.
Q: Does the pressure class make this valve high pressure?
A: It makes it rated for it. Class 600 corresponds to PN100 in the API 6D table, and at one inch the wall required is far more than the pressure needs, so the shell is not the constraint. What limits the valve is the seat compound and the joint, which is why those two are the fields worth arguing about on this size.


Hot Products


News
Ball Valves in A Kraft Pulp Mill: Black Liquor, Green Liquor And The Cost of Choosing The Alloy by Habit
White liquor at pH 14 cracks carbon steel welds, black liquor sets solid below 100 C, green liquor dregs grind seats: alloy choice and torque in a kraft mill.
Read More
Slug Flow And Ball Valves: What Actually Arrives At The Seat
A slug is liquid mass with momentum, not a pressure spike. What changes at the seat, in the cavity and at the actuator when liquid reaches a ball valve.
Read More
Ball Valves in Direct Lithium Extraction: PH 1 Eluate, Gypsum Scale And 438,000 Cycles in Twenty-Five Years
Direct lithium extraction swings valves from pH 1 eluate to pH 12 caustic, 48 column switches a day and gypsum scale. Materials, seats and torque.
Read More
Ball Valves in Geothermal Brine: Silica Scale, Chloride Cracking And The Cooling Trap
Why geothermal brine destroys ball valves: retrograde silica scale, calcite at the flash point, chloride cracking above 60 C and the 250 C seat limit.
Read More