


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q61F
-
J-VALVES
Overview of the J-VALVES PN100 F304 Three Piece Floating Ball Valve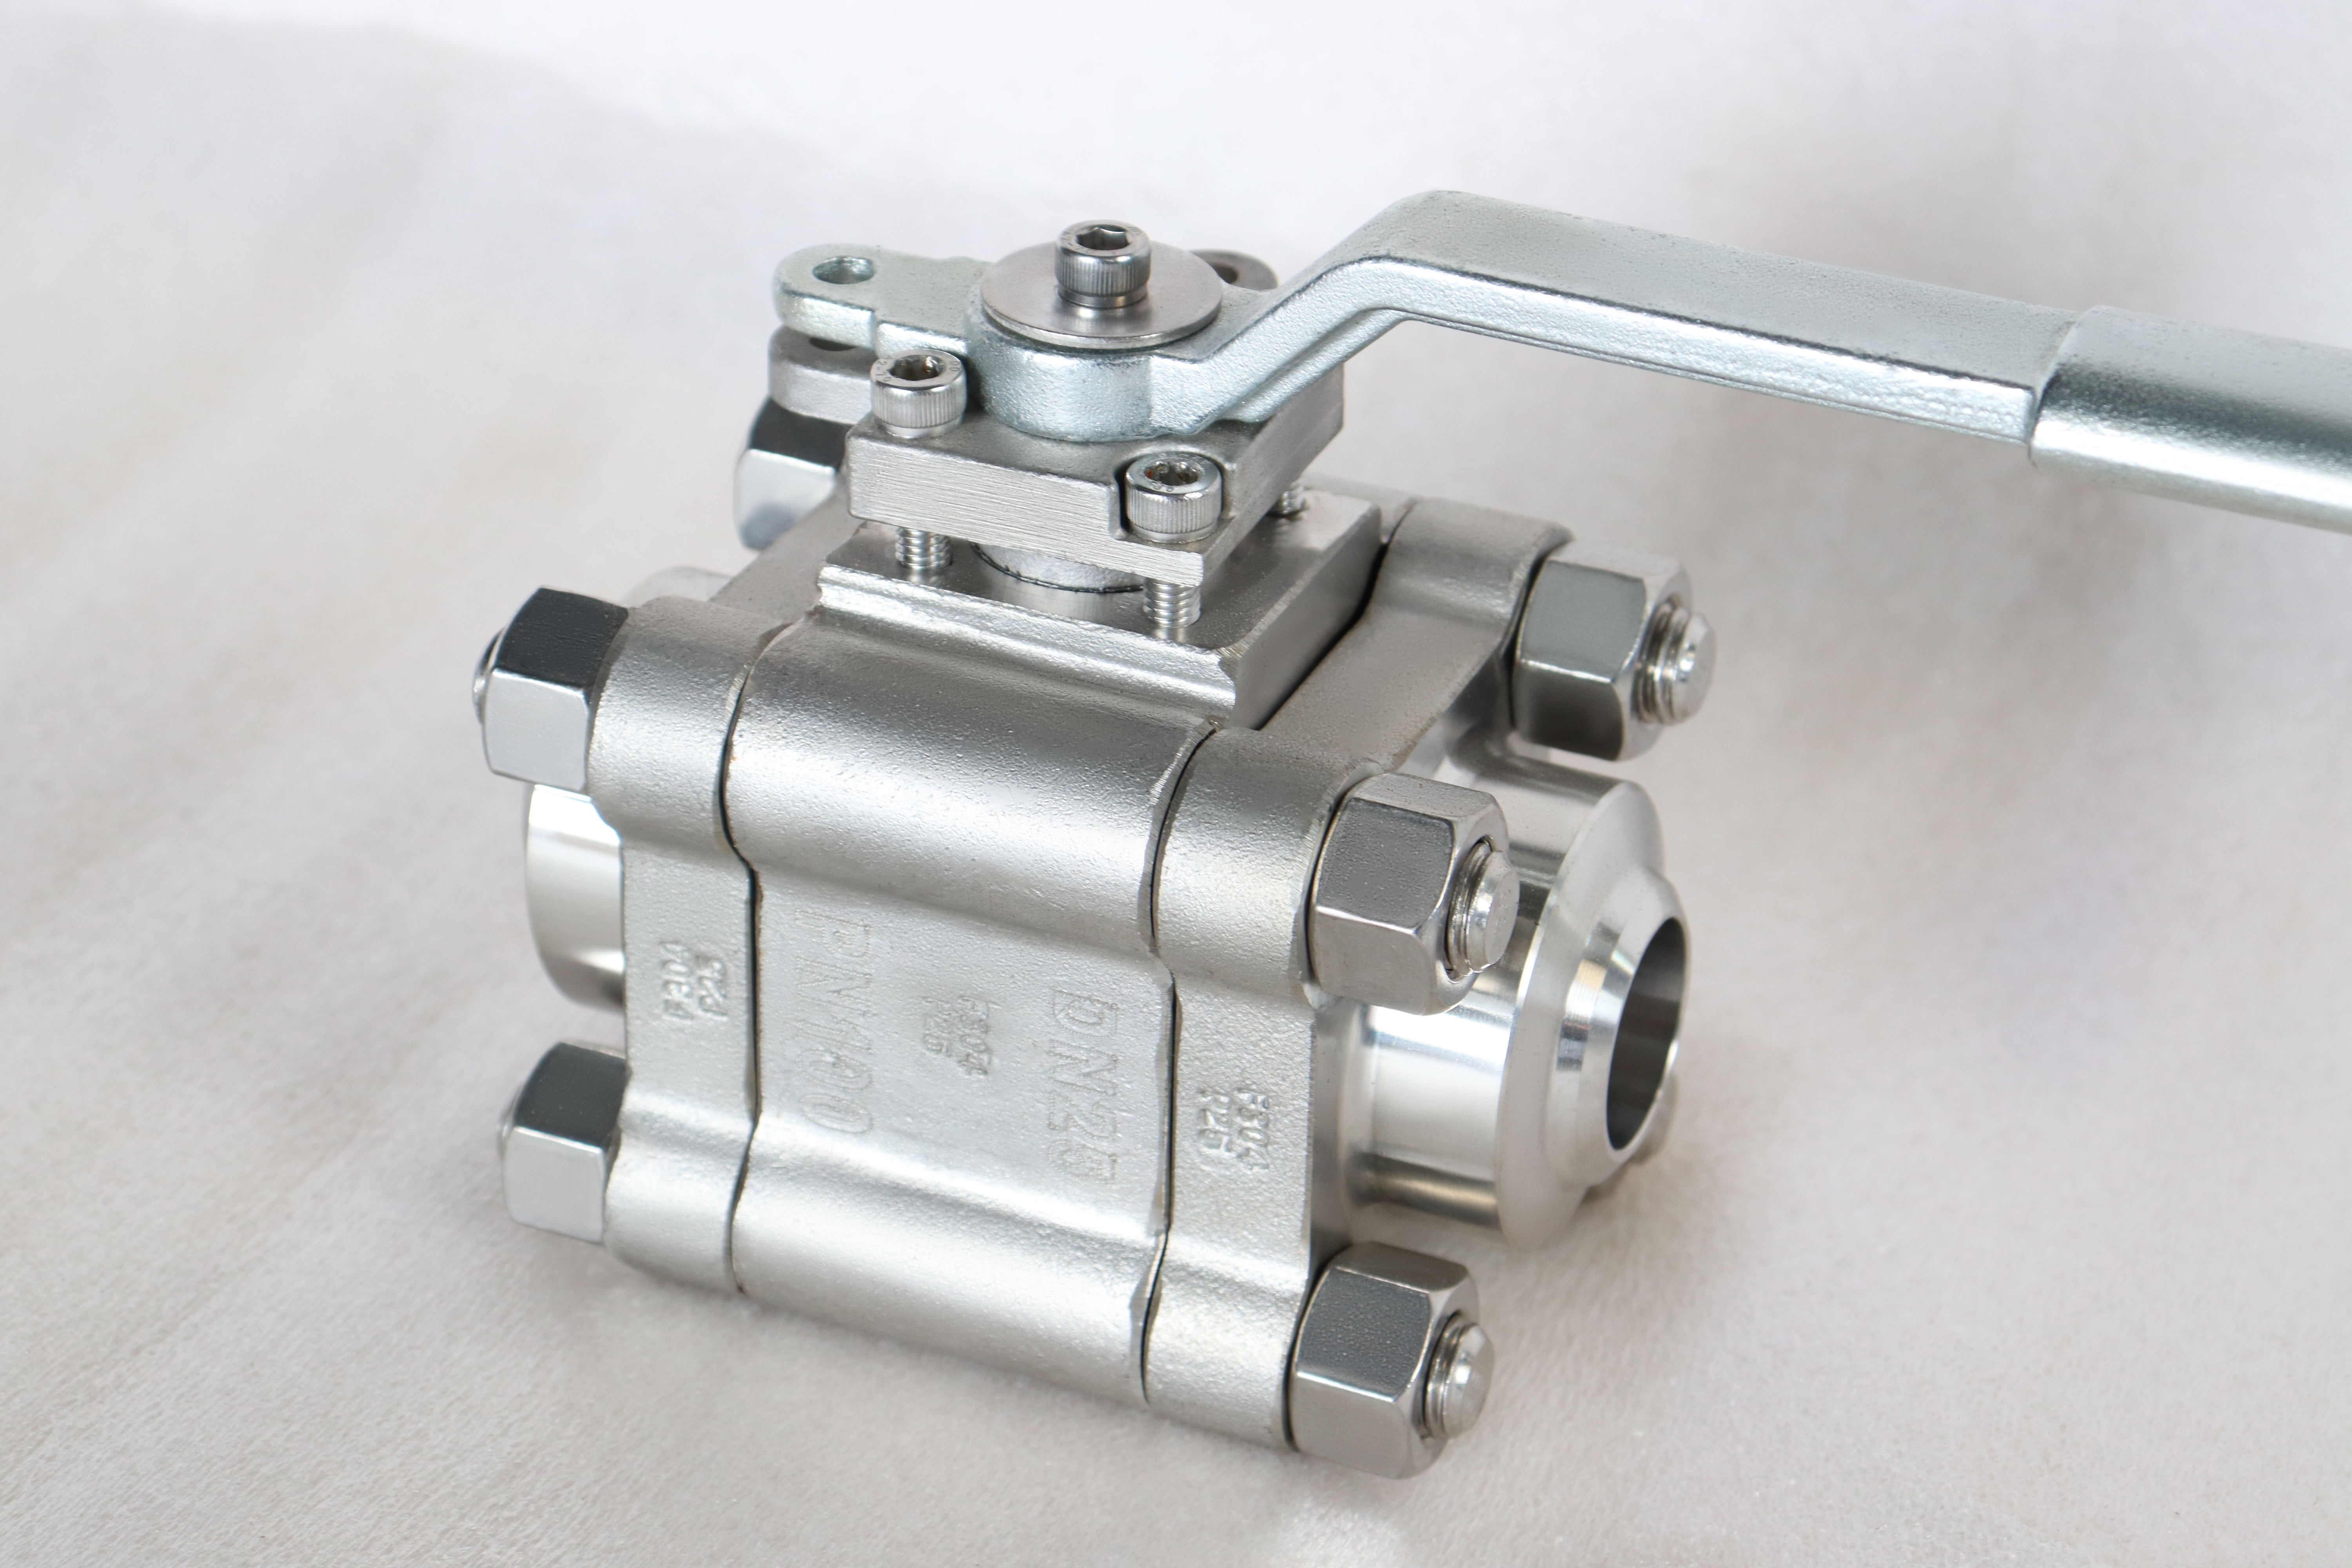
This is a one inch isolation valve built the way small bore, high pressure lines are actually built: a three piece stainless body, a floating ball, a full port bore, and threaded ends. The body in the photographs carries three lines of marking — DN25, PN100, and a grade that begins SS3 — and a lot number that ties the casting or forging to its material certificate. The centre section holds the ball and both seats; two end caps clamp onto it on four through-bolts; the whole assembly comes apart on the bench in a few minutes. That is the pattern, and everything else on this page follows from it.
The pressure number needs one sentence of translation, because two different values hide behind it. PN 100 is the European nominal designation, and API 6D clause 7.2 pairs it with Class 600 in its table of metric equivalents, so a valve marked PN100 is a Class 600 valve in American terms. At 38 degrees C, however, Class 600 does not have a single rating: the carbon steel group carries 102.1 bar, while the austenitic stainless group — the group a 304 or 316 body sits in — carries 99.3 bar, which is 1440 psi. The nameplate says 100, the ASME table says 99.3 bar for this material, and the gap is small enough to be ignored in a water line and large enough to matter in a specification review. Both numbers belong in the enquiry.
Why this valve floats instead of riding on trunnions is a question of area, not of fashion. In a floating design the line pressure pushes the whole ball downstream until it presses into the downstream seat, and that seat is what seals. The force on the seat is the pressure multiplied by the area it acts on, and that area grows with the square of the bore. Going from one inch to two inches multiplies it by four; going to four inches multiplies it by sixteen. At DN25 in Class 600 the load is still something a seat ring and a lever can handle. At DN100 in the same class it is not, which is why the same catalogue lists a trunnion valve at that size and this page does not.
The end connection is where the original page and its own photographs part company, and it is worth settling first because half the specification follows from it. The text block describes raised face or ring joint flanges to EN 1092-1 and ASME B16.5, with face-to-face dimensions to ASME B16.10. The valve in all five photographs has female threaded ends — the thread is visible inside the bore in the end view and in both three-quarter views. A flanged build of a three piece stainless valve exists and is a different product; it cannot be described with the same sentence, because a flange has a bolt circle to check and a thread does not. This page describes the threaded valve, and the flange discussion belongs to the sister page.
Put together, the valve suits instrument isolation, chemical injection points, sample connections, small bore steam and water drops, and skid packages where a one inch line has to be shut off positively and taken apart for cleaning. It does not suit a buried line, a pigged line, or any duty where a double block and bleed certificate is required, and the sections below say why in each case rather than leaving it to the reader.
Design and Construction
The body is split twice. Two end caps, one at each end, clamp against a centre section, and four long bolts pass the full width of the assembly with nuts on the far side. Everything that wears is inside the centre section: the ball, the two seat rings, the seat springs, and the stem passage. Take the four nuts off and the centre section lifts out with the ball and seats still inside it, leaving both end caps screwed onto their pipe ends. That is the practical difference between this pattern and a two piece body, and on a threaded valve it is a larger difference than it sounds, because breaking a pipe thread destroys the sealant on it and re-making it is a small job that nobody wants to do twice.
The ball is not carried on trunnions here. It sits between the two seat rings with a small amount of freedom, and it is the line pressure that decides where it sits. With the valve closed and pressure on the upstream side, the ball is pushed downstream until it bears on the downstream seat; the upstream seat is unloaded by the same movement. That is the whole sealing mechanism, and it explains two behaviours that catch people out. First, the valve seals harder as the pressure rises, because the pressure is what generates the seat load. Second, the operating torque also rises with pressure, because the same load that seals the seat is the load the ball has to slide against when it turns — which is why the torque for this valve is measured on the assembled unit rather than tabulated from a catalogue.
The stem is a separate part, not an extension of the ball. It passes through the centre section, is retained by the body so that it cannot blow out under pressure, and drives the ball on a square or flattened end. Above the body there is a mounting pad with four tapped holes — the pattern an actuator bracket or a gearbox bolts to — and the stem end stands proud of it so that the drive can be coupled. The packing sits in the body around the stem, compressed by a gland, and on this size it is replaceable with the valve in place and the line isolated. None of that is visible from the outside except the pad, and the pad is the reason this valve can be automated later without being replaced.
Two details on the photographs are worth pointing at, because they are what a buyer checks first. The four body bolts are through-bolts with nuts, not tapped holes in the centre section, so a stripped thread means a new bolt rather than a new body. And the bore is full port: the ball opening is the same size as the pipe bore, which gives a straight-through flow path with nothing to collect solids.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Body, end caps, centre section | ASTM A182 F304 forged stainless steel | ASTM A182 F316 for chloride or marine duty | Grade as declared on the data sheet; confirm against the EN 10204 3.1 certificate before release |
| Ball | F304 with hard chromium plating | F304L, or 316 ball for corrosive media | Plating thickness belongs on the drawing, not on a catalogue line |
| Stem | 304 stainless steel | 316 stainless steel | Anti-blowout retention is a body feature, not a stem option |
| Seat rings | RPTFE | PTFE, PPL, PEEK, or metal seat for high pressure and high temperature | The seat sets the real temperature limit of the valve |
| Stem packing | PTFE | Flexible graphite; ISO 15848 low emission arrangement | Low emission is a tested arrangement, not a packing brand |
| Body bolts | Alloy steel stud and nut | Stainless steel for corrosive atmospheres | Torque to the signed drawing; four bolts, cross pattern |
| End threads | ASME B1.20.1 NPT | ISO 7-1 Rc or Rp (BSP), ISO 228-1 G parallel | Thread standard is cut at machining; it cannot be changed later |
Material Options
The body is declared as ASTM A182 F304, which is a forged austenitic stainless steel, and the photographs are consistent with a forged body: flat machined faces, a machined boss around each port, and sharp edges that a casting would not have. What the photographs cannot settle is the grade itself. The marking on the body reads DN25, PN100 and a material line beginning SS3, and the third line is partly covered by the watermark, so 304 and 316 cannot be told apart from the image at this resolution; both are 300 series austenitic stainless and both are legitimate for this body. That is not a technicality, because the same product photograph appears on a page selling the same valve in F316, and both grades cannot be right for one photograph. The grade is settled by the EN 10204 3.1 certificate and by nothing else, and the enquiry should ask for it.
Between 304 and 316 the difference that matters is molybdenum. F304 contains none; F316 carries two to three percent, and that addition is what raises the resistance to pitting and crevice attack in chloride bearing water. For dry gas, oil, steam, and clean water at moderate chloride levels, 304 is the economical answer and has been for decades. For seawater, brine, chlorine dosing, or any stream where chlorides concentrate on a hot surface, 316 is the correct choice and 304 is a corrosion test that the customer pays for. The site has a sister page on chloride duty that goes further into the alloy selection; the point here is that the choice is a line item on the enquiry, not an assumption.
The letter L is worth one paragraph because it is so often ordered for the wrong reason. F304L is the low carbon variant, and its purpose is to prevent carbide precipitation in the heat affected zone of a weld. This valve's ends are threaded, so nothing on it is welded — the L buys nothing at all on a screwed valve. It becomes relevant only on the welding-end build of the same body, or when the customer's own specification applies a low carbon rule across a project regardless of joint type. Ordering 304L because it sounds safer adds cost and delivers no benefit on this end connection, and a supplier who lets that pass without saying so is not doing the buyer a favour.
The ball is F304 with hard chromium plating as standard, and the plating is what actually runs against the seat. A plated carbon steel ball is common in larger sizes but is the wrong answer in a stainless body that may see corrosive media, so this valve keeps a stainless ball. The option list offers F304L and a 316 ball; the choice matters where the medium is aggressive enough to attack the ball through a plating defect, which is a real failure mode on plating that has been damaged in assembly. Chromium thickness is a drawing value, not a catalogue value, and it is the number that decides how long the ball lasts.
Stems are 304 by default and 316 as the upgrade, and the practical reason to specify 316 is the same as for the body: a stem that pits in a chloride stream becomes a leak path at the packing, which is the one place on a small valve where a failure is both sudden and dangerous. Seat compounds are where the honest conversation happens, because the seat is the softest part in the pressure boundary. RPTFE is the standard; PPL and PEEK extend the temperature range; a metal seat is available for the top of the range and for abrasive service. Whatever the seat is made of, that material — not the body — sets the temperature limit of the assembled valve, and the seat supplier's data sheet is where the number lives. A page that prints one temperature range for the whole product is describing the body and calling it the valve.
Technical Specifications
The table below is the specification a purchaser can hold the supplier to. It contains only values that come from the nameplate, from the customer's data sheet, or from a standard that lists them; dimensions that depend on the build — face to face, end to end, bore tolerance, weight — are on the signed drawing, because they change with the end connection and the seat choice and a catalogue number for them would be a guess with a decimal point.
| Item | Value |
|---|---|
| Size | DN25 (1 inch), full port |
| Pressure designation | PN 100 on the body; Class 600 in ASME terms per API 6D clause 7.2 |
| Rating at 38 degrees C, austenitic body | 99.3 bar (1440 psi) per ASME B16.34 Table 2, 300 series group |
| Rating at 38 degrees C, carbon steel comparison | 102.1 bar (1480 psi), quoted only to show why the two are not interchangeable |
| Body material | ASTM A182 F304 forged stainless steel, as declared |
| End connection | Threaded, female; NPT per ASME B1.20.1 or BSP per ISO 7-1, to be stated on the order |
| Thread size at DN25 | 1 inch nominal: 11.5 threads per inch at 60 degrees for NPT, 11 threads per inch at 55 degrees for BSP |
| Body construction | Three piece, four through-bolts, centre section removable in line |
| Ball support | Floating, seat supported, full port |
| Temperature range, body material | ASME B16.34 group 2.1 lists -425 to 1000 degrees F (-254 to 538 degrees C); above 538 degrees C only with carbon 0.04 percent or higher |
| Temperature range, assembled valve | Set by the seat compound and the packing, from their data sheets, not by the body rating |
| Face to face | On the signed drawing for the end connection ordered |
| Top mounting | ISO 5211 pad, four tapped holes, stem drive above the pad |
| Testing | API 598, shell at 1.5 times the rating and seat at 1.1 times |
| Certificate | EN 10204 3.1, heat number matched to the body marking |
Two lines in that table carry more weight than the rest. The first is the rating line, because 99.3 bar is not a number most data sheets print and it is the number an auditor will find if they open B16.34 at Class 600 and read across to the austenitic group. A page that claims 102.1 bar for a stainless valve is quoting the carbon steel row, which is a common and quiet error. The second is the thread line, because it is the only interface on this valve that can be got wrong invisibly, and the next paragraph explains why.
A one inch NPT thread and a one inch BSP thread are the same nominal size, taper at the same 1 in 16, and are within 0.15 mm of each other on major diameter — 33.4 mm against 33.25 mm. They will start to engage by hand. What separates them is the thread count and the flank angle: NPT runs 11.5 threads per inch on a 60 degree American form with flattened crests, and BSP runs 11 threads per inch on a 55 degree Whitworth form with rounded crests. Half a thread per inch and five degrees of flank is enough that the joint binds within about two turns, and no amount of PTFE tape corrects a five degree mismatch — the tape fills a spiral gap, it does not reshape a flank. This is the threaded equivalent of a flange drilled to the wrong bolt circle, except that a wrong flange is visible across the workshop and a wrong thread looks correct until it leaks.
Standards and Compliance
Four documents do the work on this valve, and each answers a different question. ASME B16.34 gives the wall thickness and the pressure temperature table, which is where 99.3 bar at 38 degrees C comes from, and it is the document that decides whether the body is thick enough for Class 600. API 608 is the product standard: it covers metal ball valves with flanged, butt-welding, socket-welding and threaded ends, it applies to floating as well as trunnion designs, and it establishes additional requirements for valves that already conform to B16.34. API 598 is the test. ASME B1.20.1 is the thread, unless the order says ISO 7-1.
The scope of API 608 is worth knowing precisely, because it is the standard most often cited loosely. For threaded ends it covers sizes DN 8 through DN 50, which is NPS 1/4 through NPS 2, in Classes 150, 300, 600 and 800. A DN25 Class 600 threaded valve sits inside that envelope with room on both sides, which is a stronger statement than "designed to API 608" and a much stronger one than a page that cites the standard without saying which clause of its scope the product meets. For flanged ends the same standard runs to DN 600 in Classes 150, 300 and 600, which is why the flanged sister product is also covered — but by a different part of the same scope.
Two further points follow from that scope. API 608 works in classes, not in PN designations: there is no PN 100 in it, and the class the standard rates this valve against is Class 600. That does not make the nameplate wrong — PN 100 is a legitimate European designation and API 6D clause 7.2 pairs the two — but it does mean that a requisition written in PN has to be translated into a class before any American standard applies to it. And the standard's own normative references include ASME B1.20.1, so the thread requirement is not an extra the supplier invents; it comes attached to the product standard.
Fire safety and emissions are separate qualifications, not automatic ones. API 607, technically identical in method to ISO 10497, is a type test performed on a representative valve: the valve is burned and then must still seal. It is not a test performed on every unit, and a claim of fire safe design without a certificate number is a claim about intent. ISO 15848 governs fugitive emissions and is a tested stem arrangement rather than a packing brand, so it is either ordered and certified or it is not claimed. For sour service, NACE MR0175 with its identical twin ISO 15156 governs the material, and it brings hardness limits that have to be carried into the trim specification; the current designation supersedes the older MR-01-75 that still appears on many data sheets.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Body design and pressure rating | ASME B16.34, Standard Class | Wall thickness and rating to Class 600; 99.3 bar at 38 degrees C for the austenitic body |
| Product standard | API 608 | Floating ball valve, threaded ends, DN 25, Class 600, inside the threaded-end scope of DN 8 to DN 50 and Class 150 to 800 |
| Threads | ASME B1.20.1 NPT, or ISO 7-1 Rc and Rp on request | Thread cut to the standard named on the order; gauge checked before dispatch |
| Pressure and seat test | API 598 | Shell at 1.5 times the rating, seat at 1.1 times, every unit, recorded |
| Fire test | API 607 / ISO 10497 | Type tested design; certificate number on request |
| Fugitive emissions | ISO 15848 | Available as a tested stem arrangement when ordered |
| Sour service | NACE MR0175 / ISO 15156 | Trim and hardness to the standard when the line carries wet H2S |
| Material certificate | EN 10204 3.1 | Heat number matched to the body marking and to the certificate |
Manufacturing Process
The body starts as forged bar or a forged blank in A182 F304. Forging is the reason this valve can hold Class 600 in a one inch wall: a forging has no porosity to hide a leak path, and the grain flow follows the shape rather than being cast into it. The blank is machined on all faces, the bore is drilled and bored to the ball seat, and the seat pockets are cut to take the seat rings and their springs. The two end caps are machined from the same stock, and their threads are cut or rolled at this stage — rolling is preferred on stainless because it cold works the root of the thread and leaves a stronger thread than cutting does, though both are acceptable.
The centre section is the part that has to be right. Its two faces must be flat and parallel within the tolerance on the drawing, because the body seals on those faces against the end caps; a centre section that is out of parallel will leak at one side no matter how hard the bolts are pulled. The ball is ground and then plated, the plating is inspected for porosity, and the ball is matched to the seats by lapping or by selective assembly rather than by assumption. The stem bore is machined square to the ball axis, because a stem that leans puts a side load on the packing and shortens its life.
Assembly is where the torque discipline shows. The ball goes into the centre section, the seats and springs follow, the stem is inserted from inside so that its shoulder sits behind the body material that retains it, the packing and gland go on, and the two end caps are brought up with the four through-bolts. Those bolts are tightened in a cross pattern in two or three passes to the value on the drawing, not to feel. On a three piece body the bolt tension is the only thing holding the joint closed, and an uneven pattern distorts the centre section enough to be measurable at the seat.
The last step before test is marking. The body carries the size, the pressure designation, the material and a lot or heat number, and the heat number is what makes the certificate useful: without it, a 3.1 certificate is a piece of paper describing somebody's steel. The marking in the photographs shows DN25, PN100, the material line and a number of that type, which is the correct set. Painting, if any, comes after marking and never over it.

Quality Control and Testing
Every unit gets a shell test and a seat test to API 598, and both are recorded against the serial number. The shell test is at 1.5 times the rated pressure with the valve partially open, and it looks for leakage through the body wall or the body joint — on a three piece valve the joint between the centre section and the end caps is the place to watch, because it is the only pressure boundary that is bolted rather than solid. The seat test is at 1.1 times the rating, applied to one side at a time with the valve closed, and it measures leakage past the seat. A valve that passes the shell test and fails the seat test is a valve with a damaged seat or a ball that is out of round, and neither is fixable by tightening anything.
Thread inspection is the step that small bore valves most often skip and most need. A thread gauge is a go and no-go pair: the go gauge must enter the full thread length by hand, and the no-go gauge must not enter more than the permitted number of turns. An NPT gauge will not accept a BSP thread and a BSP gauge will not accept an NPT thread, which makes the gauge the only reliable way to catch a mixed batch — a mixed batch that will otherwise be discovered by a fitter on site, holding a valve that starts to thread and then stops. On an order where the customer has specified NPT, the gauge used at final inspection should be an NPT gauge, and the record should say so.
Material verification sits alongside the dimensional work. The heat number on the body is matched to the 3.1 certificate, and the certificate is checked for the grade, the chemical composition and the mechanical properties. Where the customer's specification calls for it, the ball plating thickness is measured rather than assumed, and the stem is hardness tested if the service is sour. None of this is exotic; all of it is the difference between a valve that is what the drawing says and a valve that looks like it.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| Incoming material | Heat number, grade, certificate | EN 10204 3.1 matched to the body marking |
| Body machining | Wall thickness, face flatness and parallelism of the centre section | Drawing dimensions and tolerance |
| Ball and plating | Sphericity, plating thickness, plating porosity | Drawing and plating specification |
| Thread | Go and no-go gauge, full engagement by hand | ASME B1.20.1 or ISO 7-1, as ordered |
| Assembly | Bolt torque in cross pattern, two or three passes | Torque value on the signed drawing |
| Shell test | Body wall and body joint, valve partially open | API 598, 1.5 times the rating, no leakage |
| Seat test | Leakage past each seat, one side at a time | API 598, 1.1 times the rating |
| Final | Marking, packing, certificate pack | Marking complete before painting; documents with the valve |

Applications and Industry Service
The natural home for this valve is the one inch line that has to be shut off and proved shut: an instrument impulse line, a pressure transmitter isolation, a gauge root valve, a sample point, a chemical injection branch. These are lines where the pressure can be high, the bore is small, and the consequence of a passing valve is a wrong reading or an unplanned dose rather than a spill — and they are exactly the lines where a three piece body earns its keep, because the valve can be taken apart and cleaned when the medium crystallises or polymerises.
Chemical and pharmaceutical service is the second group. A 304 or 316 body with a PTFE or RPTFE seat and a full port bore has no pocket for product to sit in, and the centre section comes out for inspection without disturbing the pipe. Where the medium is aggressive, the ball plating and the seat compound matter more than the body grade, and that is the conversation to have at enquiry rather than after delivery. Where the medium is chloride bearing, 316 replaces 304, and where the line runs hot, PPL or PEEK replaces RPTFE.
Steam and hot water on small bore drops is the third. Here the limiting component is the seat, and a valve ordered with an RPTFE seat for a line that runs above what that compound will take will fail at the seat rather than at the body. The honest way to specify is to give the temperature and the medium, and let the seat compound be selected against them, rather than to order the standard build and hope.
Three duties this valve should not be sold into. It is not a buried valve: there is no extended stem or bonnet on this pattern, and the operator has to reach the lever. It is not a pigged line valve: at DN25 there is nothing to pig, and a pig would not pass the body cavity even at full port. And it is not a double block and bleed valve in the sense that a specification usually means: double block and bleed is not available on this size, because the body has no drain port between the seats — the cavity can be isolated by two seats, but there is no way to bleed it and prove that both are holding. A page that claims DBB for this valve is describing a trunnion valve with a drain plug, not this one.
Installation, Operation and Maintenance
The thread is the joint, so the thread is the installation. Clean both threads, apply sealant to the male thread only, and use the right sealant: PTFE tape wound in the direction of tightening for general service, an anaerobic thread sealant where vibration or temperature rules out tape. Leave the first thread bare so that no tape enters the line. Then tighten by the flats with a wrench on the valve body hex, not by the lever, and not by the pipe — a valve used as a wrench to pull a pipe into alignment is a valve with a distorted body and a seat that will not seal. If the pipe does not line up, fix the pipe.
Support is worth a sentence because threaded joints are less forgiving than flanges. A small valve hanging on two threaded connections with unsupported pipe either side puts bending into the body joint, and the body joint is where a three piece valve leaks. Support the pipe close to the valve on both sides, and do not use the valve to carry the weight of a fitting or a hose.
Operation is a quarter turn, and the lever has a travel stop so that the quarter turn is unambiguous. The valve is not a control valve: it is designed to be fully open or fully closed, and throttling it puts the seat and the ball edge in the flow path where erosion works fastest. Where the line needs modulation, that is a different product. Where the valve is to be automated, the ISO 5211 pad takes a bracket and the stem takes a coupler; the pad size, the stem dimensions and the required torque are the three things the actuator supplier needs, and the torque has to be measured on the valve rather than taken from a table.
Maintenance is the reason to buy three piece. Isolate the line, drain it, take off the four nuts, and lift the centre section out with the ball and seats inside; the end caps stay on the pipe, so no thread is broken and no pipe is moved. Replace the seats, the body gaskets and the stem packing as a set, check the ball for plating damage, and reassemble to the same torque in the same cross pattern. Do not reuse a body gasket: it has already taken a set, and a second compression will not restore it. If the valve has been in a dirty service, clean the cavity before reassembly, because the cavity is where debris collects and where it will hold the ball off its seat.
How to Specify and Order
An enquiry for this valve needs eight lines, and a supplier who receives them can quote without guessing. Size and bore: DN25, full port, or state reduced bore if that is what the line needs. Pressure: PN 100, or Class 600, and say which one the specification is written in so that no translation happens twice. Material: body grade and ball and stem grades, if the project specifies them. End connection: NPT or BSP, and which variant — Rc, Rp or G — because a one inch thread is not one thread. Seat compound: PTFE, RPTFE, PPL, PEEK or metal, against a stated temperature and medium. Operation: lever, or actuator with the pad size and torque. Testing and documents: API 598 by default, 3.1 certificate, and whether a third party witness is required. And marking: what has to appear on the body, if the customer's own specification governs it.
Three of those lines are the ones that go wrong most often. The thread is first, because "one inch" is not a specification and a valve threaded to the wrong standard cannot be fixed in the warehouse. The seat compound is second, because it is the part that sets the temperature limit and the part most often left to the supplier's default. The grade is third, and on this valve it has an extra reason to be stated: the body marking reads SS3, the page declares A182 F304, and the same photograph is used on a sister page selling F316. One of those two pages is describing a valve the photograph does not show. The certificate settles it, and it is cheaper to settle it at enquiry than at installation.
What J-VALVES supplies with the valve is a documentation pack rather than a promise: the 3.1 certificate matched to the heat number on the body, the test records for shell and seat, the thread standard as ordered, and the drawing that carries the dimensions that this page deliberately does not print. Where a customer needs a witnessed test, a fire certificate copy, an ISO 15848 report or a NACE compliance statement, those are ordered with the valve, not requested afterwards, because each one attaches to a specific unit and a specific heat.
FAQ
Q: Is PN 100 the same as Class 600?
A: As a designation, yes; as a number at 38 degrees C, not quite. API 6D clause 7.2 pairs Class 600 with PN 100 in its table of metric equivalents, so a valve marked PN100 is a Class 600 valve in American terms, and PN 100 means a nominal 100 bar in European terms. The ASME rating for Class 600 at 38 degrees C is 102.1 bar for carbon steel, but this body is austenitic stainless, and the same table gives that group 99.3 bar, which is 1440 psi. So the nameplate says 100, the ASME table says 99.3 for this material, and the European nominal says 100 as well. The three numbers are within one percent of each other and only the ASME one is a calculated allowable, which is why it is the one to quote in a specification review.
Q: The photographs show threaded ends, but the specification on the page says flanged. Which is it?
A: Threaded, on the valve photographed. The end view shows the thread cut inside the bore, and both three-quarter views show it at one end and the protective cap at the other. A flanged build of the same three piece body exists and is a separate product with a separate page, and the two cannot share one sentence: a flange is defined by a bolt circle and a hole size that a purchaser checks with a tape, while a thread is defined by a pitch and a flank angle that only a gauge confirms. A page that describes flanges for a threaded valve sends the buyer to measure something that is not there.
Q: What thread is on it, and can I put an NPT valve into a BSP line?
A: No. Both are one inch nominal and both taper at 1 in 16, and they are within 0.15 mm of each other on major diameter, which is why they start to engage by hand and feel right for a turn and a half. One inch NPT is 11.5 threads per inch on a 60 degree American form with flattened crests; one inch BSP is 11 threads per inch on a 55 degree Whitworth form with rounded crests. Half a thread per inch and five degrees of flank is enough to bind the joint within about two turns, and PTFE tape cannot correct it, because tape fills a spiral gap and does not reshape a flank. Specify NPT or BSP, and say which BSP variant if it is BSP, on the order.
Q: Why is this valve floating, and at what size does it have to become trunnion?
A: Because the load is still small enough for the seat to carry it. In a floating design the line pressure pushes the whole ball into the downstream seat, and the force on that seat is the pressure times the area it acts on. That area grows with the square of the bore, so a two inch valve sees four times the load of a one inch valve in the same class and a four inch valve sees sixteen times. At DN25 in Class 600 the seat and the lever handle it comfortably, and the design stays simple. At DN100 in the same class the same arithmetic sends the ball onto trunnions, which is why the catalogue lists a different product at that size rather than a bigger version of this one.
Q: Can an actuator be fitted, and why are there no torque figures?
A: The ISO 5211 pad on top takes a bracket and the stem end takes a coupler, so the valve can be automated without being replaced. What the actuator supplier needs is the pad size, the stem dimensions and the torque, and the third one is not printed here because it is not a property of the size: it follows the seat compound, the differential pressure, the temperature and the safety factor in the purchaser's own specification. A table value would be a guess with a decimal point, and a guess that is too low produces an actuator that will not seat the valve. The figure is measured on the built valve and issued with the signed drawing, together with the fail position the order asks for.
Q: What is the real temperature limit of this valve?
A: Two limits, and the lower one governs. The body material sits in group 2.1 of ASME B16.34, which lists a service range from minus 425 to 1000 degrees Fahrenheit, that is minus 254 to 538 degrees C, with the top of that range available only when the carbon content is 0.04 percent or higher. That is the body. The valve is limited by the seat, because a thermoplastic seat cannot be sold against the top of the body range, and PPL, PEEK or a metal seat is what moves the limit up. The minus 29 to 425 degrees C that appears on carbon steel data sheets is a group 1.1 range and has no business on a stainless valve: it is too narrow at both ends.


Hot Products


News
Ball Valves in A Kraft Pulp Mill: Black Liquor, Green Liquor And The Cost of Choosing The Alloy by Habit
White liquor at pH 14 cracks carbon steel welds, black liquor sets solid below 100 C, green liquor dregs grind seats: alloy choice and torque in a kraft mill.
Read More
Slug Flow And Ball Valves: What Actually Arrives At The Seat
A slug is liquid mass with momentum, not a pressure spike. What changes at the seat, in the cavity and at the actuator when liquid reaches a ball valve.
Read More
Ball Valves in Direct Lithium Extraction: PH 1 Eluate, Gypsum Scale And 438,000 Cycles in Twenty-Five Years
Direct lithium extraction swings valves from pH 1 eluate to pH 12 caustic, 48 column switches a day and gypsum scale. Materials, seats and torque.
Read More
Ball Valves in Geothermal Brine: Silica Scale, Chloride Cracking And The Cooling Trap
Why geothermal brine destroys ball valves: retrograde silica scale, calcite at the flash point, chloride cracking above 60 C and the 250 C seat limit.
Read More