


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q41F
-
J-VALVES
Overview of the J-VALVES DN50x40 1500LB F44 Two Piece Extended Stem Floating Ball Valve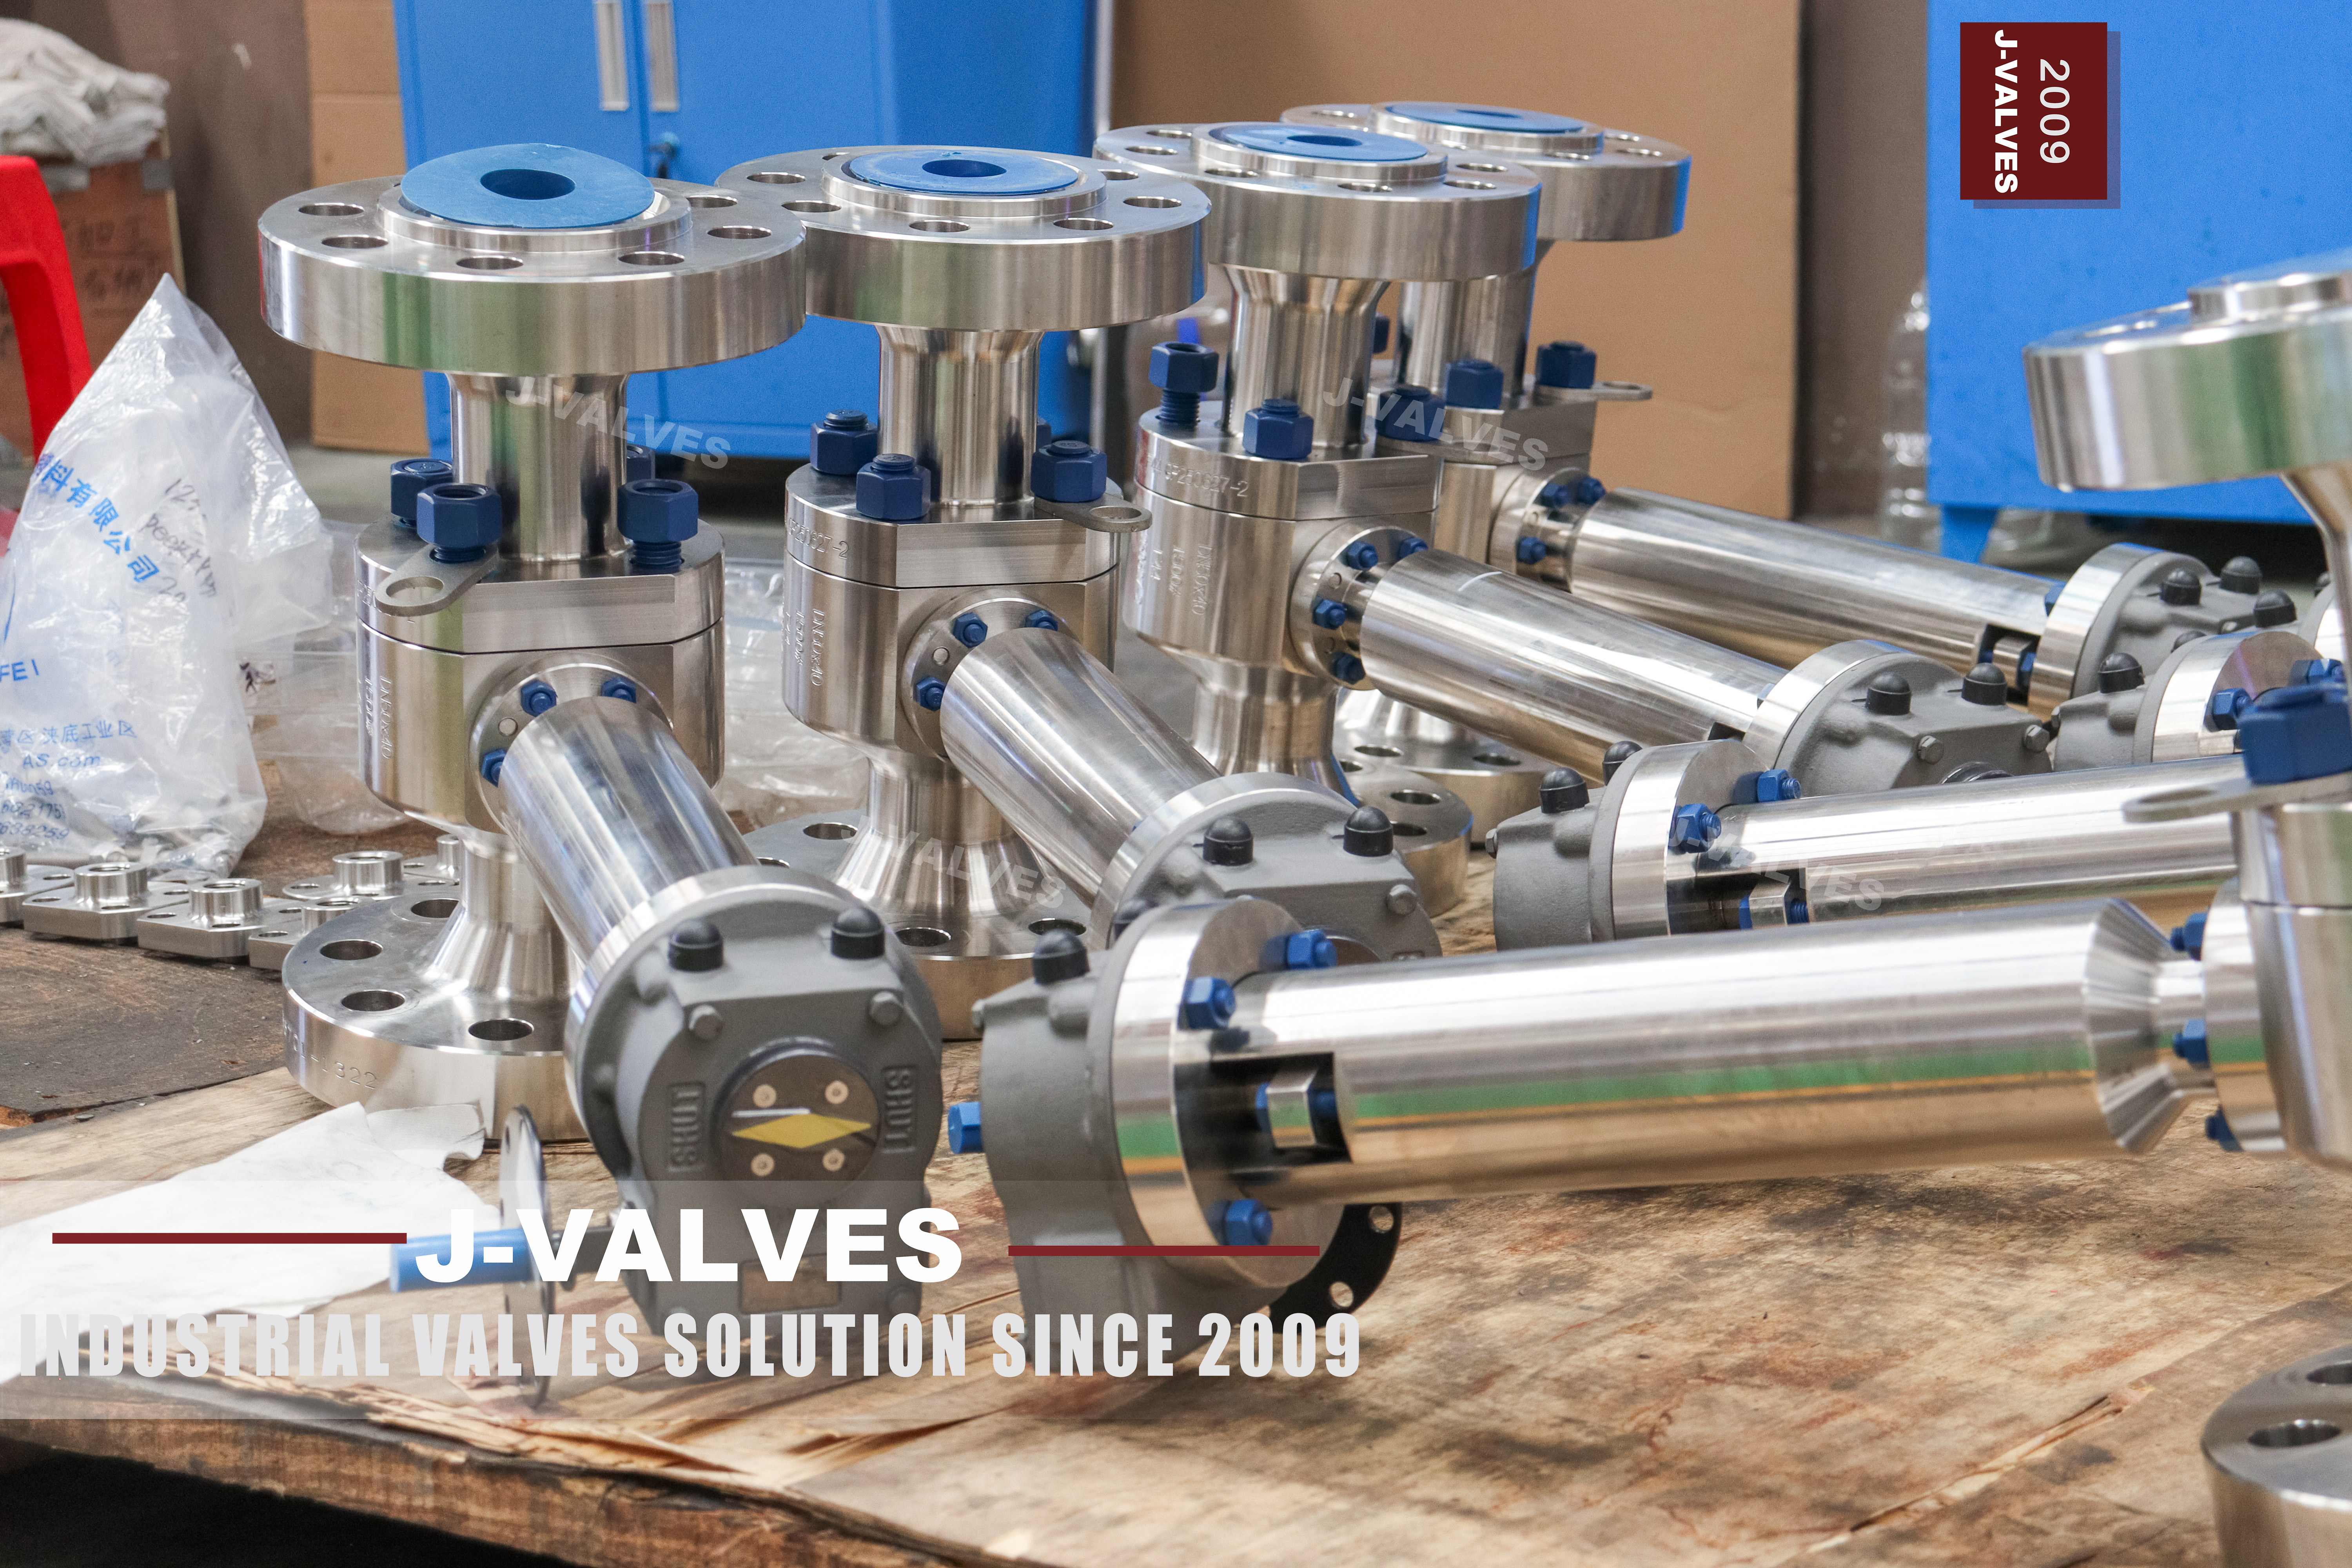
The valve is small and the class is not. Two inch ring joint ends, a one and a half inch bore, and a Class 1500 rating put this in the group where the flange is the heaviest part of the assembly and the bolting is doing more work than its size suggests. That combination is what makes the fasteners the interesting part of the order rather than an afterthought, and it is the reason this page is about the joint rather than about the alloy.
The page lists the fasteners as either the body alloy or a matching alloy steel. Those are two different valves in service even though they are identical on the drawing, because one fails by galling when it is tightened and the other fails by corrosion when it is not. Both failures happen at the same place, which is the joint that has to be opened every time the body is serviced, and that is the joint this page is about.
Design and Construction
Two body halves, one bolted joint, and on this valve that joint carries a Class 1500 load with a ring joint gasket between the faces. A ring joint gasket seals on metal to metal contact in a groove, which means the faces have to be parallel and the studs have to be tightened evenly; it does not forgive the way a soft sheet gasket does. The joint is also the route into the body, so it is opened for every seat change rather than only in an emergency.
The ball floats, and at this class the seat load is high enough that the seat compound and the surface finish matter more than they do on a low pressure valve. The bore is reduced to DN40 inside a DN50 body, which keeps the ball and the seat rings small enough to stay hand operable. The extended stem puts the lever where the operator can reach it and leaves everything else, including the joint described above, at the pipe.
Material Options
The body is forged super austenitic stainless, and the page names the F44 catalogue code. The alloy family is what matters for selection: it is bought for chloride bearing, acidic and strongly oxidising media at pressure, not for strength, because at Class 1500 a plain stainless forging would carry the pressure perfectly well. The composition and the heat treatment record sit on the mill certificate behind the 3.1 documentation, and the code on the nameplate is what the order should match.
Trim follows the body. The ball is the same alloy with hard chrome plating or a nitriding treatment, the stem is the body alloy or 17-4PH, and the seats are RPTFE, PEEK or PPL, with a hardfaced metal seat available as a different design for higher temperature. The fasteners are the line that matters here: either the body alloy or an alloy steel, and the order has to say which, because the two have different assembly behaviour and different external corrosion behaviour.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Body and side body | forged super austenitic stainless, code as stamped | the F44 catalogue code | two pieces, one bolted joint |
| Ball | body alloy with hard chrome or nitriding | as ordered | ground, then treated |
| Stem | body alloy | 17-4PH | packing stays in the body |
| Seat | RPTFE | PEEK or PPL | sets the service temperature |
| Metal seat | hardfaced, a different design | judged on leakage rate | not an upgrade to the soft seat |
| Fasteners | body alloy | matching alloy steel | galling or external corrosion, pick one |
| Ends | ring joint to ASME B16.5 | Class 1500 only | ring gasket is single use |
Technical Specifications
Ends are ring joint to ASME B16.5 at Class 1500, and that is a specification with consequences rather than a facing choice: the groove is machined into the flange, the gasket is a metal ring, and the stud length is set by the ring rather than by a sheet gasket compressed between flat faces. The pressure class is written as Class 1500 throughout this page, which is the same rating the metric system calls PN 250; the number 260 sometimes printed beside it is not a rating in either standard.
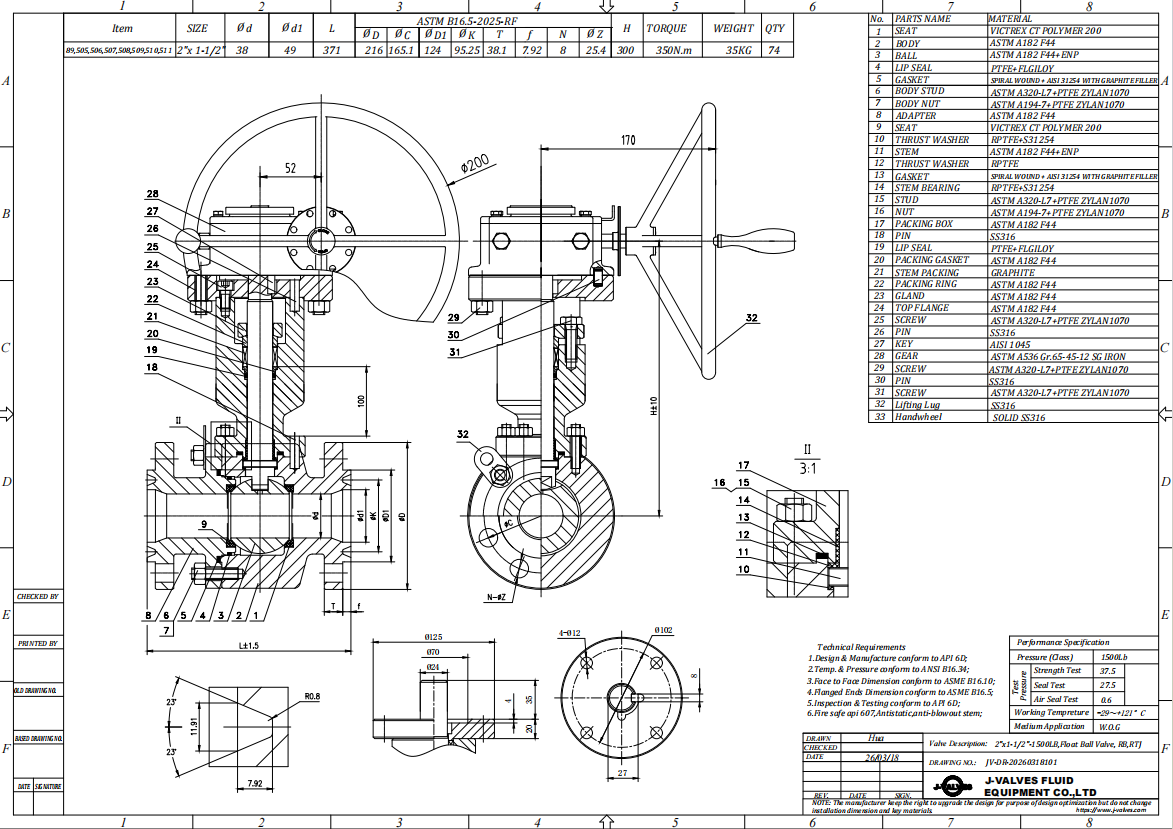
Face to face is held to ASME B16.10 for a flanged valve of this size and class, and the bore is DN40 in a DN50 body, so pressure drop is calculated on the bore rather than on the flange. Neither dimension is printed here as a number, because the number belongs to the standard table, and anything that depends on the build, such as overall height with a particular extension, is dimensioned on the signed general arrangement drawing for the size and trim ordered.
| Item | Value |
|---|---|
| Nominal size | DN50x40 (2x1.5 inch, DN50 flanged ends and DN40 bore) |
| Pressure class | Class 1500 (PN 250) |
| Body style | two piece, one bolted joint |
| Ball support | floating, no trunnion |
| Bore | reduced bore, DN40 |
| Body material | forged super austenitic stainless, catalogue code as stamped |
| Ball material | body alloy with hard chrome plating or nitriding |
| Stem | body alloy or 17-4PH |
| Seat | RPTFE, PEEK or PPL; hardfaced metal seat as a different design |
| Packing | high density flexible graphite |
| Fasteners | body alloy or matching alloy steel, stated on the order |
| End connection | ring joint flange, ASME B16.5 Class 1500 |
| Ring gasket | single use, replaced at every opening |
| Face to face | dimension on the signed GA drawing, held to ASME B16.10 |
| Design standard | ASME B16.34 and API 608 |
| Test standard | API 598 shell and seat test |
| Test pressure | shell 1.5 times and seat 1.1 times the class rating |
| Temperature range | minus 29 to plus 425 Celsius, metal temperature |
| Temperature limit | set by the seat compound, not by the body |
| Galling risk | austenitic fasteners under high preload, treated before assembly |
| Extended stem length | 300 mm to 1200 mm typical, set by the service |
| Operation | lever, low torque; gear, pneumatic, electric or hydraulic optional |
| Fire test | not claimed on this page, API 607 to be specified if required |
| Anti static device | not claimed on this page |
| Documentation | EN 10204 3.1 on request |
| Weight | quoted with the drawing for the size and trim ordered |
| Country of manufacture | China |
Standards and Compliance
B16.34 supplies the wall and the rating, and at Class 1500 both are doing real work rather than sitting on a minimum, which is the opposite of the situation at Class 150. API 608 adds the quarter turn requirements and API 598 supplies the test multipliers. What none of the three covers is the pair of questions that decide whether this valve opens cleanly in five years: whether the fasteners will gall while they are being tightened, and whether the ring groove will still be true when a new ring goes in.
No fire test is claimed for this valve on the page and no anti static device is described. That matters at Class 1500 in hydrocarbon service, where a soft seated valve is commonly required to hold a fire test of the API 607 type before acceptance, and where that test qualifies a design rather than a unit. The ring joint facing has its own standard for groove dimensions and ring profile, but that standard says nothing about how the joint behaves after it has been opened and rebuilt twice, which is a matter of procedure rather than of certificate.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Pressure boundary | ASME B16.34 | minimum wall and the rating for the alloy group at Class 1500 |
| Ball valve design | API 608 | the quarter turn requirements for this product |
| Shell and seat test | API 598 | 1.5 times the rating for the shell, 1.1 times for the seat |
| Flange facing | ASME B16.5 Class 1500 | ring joint groove and ring gasket |
| Face to face | ASME B16.10 | flanged valve length for the size and class |
| Ring gasket | ASME B16.20 ring dimensions | single use, replaced at every opening |
| Fire test | not claimed on this page | API 607 named on the order if required |
| Documentation | EN 10204 3.1 | issued against the heat number on request |
Manufacturing Process
Forged blanks are machined in one setup where the shape allows, so the bore, the seat pockets and the ring groove stay concentric and square to each other. On a ring joint valve the groove is the feature that punishes bad machining: a groove that is not square to the stud circle loads the ring unevenly and the joint leaks at pressure even though every component measured in tolerance on its own.
Assembly is dry and clean, and the body joint is drawn to a controlled torque with the ring in place so the metal to metal contact is even all round. Where the fasteners are the body alloy, the threads are treated against galling before assembly, because two austenitic surfaces under high preload will pick up and seize. The extension is fitted afterwards and the coupling set so the stem turns without side load on the gland.

Quality Control and Testing
The shell test here is also the first assembly check of the ring joint. With the ring in its groove and the studs at torque, a groove that is out of square or a ring of the wrong profile shows up as a weep at the joint rather than as a seat problem three months later. The seat test follows with the valve cycled between directions, and it is the one that catches a seat ring lapped too proud. Neither test says anything about the second assembly.
Two things the bench does not settle. The alloy is settled by the mill certificate and, where the order asks for it, by positive material identification on the finished body, which matters more here than on a carbon steel valve because the difference between two austenitic grades cannot be seen. The ring groove condition is settled by inspection and by the joint being rebuilt correctly after the first service, which is a site activity rather than a factory one.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| Incoming forgings | grade, heat number, wall thickness | certificate against the stamped code |
| Machining | bore, seat pocket depth, ring groove squareness | in process gauging against the drawing |
| Groove inspection | dents, brinelling, surface finish | checked before the ring is fitted |
| Assembly | seat crush both sides, joint torque | controlled torque with the ring in place |
| Shell test | no leakage through the body wall or the ring joint | API 598 at 1.5 times the rating |
| Seat test | no visible leakage, both directions | API 598 at 1.1 times the rating |
| Fasteners | grade, thread condition, anti seize where specified | checked against the order line |

Applications and Industry Service
This valve is bought for high pressure lines carrying something that would eat a plain stainless body. That covers chloride bearing process water, brine and seawater duty on the low flow branches, acids and oxidising media, and the injection or sampling points where DN50 pipe runs at Class 1500. The extended stem is a separate decision: it puts the lever outside insulation or above a pit while the body and the ring joint stay at the pipe.
It is the wrong valve in three situations. A medium that needs a higher alloy will not be saved by this one, which is resistant to a specific list rather than universal. A line that must be pigged cannot use a reduced bore body. And a service above the seat ceiling will deform the seat long before the body is in trouble, since the printed range describes the metal and the seat has its own much lower limit.

Installation, Operation and Maintenance
The first installation is the easy one and the second is where the cost sits. Ring gasket replacement is not optional: the ring takes a permanent set in the groove, and a joint rebuilt with the old one will weep, and that weep then gets read as a seat problem. The groove is inspected for dents and brinelling before a new ring goes in, and the studs are examined for stretched threads rather than reused on the assumption that they were fine last time. None of that appears in a shell and seat certificate.
Where the fasteners are the body alloy, they gall: the threads pick up during tightening and the stud either seizes before torque is reached or releases with damaged threads. Anti seize treatment on assembly and a controlled tightening sequence are what prevent it, and both belong on the order if the joint is expected to be opened more than once. Alloy steel studs avoid the galling and move the problem outside, where external corrosion decides.
How to Specify and Order
The order line needs the size as flange by bore, the class, the body alloy code as it will be stamped, the seat compound, the end facing and the extension length with its datum. Two more belong on it for this valve: the fastener material, and whether anti seize treatment and a tightening procedure are required. Those two lines are what separate a joint that opens cleanly in five years from one that has to be cut out.
Two lines are usually left off an order for this valve and both are cheap to add. The first is the number of ring gaskets, because the gasket is a single use item and a valve that will be serviced twice needs three of them rather than one. The second is the fastener material with its anti seize requirement, since that decides whether the joint opens cleanly or has to be cut out. The nameplate, the certificate and the drawing should still agree, but they will agree about a valve that cannot be taken apart.
FAQ
Q: Why does the bolting matter so much on this valve?
A: Because it is the only part that can be supplied in either the body alloy or an alloy steel, and the two fail differently. Austenitic fasteners under Class 1500 preload will gall, so the threads pick up during tightening and the stud either seizes or releases damaged. Alloy steel fasteners avoid that and instead corrode externally. Both failures land on the joint that has to be opened for every service.
Q: Can the ring joint gasket be reused?
A: No. A ring joint gasket seals on metal to metal contact and takes a permanent set in the groove, so it is replaced every time the joint is opened. The groove itself is inspected for dents and brinelling before a new ring goes in, because a damaged groove will leak with a new ring too. A joint rebuilt with the old ring will weep and the weep is usually misread as a seat problem.
Q: What does the F44 code mean and can it be cross referenced?
A: It is a catalogue code stamped on the nameplate, not a designation that can be converted into another system by looking it up. The alloy family is super austenitic stainless, bought for chloride bearing and oxidising media at pressure. The chemical composition and the heat treatment record are on the mill certificate behind the 3.1 documentation, and that certificate is what an order should be matched against.
Q: Is the pressure class PN 250 or PN 260?
A: Class 1500 corresponds to PN 250, which is the designation used both in the API 6D pressure code list and in the European flange standard. The figure 260 printed on some catalogue pages is not a rating in either system, and an enquiry written against PN 260 will not match a flange schedule. This page uses Class 1500 throughout.
Q: Does the extended stem move the pressure boundary?
A: No. The packing and the stem seal stay in the body, and the extension is a mechanical link to the handle. On this valve that matters because the ring joint and the bolted body joint stay at the pipe while the operator stands somewhere else. Insulating or burying the body does not protect the joint; it only makes it harder to reach when it needs rebuilding.
Q: Why are there other pages for this same valve?
A: Because it has been listed more than once and the earlier pages were written around different questions. This page takes the bolting and the rebuild question only. One listing should be kept as the indexed page and the others redirected to it, since several URLs for one valve split their own link equity and give a search engine several answers to the same question.


Hot Products


News
Ball Valves in Geothermal Brine: Silica Scale, Chloride Cracking And The Cooling Trap
Why geothermal brine destroys ball valves: retrograde silica scale, calcite at the flash point, chloride cracking above 60 C and the 250 C seat limit.
Read More
Ball Valve Face To Face Dimensions: Why A Correctly Ordered Replacement Still Does Not Fit
A 6 inch Class 150 ball valve can be 267 or 305 mm face to face and both are compliant. How B16.10, EN 558 and flange drilling decide whether it fits.
Read More
Ball Valve Stem Key And Keyway: What Gives Way First, And What The Handle Cannot Tell You
Between the handle and the ball there are four fits. Which one shears, which one cracks, and how a few degrees of lost motion hides a valve that never seated.
Read More
Ball Valve Datasheet: Six Blocks That Decide Whether Two Quotes Are Comparable
A ball valve datasheet only works when six blocks are fixed: pressure basis, bore, temperature ceiling, test, end connection, operator. How each is written.
Read More