


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q41F
-
J-VALVES
Overview of the J-VALVES 1 Inch PN100 F304 Floating Ball Valve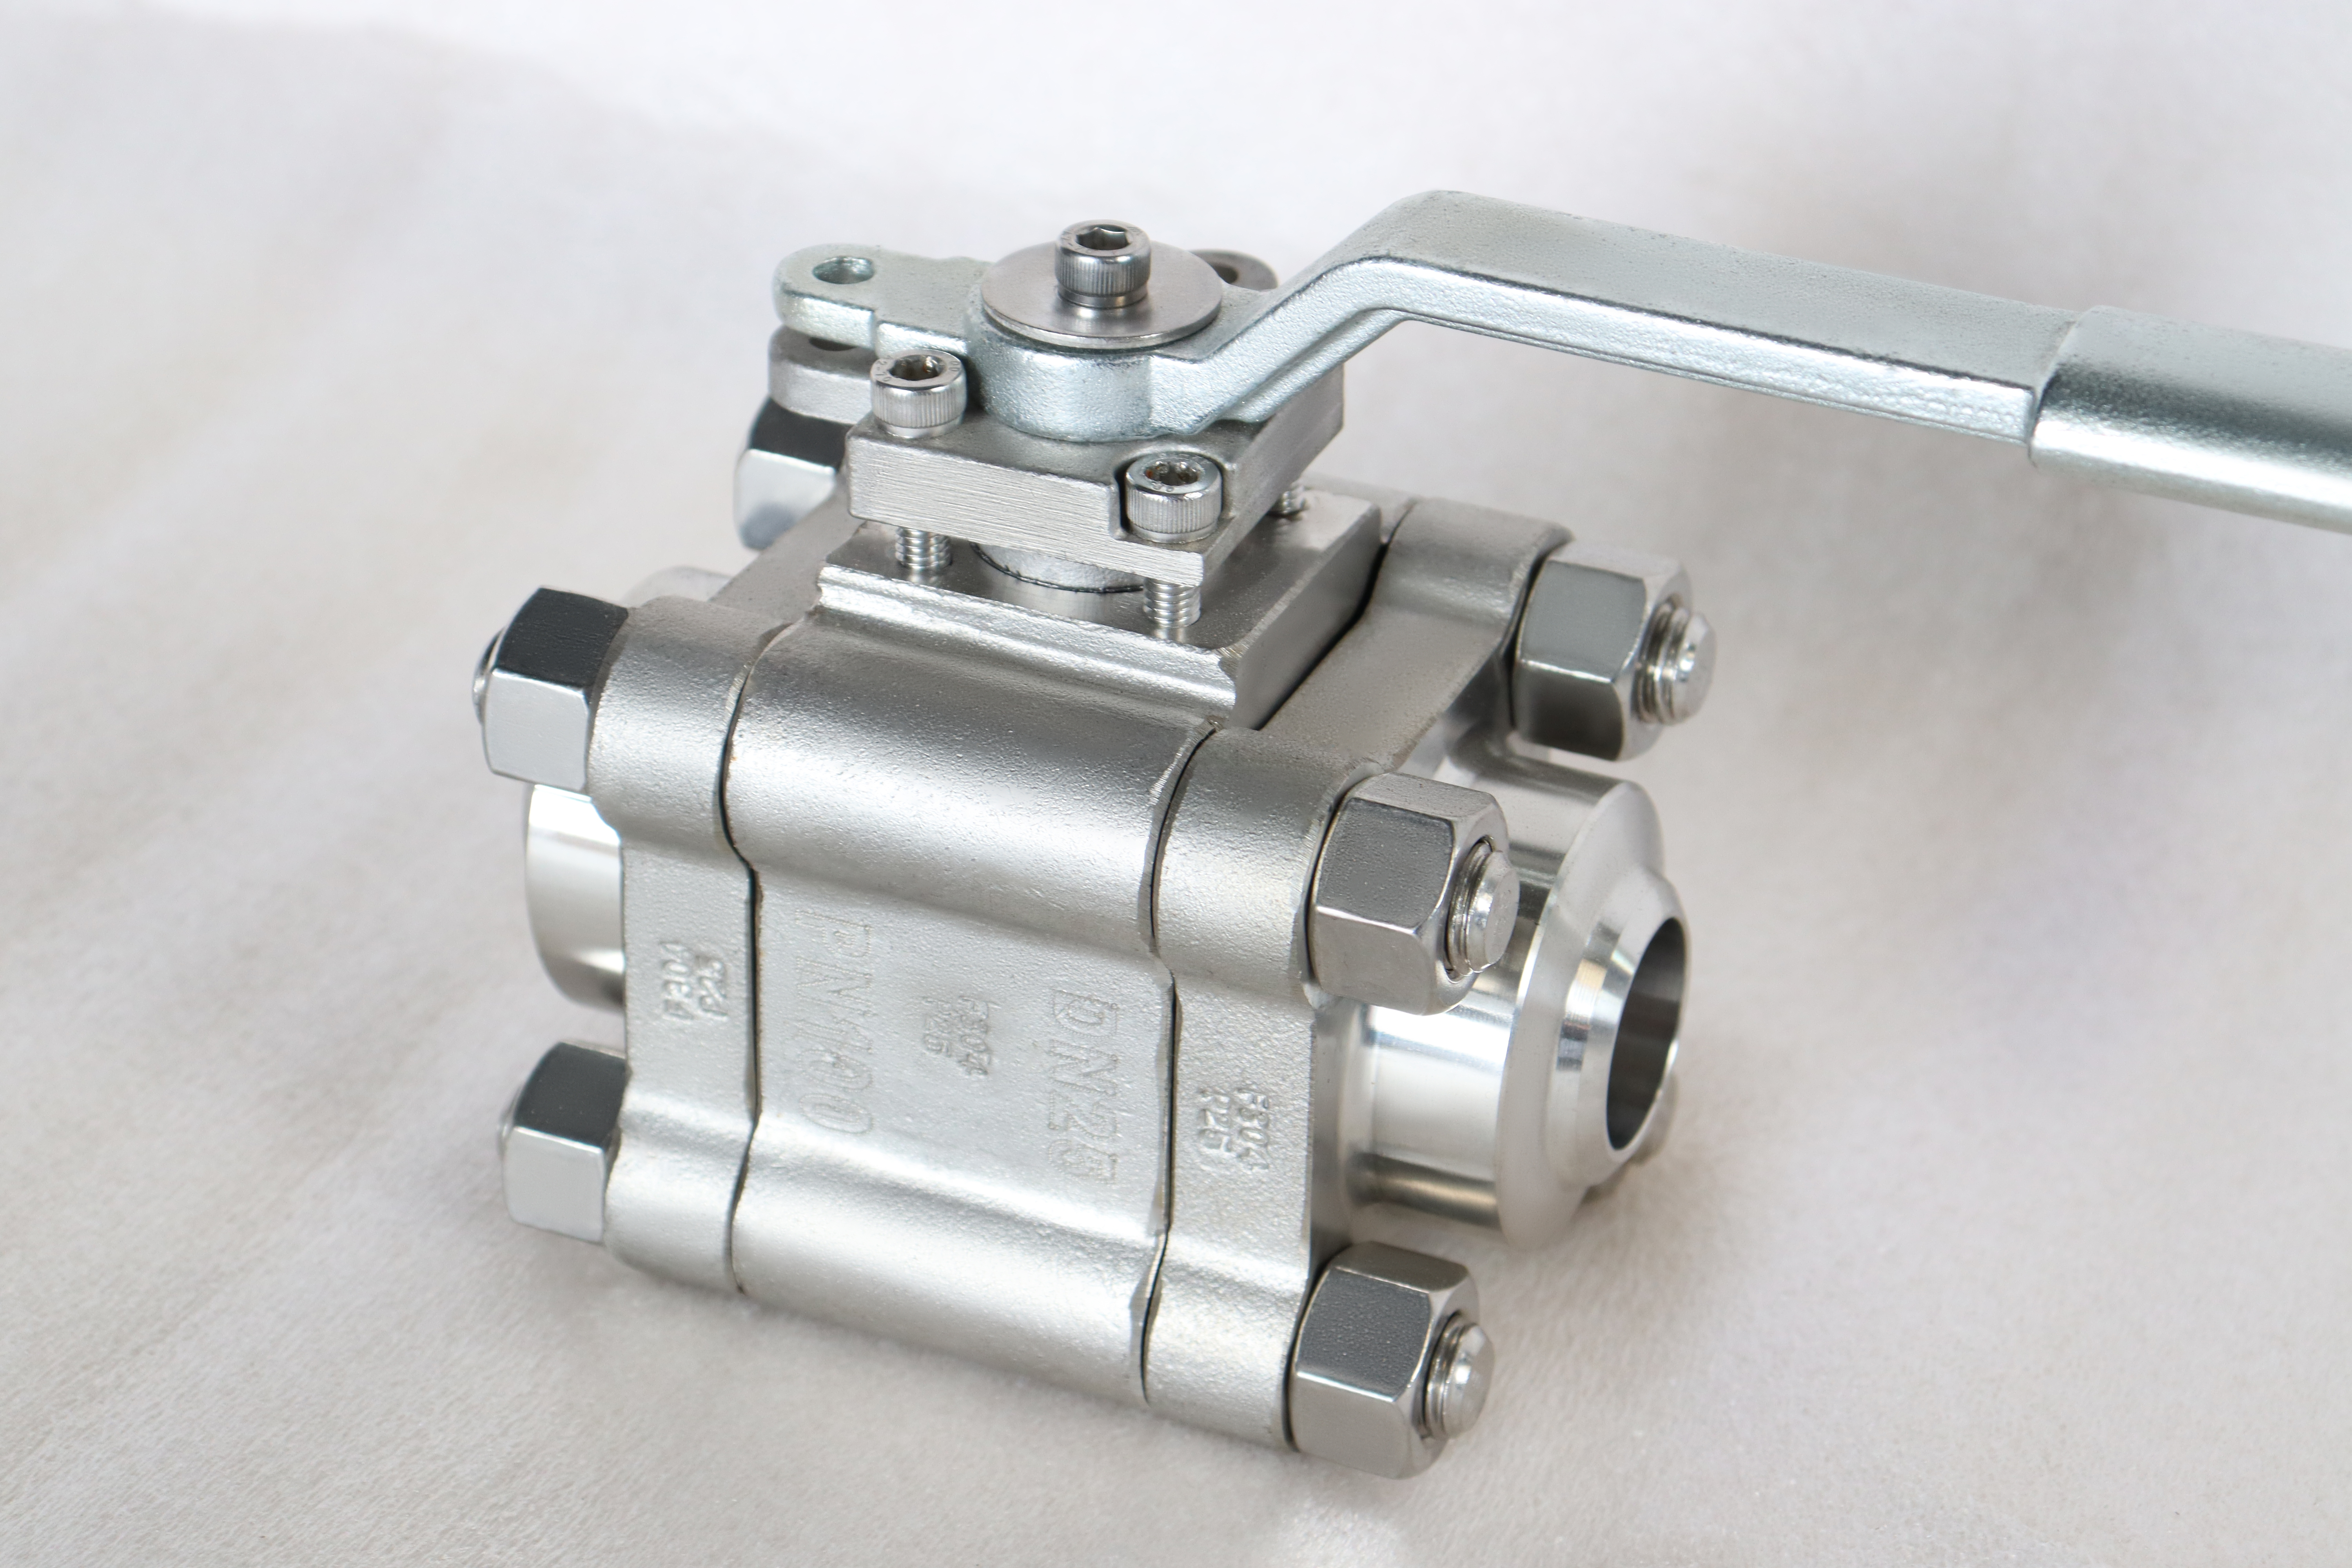
A one inch valve does not look like much on a skid: DN25, PN100, a forged A182 F304 body in three bolted sections, a lever with a locking device, and a square pad on the bonnet where a small actuator can be mounted later. The ends can be threaded, socket welded or butt welded, and that choice changes the machining rather than the pressure capacity. What does not change is that the seal is made by two polymer rings, one at each end of the ball, and nothing else.
Nothing in that list is where these valves actually fail. A Class 600 body in forged stainless is thick enough that the rating never comes into question, and the ends are proven by the same hydrostatic test that proves every other valve on the skid. The two rings are the whole story: polymer parts, sitting in machined pockets, asked to hold a pressure roughly four times what an identical bore would see at Class 150.
This page is therefore organised around the ring rather than around the body. It covers how the ring is held in place, which compound suits which temperature, what the standards do and do not fix, and the short list of facts an enquiry has to carry so that the valve arrives with the right ring inside it. Buyers who already know the size and only want the rating table will find it in the specification section.
Design and Construction
The ball in this design has no shaft of its own. It is trapped between the two rings with a fraction of a millimetre of freedom, and once the line is pressurised the upstream half of the ball takes the full load and the ball is pushed onto the downstream ring. That is the seal, and it produces an asymmetry worth remembering: while the valve is shut, the upstream ring is doing no sealing work at all, and the tightness of the valve is decided entirely by the ring on the outlet side.
Because the load arrives from the line, the ring has to be held against it. Polymer under sustained compression stops behaving like a spring and starts behaving like a very stiff liquid: it migrates, slowly, into any void within reach. The void here is the radial clearance between the outer diameter of the ring and the wall of the pocket. A ring simply dropped into a pocket creeps into that gap; a ring backed up around its outside diameter has nowhere to go. That backing is what the drawing shows as a shoulder or a separate support ring.
Four bolts hold the three sections together and a gasket closes each joint. Those joints are meant to be opened, so they belong in the maintenance plan as serviceable pressure boundaries: a fresh gasket every time, and the bolt load the drawing states, taken up in a cross pattern rather than round in a circle. In return the ball and both rings come out with the valve still piped in, which on a welded instrument run is the difference between a shutdown and a maintenance window.
Turning effort comes from the same pressure that makes the seal, because it is the friction of the ball against the loaded ring. At DN25 that effort stays inside what a hand lever can deliver at any rating, so no gearbox is needed; on larger bores the same arithmetic is what forces a trunnion or an operator. The stem is shouldered so that pressure cannot push it out, carries an anti static path into the body, and its top is squared under the bonnet pad for a miniature actuator.

Material Options
F304 is the body grade here: forged austenitic stainless, eighteen chromium and eight nickel, non magnetic, tough at low temperature, resistant to fresh water and to the atmosphere. F304L is the version for welded ends, since the lower carbon leaves the heat affected zone less prone to sensitising. F316 and F316L add molybdenum and are chosen where the medium carries chlorides. All four are forgings rather than castings, and that is part of where the pressure capacity comes from.
The trim follows the body, but the ring follows the temperature. A soft seated valve is the default, and the compound is what decides how hot it may run: PTFE for clean cold duty, RPTFE as the temperature climbs, PPL where it climbs further, and a metal seat with flexible graphite once no polymer will survive. Ball in solid F304, bare or nickel plated, with hard chrome where the medium is mildly abrasive; stem in F304 or F316, in 17-4PH where the valve is cycled hard.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Body and end caps | ASTM A182 F304 forged stainless | F304L, F316, F316L | three bolted pieces, each forged |
| Ball | Solid F304 | F304 with ENP, hard chrome | one sealing face, lapped |
| Stem | F304 | F316, 17-4PH | blowout proof, retained by the body |
| Seat ring | PTFE or RPTFE in a confined pocket | PPL, metal with flexible graphite | the ring is supported so it cannot extrude |
| Body gasket | Graphite spiral wound with stainless hoop | Metal ring gasket | new gasket every time a joint is opened |
| Stem packing | PTFE V-ring | Flexible graphite with wire reinforcement | matched to the seat temperature |
| Body bolts | ASTM A193 B8 with A194 8 nuts | B8M with A194 8M nuts | four fasteners, two bolted joints |
| Anti static device | Spring loaded path from ball to stem to body | Not applicable | required by API 608 |
| Operator | Lever with locking device | Miniature pneumatic, electric | square pad on the bonnet for actuation |
Technical Specifications
The number buyers ask for first is the end to end length, and on this valve it is not published anywhere: with threaded, socket weld or butt weld ends the length is the one dimensioned on the signed drawing for the size and preparation ordered, and it changes when the preparation changes. Only a flanged version has a tabulated length, ASME B16.10. The rest of the envelope is fixed: DN25 bore, PN100 or Class 600, three bolted sections in forged F304, a lever with a locking device, shell and seat tests to API 598.
Two decisions have to be taken before anything is machined. The first is the end preparation, because a threaded valve and a butt weld valve stop being interchangeable the moment the pipe is in place. The second is the ring compound, because the body can take far more heat than any polymer inside it, so the finished valve is only as good as the soft part. Both belong in the enquiry, not in a telephone call a fortnight later.
| Item | Value |
|---|---|
| Nominal size | 1 inch (DN25) |
| Pressure rating | PN100 (Class 600) |
| Body construction | three piece, bolted, four fasteners |
| Ball support | floating, no trunnion |
| Body material | ASTM A182 F304 forged stainless steel |
| Body options | F304L, F316, F316L |
| Material group | ASME B16.34 group 3.1 austenitic |
| Rating at 38 C | Class 600 = 102.1 bar |
| Ball | solid F304 |
| Ball options | electroless nickel plating, hard chrome |
| Stem | F304 |
| Stem options | F316, 17-4PH |
| Temperature basis | set by the seat compound; body group 3.1 rated to 538 C |
| Seat | PTFE or RPTFE, confined in the pocket |
| Seat options | PPL, metal with flexible graphite |
| Packing | PTFE V-ring |
| Packing option | flexible graphite with wire reinforcement |
| Body gasket | graphite spiral wound with stainless hoop |
| Body bolts | ASTM A193 B8 with A194 8 nuts |
| Bolt option | B8M with A194 8M nuts |
| Bore | full port, DN25 |
| End connection | NPT female to ASME B1.20.1 |
| End options | socket weld to ASME B16.11, butt weld to ASME B16.25 |
| Face to face | as drawn; the flanged version follows ASME B16.10 |
| Wall thickness | ASME B16.34 |
| Design standard | ASME B16.34 and API 608 |
| Fire safety | API 607 where ordered |
| Pressure testing | API 598 shell and seat, both directions |
| Operator | lever with locking device |
| Mounting pad | square pad with four tapped holes on the bonnet |
| Anti static | spring loaded path from ball to stem to body |
| Marking | size, class, F304 and heat number on the body and nameplate |
| Documentation | EN 10204 3.1, test record, general arrangement drawing |
Standards and Compliance
Class 600 sits at 102.1 bar in the ASME B16.34 table at 38 degrees Celsius, and the standard does two jobs on this page: it fixes the wall thickness of the body and it sets the pressure temperature rating. F304 appears there under material group 3.1, whose curve spans minus 254 to plus 538 degrees, far wider than any polymer ring allows, which is the point the rating table does not make for you.
Two designations, one step: PN100 is the European label and Class 600 the American one, and API 6D prints them on the same line of its pressure designation table. Reading that table is where confusion starts, because PN100 also exists as a flange size under EN 1092-1, and an EN 1092-1 PN100 flange will not bolt to an ASME B16.5 Class 600 flange: the same name for the pressure, a different bolt circle for the joint. Here the ends are threaded or welded, so the designation stays a rating label. Fire safety, when ordered, is to API 607.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Wall thickness and rating | ASME B16.34 | group 3.1 austenitic, Class 600 = 102.1 bar at 38 C |
| Ball valve specifics | API 608 | anti static path, blowout proof stem, nameplate content |
| Fire safety where ordered | API 607 | fire test certificate |
| Threaded ends | ASME B1.20.1 | NPT gauged |
| Socket weld ends | ASME B16.11 | socket depth and bore gauged |
| Butt weld ends | ASME B16.25 | end preparation drawing |
| Pressure testing | API 598 | shell at 1.5 times, seat at 1.1 times, both directions |
| Material certificate | EN 10204 3.1 | certificate per heat number |
Manufacturing Process
Each of the three sections begins as an A182 F304 forging, is solution annealed, and is then machined. The bore, the joint face and the ring pocket are finished in one setting, so that the ring sits square to the ball axis; a pocket a few hundredths out of square will show up months later as a weep that no amount of bolt torque will close. Pocket depth and the shoulder behind it are measured, not merely cut.
The ball is machined, ground, lapped and, where ordered, plated. The stem is cut with the drive slot and the anti static recess, and its gland thread is cut to take the packing load. Assembly runs in a fixed order: rings into the centre section, ball between them, end caps and gaskets, four bolts to the specified torque in a cross pattern, packing compressed, lever fitted, and the locking device checked against the lever before the valve leaves the bench.

Quality Control and Testing
Two tests are recorded on every valve, both to API 598: a shell test at one and a half times the rating, and a seat test at one point one times. On a floating design the second has to be run from both sides, because the seal only forms on the downstream ring; test it in a single direction and the upstream ring is never proven, which is how a valve passes on the bench and then weeps the first time the line is pressurised from the other end.
The rest of the record is dimensional and material. The thread is gauged to ASME B1.20.1, the socket to ASME B16.11 and the butt weld end to ASME B16.25; the bore is checked at DN25 and the pocket shoulder checked for depth; the heat number on the EN 10204 3.1 certificate is checked against the marking on the body. Breakaway torque is measured on the assembled valve and issued with the drawing, because that is the figure an actuator has to be sized on.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| Incoming forging | heat number and chemical composition | EN 10204 3.1 against A182 F304 |
| Machining | seat pocket squareness to the ball axis, joint face flatness | drawing tolerance, checked on a surface plate |
| Seat pocket | support shoulder depth behind the ring | drawing dimension, checked with a depth gauge |
| Ball finish | roundness and surface finish, plating thickness where plated | no blistering, finish within the drawing range |
| Thread or weld end | thread gauge, socket depth, bevel angle | ASME B1.20.1, B16.11 or B16.25 |
| Bore | bore against the DN25 nominal size | gauged through the assembled valve |
| Shell test | body, both bolted joints and the gland at 1.5 times | API 598, no leak |
| Seat test | each seat in both directions at 1.1 times | API 598, no visible leak |
| Torque | breakaway and running torque on the assembled valve | recorded and issued with the drawing |

Applications and Industry Service
The duty is small bore isolation where the pressure is high and the flow is small: chemical injection points, sampling and analyser systems, instrument air and nitrogen headers, hydraulic power packs, pilot plants and test rigs. On most of those the valve is one of twenty on a skid, and it is bought against a project specification that names the body grade, the end preparation and the ring rather than leaving the choice to the supplier.
It is the wrong valve for slurry, for throttling, and for a line that swings in temperature often enough to work a polymer ring loose. Dirty media belong to a metal seated valve; a throttling duty belongs to a control valve of some other type entirely. Writing that down before the order rather than after the first leak saves more money than any discount on the valve, and it is the part of a specification that is easiest to leave out.

Installation, Operation and Maintenance
On a threaded end use a sealant that suits the medium, and support the pipe run so that the valve body is never the support. On a socket weld end the heat is the risk, because the ring is only a few centimetres away: weld with the ball and rings removed, or with a heat sink clamped to the body, and never quench the weld with water while the valve is assembled. A butt weld end follows the same rule with a longer thermal path.
Operate the valve a quarter turn, fully open or fully closed. Part open, the edge of the ring sits in the flow and erodes, and on a small bore line the velocity is high enough to do that in weeks rather than years. If the lever becomes stiff, do not fit a longer handle: at this size a stiff lever usually means a deposit on the ball or a swollen ring, and the answer is to take the body apart and look.
How to Specify and Order
Seven items settle an order: size, rating, body grade, ball and ring trim, end preparation, operator. Written out for this valve they read: DN25, PN100 which is 600LB, body A182 F304, ball F304 with electroless nickel, ring RPTFE, NPT female ends to ASME B1.20.1, lever with locking device. Change one item and the machining changes with it; ask for socket weld to ASME B16.11 or butt weld to ASME B16.25 instead of the thread, and the end preparation has to be right on the first drawing, because it cannot be added to a finished body.
Send the medium, the design pressure and temperature, and whether the valve will be actuated. The medium decides the body grade, the temperature decides the ring, and the actuation decides whether the bonnet is machined with the pad and the stem top squared for a drive. A valve ordered without that pad cannot be actuated later without a new bonnet, and on a one inch valve the bonnet costs more than the valve did.
FAQ
Q: What holds the seat in at Class 600?
A: A shoulder or a backing ring behind the polymer, not the polymer itself. Under pressure a PTFE ring behaves like a very stiff liquid and creeps into any clearance it can reach, so the seat is supported on its outside diameter and the clearance behind it is kept small. That support is a drawing detail, and it is the first thing to check on a valve that starts weeping at the seat after a few months rather than at commissioning.
Q: Is PN100 the same as Class 600?
A: As a pressure designation, yes. API 6D lists PN100 against Class 600, and Class 600 is 102.1 bar at 38 degrees. As flanges they are not interchangeable: PN100 under EN 1092-1 and Class 600 under ASME B16.5 have different bolt circles. This valve has threaded or welded ends, so the designation only labels the rating and the ends are what the pipe has to match.
Q: Why is this valve not trunnion mounted?
A: Because at DN25 the floating design does the job better. The pressure acts on a small ball area, so the seat load and the breakaway torque stay inside what a hand lever can supply even at Class 600, and the seal gets tighter as the pressure rises. A trunnion earns its place when the bore grows, the class rises further, or the valve is cycled often enough that seat wear matters.
Q: Can the socket weld ends be welded with the valve assembled?
A: Not safely. The seat ring is a few centimetres from the weld and polymer does not survive welding heat, so the ball and seats come out first or a heat sink goes on the body. The same applies to the paint and the packing. Quenching the weld with water while the valve is assembled is the fastest way to crack a seat ring that was perfectly good.
Q: What temperature can the valve take?
A: The body is group 3.1 austenitic stainless and the B16.34 table runs from minus 254 to plus 538 degrees, but the valve will never see that range because the seat sits inside it. PTFE is good to about 150 degrees, RPTFE to about 180, PPL to about 280, and a metal seat with flexible graphite goes to the body limit. The seat compound decides, so it belongs in the order.
Q: Can it be actuated?
A: Yes, on a valve built for it. There is a square pad with four tapped holes on the bonnet and the stem top is machined to take a drive, so a miniature pneumatic or electric actuator mounts directly. Order it as a build rather than adding it later: a valve supplied without the pad and the drive cannot be converted without changing the bonnet, and on this size that costs more than the valve.


Hot Products


News
Ball Valves in Geothermal Brine: Silica Scale, Chloride Cracking And The Cooling Trap
Why geothermal brine destroys ball valves: retrograde silica scale, calcite at the flash point, chloride cracking above 60 C and the 250 C seat limit.
Read More
Ball Valve Face To Face Dimensions: Why A Correctly Ordered Replacement Still Does Not Fit
A 6 inch Class 150 ball valve can be 267 or 305 mm face to face and both are compliant. How B16.10, EN 558 and flange drilling decide whether it fits.
Read More
Ball Valve Stem Key And Keyway: What Gives Way First, And What The Handle Cannot Tell You
Between the handle and the ball there are four fits. Which one shears, which one cracks, and how a few degrees of lost motion hides a valve that never seated.
Read More
Ball Valve Datasheet: Six Blocks That Decide Whether Two Quotes Are Comparable
A ball valve datasheet only works when six blocks are fixed: pressure basis, bore, temperature ceiling, test, end connection, operator. How each is written.
Read More