


CHINA J-VALVES Offers Various High-quality I ndustrial Ball Valves
J-VALVES, a distinguished professional ball valve manufacturer rooted in China, takes pride in its extensive product portfolio. Our offerings span a wide range, including trunnion-mounted ball valves, floating ball valves, high-temperature ball valves, high-pressure ball valves, metal-sealed ball valves, ultra-low temperature ball valves, DBB ball valves, Three-way And Four-way Ball Valve, and fully welded ball valves. Each product is a testament to our commitment to precision engineering and reliable performance. Meticulously crafted, they are designed to not only meet but exceed the most stringent industrial demands, ensuring stable operation even under extreme conditions. This enables us to provide our clients with high-value services and makes our valves widely sought-after in industries.
Product Category
Contact Us


-
J-VALVES-Q41F
-
J-VALVES
Overview of the J-VALVES DN50x40 F2 Extended Stem Floating Ball Valve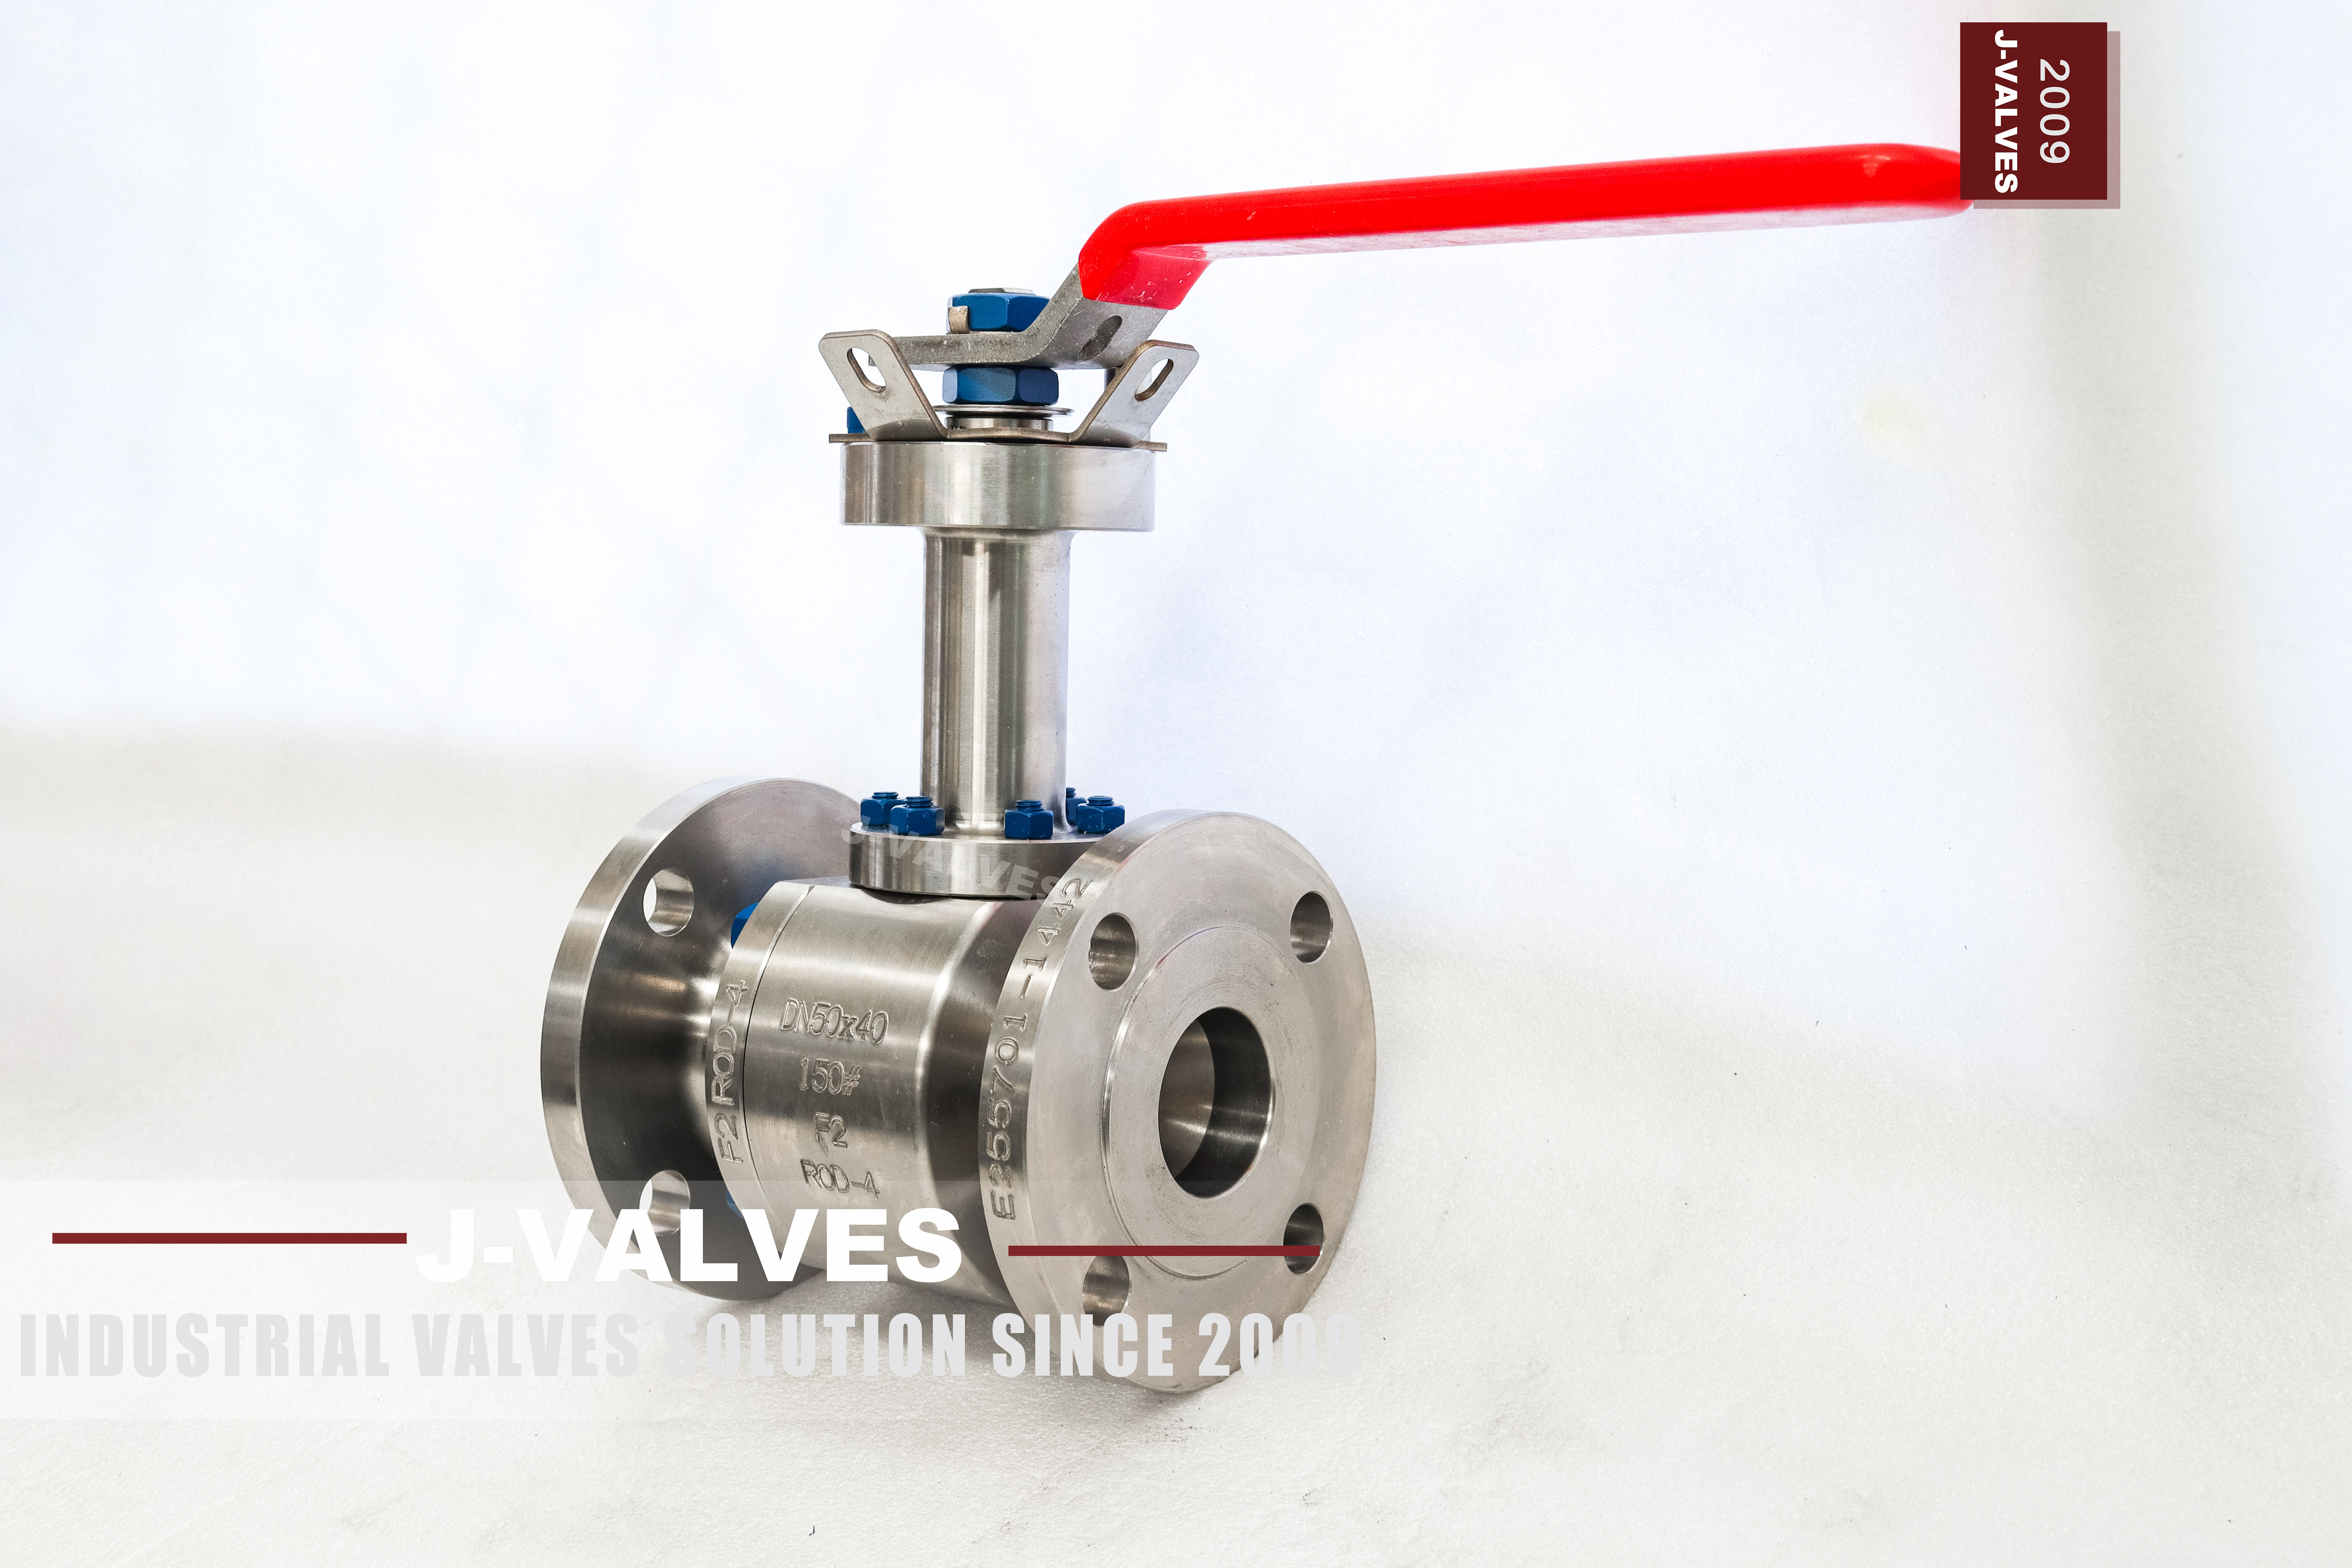
This is a two piece, flanged floating ball valve with a 2 inch body, a 1.5 inch bore and a stem long enough to put the lever outside an insulation jacket. The body is marked F2, Class 150, DN50 x DN40. It is a low pressure valve for chilled water, glycol, food grade liquid and weak solutions, and it is almost always ordered because the line is insulated or buried and the operator has to reach the valve.
One thing about the marking needs to be settled before anything else. F2 is a catalogue code, not an ASTM grade. It does not appear in ASTM A182, it does not appear in EN 10239 or in the UNS list, and it cannot be converted into a grade by adding a prefix. The alloy actually poured is declared on the EN 10204 3.1 certificate, and that certificate is the only document that says what the body is made of.
Design and Construction
The body splits at one joint with the end cap downstream, so the joint sits on the low pressure side while the valve is closed. At Class 150 the flange is a four bolt pattern at DN50 and the joint is a raised face with a spiral wound gasket, which is the cheapest sealing arrangement that works at this pressure and the one that most plants already stock.
The ball floats on line pressure and seals against the downstream seat, which means the seat load is set by the line pressure rather than by a spring. At Class 150 that load is small, the operating torque is low, and a lever at the top of a long extension is still easy to turn. This is the reason the extended stem works so well on a low pressure valve and becomes a torque problem on a high pressure one, where the same extension would need a gearbox to overcome the seat load.
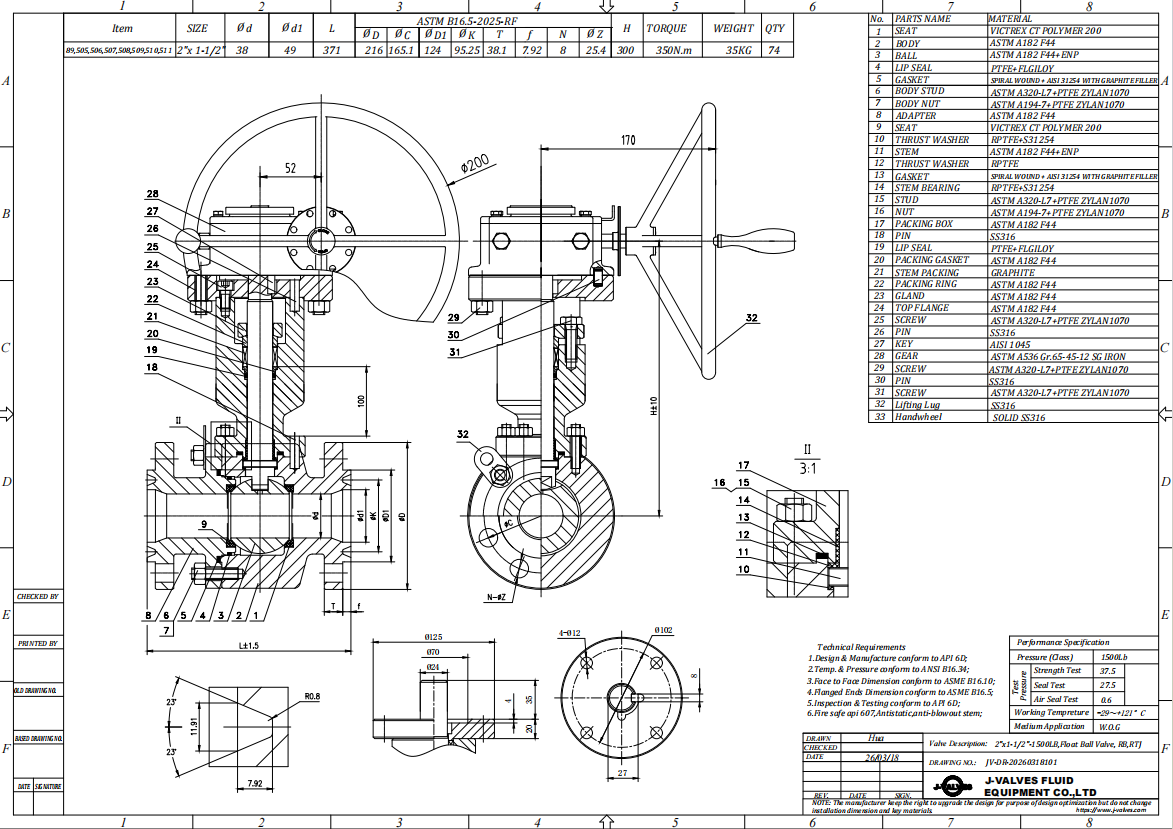
Material Options
The material question on this valve is not which stainless to choose, it is what the certificate says. A buyer can reasonably ask for a 304 or a 316 build, and the maker can build it, but the way to specify that is to write the grade on the order and have it declared on the certificate, not to read the grade out of the F2 code. Reading a grade into a catalogue code is how a valve ends up with a certificate that does not match the purchase order, and that is a documentation failure that surfaces at the customer audit rather than at the factory.
What the code does tell you is that the body is a forged stainless part rather than a carbon steel casting, which is consistent with the rest of the build: stainless ball, stainless stem, PTFE seat, stainless or B7 bolting. On a washdown duty or a food line, stainless studs are worth specifying, because B7 studs in a wet stainless flange corrode at the thread and gall on removal.
| Component | Standard Material | Optional Upgrade | Service Notes |
|---|---|---|---|
| Main body | F2 forged stainless steel, catalogue code | Grade declared on the 3.1 certificate | Forged body, no weld in the pressure boundary |
| End cap | F2 forging | Same heat as the main body | Carries the downstream seat |
| Ball | F2 or stainless, hard chrome | Stainless ball with ENP | Lapped after the joint closes |
| Stem | Stainless steel | 17-4PH where a harder stem is wanted | Blowout proof shoulder above the packing |
| Stem extension | Stainless tube with a guide bush | Length to the insulation thickness | Moves the operator, not the packing |
| Seat | PTFE | RPTFE, PPL | Sets the temperature ceiling of the valve |
| Packing | PTFE V rings | Flexible graphite | Adjusted at the body gland |
| Joint gasket | Spiral wound, graphite filler | PTFE envelope for clean service | Single use item |
| Bolting | A193 B7 with A194 2H | Stainless studs for a washdown area | Cross pattern, staged torque |
| Operator | Lever at the extension top | Worm gear or actuator | ISO 5211 pad at the top of the extension |
Technical Specifications
Three numbers define the valve. DN50 is the flange and DN40 is the bore, so the line connects at 2 inch and the flow passes through 1.5 inch. Class 150 is the rating, and its API 6D code is PN20. The extension length is the fourth number and it is the one that has to be measured on site: it is the insulation thickness plus clearance for the hand, taken from the body flange face to the top of the extension.
At Class 150 the wall is thin and the flange is light, so the valve is not a structural member and should not be used to pull pipe ends together. The face to face length follows ASME B16.10, but on an extended stem valve that figure describes the body; the overall length including the extension is a separate dimension and belongs on the drawing, otherwise the valve arrives too short or too long for the jacket that has already been built around the pipe.
| Item | Value |
|---|---|
| Product type | Two piece flanged floating ball valve, extended stem for insulated pipework |
| Nominal size | DN50 x DN40, 2 x 1.5 inch, reduced bore |
| Pressure class | Class 150 (marked 150LB), PN20 in the API 6D designation |
| Body material | F2 forged stainless steel |
| Material code note | F2 is a catalogue code, not an ASTM or EN grade designation |
| Grade declaration | The alloy grade is declared on the EN 10204 3.1 certificate |
| Body construction | Two piece, one bolted joint, end cap downstream |
| Ball | F2 or stainless, hard chrome plated |
| Stem | Stainless steel, extended through the insulation |
| Stem extension | Length to the insulation thickness, stated on the order |
| Extension guide | Guide bush at the top of the extension |
| Seat | PTFE, to 150 C on the data sheet |
| Seat option | RPTFE to 180 C, PPL to 280 C |
| Packing | PTFE V rings, flexible graphite option |
| Body joint gasket | Spiral wound with graphite filler |
| Bolting | A193 B7 with A194 2H, or stainless on request |
| End connection | Flanged raised face, ASME B16.5 Class 150 |
| End option | Ring type joint or butt weld ends |
| Face to face | ASME B16.10, body length and overall length stated separately |
| Bore | DN40 through the body, reduced from the DN50 flange |
| Design standard | ASME B16.34, API 608 |
| Test standard | API 598 |
| Temperature range | -29 to 425 C body, ceiling set by the seat |
| Low temperature option | Impact tested body for cold service |
| Media | Water, chilled water, glycol, food grade liquid, weak solutions |
| Operation | Lever at the top of the extension |
| Operation option | Worm gear, pneumatic or electric on the extension top |
| Anti static | Ball to body continuity, measured per valve |
| Marking | Size, class, F2 and heat number on the body |
| Traceability | EN 10204 3.1, with the grade and chemistry declared |
Standards and Compliance
The design follows ASME B16.34 for the wall and the rating and API 608 for the floating ball details: anti static path, blowout proof stem and nameplate content. The flange is ASME B16.5 Class 150, the length ASME B16.10, and the test API 598 with a shell test at one and a half times the rating and a seat test at one and a time the rating in both directions.
The standard that matters most on this valve is EN 10204 3.1, because it is the document that resolves the F2 code into an actual alloy. A 3.1 certificate is issued by the manufacturer with the results of the specific tests on the specific heat, and it is checked against the heat number stamped on the body. A certificate that names a grade but not a heat number cannot be tied to the valve in front of you, and that is the practical difference between 3.1 and 2.2 paperwork.
| Requirement | Standard | What J-VALVES Supplies |
|---|---|---|
| Wall and rating | ASME B16.34 | Forged wall tabulated for Class 150 in austenitic material |
| Valve design and marking | API 608 | Anti static path, blowout proof stem, nameplate content |
| Flange drilling | ASME B16.5 Class 150 | Four bolt pattern at DN50, raised face |
| Face to face | ASME B16.10 | Body length and overall length on the drawing |
| Pressure test | API 598 | Shell 1.5 times and seat 1.1 times the rating |
| Material certificate | EN 10204 3.1 | Grade and chemistry declared, which is how F2 is resolved |
| Identification | Positive material identification | Every body, read against the certificate chemistry |
| Actuator interface | ISO 5211 | Pad at the extension top, drive size on the drawing |
| Pressure code | API 6D clause 7.2 | Class 150 is PN20 |
Manufacturing Process
The body is forged and then solution annealed, which for an austenitic stainless forging is what restores the corrosion resistance after the hot work. It is machined as a pair so that the two halves of the joint line up when they are bolted together, and the seat pockets are cut in the same setting as the bore so the ball seats without shimming.
The extension is welded to the body neck at its base, which puts a weld in the pressure boundary, so that weld is penetrant tested and the assembly is pressure tested with the extension fitted. A leak at that weld appears inside the insulation where nobody looks, and by the time it is found the insulation is wet and the body is corroding under it. That is the reason the weld is tested rather than visually inspected.

Quality Control and Testing
Material identification is the check that carries the weight here. Because the code does not name an alloy, the body has to be identified positively and the result read against the certificate chemistry rather than against the stamp. Positive material identification is run on every body, and a body whose chemistry does not match the certificate is rejected as the wrong product rather than as a paperwork problem.
The mechanical checks are the standard set for a floating valve plus two for the extension: stem runout measured at the top of the extension with the valve assembled, and a pressure test of the extension weld at the same time as the body. Torque is measured at the top of the extension rather than at the stem, because that is where the operator applies it and the guide bush adds a little friction that a bare stem figure does not include.
| Step | What Is Checked | Standard or Acceptance |
|---|---|---|
| Chemistry | Grade against the certificate, not against the stamp | Spectrographic analysis per heat on the 3.1 certificate |
| Identification | F2 bodies against the declared grade | Positive material identification on every body |
| Extension runout | Stem square over the extension length | Dial gauge at the top of the extension |
| Shell test | Body, joint and extension base | 1.5 times the rating, held to API 598 |
| Seat test | Both directions | 1.1 times the rating, no visible leakage |
| Packing test | Stem seal at the rated pressure | No weep over the holding time |
| Flange drilling | Four bolt pattern against ASME B16.5 | Gauged, recorded per valve |
| Anti static | Ball to body continuity | Measured in ohms per valve |
| Torque | Breakaway torque at the top of the extension | Measured, issued with the drawing |

Applications and Industry Service
The valve is used on chilled water and glycol loops, food and beverage lines, deionised water, weak chemical solutions, and any line where the pipe is insulated and the valve has to be operated from outside the jacket. It is also used on buried lines where the valve sits in a pit and the stem comes up to a handle at grade, which is the same product with a longer extension and a different surface treatment.
It is the wrong valve for steam above the PTFE ceiling, for chlorides, and for anything at a pressure where the floating ball seat load would make the extension hard to turn. It is also the wrong valve where the extension would have to be horizontal, because the guide bush is designed for a vertical or near vertical load and a horizontal extension wears it on one side.

Installation, Operation and Maintenance
The extension is installed vertical or near vertical, and it is supported where it passes through the insulation rather than being held by the insulation. On a chilled line the extension is a thermal bridge: it carries cold up to the packing, and an extension without a vapour seal at the jacket is how a gland starts weeping condensation in summer. The seal belongs in the installation detail, not in the valve.
The packing is adjusted at the body gland, which means the insulation collar comes off for that job, and the collar should be built to come off without cutting the jacket. A seat change is a joint job: isolate, drain, take out the studs, lift the end cap, and the downstream seat and ball are accessible. The joint gasket is replaced every time the joint opens.
How to Specify and Order
An order should state DN50 flange with DN40 bore, Class 150, the grade required with a request that it be declared on the 3.1 certificate, the flange facing, and the extension length in millimetres from the flange face. If the grade is not specified, the certificate will declare whatever was poured, and that is only a problem if the purchase order expected something else.
Ask for the 3.1 certificate with the heat number and the actual chemistry, the pressure test record, the penetrant report on the extension weld and the measured torque at the top of the extension. A spare joint gasket and a seat pair cover the two items that fail first, and on a buried or insulated valve they are worth holding on site rather than ordering after a failure.
FAQ
Q: What grade is F2?
A: F2 is a catalogue code rather than an ASTM or EN grade. It does not appear in ASTM A182, EN 10239 or the UNS list, and it cannot be converted into a grade by adding a prefix. The alloy is declared on the EN 10204 3.1 certificate, and that certificate checked against the heat number is the only reliable statement of what the body is made of.
Q: Is F2 the same as 304 stainless?
A: Not on the evidence of the code. Writing F2 as A182 F304 would be a material declaration made without a basis, and it is exactly the kind of claim that fails at a customer audit. If a 304 body is required, specify 304 on the order and have it declared on the certificate; do not infer it from the code.
Q: Why is the stem extended on this valve?
A: To put the lever outside an insulation jacket or up to grade on a buried line. The packing stays in the body, so the extension moves the operator rather than the seal. That is why a weeping gland on this valve is still a body job and not something adjusted at the top of the extension.
Q: What does DN50x40 mean?
A: The first number is the flange size and the second is the bore. This valve bolts to a two inch line and passes a 1.5 inch bore, so it is a reduced bore design. The two numbers are not two end sizes, and the pressure drop across the reduction should be checked against the duty before the valve is ordered.
Q: How long should the extension be?
A: The insulation thickness plus clearance for the hand, measured from the body flange face to the top of the extension. It is a site dimension rather than a standard part, which is why it belongs on the drawing and why a valve ordered without it arrives with an extension that fits nothing in particular.
Q: Is Class 150 the same as PN20?
A: Yes. API 6D clause 7.2 lists PN20 against Class 150. The valve is marked with the class and flanged to ASME B16.5 Class 150, which is a four bolt pattern at DN50 and is not the same as a PN20 flange to EN 1092-1.


Hot Products


News
Ball Valves in Geothermal Brine: Silica Scale, Chloride Cracking And The Cooling Trap
Why geothermal brine destroys ball valves: retrograde silica scale, calcite at the flash point, chloride cracking above 60 C and the 250 C seat limit.
Read More
Ball Valve Face To Face Dimensions: Why A Correctly Ordered Replacement Still Does Not Fit
A 6 inch Class 150 ball valve can be 267 or 305 mm face to face and both are compliant. How B16.10, EN 558 and flange drilling decide whether it fits.
Read More
Ball Valve Stem Key And Keyway: What Gives Way First, And What The Handle Cannot Tell You
Between the handle and the ball there are four fits. Which one shears, which one cracks, and how a few degrees of lost motion hides a valve that never seated.
Read More
Ball Valve Datasheet: Six Blocks That Decide Whether Two Quotes Are Comparable
A ball valve datasheet only works when six blocks are fixed: pressure basis, bore, temperature ceiling, test, end connection, operator. How each is written.
Read More