

I. Introduction
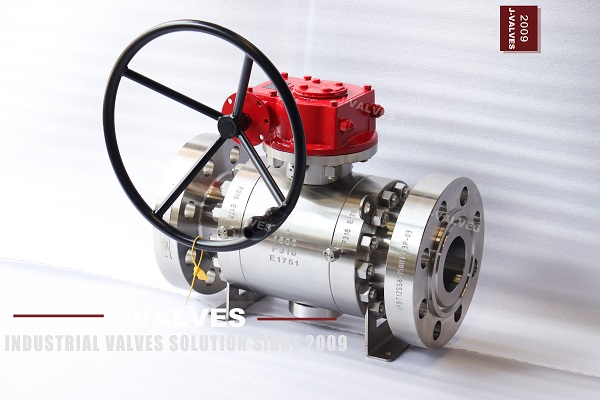
A trunnion ball valve is widely used in oil and gas, petrochemical, power generation, and industrial pipeline systems. Because it often works under high pressure, large diameter, and demanding operating conditions, pressure testing is one of the most important steps in valve quality verification.
For buyers, engineers, and inspection teams, understanding the Trunnion Ball Valve Pressure Test helps determine whether a valve is ready for service and whether it meets the required sealing and structural performance.
II. What Is a Trunnion Ball Valve Pressure Test?
A trunnion ball valve pressure test is a controlled test that applies pressure to the valve body and seats to verify strength, sealing performance, and leak tightness.
Common test items include:
Shell test
Seat test
Low-pressure sealing test
High-pressure sealing test
Backseat or special functional tests, when required
The exact procedure depends on the applicable standard, project specification, and customer requirements.
III. Why Pressure Testing Matters
Pressure testing is not only a factory inspection step. It is also a critical quality control process that confirms the valve can perform safely in real operating conditions.
1. It verifies body strength
The shell test helps identify casting defects, machining issues, weld problems, or structural weakness before shipment.
2. It confirms seat tightness
Seat leakage performance is essential for preventing internal leakage and maintaining system integrity.
3. It improves delivery confidence
A properly documented test report increases customer trust and supports final inspection and project acceptance.
4. It reduces operational risk
Valves that are not properly tested may fail in service, leading to leakage, downtime, and maintenance cost.
IV. Typical Trunnion Ball Valve Pressure Test Procedure
Although test details may vary by standard and manufacturer, a complete procedure usually follows these steps.
1. Pre-test inspection
Before pressurizing the valve, the inspector should confirm the valve condition, cleanliness, identification, and test setup.
Key checks include:
Correct valve model, size, and pressure class
Clean internal cavity
No visible damage to sealing surfaces
Proper test medium, gauges, and fixtures
Valve positioned in the correct open or closed state
2. Shell test
The shell test is used to verify the pressure integrity of the valve body. The valve is filled with the test medium and pressurized to the specified level. During the holding period, the body, end connections, and welded areas are checked for leakage, deformation, or other abnormal conditions.
3. Seat test
The seat test evaluates sealing performance after the valve is closed. Pressure is applied to one side of the valve, and leakage is monitored on the other side. For trunnion ball valves, seat tightness is especially important because it directly affects shutoff performance.
4. Bidirectional sealing check
Many trunnion ball valves are designed for bidirectional sealing or specific directional sealing requirements. Testing both flow directions helps confirm stable performance in real service conditions.
5. Result recording
After the test, the results should be documented, including pressure values, holding time, temperature, leakage status, inspector name, and final conclusion.
V. Acceptance Criteria
Acceptance criteria should always follow the project specification, purchase order, and applicable standard. In general, the following points are checked:
1. No visible body leakage
During the specified pressure and holding time, there should be no visible leakage from the body, flange, welds, or end connections.
2. Seat leakage within allowable limits
Seat leakage must remain within the permitted range defined by the relevant standard or customer requirement.
3. No structural abnormality
The valve should not show deformation, sticking, unusual noise, or operating failure during the test.
4. Complete documentation
A proper test report should include valve data, test medium, pressure levels, test duration, results, and sign-off records.
VI. Factors That Affect Test Results
Even a well-manufactured valve can show test variation if the setup is not correct. Common influencing factors include:
Dirty sealing surfaces
Incorrect test medium
Inaccurate pressure gauges
Poor fixture installation
Temperature changes during the test
Uneven assembly torque
This is why consistent procedures and clear documentation are essential.
VII. How to Improve Pressure Test Success
Manufacturers can improve test reliability through better design, machining, and assembly practices:
Use stable and suitable sealing materials
Improve ball and seat machining precision
Control assembly tolerances carefully
Maintain clean surfaces and proper finishing
Perform pre-shipment inspection before final testing
For buyers, choosing a manufacturer with a mature testing process and strong quality control system can significantly reduce project risk.
VIII. Common Questions
Why does the shell test pass but the seat test fail?
Typical causes include sealing surface damage, assembly error, contamination, or an unsuitable seat material.
Why does the pressure gauge fluctuate?
This may be caused by temperature changes, insufficient air removal, or minor leakage in the test circuit.
Why are bidirectional tests important?
Because many trunnion ball valves operate in systems with different flow directions, both sealing directions should be verified when required.
IX. Conclusion
The pressure test is one of the most important quality checks for a trunnion ball valve. A properly executed Trunnion Ball Valve Pressure Test, combined with clear acceptance criteria, ensures the valve is ready for reliable industrial service.
If your project requires dependable valve performance, paying attention to test procedures, sealing integrity, and quality documentation will help you choose a better product and reduce long-term operating risk.